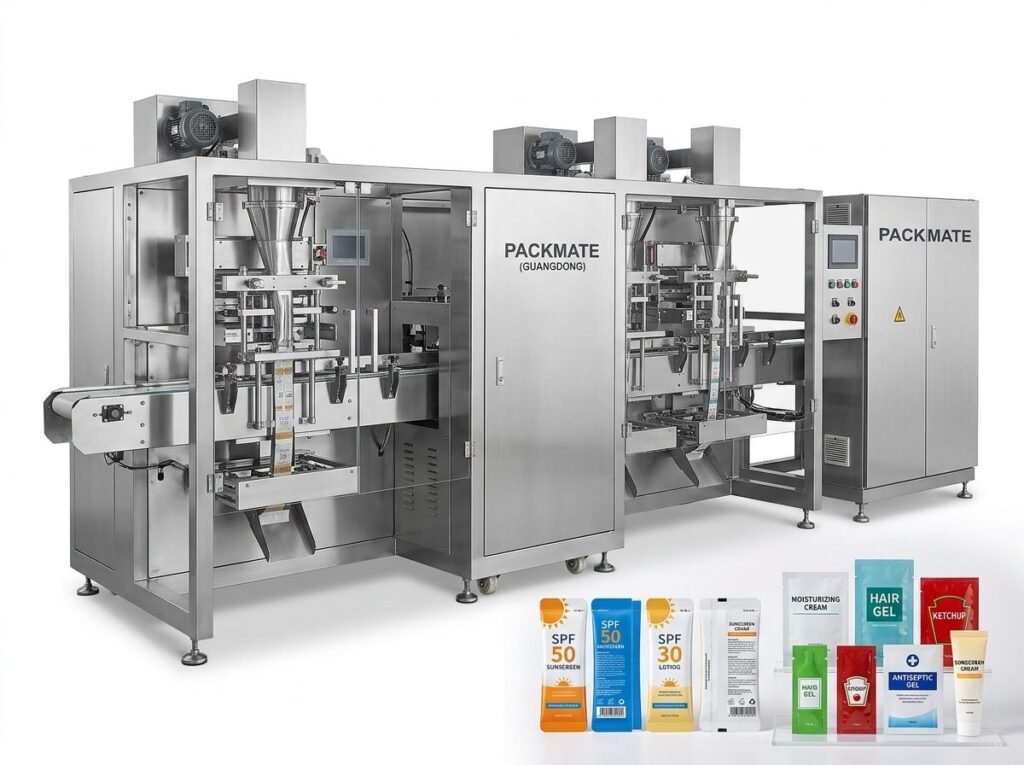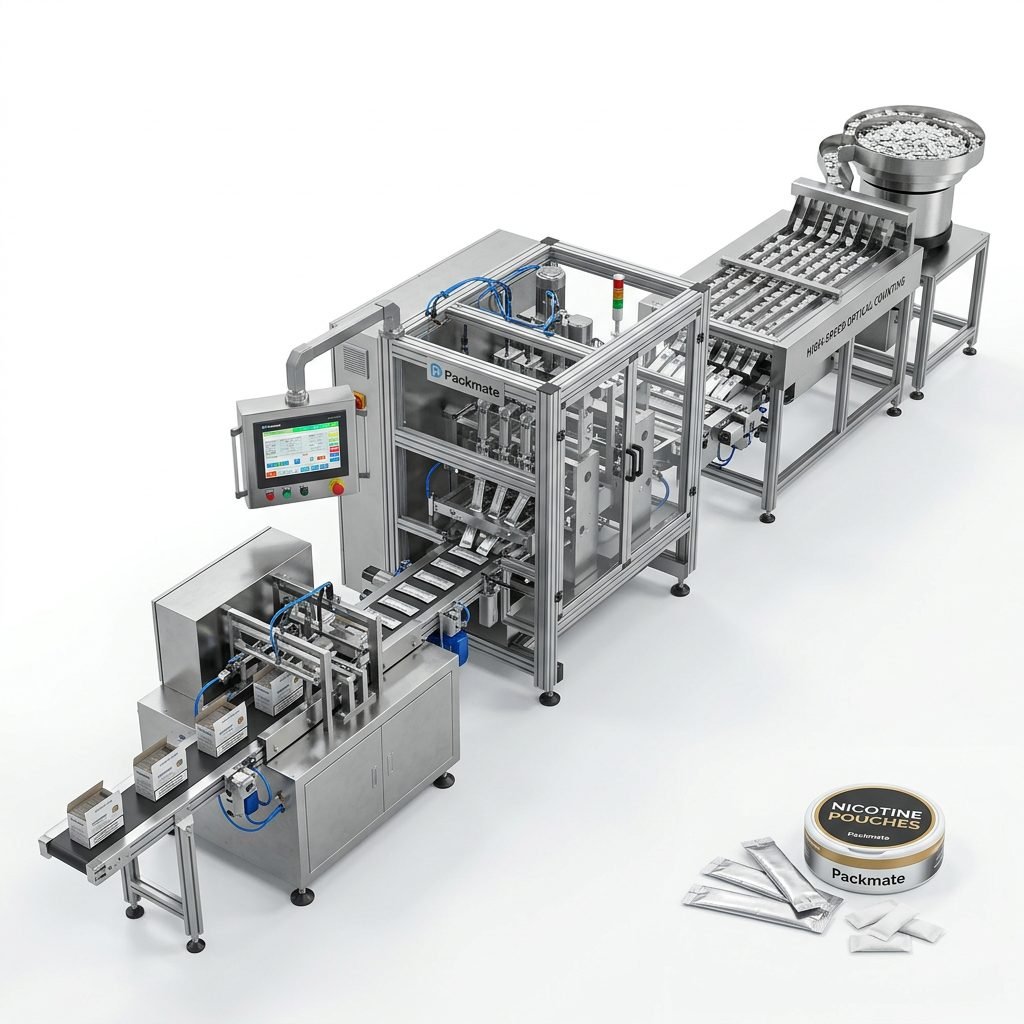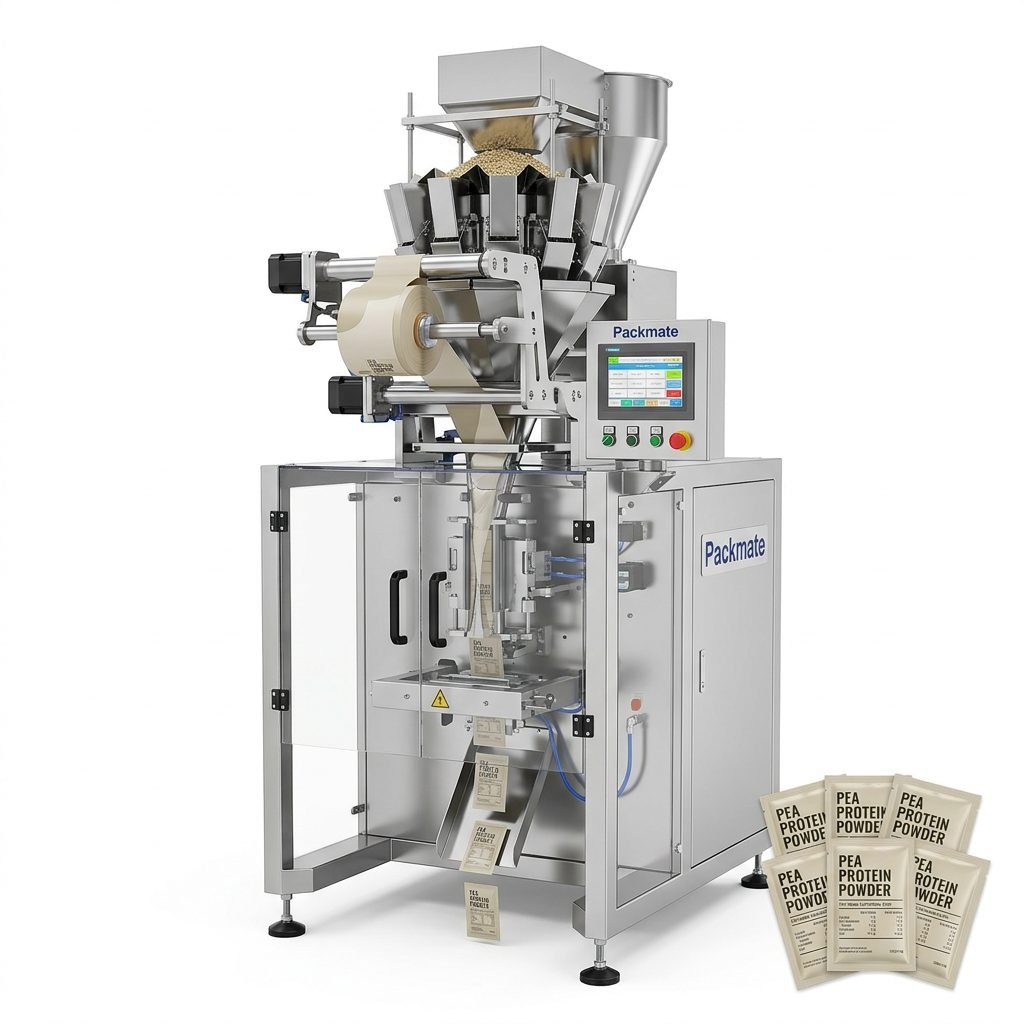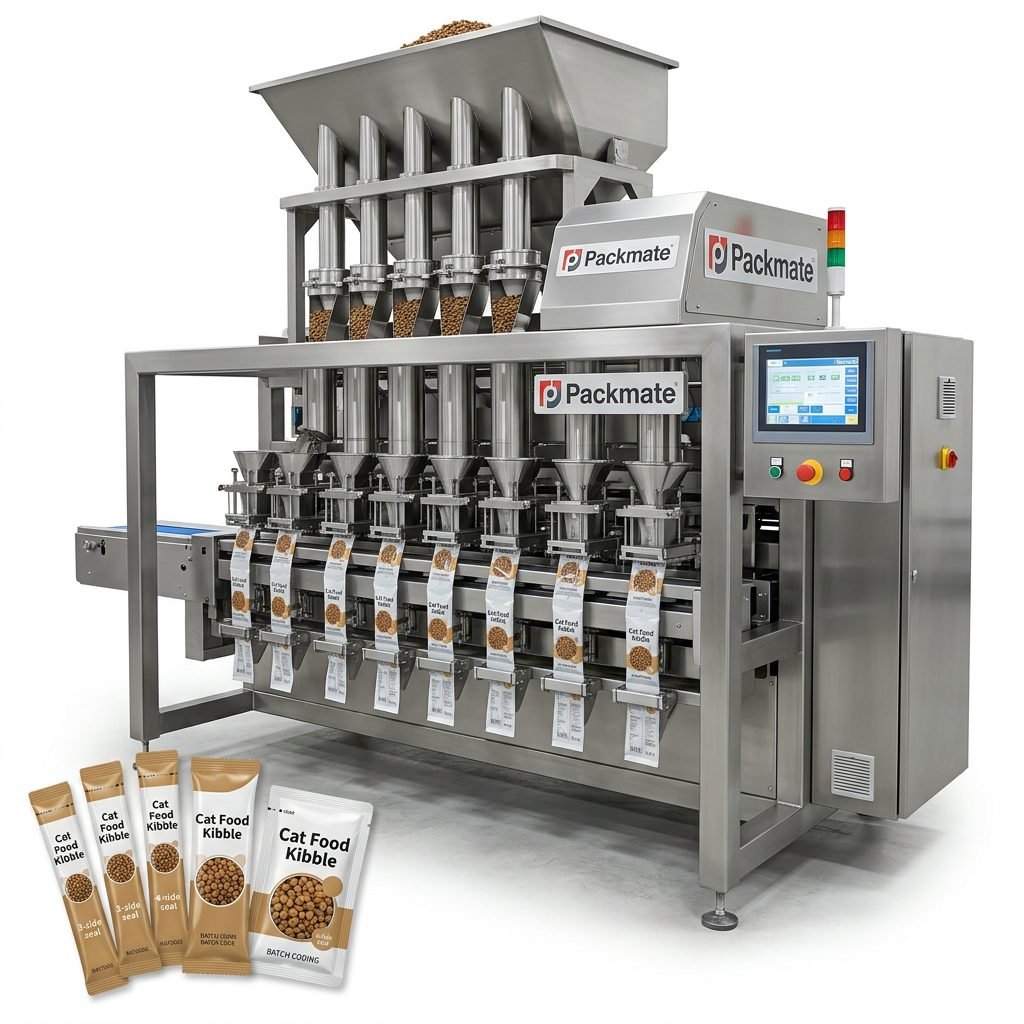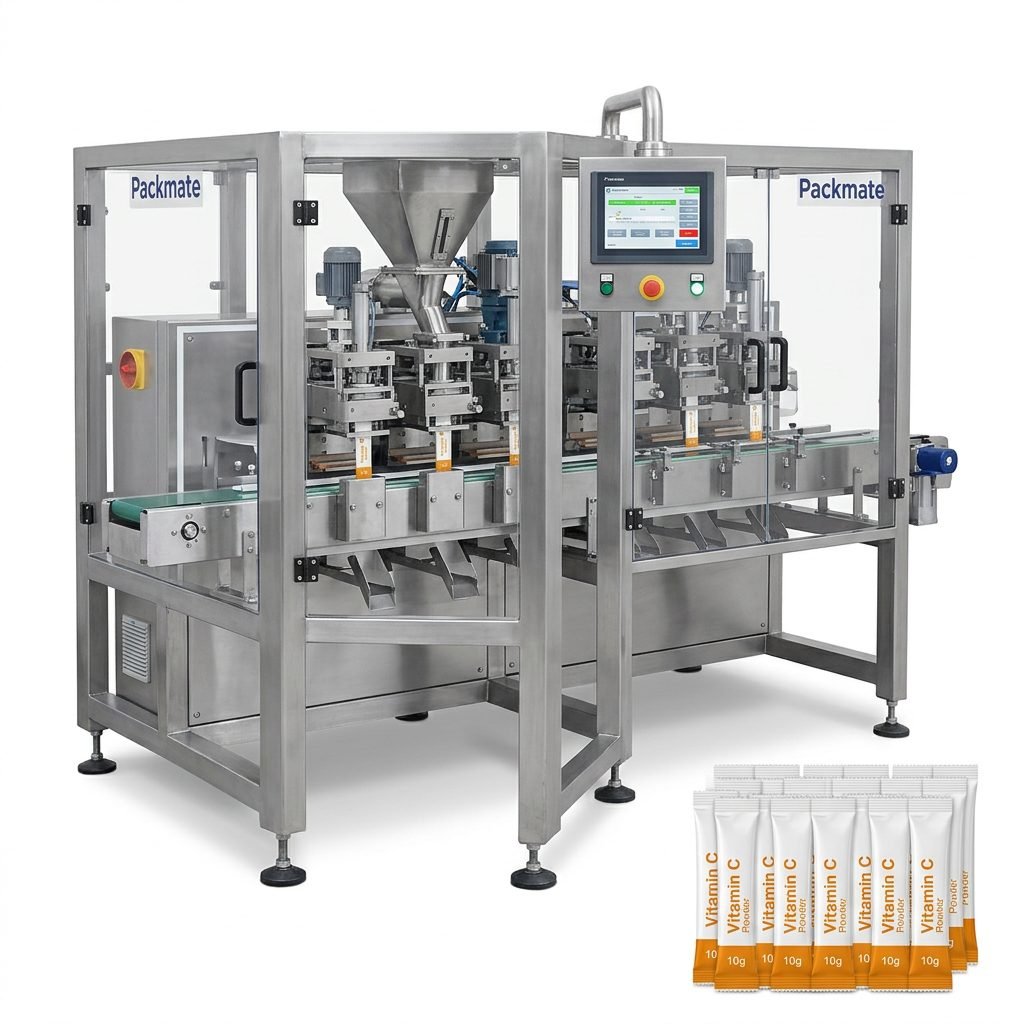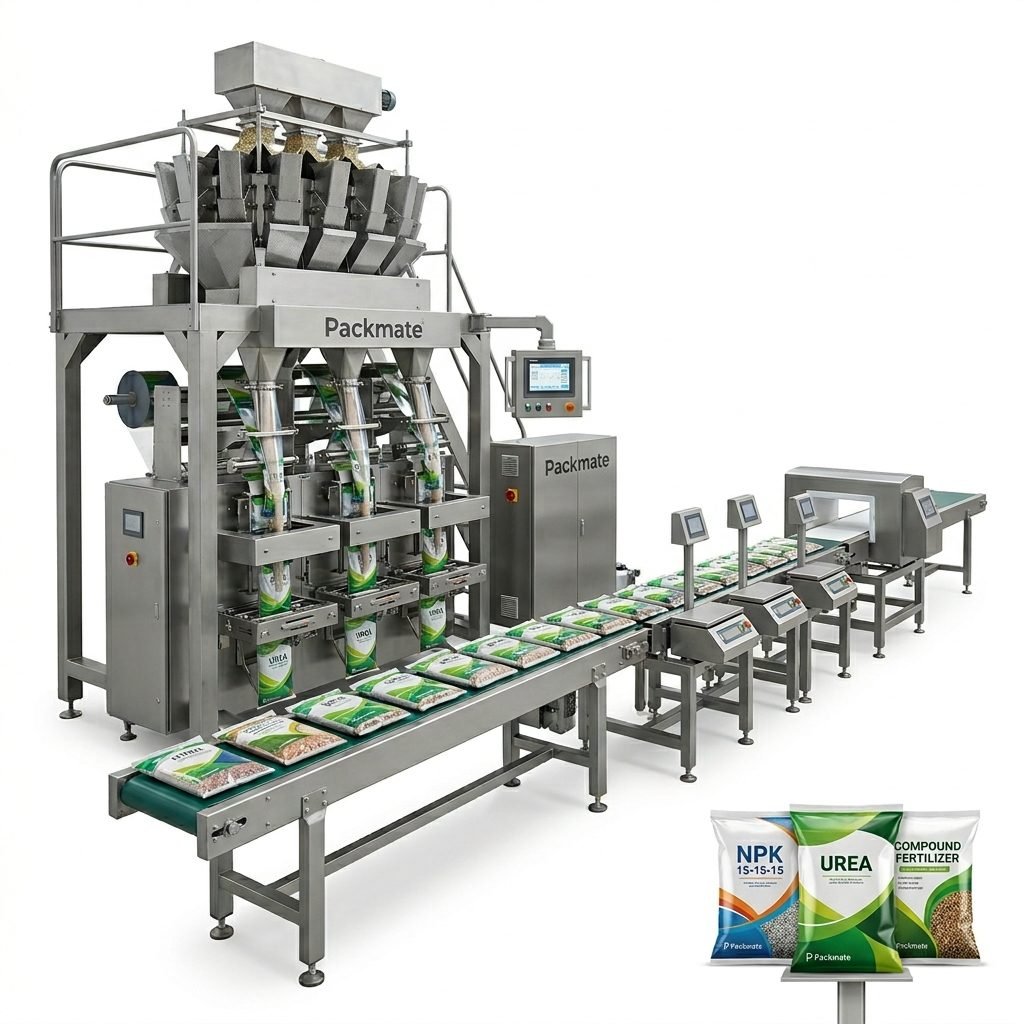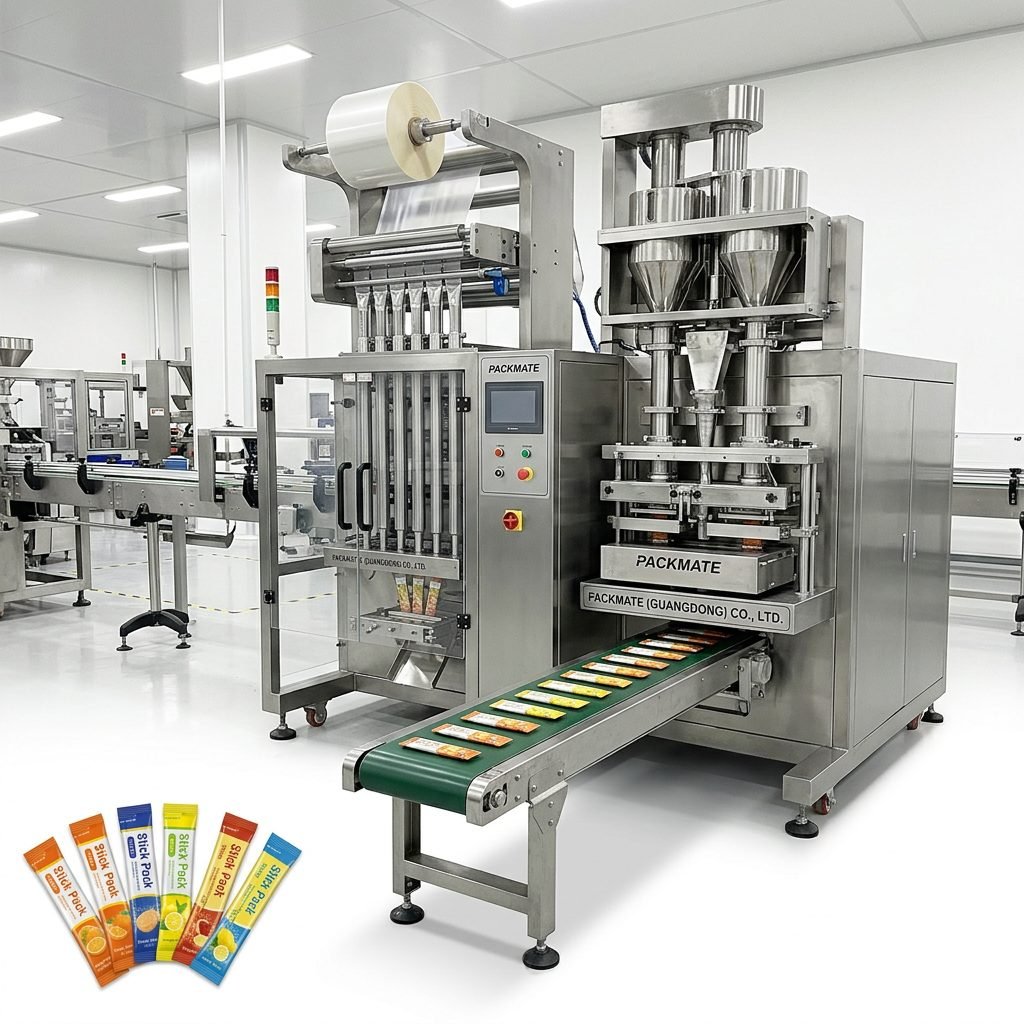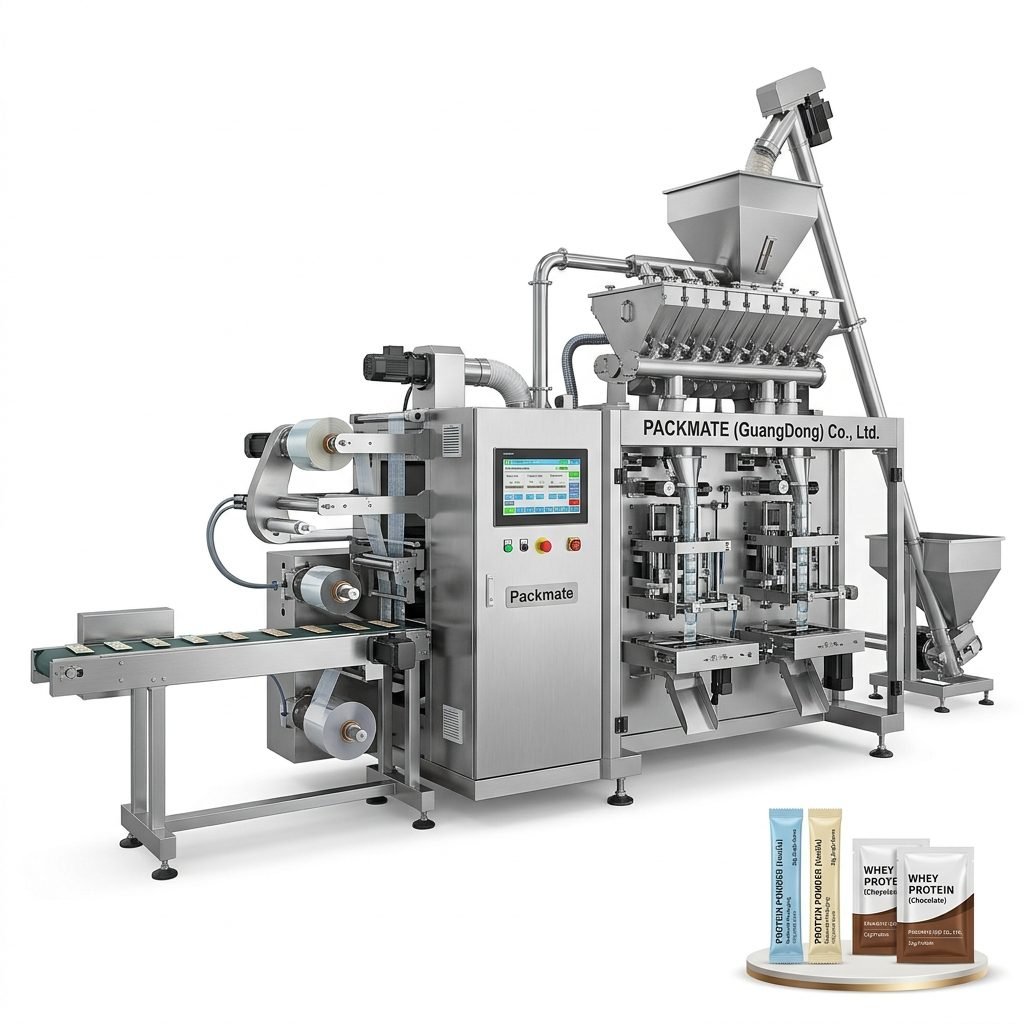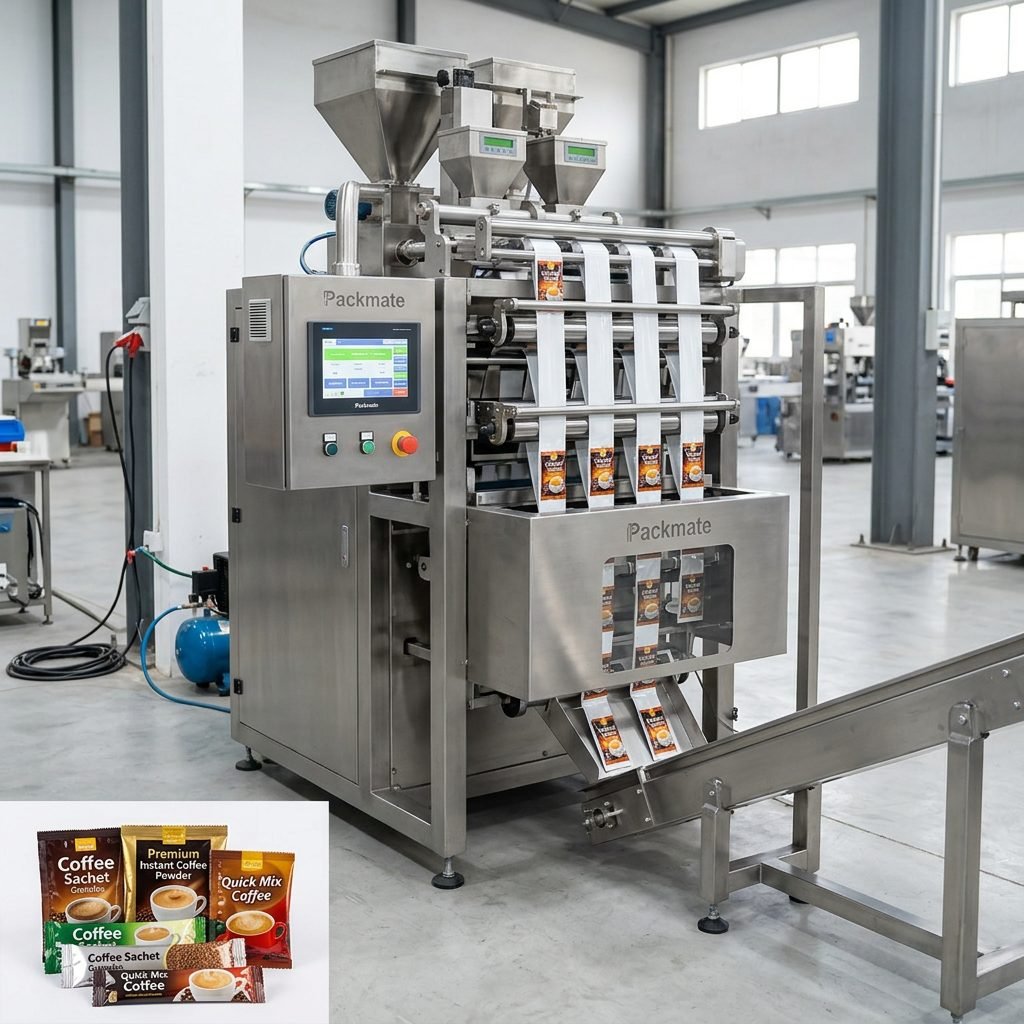
In today’s competitive manufacturing landscape, efficiency, hygiene, and scalability are not just advantages—they are necessities. For producers in the food, pharmaceutical, and health product sectors, the packaging line is the critical final link in the supply chain, directly impacting product integrity, brand reputation, and operational costs. This is where the concept of a turnkey packaging line solution becomes a game-changer. It represents a comprehensive, ready-to-operate system designed to handle everything from product feeding to final cartoning, all provided by a single, trusted partner.
What is a Turnkey Packaging Line Solution?
A turnkey solution is a complete, integrated system delivered to your facility, fully assembled, tested, and ready for production. Unlike purchasing individual machines from different vendors, a turnkey approach provides a seamless workflow. The provider handles the entire process: design, engineering, machine manufacturing, integration, installation, commissioning, and operator training. This eliminates compatibility issues, reduces project management overhead, and ensures a single point of accountability. For manufacturers, it means a faster path to market, predictable budgeting, and a system optimized for their specific product—be it protein powder sachets, effervescent tablet stick packs, or liquid health tonics in large-volume bags.
Core Benefits for Manufacturers
Streamlined Project Management: One vendor manages the entire project lifecycle, from initial concept to full production, saving you time and internal resources.
Guaranteed System Compatibility: All components—from fillers and sealers to conveyors and coders—are designed to work in perfect harmony, maximizing uptime and efficiency.
Enhanced Product Safety & Compliance: Solutions are built with industry-specific regulations in mind (e.g., FDA, cGMP for pharmaceuticals, HACCP for food), ensuring packaging integrity and traceability.
Scalability for Future Growth: A well-designed turnkey line can be modular, allowing for future expansion or reconfiguration as your product portfolio evolves.
Tailored Solutions for Critical Industries
The requirements for packaging food, pharmaceuticals, and health products, while sharing a need for precision and hygiene, have distinct nuances that demand specialized solutions.
Food Industry Packaging
Food manufacturers face challenges like preserving freshness, preventing contamination, and meeting high-speed production demands for items like spices, instant coffee, or soup mixes. Turnkey lines for food focus on hygienic design with easy-clean surfaces, robust sealing to prevent leakage and spoilage, and accurate filling to ensure consistent portion control. Solutions often include nitrogen flushing capabilities for extended shelf life and advanced checkweighers to guarantee every packet meets label claim.
Pharmaceutical & Nutraceutical Packaging
This sector operates under the strictest regulations. Packaging lines must ensure absolute product purity, precise dosing, and complete traceability. Turnkey solutions here incorporate features like cleanroom-compatible construction, dust extraction systems, and sophisticated vision inspection systems to check for fill level, cap presence, or label accuracy. Serialization and aggregation capabilities are also integrated to meet global track-and-trace mandates. Whether packaging powder supplements into stick packs or tablets into sachets, the system is validated to meet rigorous standards.
Health & Wellness Product Packaging
The booming market for vitamins, protein powders, and herbal supplements requires packaging that protects sensitive ingredients from moisture and light while appealing to health-conscious consumers. Lines are designed for gentle product handling to prevent degradation, high accuracy for premium ingredients, and flexible formatting for various pack types—from single-dose sachets to refillable pouches. Aesthetics are also key, with capabilities for high-quality printing and finishing.
Why Partner with an Experienced Turnkey Provider?
Selecting the right partner is as crucial as the technology itself. A provider with deep industry experience brings invaluable expertise to the table. For instance, a company like Packmate (GuangDong) Co., Ltd. leverages over 22+ years of company development to understand the unique pain points of each sector. Their journey, from a focused workshop to a modern facility spanning 20,000 ㎡, reflects a commitment to innovation and growth that directly benefits clients.
The Packmate Advantage: From Vision to Reality
Founded on a passion for automation, Packmate’s story is one of solving practical manufacturing challenges. This hands-on engineering mindset translates into solutions that are not only technologically advanced but also robust and reliable on the factory floor. With a portfolio of over 50 machine models and a professional team of 125+ members, they offer more than just equipment; they deliver a production asset. Their comprehensive solutions cover multi-lane stick pack machines, sachet packaging lines, and large-bag filling systems, ensuring a perfect fit for your product format and output goals.
Exploring their real-world case studies can provide tangible proof of capability across different applications and regions.
Key Considerations When Evaluating a Provider
1
Industry-Specific Expertise: Do they have a proven track record in your specific sector (food, pharma, health)?
2
Technical & Support Capability: What is the depth of their engineering team? What does their after-sales service and support structure look like?
3
Manufacturing & Quality Control: Do they control manufacturing in-house? Inquire about their quality certifications and testing protocols.
4
Project Transparency: Will they provide clear timelines, documentation, and communication throughout the project?
Implementing Your Turnkey Line: A Collaborative Journey
The implementation of a turnkey packaging line is a partnership. It typically follows these stages:
- Consultation & Needs Analysis: The provider works with you to understand your product, materials, desired output, and facility constraints.
- Line Design & Proposal: A customized line layout and technical specification is created, often including 3D simulations.
- Manufacturing & Factory Acceptance Test (FAT): The line is built and tested at the provider’s facility, where you can witness its performance before shipment.
- Installation & Site Acceptance Test (SAT): Expert engineers install the line at your plant, commission it with your actual product, and train your operators.
- Ongoing Support: A reliable partner offers continuous technical support, spare parts, and potential upgrade paths.
Frequently Asked Questions (FAQs)
1. What is the main advantage of a turnkey line over buying machines separately?
The primary advantage is single-source responsibility and guaranteed system integration. A turnkey provider ensures all machines work together seamlessly, handles all interfaces and controls, and provides one point of contact for service and support. This reduces technical risk, accelerates startup time, and simplifies maintenance.
2. How long does it typically take from order to full operation?
The timeline varies based on line complexity and customization, but a typical project ranges from 4 to 9 months. This includes design, manufacturing, FAT, shipping, installation, and SAT. A detailed project plan with milestones should be provided by your vendor during the quotation phase.
3. Can a turnkey line be modified if our product or output needs change in the future?
Yes, a key benefit of working with an experienced provider is designing for scalability and flexibility. Modular lines can often be upgraded with additional lanes, new functions (like inspection systems), or reconfigured for different pack sizes. Discuss future growth plans with your provider during the initial design phase.
4. How do you ensure the line meets our industry’s regulatory standards (e.g., FDA, cGMP)?
Reputable providers design machines with regulatory compliance in mind, using appropriate materials (e.g., food-grade stainless steel, FDA-compliant seals) and constructing them for easy cleaning and inspection. They provide necessary documentation (e.g., material certificates, design files) to support your validation process. It is crucial to specify your regulatory requirements upfront.
5. What kind of training and post-installation support can we expect?
Comprehensive operator and maintenance training is a standard part of a turnkey project. Support typically includes a warranty period, access to spare parts, remote technical assistance, and options for on-site service visits. Ensure you understand the details of the service level agreement (SLA) offered. For more queries, visit the dedicated FAQs page.