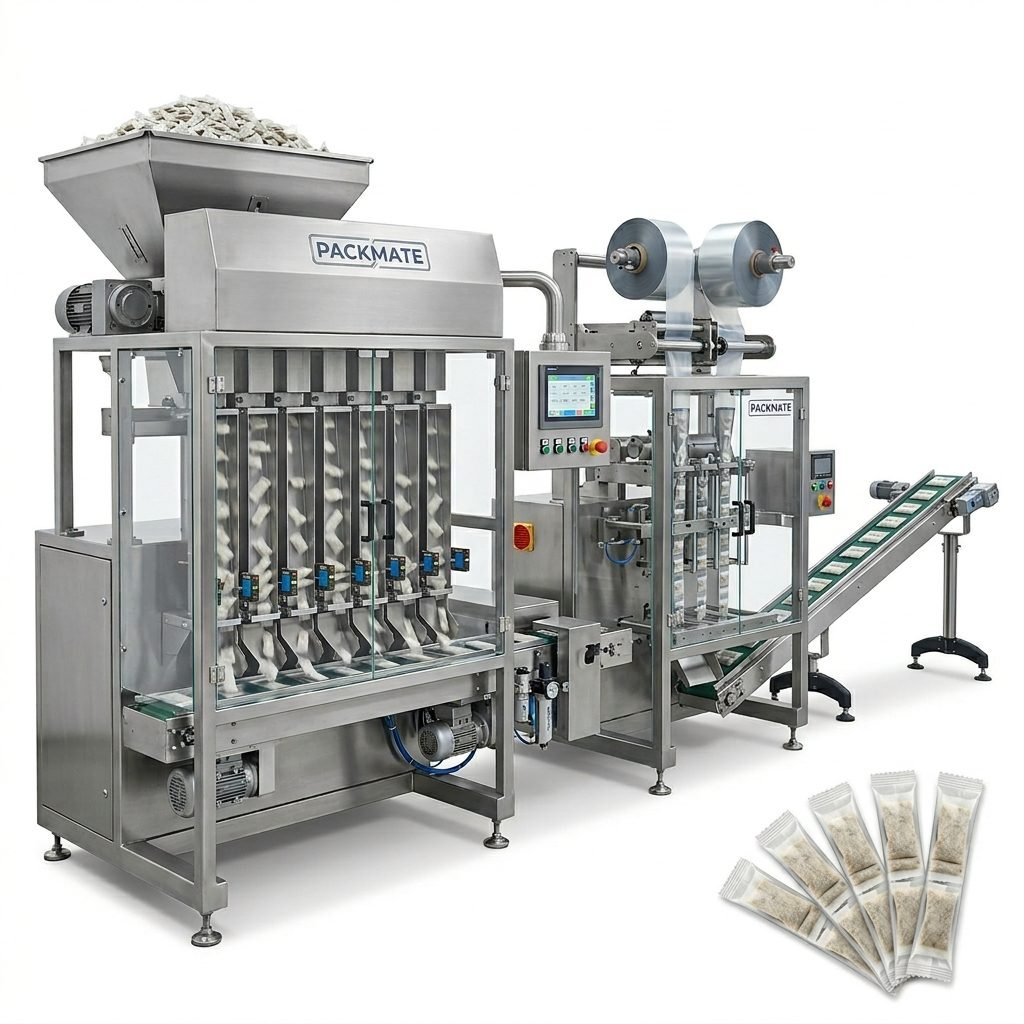
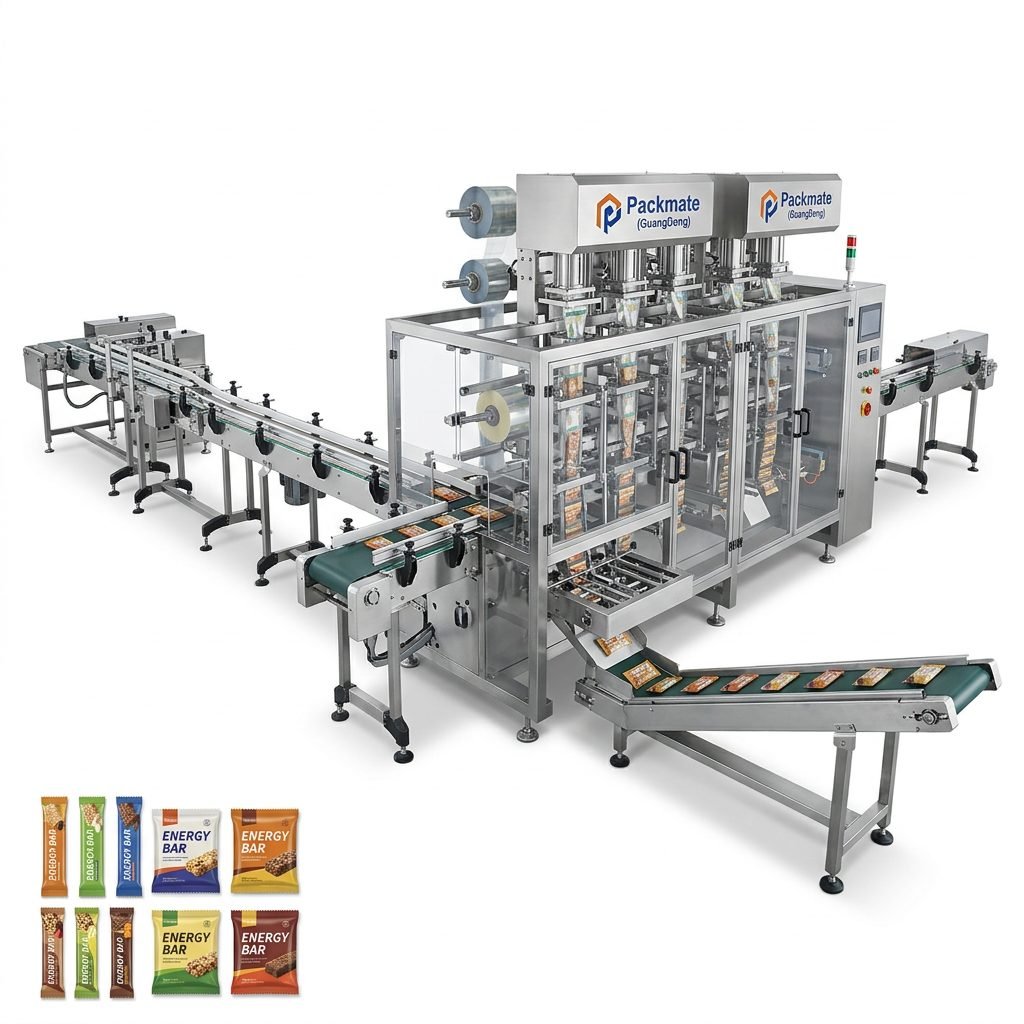
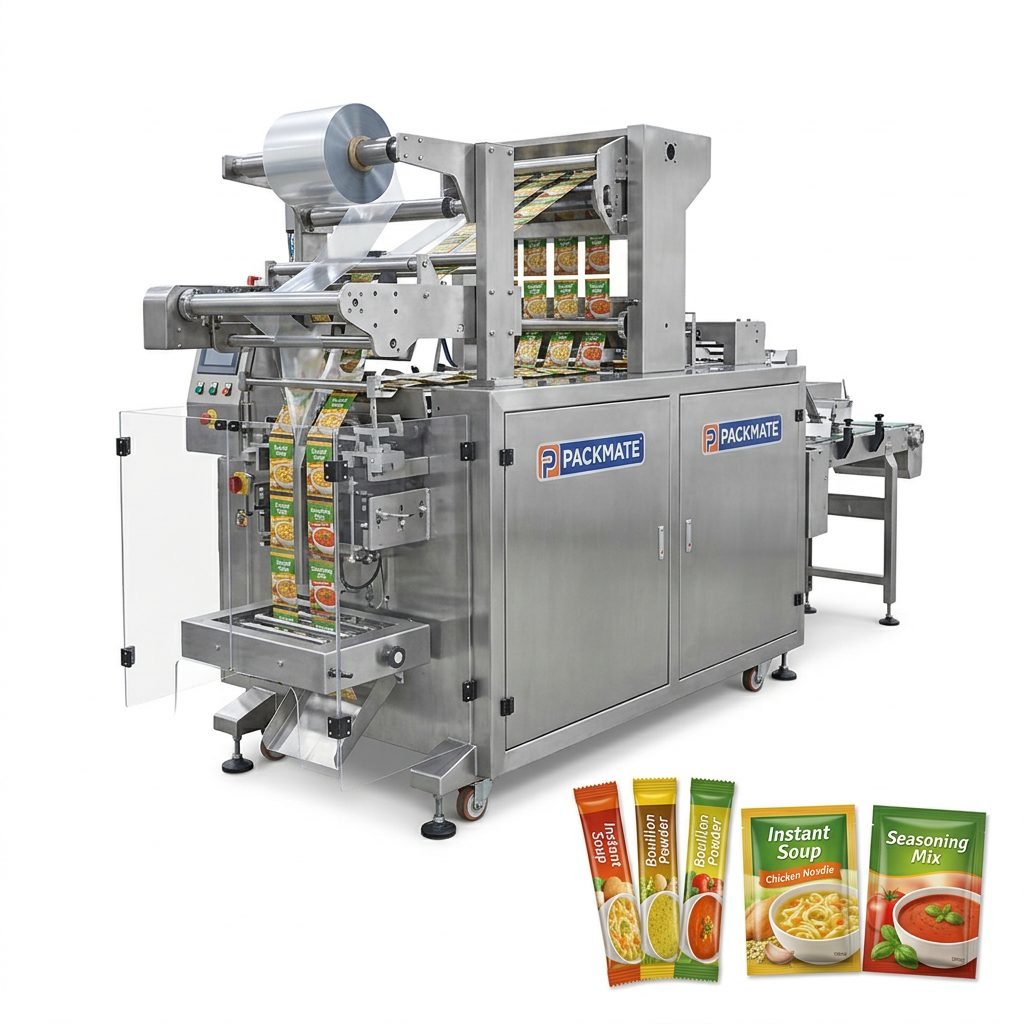
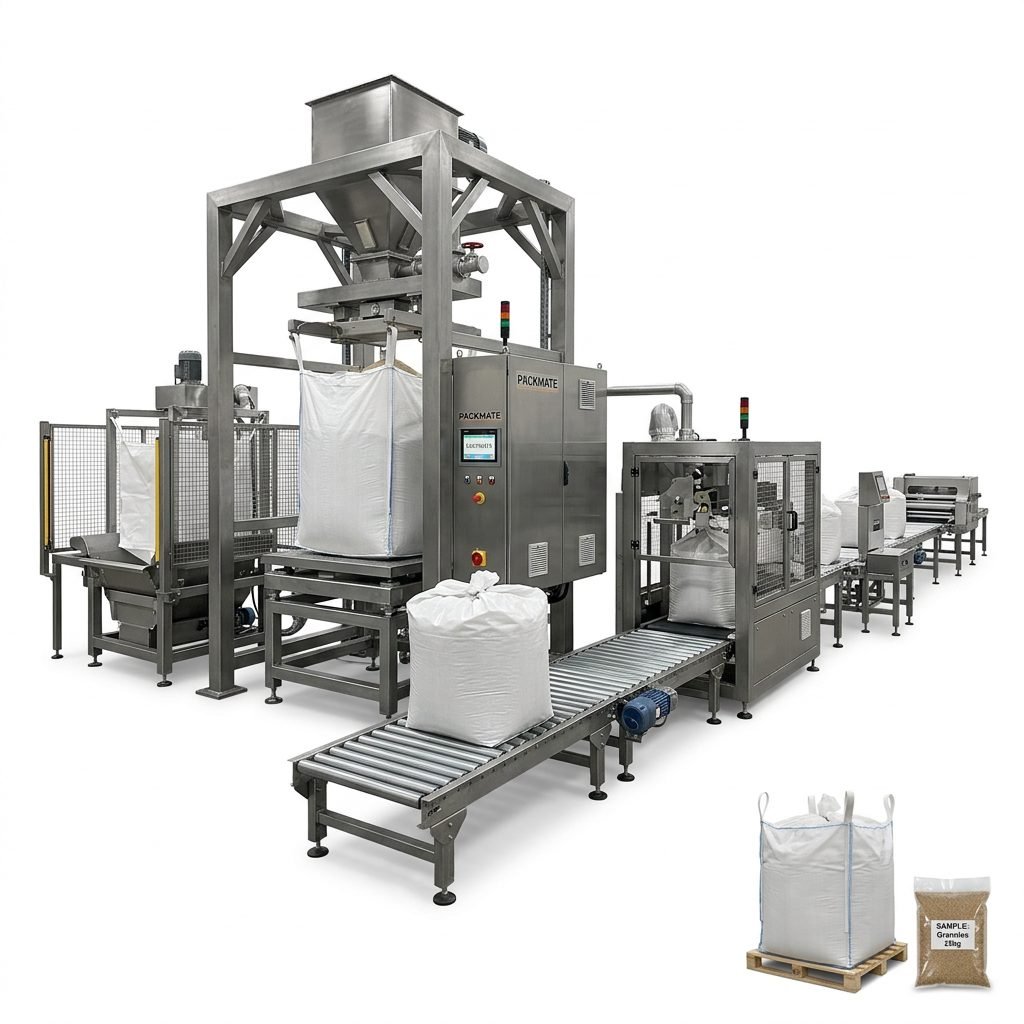
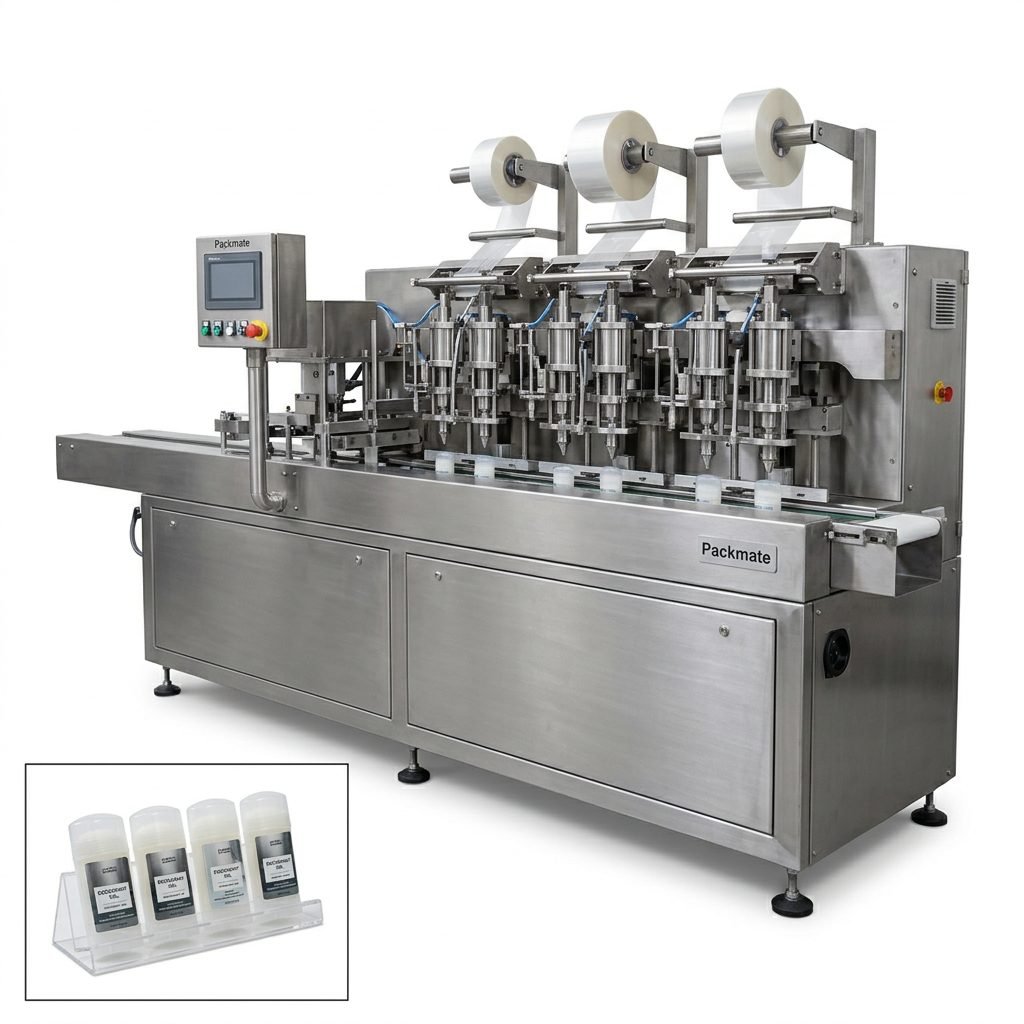
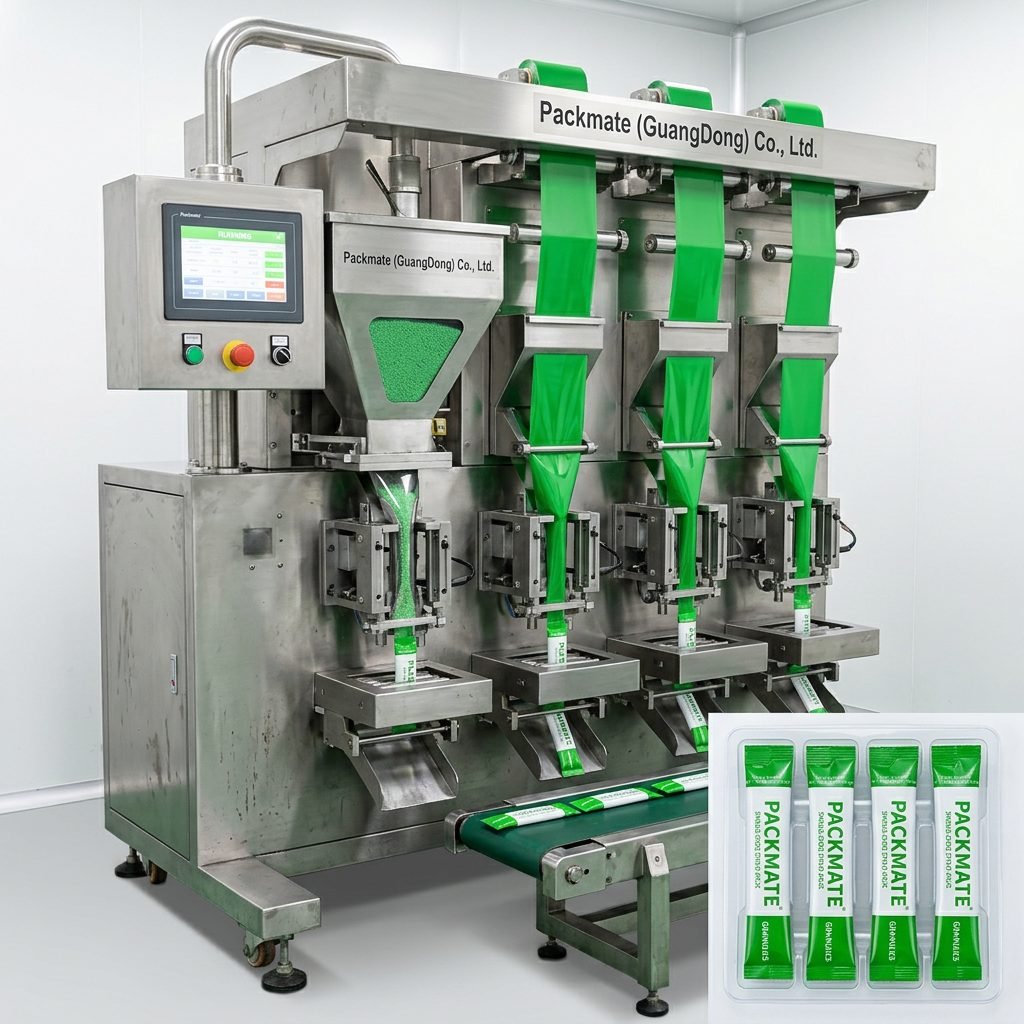
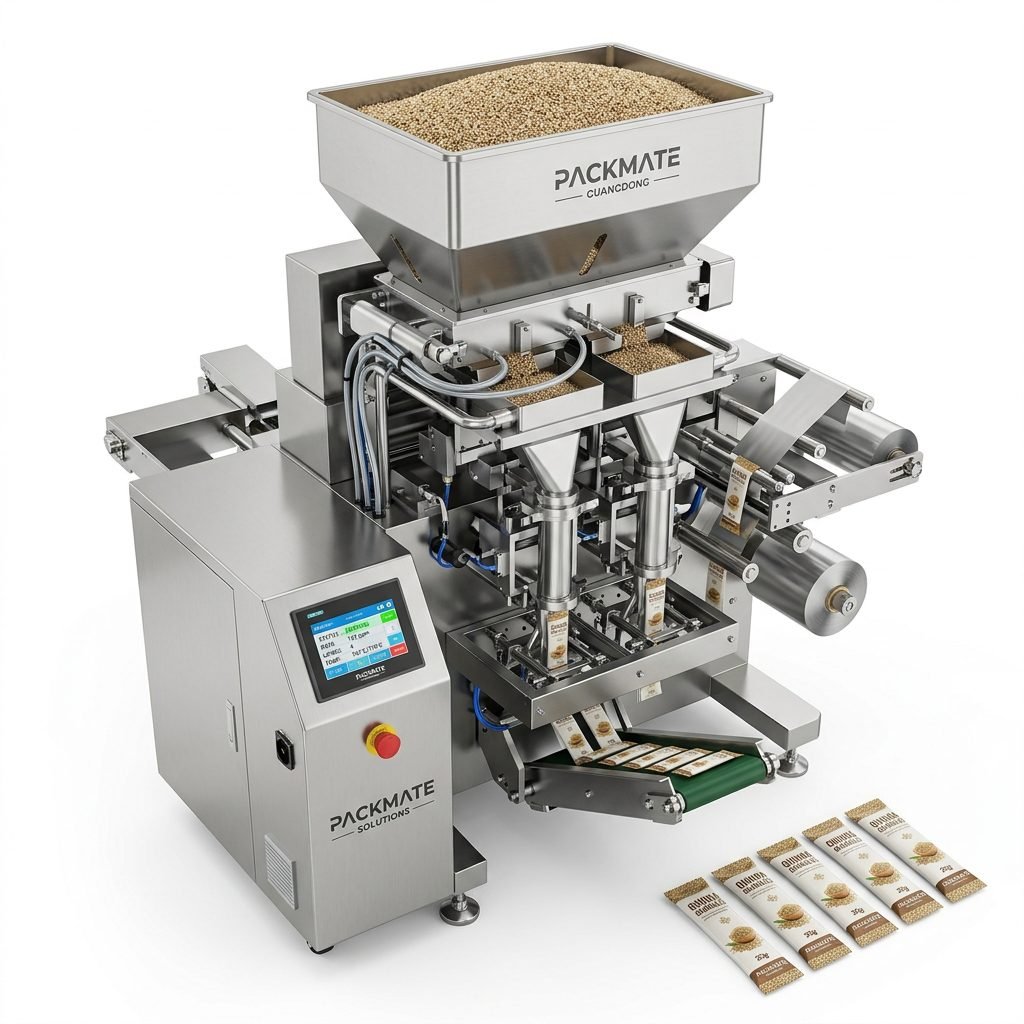
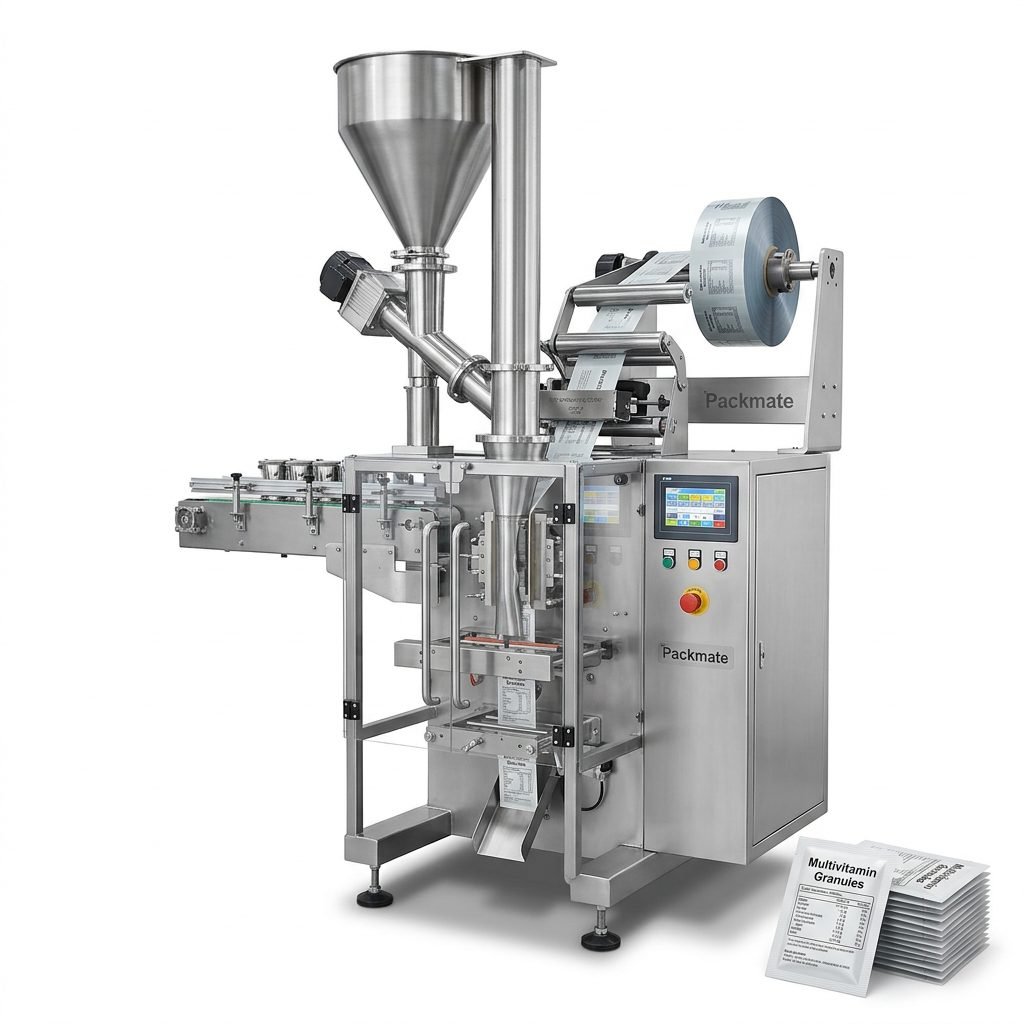
In today’s fast-paced manufacturing landscape, the ability to adapt is paramount. For producers in the food, pharmaceutical, and health product sectors, a rigid, one-size-fits-all packaging line is a liability. The future belongs to modularity—the strategic design of packaging systems from interchangeable, purpose-built components. This approach delivers the ultimate in flexibility, allowing businesses to scale production, switch product formats, and integrate new technologies without the cost and downtime of a complete overhaul. It is the foundation of truly flexible turnkey solutions.
The Core Philosophy: What is Packaging Line Modularity?
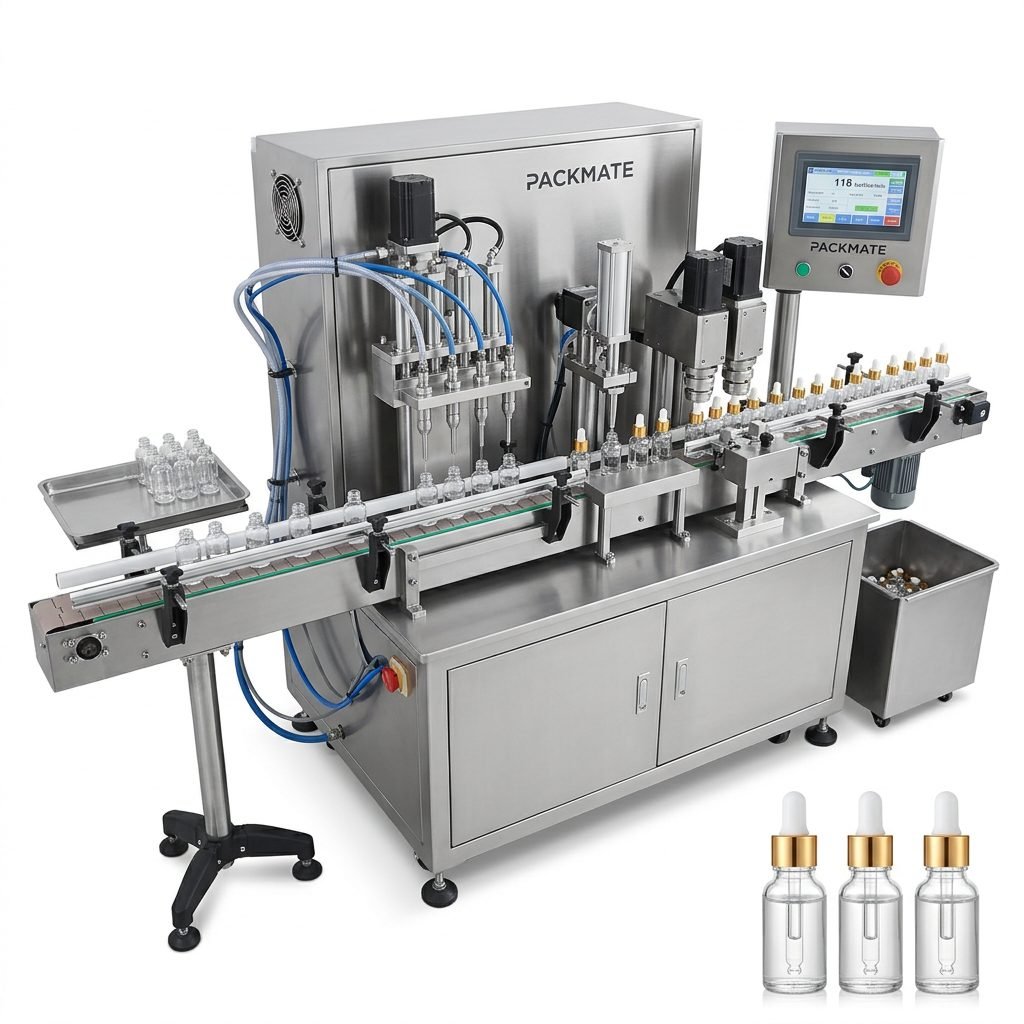
Modularity in packaging automation is more than a buzzword; it’s a systematic engineering philosophy. It involves designing a production line not as a single, fixed machine, but as a series of interconnected, standardized modules. Each module performs a specific function: feeding, weighing, filling, sealing, coding, or cartoning. These modules are designed to interface seamlessly, like building blocks, creating a cohesive system that can be easily reconfigured.
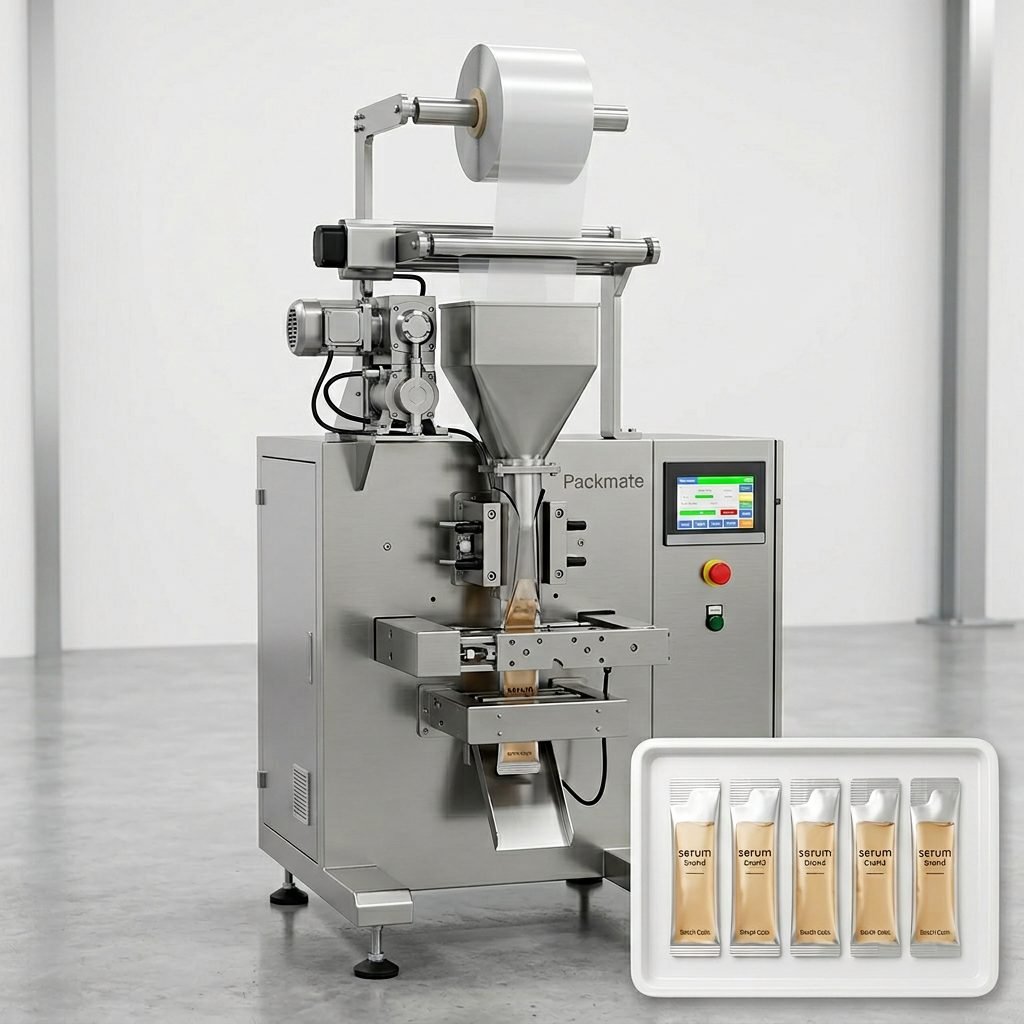
Key Advantage: This architecture future-proofs your investment. When market demand shifts—for instance, from single-serve sachets to multi-pack stick packs—you can swap out the forming-and-filling module and adjust the downstream collation module, rather than replacing the entire line. This drastically reduces capital expenditure and maximizes equipment utilization over its lifespan.
Driving Forces Behind the Shift to Modular Systems
Several critical industry trends are accelerating the adoption of modular packaging solutions:
1. Demand for Product Diversification & SKU Proliferation
Consumers crave variety, leading brands to offer products in multiple sizes, formats, and subscription models. A modular line can handle this complexity, quickly switching between different fill volumes, pouch styles, or materials with minimal changeover time and manual intervention.
2. The Need for Scalable Production
Start-ups and growing brands need lines that can grow with them. A modular approach allows you to begin with a core filling and sealing system. As volume increases, you can integrate additional modules for automated cartoning, case packing, and palletizing, creating a continuous, end-to-end solution. Explore our scalable packaging solutions designed for growth.
3. Stringent Regulatory Compliance
Particularly in pharmaceuticals and health products, regulations around traceability and cleanliness are non-negotiable. Modular systems can be designed with compliance in mind, allowing for the easy integration of specialized modules like vision inspection systems, serialization coders, or wash-down compatible components without disrupting the entire line’s validation.
Modularity in Action: Sector-Specific Applications
The benefits of modularity translate powerfully across our core industries, each with its unique requirements.
For the Food Industry: Agility Meets Hygiene
Food producers face seasonal peaks, promotional campaigns, and rapid new product launches. A modular packaging line provides the agility to run a batch of seasoning packets one week and snack bars the next. Hygienic design is paramount; modules feature smooth surfaces, easy-access panels for cleaning, and can be constructed from food-grade stainless steel. The ability to quickly integrate checkweighers or metal detectors as standalone modules ensures product safety and quality control are never compromised. View real-world application cases in food production.
For the Pharmaceutical Industry: Precision & Traceability
Here, modularity is synonymous with control and compliance. Lines for powders, granules, or liquids can be built with contained, dust-free transfer modules. Critical is the seamless integration of process analytical technology (PAT) and serialization modules to meet track-and-trace mandates worldwide. The modular design simplifies validation (IQ/OQ/PQ) for each individual component and allows for upgrades to meet new pharmacopeia standards without invalidating the entire system.
For Health & Nutraceutical Products: Brand Versatility
This dynamic sector blends the needs of food and pharma. Products range from protein powders and vitamin capsules to herbal teas and liquid supplements. Modular lines excel here by offering format flexibility—from sleek stick packs for on-the-go consumers to premium sachets or jars. Quick changeovers enable contract manufacturers to serve multiple brands efficiently, while precision filling modules ensure accurate dosing of active ingredients, a critical factor for product efficacy and consumer trust.
The Turnkey Advantage: From Modules to Complete Solution
Modularity is the “how,” but the turnkey solution is the “what” you receive. A true turnkey provider like Packmate (GuangDong) Co., Ltd. doesn’t just sell machines; they deliver a fully operational production asset. This encompasses:
- Consultation & Design: Engineering a modular layout optimized for your product, output, and factory space.
- Integration & Assembly: Pre-assembling and testing modules to ensure flawless interoperability before shipment.
- Installation & Commissioning: On-site setup, calibration, and running of production-ready batches.
- Training & Support: Comprehensive training for your operators and maintenance teams, backed by ongoing technical support and access to preventive maintenance services.
💡 Why This Matters: The turnkey approach eliminates the immense burden and risk of sourcing, integrating, and debugging modules from multiple vendors. You have a single point of responsibility, ensuring system coherence, performance guarantees, and streamlined after-sales service. It transforms a complex capital project into a predictable, operational outcome.
Implementing Your Modular Packaging Line: Key Considerations
Successfully deploying a modular system requires strategic planning. Here are essential factors to evaluate with your provider:
Defining Current & Future Needs
Clearly articulate not only today’s production requirements but also your 3-5 year roadmap. Consider potential new products, packaging formats, desired output speeds, and regulatory changes. This foresight informs the modular architecture’s scalability.
Selecting the Right Technology Partner
Look for a partner with proven experience in your specific industry and a deep portfolio of compatible modules. Assess their capability for custom engineering when standard modules need adaptation. Their certifications and quality standards are a testament to their manufacturing rigor.
Focusing on Total Cost of Ownership (TCO)
While the initial investment in a high-quality modular turnkey line may be higher, the TCO is often lower. Factor in savings from reduced changeover time, lower maintenance costs due to standardized parts, higher overall equipment effectiveness (OEE), and the avoided cost of a premature line replacement.
Conclusion: Building Resilience with Modular Design
Packaging line modularity is no longer a luxury; it’s a strategic imperative for competitive manufacturers in the food, pharmaceutical, and health product industries. It embodies operational resilience, providing the flexibility to respond to market changes, the efficiency to optimize production, and the scalability to support sustainable growth. By partnering with a seasoned turnkey solution provider, you leverage this philosophy to create a packaging operation that is not just productive, but also profoundly adaptable and ready for the future.
Frequently Asked Questions (FAQs)
1. How much downtime is expected when reconfiguring a modular line for a different product?
Downtime varies based on the complexity of the changeover. However, a well-designed modular system aims for quick changeovers—often in minutes or a few hours—by using quick-release mechanisms, pre-programmed recipes, and tool-less adjustments. This is a fraction of the downtime required to retool a monolithic machine.
2. Can I add modules from other manufacturers to my existing modular line?
While technically possible, it is generally not recommended. Seamless communication (via PLC, sensors, etc.) and mechanical interfacing are optimized when all modules are designed by the same OEM or within a certified partner ecosystem. Mixing brands can lead to integration challenges, voided warranties, and reduced overall line performance and support.
3. Are modular packaging lines more expensive than traditional integrated lines?
The initial capital outlay can be comparable or slightly higher due to the advanced engineering of standardized, interoperable components. The financial benefit is realized over time through lower long-term costs: reduced changeover losses, easier maintenance, extended machinery life through upgrades, and protection against obsolescence, leading to a superior return on investment.
4. How does modularity impact validation processes in GMP environments?
Modularity can simplify validation. Each individual module (e.g., filler, sealer) can undergo Installation Qualification (IQ) and Operational Qualification (OQ) independently. When the line is reconfigured, you primarily need to re-qualify the changed module and its interfaces, rather than the entire system, saving significant time and resources.
5. What kind of technical support is available for modular systems?
Reputable providers offer comprehensive support, including detailed documentation for each module, remote diagnostics, on-demand spare parts for the entire system, and technician training. This single-source support is a major advantage, as you don’t need to coordinate with multiple vendors for troubleshooting. For more answers, visit our dedicated FAQs page.