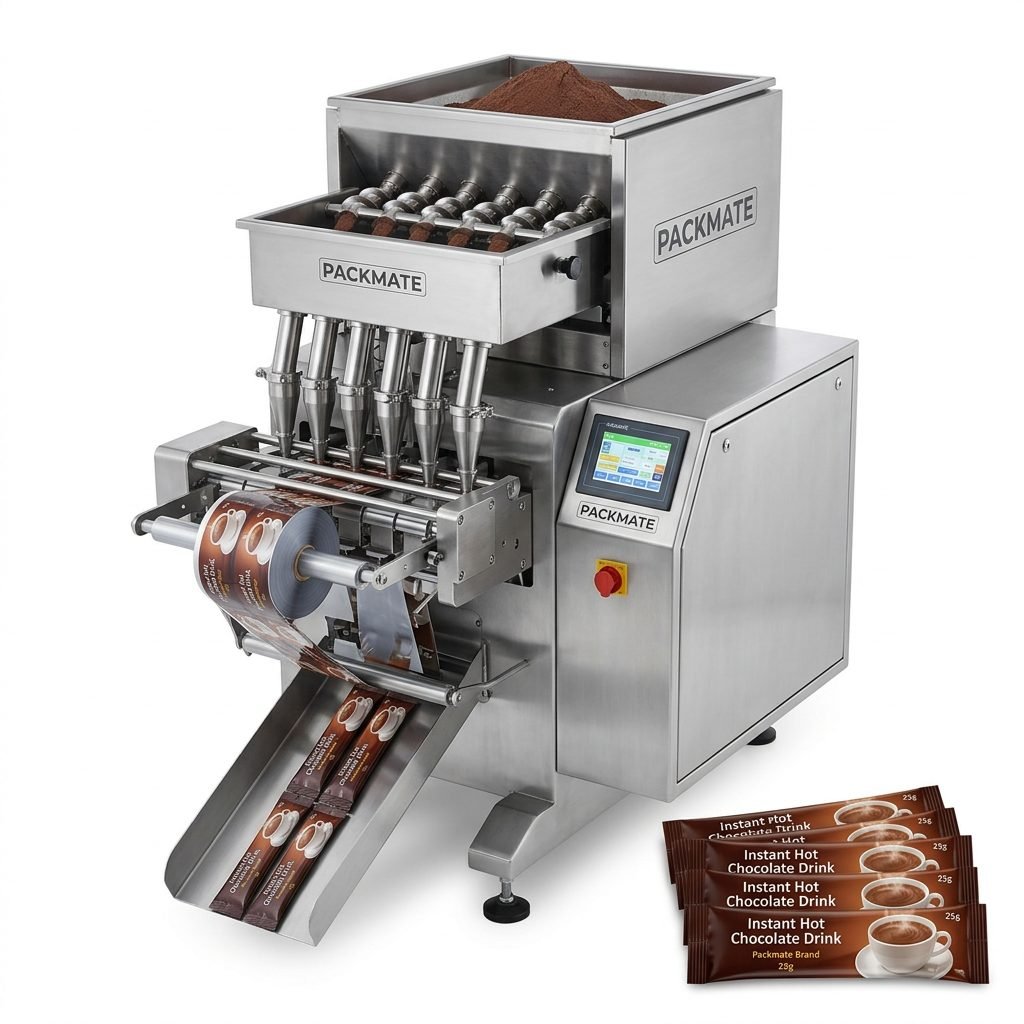
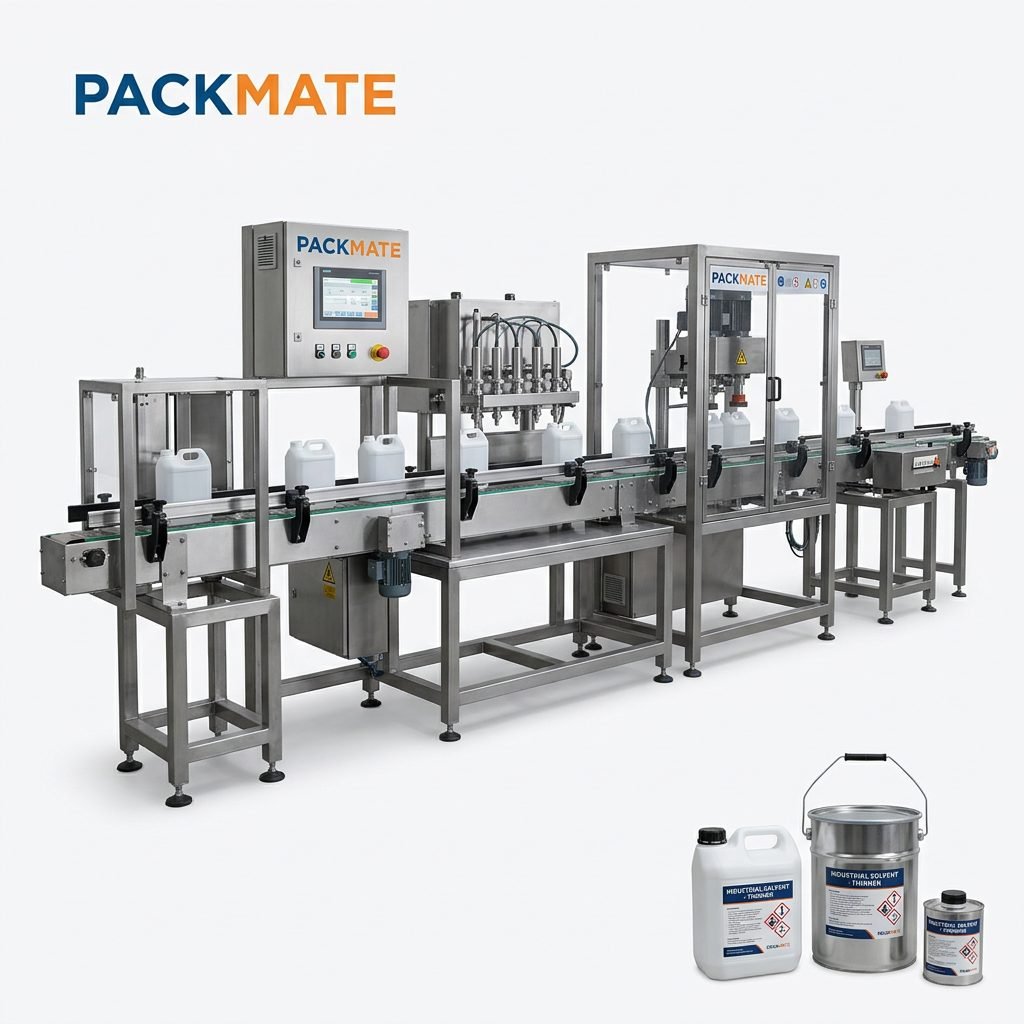
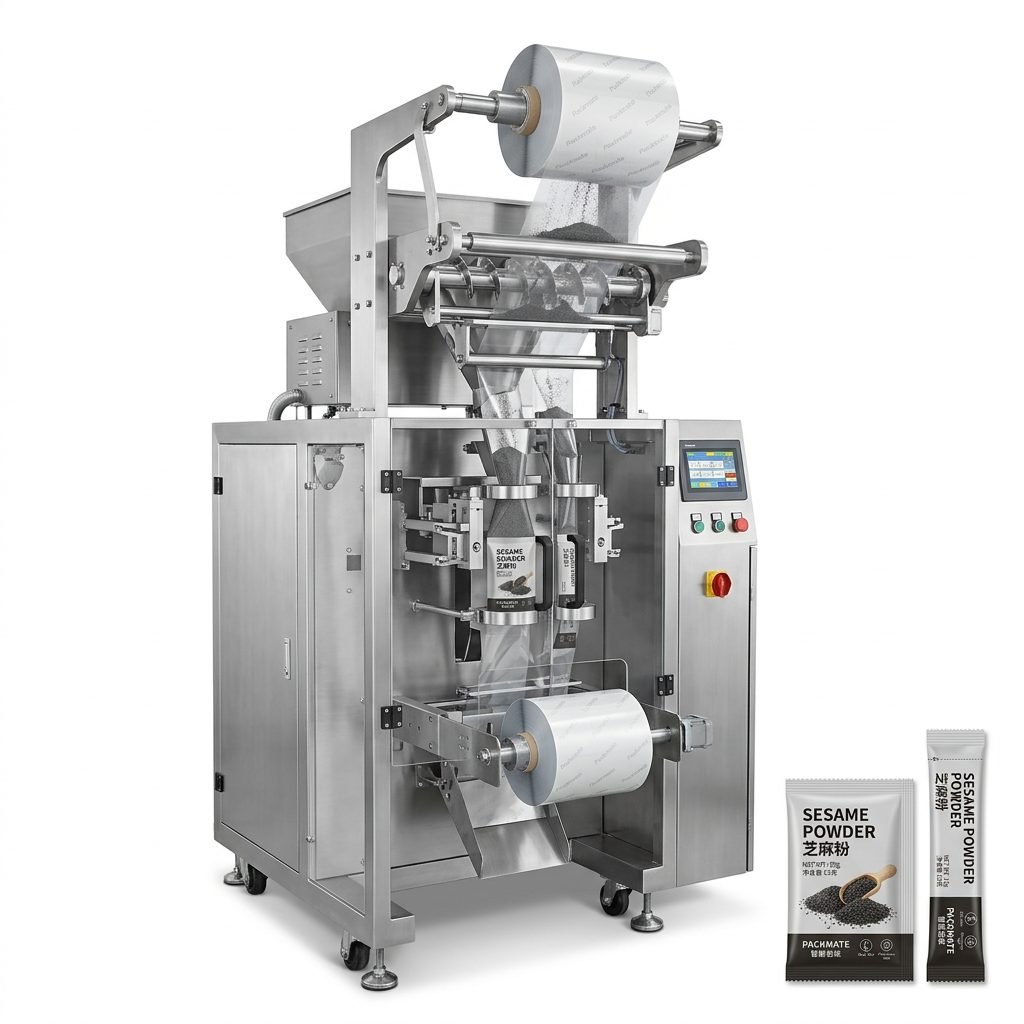
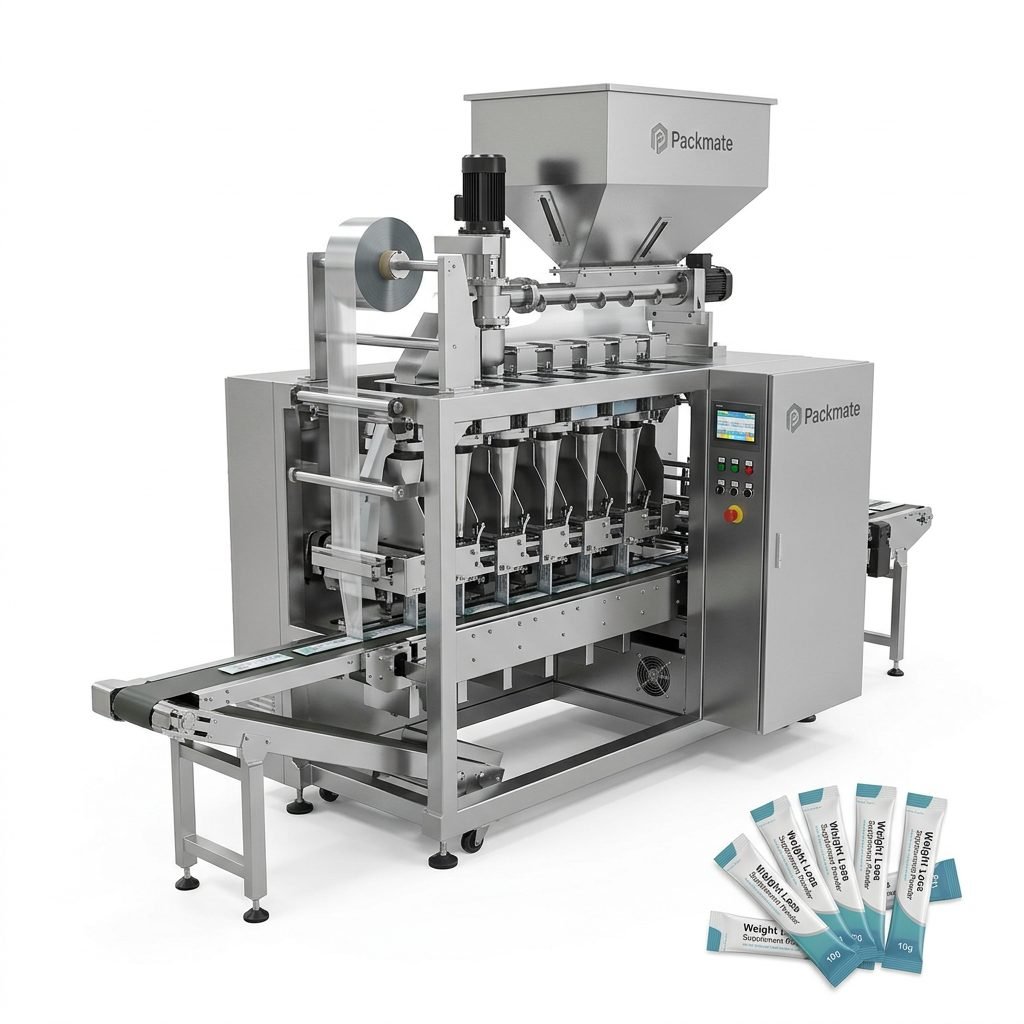
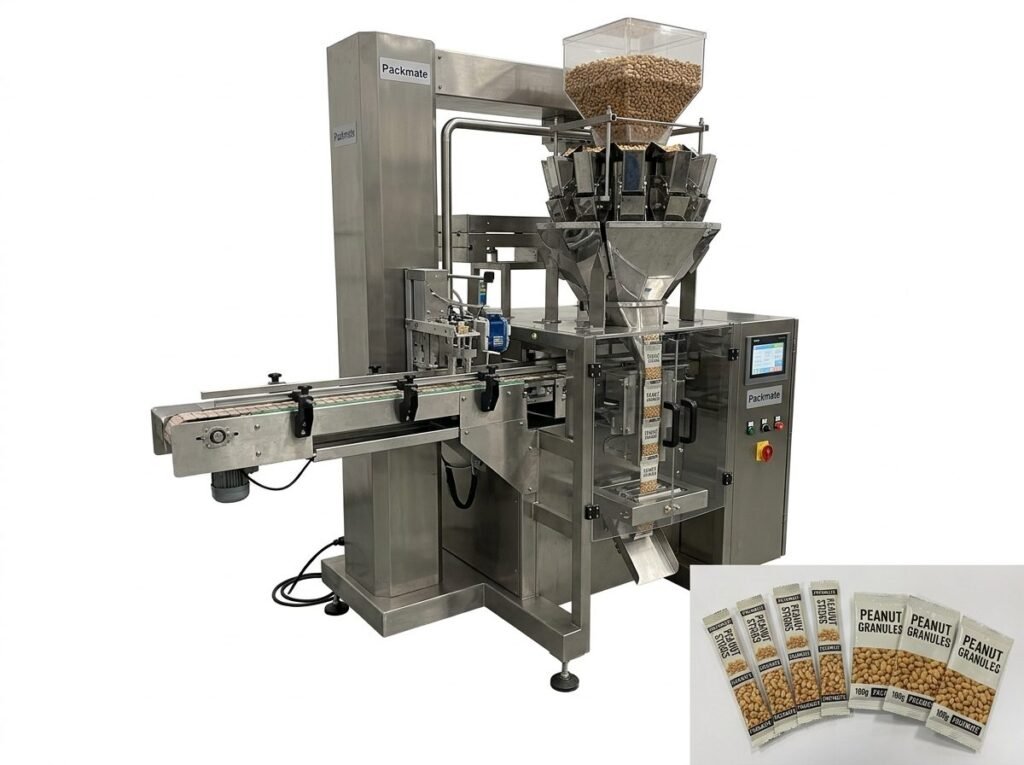
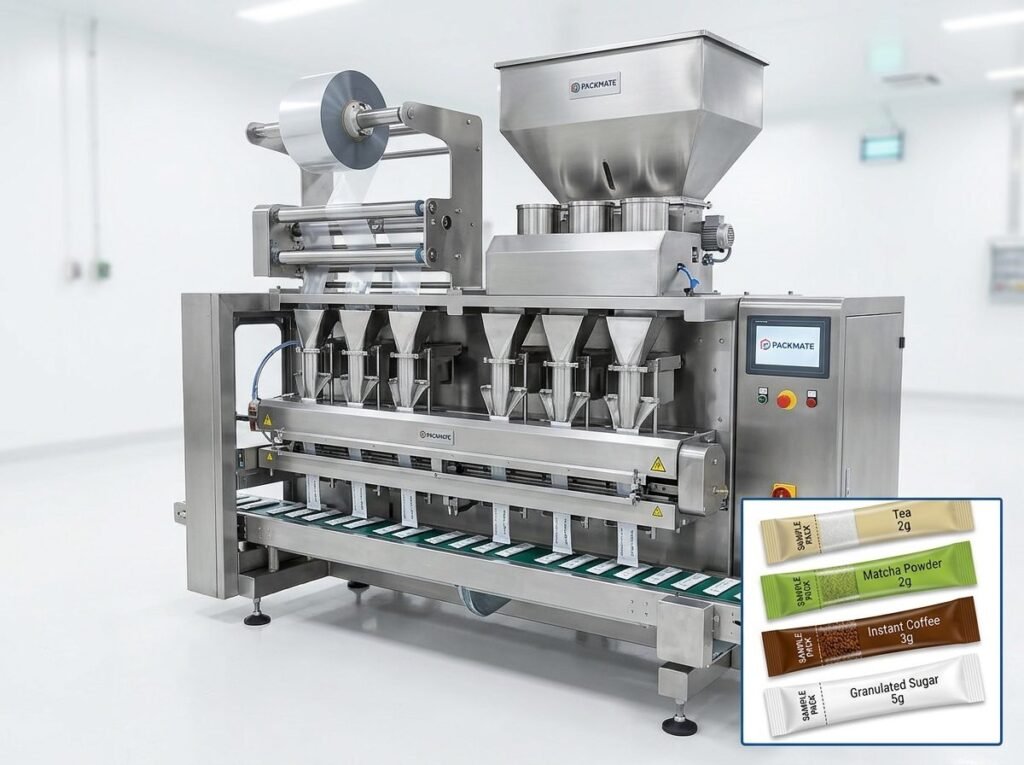
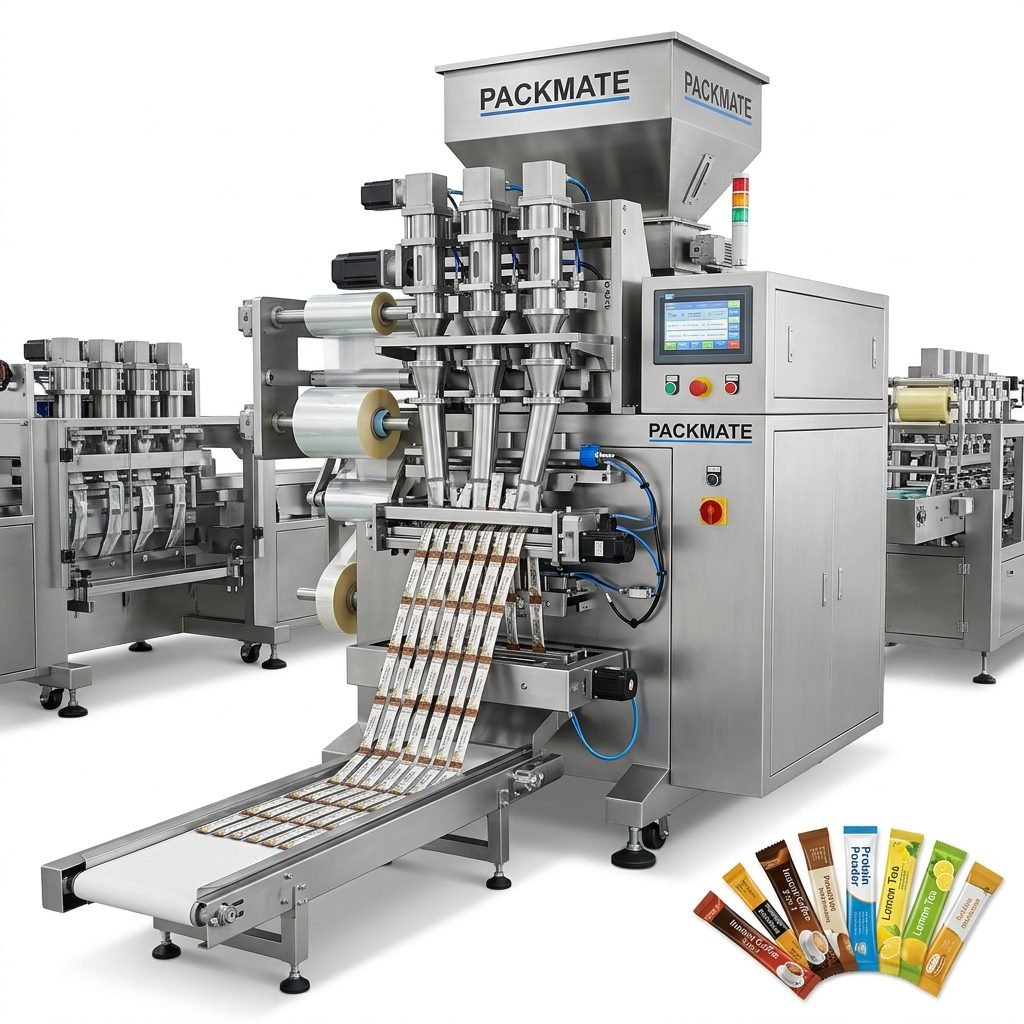
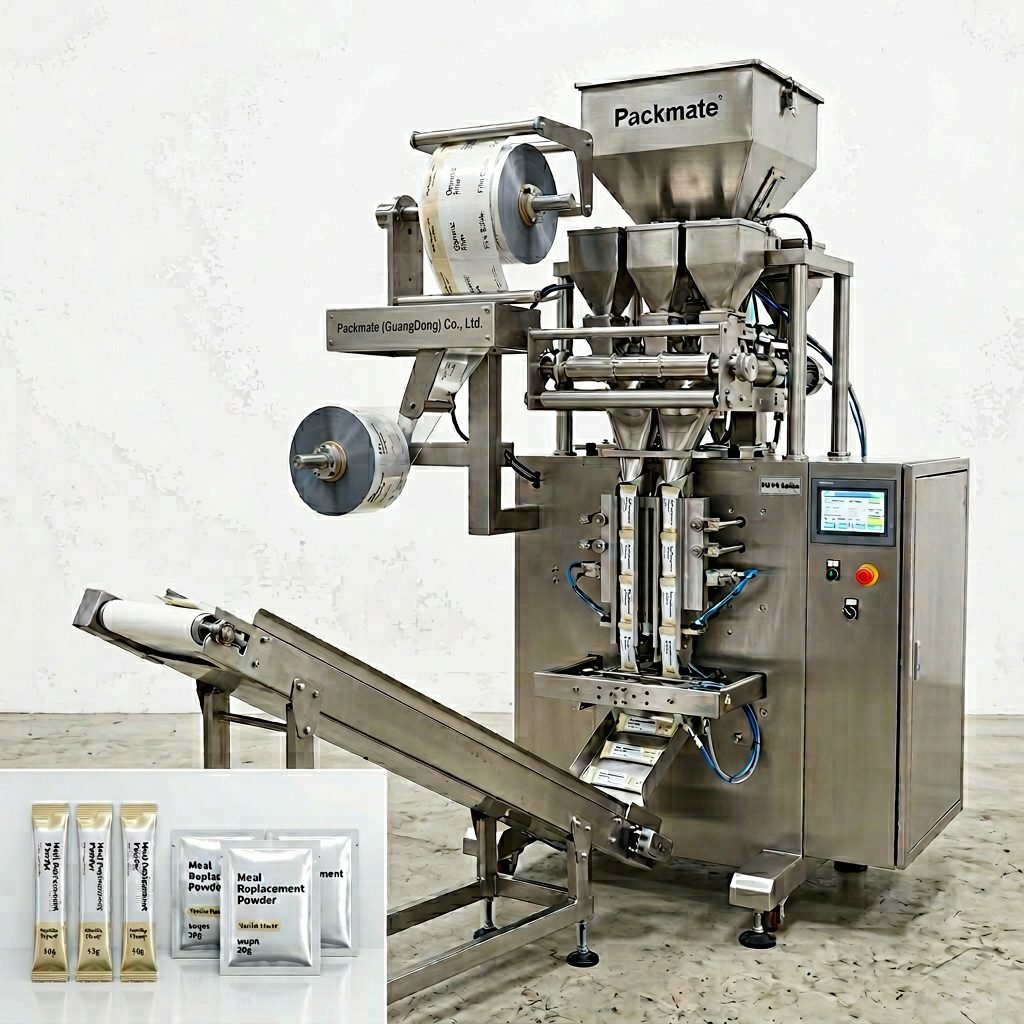
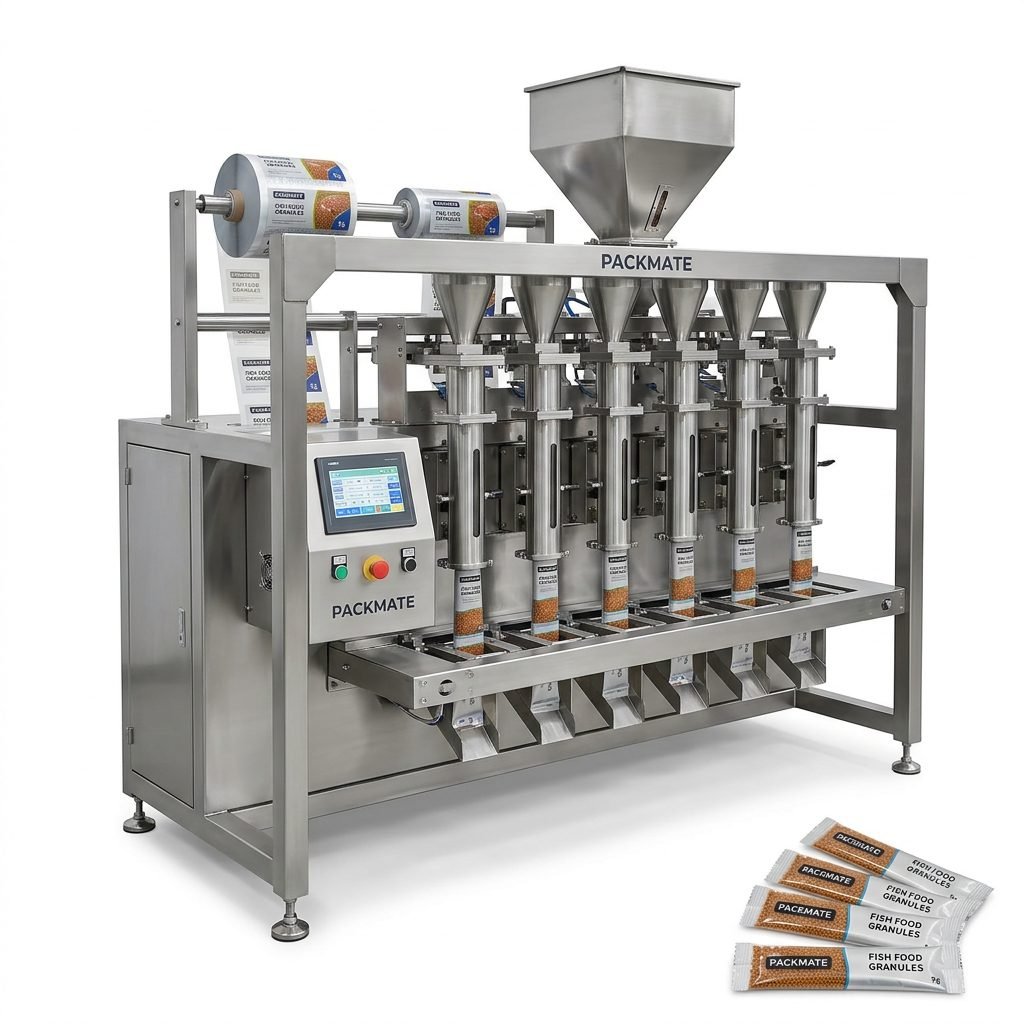
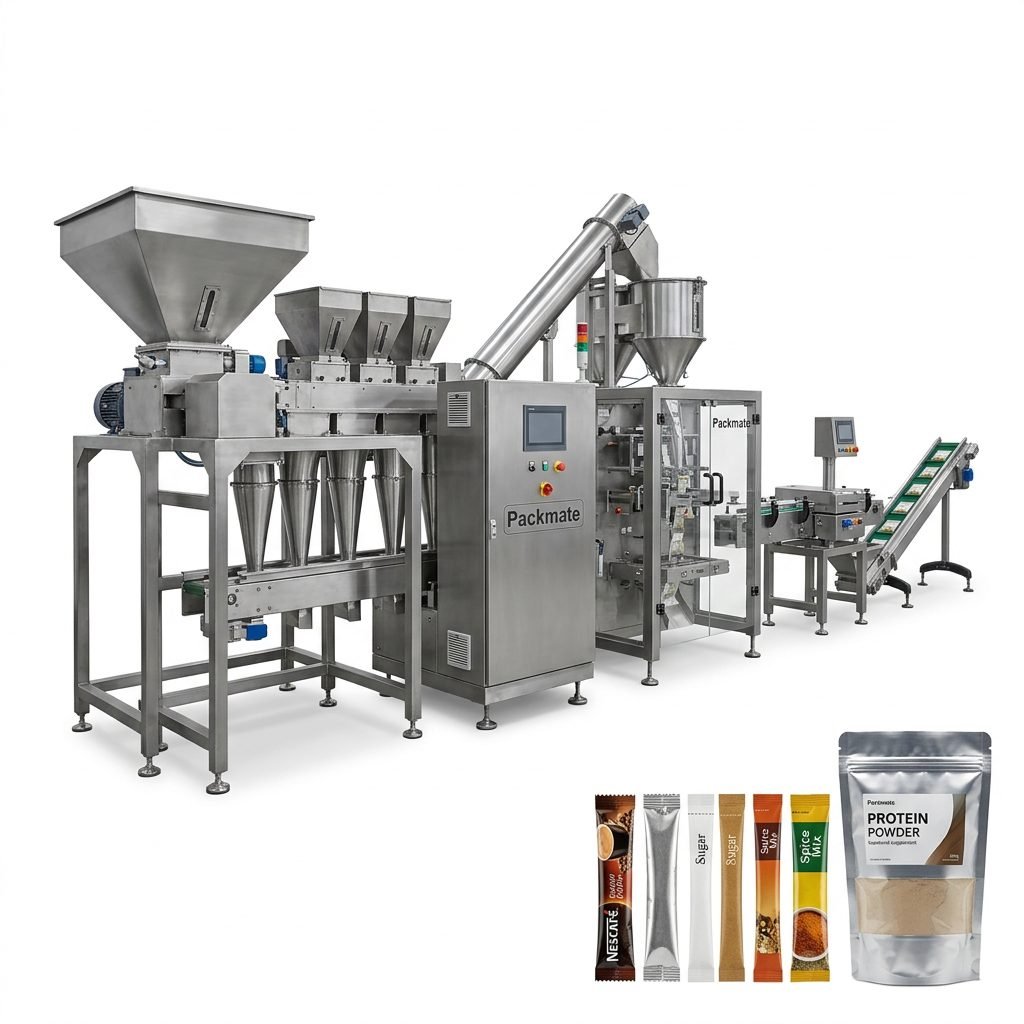
In the fast-paced and highly regulated worlds of food, pharmaceuticals, and healthcare, the final step of production—packaging—is often the most critical. Ensuring product integrity, safety, and shelf appeal requires precision, hygiene, and unwavering reliability. This is where a dedicated Packaging Line for Liquid transitions from a mere operational necessity to a strategic asset. A complete, turnkey filling and packing solution integrates seamlessly into your workflow, delivering not just efficiency but also peace of mind.
The Core of Modern Liquid Packaging: Beyond the Machine
A turnkey solution is far more than a collection of machines. It represents a holistic approach, encompassing design, engineering, installation, validation, and ongoing support. For liquid products—whether it’s a delicate pharmaceutical syrup, a nutrient-rich health drink, or a viscous food sauce—each step must be meticulously controlled.
Key Components of a Turnkey Liquid Line:
- Unwinding & Forming: Precision handling of packaging film, crucial for maintaining barrier properties against oxygen and moisture.
- Volumetric or Piston Filling: The heart of accuracy. Advanced fillers ensure dose-perfect consistency, critical for pharmaceuticals and costly ingredients.
- Sealing & Coding: Creating hermetic seals to prevent contamination and leakage, integrated with date/batch coding for traceability.
- Cartoning & Secondary Packaging: Automating the transition from primary sachet or stick pack to retail-ready boxes.
- Control & Monitoring (SCADA): The intelligent brain providing real-time data on output, efficiency, and potential faults.
Industry-Specific Challenges and Tailored Solutions
The “one-size-fits-all” approach fails in liquid packaging. Each sector imposes unique demands that a competent provider must address through customized engineering.
For the Pharmaceutical & Healthcare Sector
Here, compliance is non-negotiable. Packaging lines must be designed for easy cleaning and sterilization, often utilizing materials compatible with clean-in-place (CIP) systems. The environment demands Grade A or B air classification for filling zones. Traceability, from raw material to finished pack, is paramount. A partner like Packmate, with deep industry understanding, builds solutions that adhere to cGMP, FDA, and other global regulatory standards, ensuring patient safety and audit readiness.
For the Food & Beverage Industry
Speed, versatility, and hygiene define success. Lines must quickly switch between different viscosities—from water-thin juices to creamy dressings—with minimal downtime. Packaging materials must preserve flavor and nutritional value while extending shelf life. Efficiency directly impacts profitability, making high-speed, multi-lane configurations, such as those detailed in our packaging solutions portfolio, essential for competitive producers.
The Tangible Benefits of a Complete Turnkey System
Investing in an integrated line from a single source yields measurable returns across the entire operation.
Operational Excellence
Maximized Efficiency & Uptime: Perfectly synchronized machines eliminate bottlenecks. Single-source responsibility means no finger-pointing between equipment vendors; the provider owns the line’s performance.
Reduced Labor Costs & Human Error: Automation handles repetitive, precise tasks, freeing skilled personnel for quality control and supervision, while minimizing contamination risks.
Scalability for Growth: A well-designed system allows for modular expansion. Adding lanes or integrating downstream cartoning can be planned from the outset.
Quality & Compliance Assurance
Consistent Product Integrity: Precision filling and sealing protect your product’s efficacy, taste, and safety from production to consumption.
Simplified Validation: A turnkey provider delivers Installation Qualification (IQ), Operational Qualification (OQ), and Performance Qualification (PQ) documentation, streamlining the regulatory approval process.
Enhanced Brand Protection: Flawless packaging execution safeguards your brand’s reputation on the shelf and in the hands of the end-user.
Choosing the Right Partner: More Than a Supplier
Selecting a provider for your liquid packaging line is a long-term strategic decision. Look for a partner with proven industry case studies that demonstrate success in your specific field. Evaluate their engineering capability, quality of components, and depth of after-sales support. A partner with a strong company profile and a clear mission will align with your goals for innovation and reliability.
Consider their global service network, availability of spare parts, and training programs for your operators. The ideal partner acts as an extension of your team, committed to your production success for years to come. Exploring their comprehensive service offerings is a crucial step in this evaluation.
Conclusion: The Strategic Imperative
In conclusion, a complete turnkey packaging line for liquids is not merely a capital expense; it is a foundational investment in quality, efficiency, and market competitiveness. For industries where product purity and presentation are inseparable from brand value, the right automated solution mitigates risk, ensures compliance, and drives sustainable growth. By partnering with an experienced and innovative provider, you secure more than machinery—you secure a reliable pathway to operational excellence.
Frequently Asked Questions (FAQs)
1. What does “turnkey” mean in the context of a packaging line?
A turnkey solution means the provider delivers a fully integrated, ready-to-operate production line. This includes design, manufacturing, installation, commissioning, operator training, and initial validation support. You receive a complete system that you can essentially “turn the key” to start production, with single-point accountability.
2. How do you ensure the packaging line meets hygiene standards for Pharma and Food?
Lines are designed with hygienic principles: using stainless steel (often 304 or 316L) for contact parts, implementing smooth, crevice-free surfaces, and designing for easy disassembly and cleaning. For pharma, we incorporate requirements for cleanroom compatibility and validated sterilization processes, adhering to cGMP guidelines.
3. Can one line handle different liquid viscosities and package sizes?
Yes, modern lines are built for flexibility. Key components like filling pumps and sealing jaws can be adjusted or changed. Quick-change parts and programmable recipes allow for efficient changeovers between different products and pack formats, minimizing downtime.
4. What kind of after-sales support and warranty is typically provided?
Reputable providers offer comprehensive support including a standard warranty on parts and workmanship, remote diagnostic support, on-site technical service, readily available spare parts, and periodic maintenance contracts. Training for your maintenance and operational staff is also a critical part of the package.
5. How long does it take from project initiation to having an operational line?
The timeline varies based on line complexity and customization. A standard configuration may take 3-6 months for manufacturing and delivery, followed by 2-4 weeks for installation and commissioning. Highly customized or large-scale projects require more detailed engineering and thus a longer timeline, which is established during the initial project planning phase.