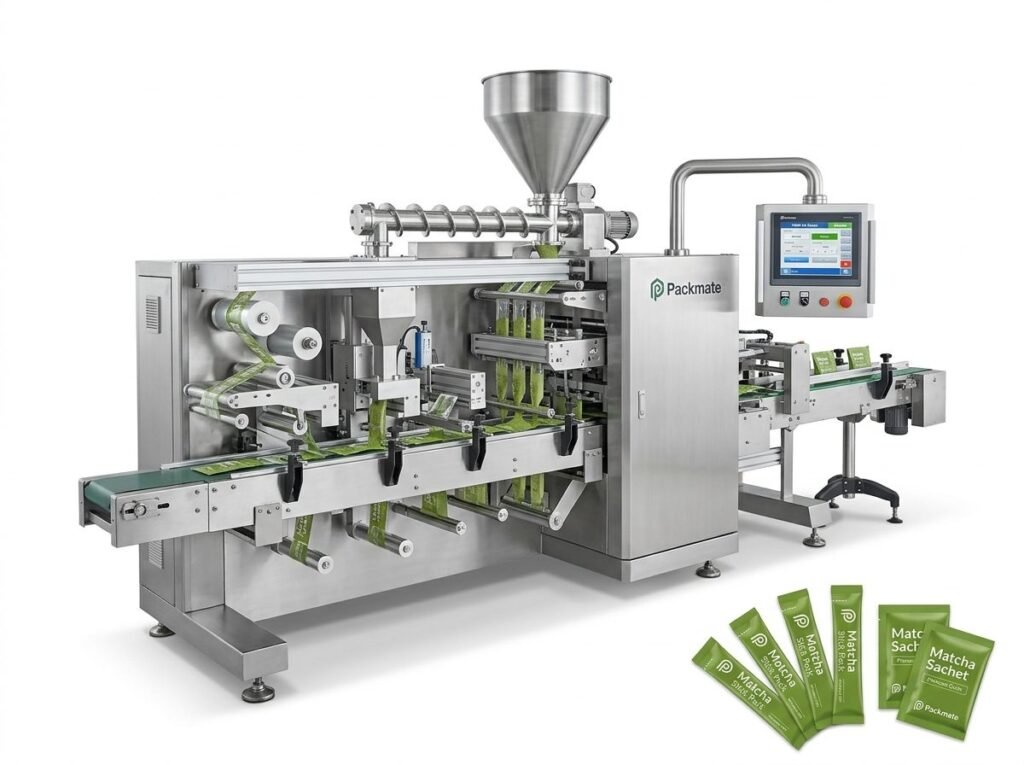
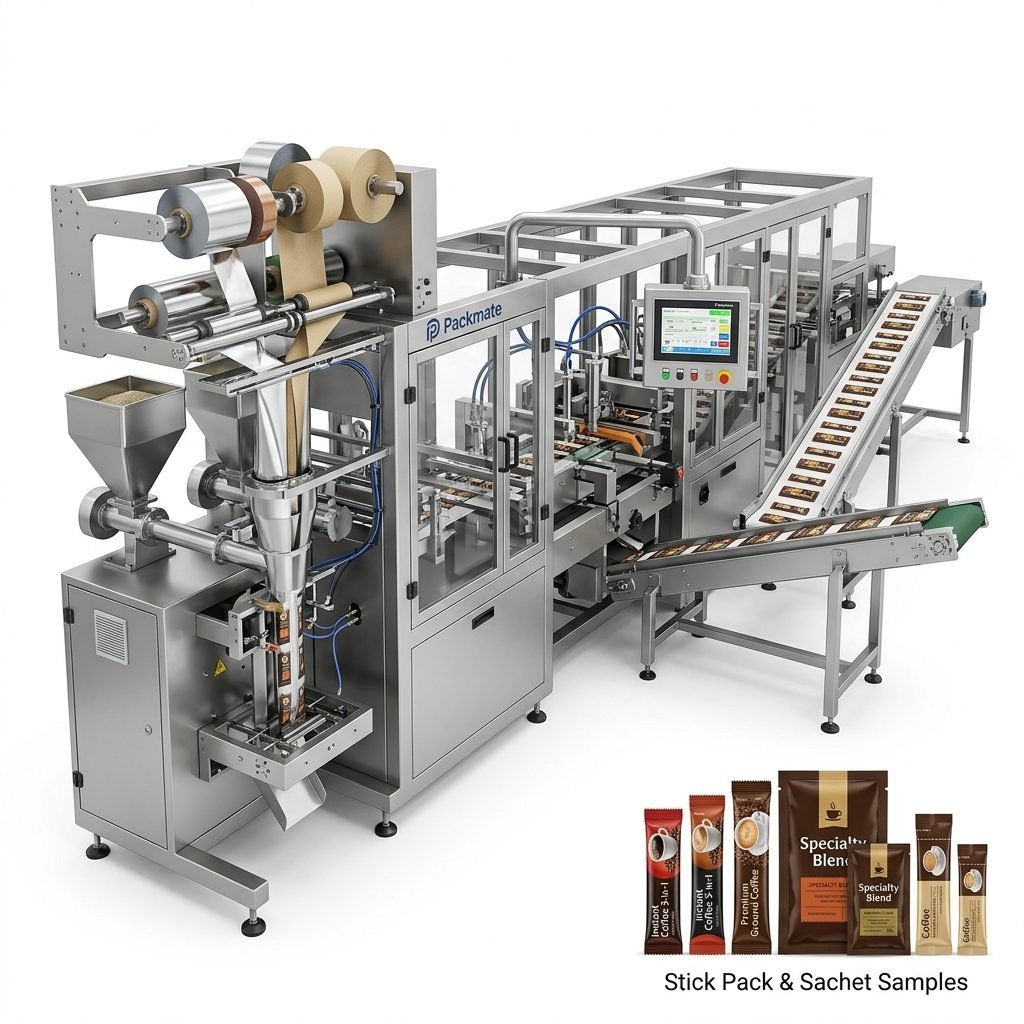
The pharmaceutical industry operates under the most stringent regulations globally, where product integrity, patient safety, and traceability are non-negotiable. Packaging is not merely the final step in production; it is a critical component of the product itself. For manufacturers of granules, powders, and liquids, achieving consistent, compliant, and efficient packaging at scale is a formidable challenge. This is where the concept of a turnkey pharma packaging line becomes not just an operational upgrade but a strategic imperative. A fully integrated solution handles everything from dosing and filling to sealing, labeling, and cartoning, ensuring a seamless, validated process from raw material to finished, shippable product.
The Critical Role of Specialized Packaging in Pharma
Pharmaceutical products are inherently sensitive. Granules may be hygroscopic, powders can be volatile or require precise dosing, and liquids need protection from contamination and leakage. The packaging line must be more than just fast; it must be intelligent, adaptable, and built with materials and processes that meet cGMP (current Good Manufacturing Practice) standards. Cross-contamination prevention, easy cleaning and sterilization (CIP/SIP where applicable), and data integrity for full traceability are paramount. A disjointed system of individual machines from different vendors introduces points of failure, validation complexity, and compliance risk that a unified turnkey solution is designed to eliminate.
Key Challenges Addressed by Turnkey Lines:
- Product Integrity: Protecting sensitive formulations from moisture, oxygen, and light.
- Dosing Accuracy: Ensuring each sachet, stick pack, or bottle contains the exact specified amount, critical for efficacy and safety.
- Regulatory Compliance: Adhering to FDA, EMA, and other global regulatory body requirements for equipment design, materials, and documentation.
- Operational Efficiency: Minimizing changeover times, reducing waste (overfills/underfills), and maximizing Overall Equipment Effectiveness (OEE).
- Serialization & Aggregation: Integrating technology for track-and-trace mandates, a global requirement for pharmaceutical products.
Tailored Solutions for Granules, Powders, and Liquids
A one-size-fits-all approach fails in pharma packaging. Each product form demands specific handling and packaging technologies. Leading providers like Packmate (GuangDong) Co., Ltd. engineer their lines with this core understanding.
Granules & Powder Packaging Lines
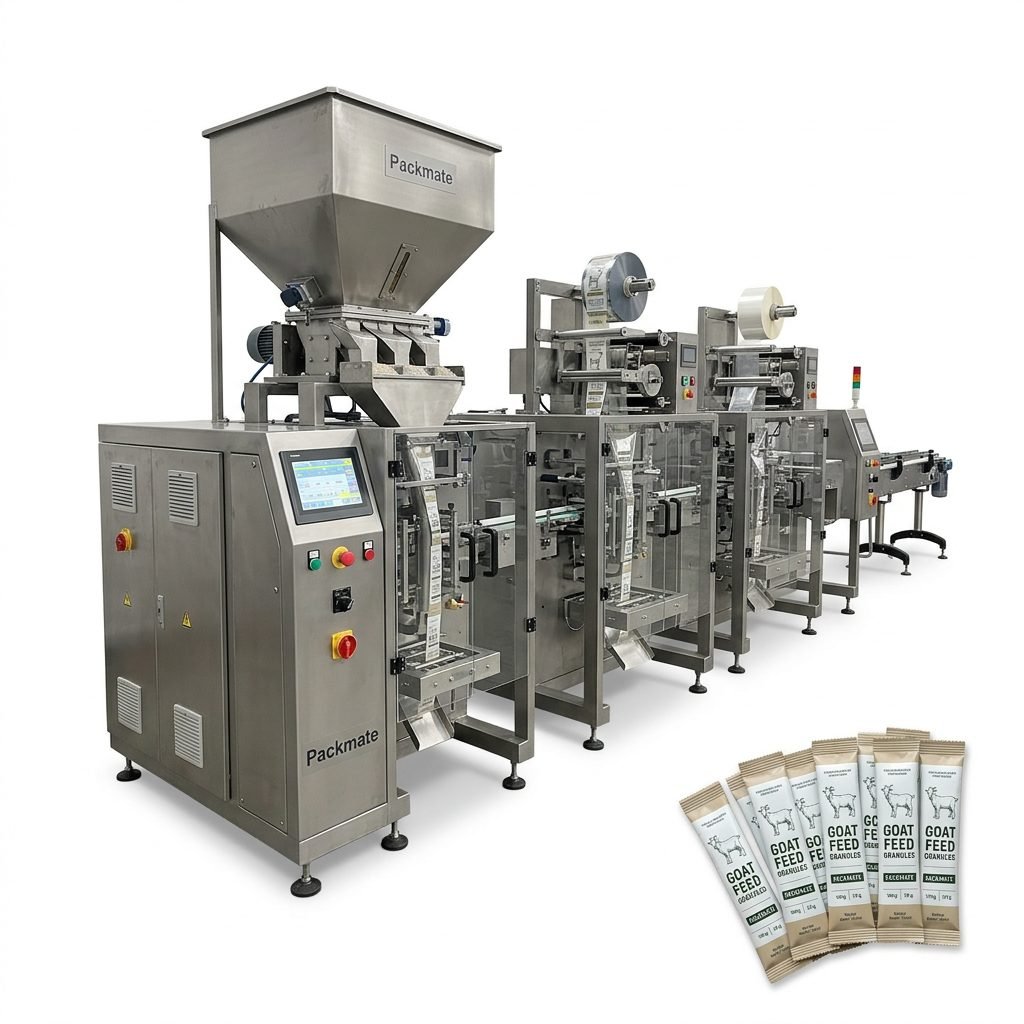
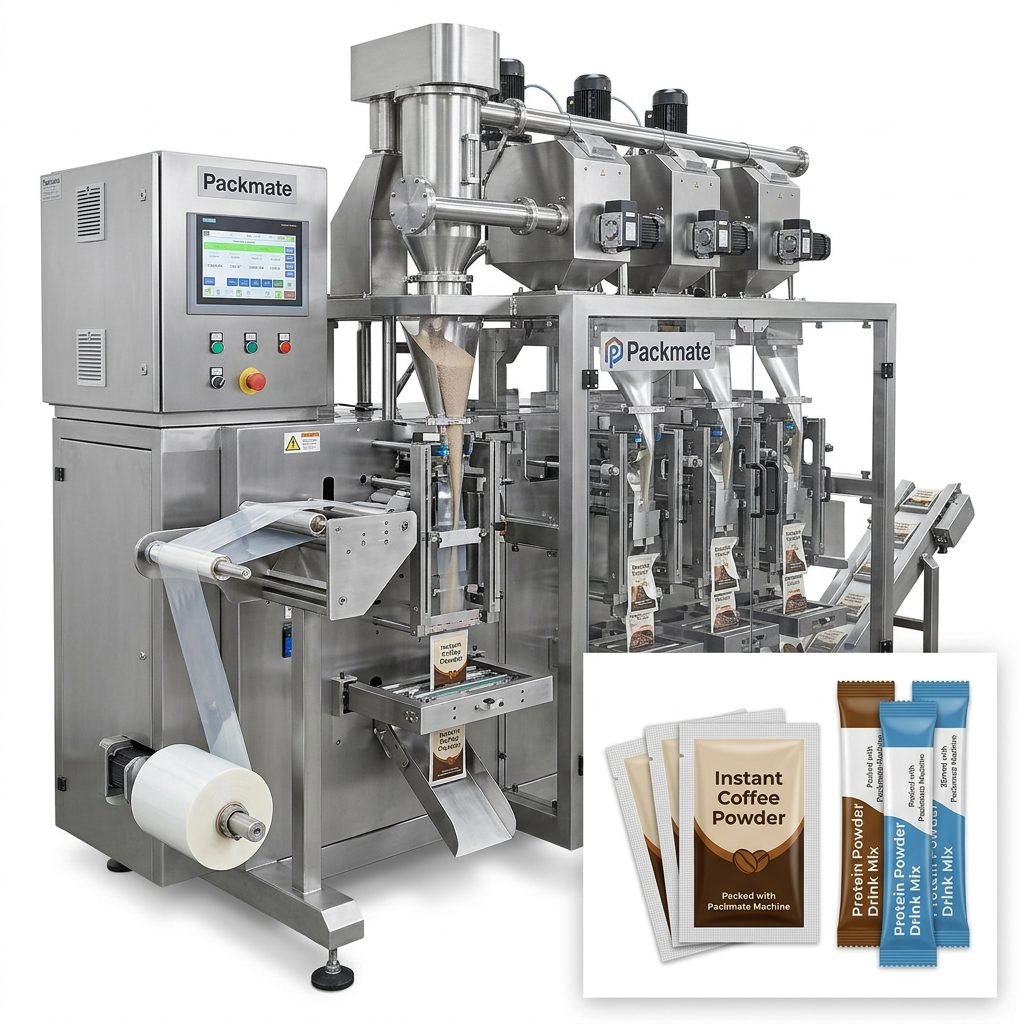
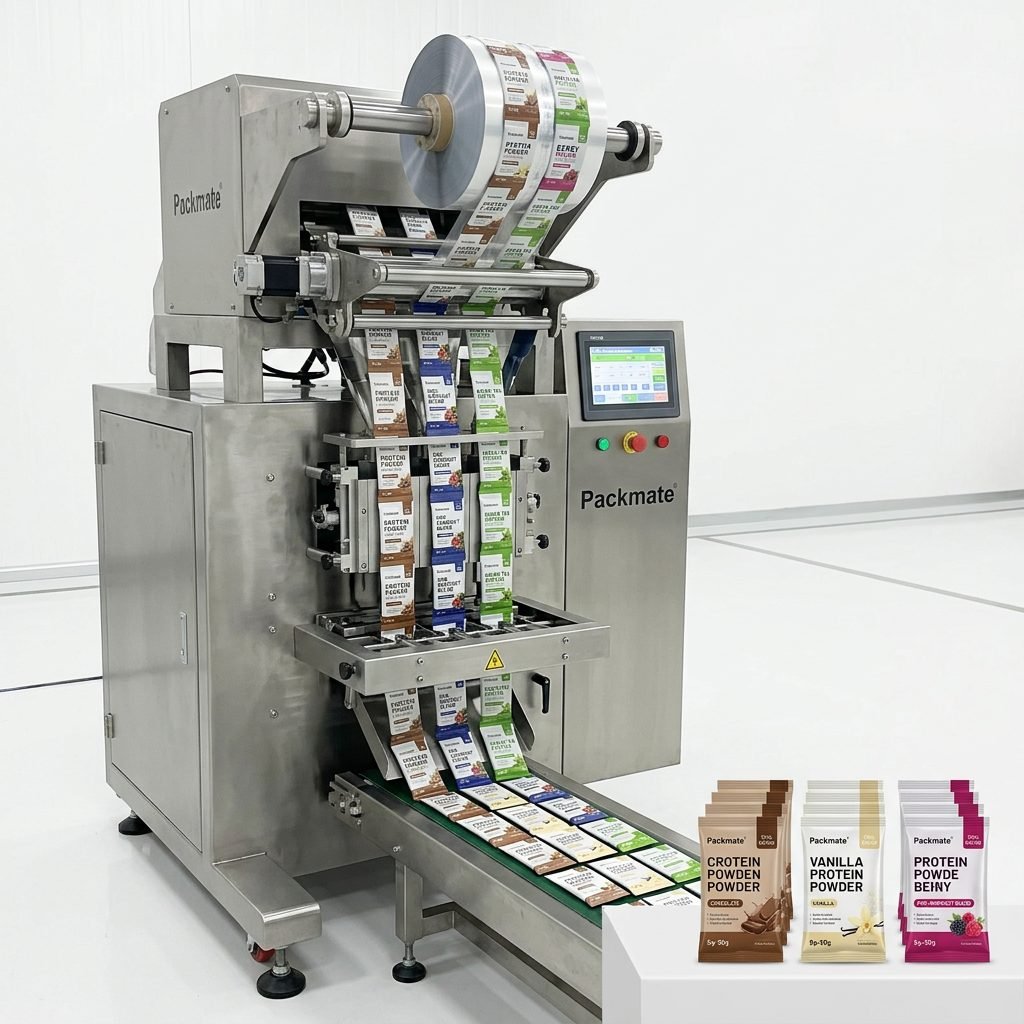
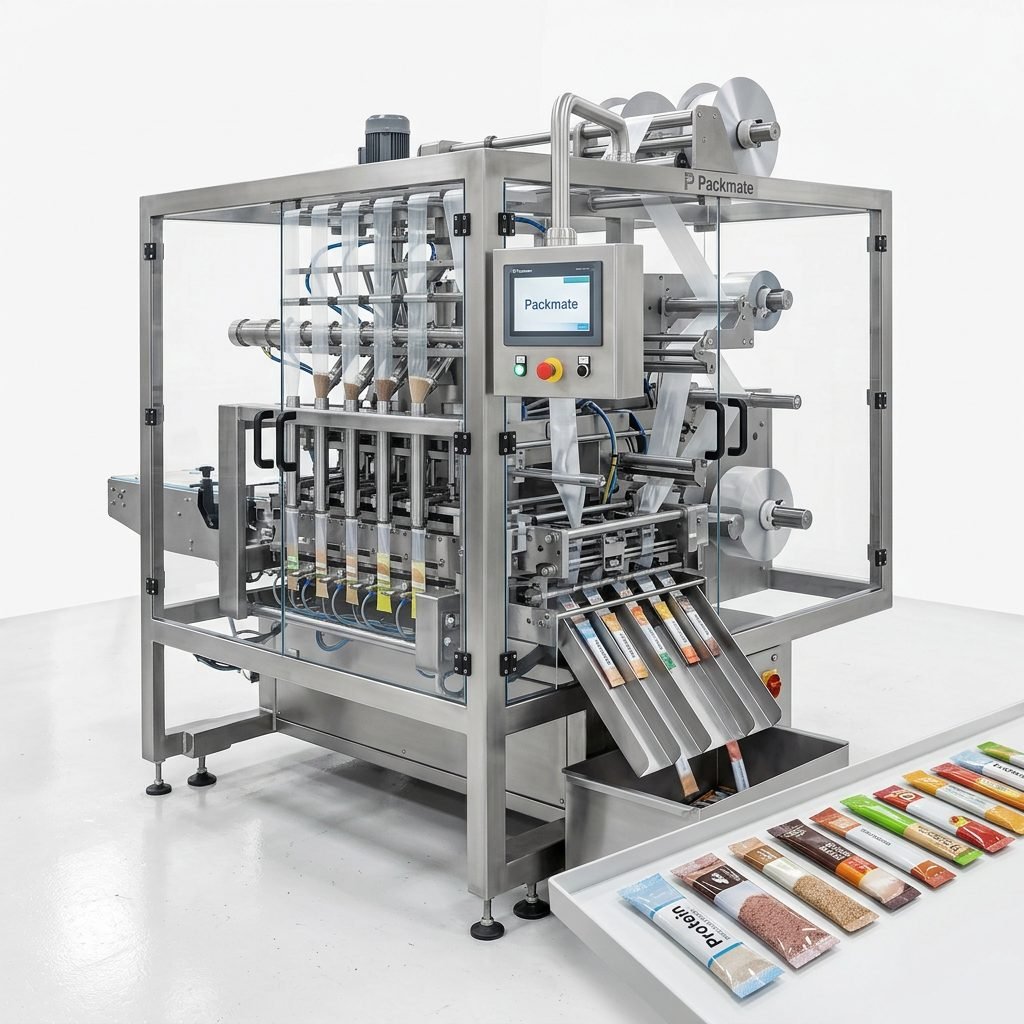
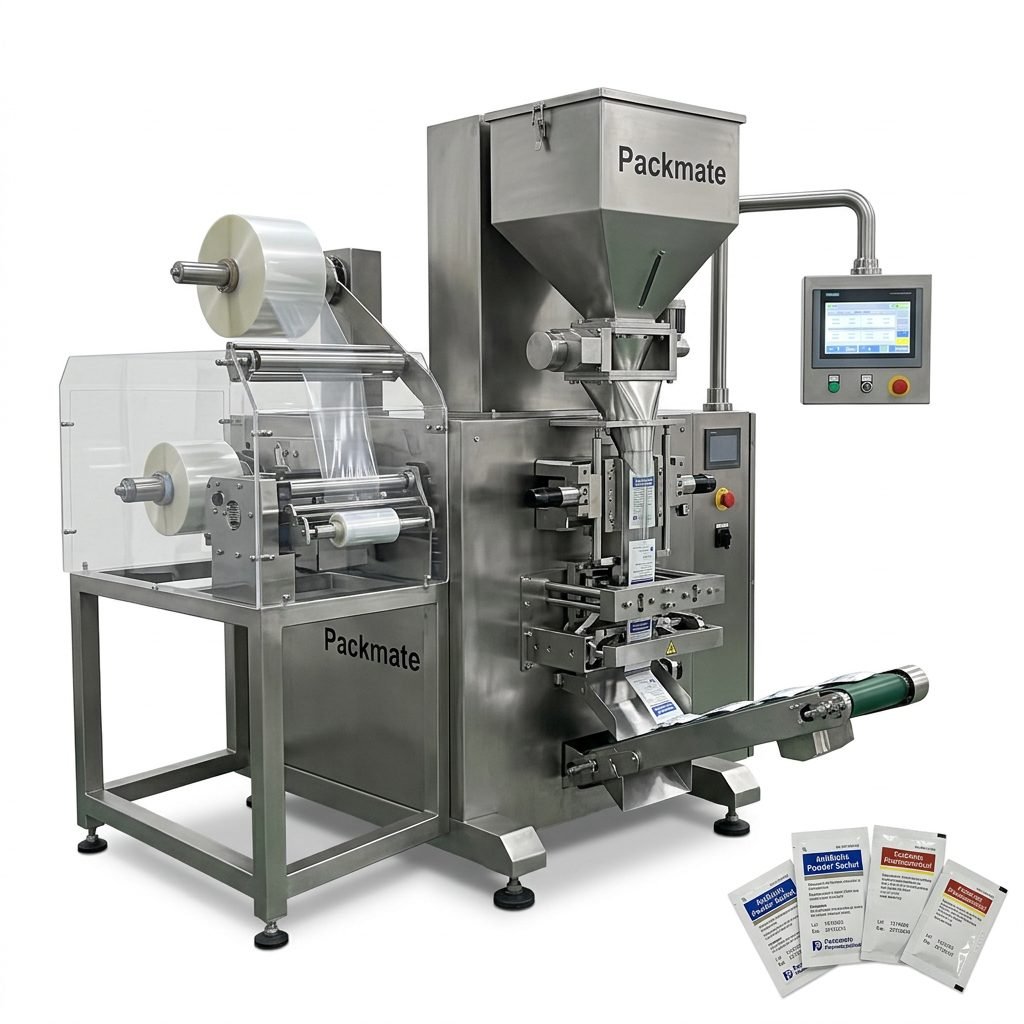
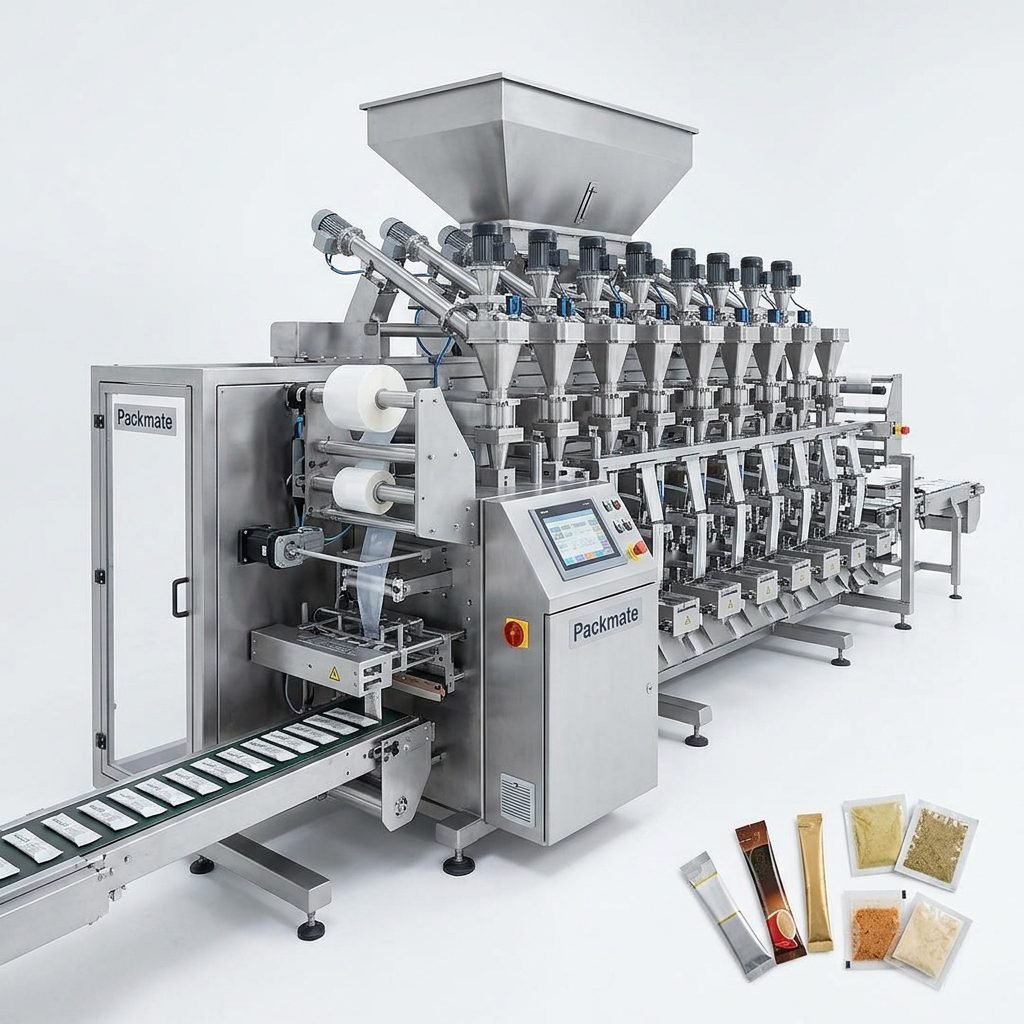
For products like effervescent granules, instant drink mixes, or medicinal powders, precision and protection from clumping are key. Modern lines utilize auger filler technology with servo-driven motors for unparalleled accuracy. The packaging environment is often controlled with dehumidification to prevent moisture uptake. Multi-lane stick pack and sachet machines are ideal for creating convenient, single-dose units. These lines integrate checkweighers and metal detectors seamlessly to ensure every unit meets weight and purity specifications before proceeding to secondary packaging.
Liquid Packaging Lines
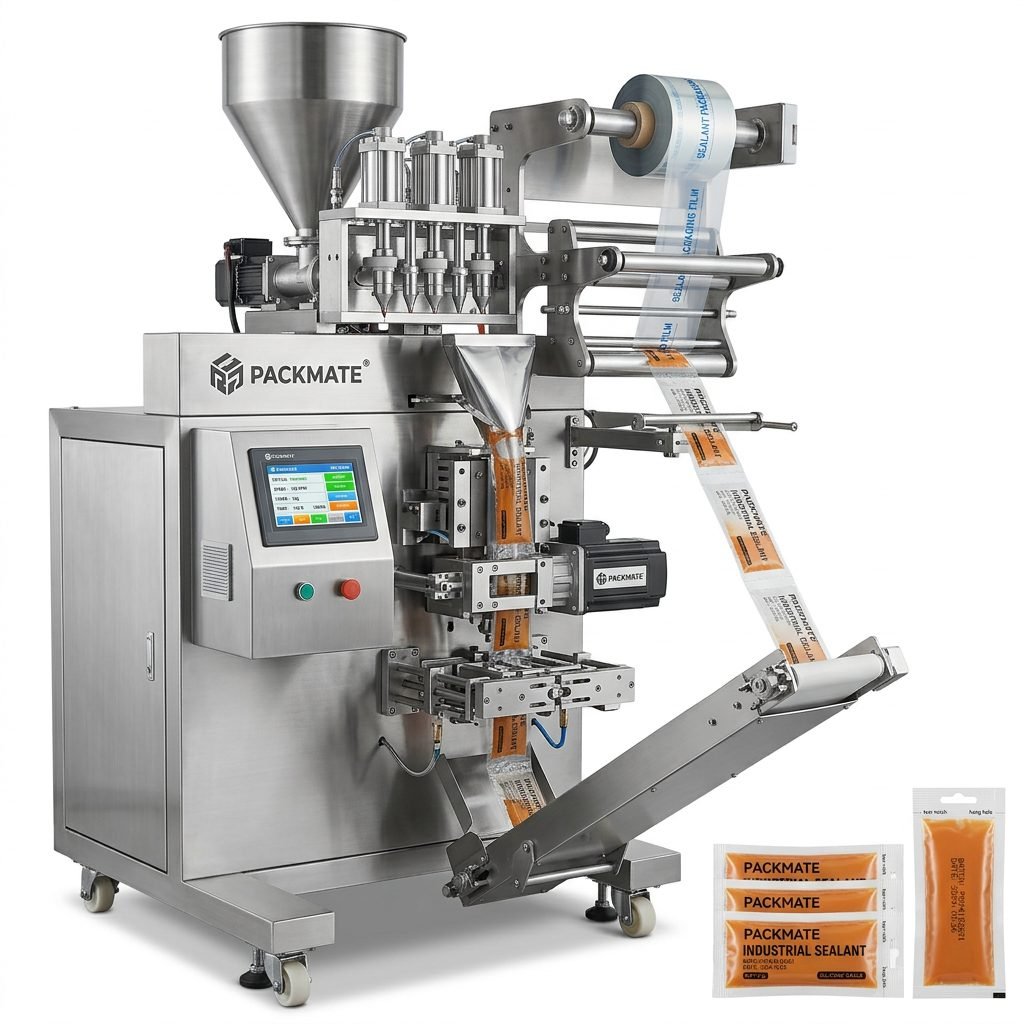
Liquids, such as syrups, suspensions, or sterile solutions, present challenges of leakage, foaming, and accurate volumetric or gravimetric filling. Turnkey lines for liquids employ piston fillers or peristaltic pumps designed for sanitary operation and easy cleaning. Inline vision systems inspect for fill level, cap placement, and label alignment. For sensitive biologics, the line can be designed to operate in a controlled environment or integrated with isolator technology.
The Turnkey Advantage: From Vision to Validation
The true value of a turnkey production line lies in the holistic service. It begins with a deep analysis of the product characteristics, required output, and regulatory landscape. The provider then designs, manufactures, assembles, and factory acceptance tests (FAT) the entire line as one cohesive unit. This includes all mechanical integration, electrical control systems (often with a unified PLC/HMI), and software for monitoring and data collection. Upon installation at your facility, the provider manages site acceptance testing (SAT), operational qualification (OQ), and supports performance qualification (PQ), delivering a production-ready, validated system. This single-point responsibility drastically reduces project timeline, risk, and long-term operational headaches. You can see examples of such integrated systems in our detailed project case studies.
Why Partner with an Experienced Turnkey Provider?
Selecting a partner for your pharmaceutical packaging line is a long-term decision. Experience matters. A company with a proven track record, like Packmate, brings over two decades of specialized knowledge. Their 20,000㎡ modern facility is not just a factory; it’s an innovation hub where lines are pre-built and tested under real-world conditions before shipment. This experience translates into robust machine design, intelligent layout planning for optimal workflow, and deep insights into solving the unique challenges of packaging pharmaceutical-grade granules, powders, and liquids. Their commitment extends beyond installation, offering comprehensive training, spare parts, and technical support to ensure your line remains productive for years.
Future-Proofing Your Investment
The pharmaceutical landscape is constantly evolving. A well-designed turnkey line is modular and scalable. It should allow for future integration of additional modules like more advanced inspection systems, serialization hardware, or robotic palletizers without requiring a complete overhaul. Partnering with an innovative provider ensures your investment is protected and can adapt to new products and regulations.
Conclusion
In the high-stakes world of pharmaceutical manufacturing, the packaging line is a critical control point. For granules, powders, and liquids, investing in a custom-engineered, turnkey packaging line is the most reliable path to achieving compliance, efficiency, and market agility. It consolidates responsibility, streamlines validation, and delivers a synchronized production system designed for peak performance and patient safety. By choosing a partner with deep expertise and a full-service approach, you secure not just machinery, but a strategic asset for your company’s future.
Frequently Asked Questions (FAQs)
1. What is the lead time for a complete turnkey pharma packaging line?
Lead time varies significantly based on line complexity, customization, and validation requirements. A standard line for sachets or stick packs may take 4-6 months from order to delivery, while highly complex liquid lines with full serialization can take 8-12 months. A detailed project plan with milestones is provided after the initial design phase.
2. How do you ensure the line meets cGMP and regulatory standards (e.g., FDA, EU GMP)?
Our lines are designed with cGMP principles from the ground up. This includes using 316L or equivalent stainless steel for contact parts, designing for cleanability (rounded corners, minimal dead legs), providing full documentation packs (DQ, IQ, OQ templates), and integrating data recording systems. We design to major international standards, but final validation is always site-specific.
3. Can your lines handle very small batch sizes or frequent product changeovers?
Yes, modern servo-driven machines and smart line design facilitate quick changeovers. Features like recipe storage on the HMI, quick-change tooling kits, and color-coded parts can reduce changeover time dramatically, making the lines suitable for small batches and high product variety.
4. What kind of after-sales support and training do you provide?
We provide comprehensive training for operators, mechanics, and engineers during installation and commissioning. Our support includes a 24/7 remote assistance hotline, an online spare parts portal, and scheduled preventive maintenance visits. Detailed manuals and video guides are also supplied. Learn more about our commitment on our service and support page.
5. Do you offer solutions for pharmaceutical serialization and aggregation?
Absolutely. We can integrate leading serialization hardware (printers, cameras, coders) and software solutions into the turnkey line. The line’s central control system manages the serialization data flow, ensuring compliance with regional regulations like the EU FMD or the U.S. DSCSA.