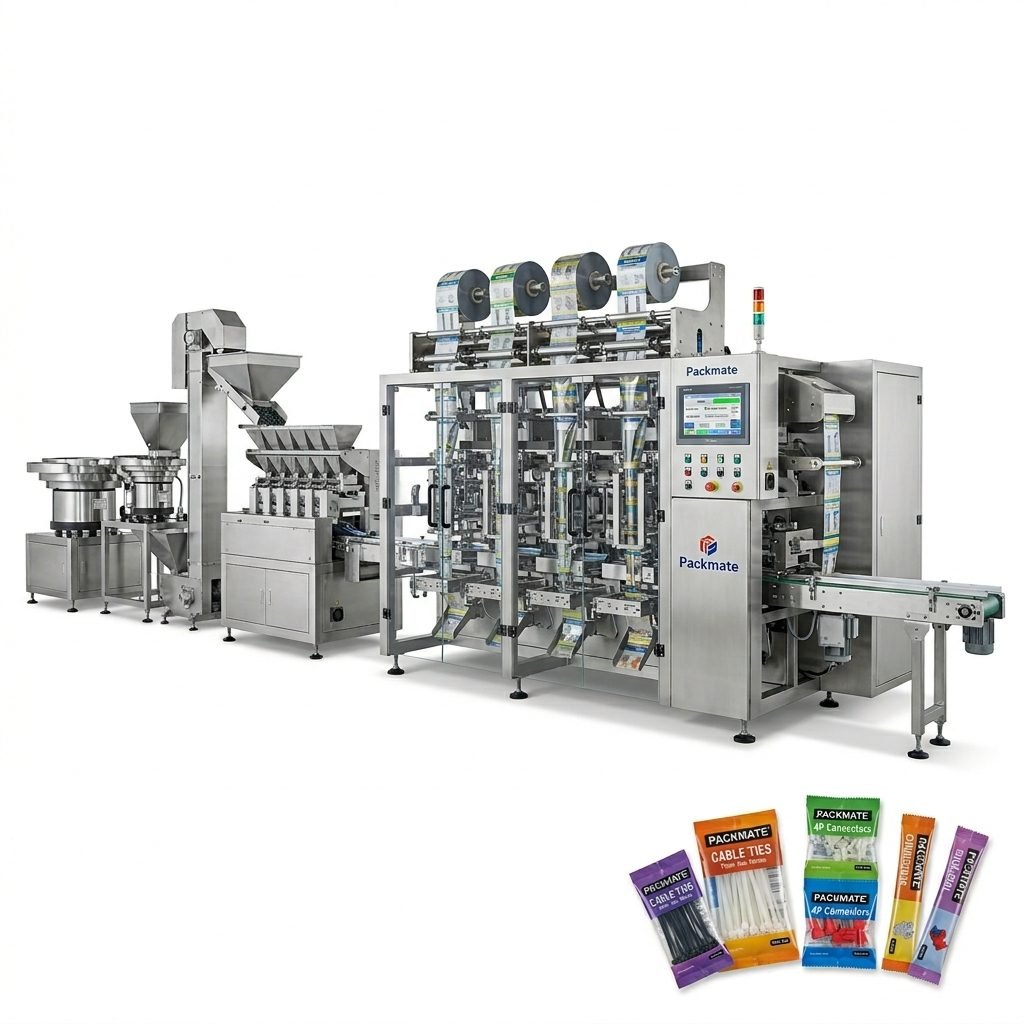
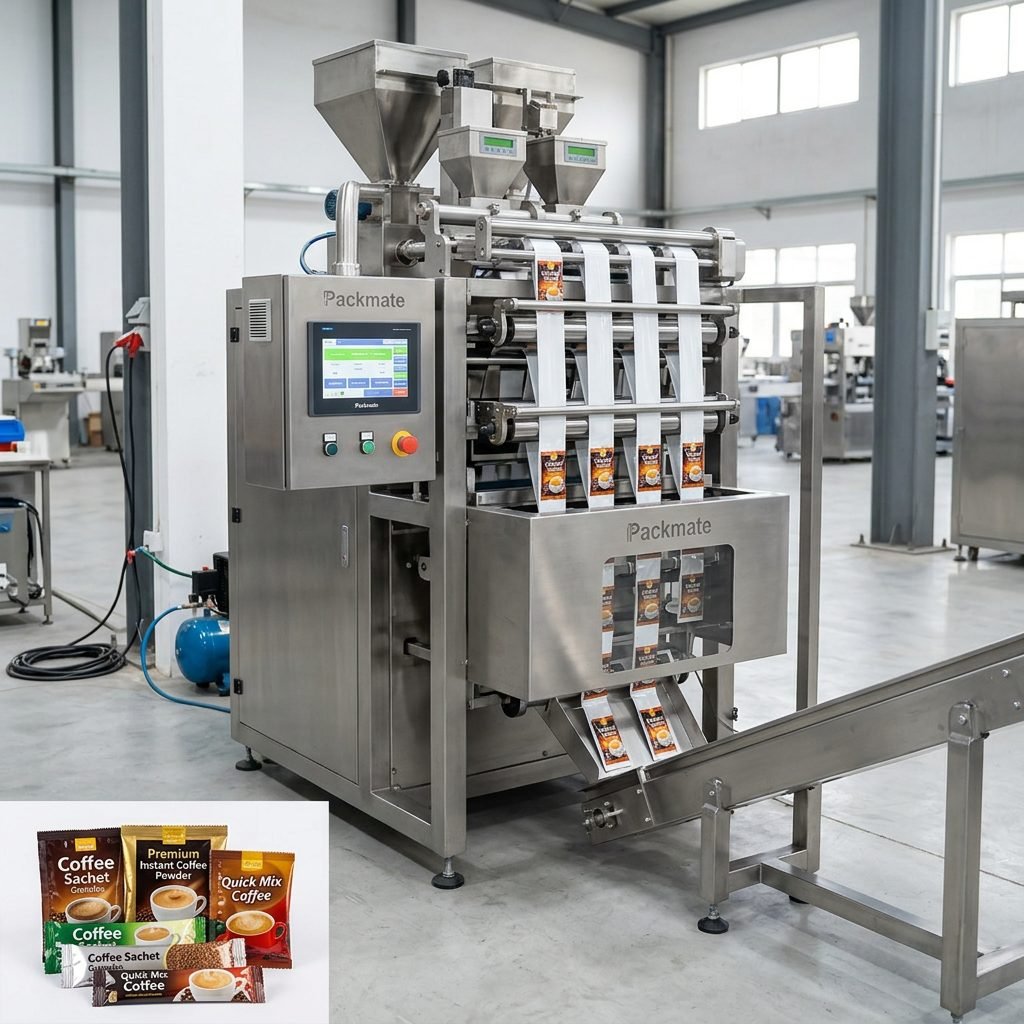
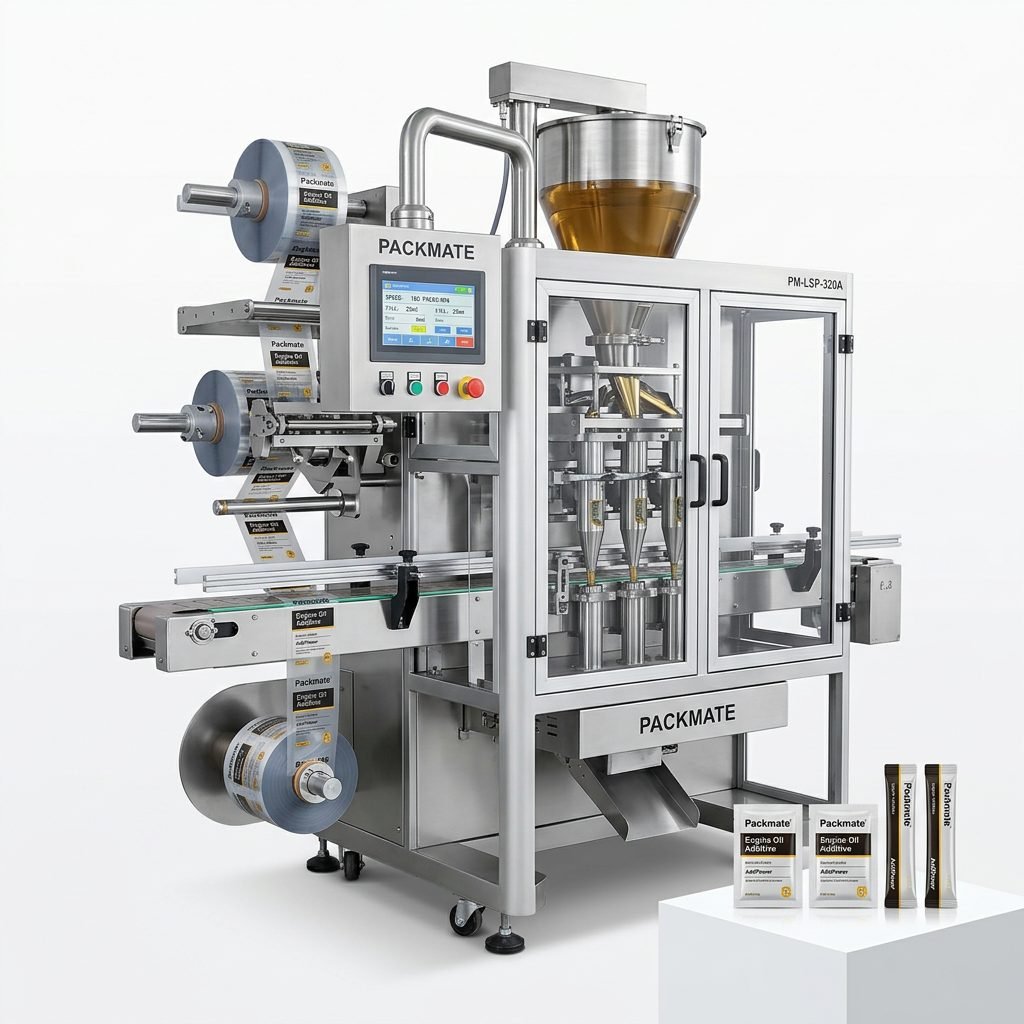
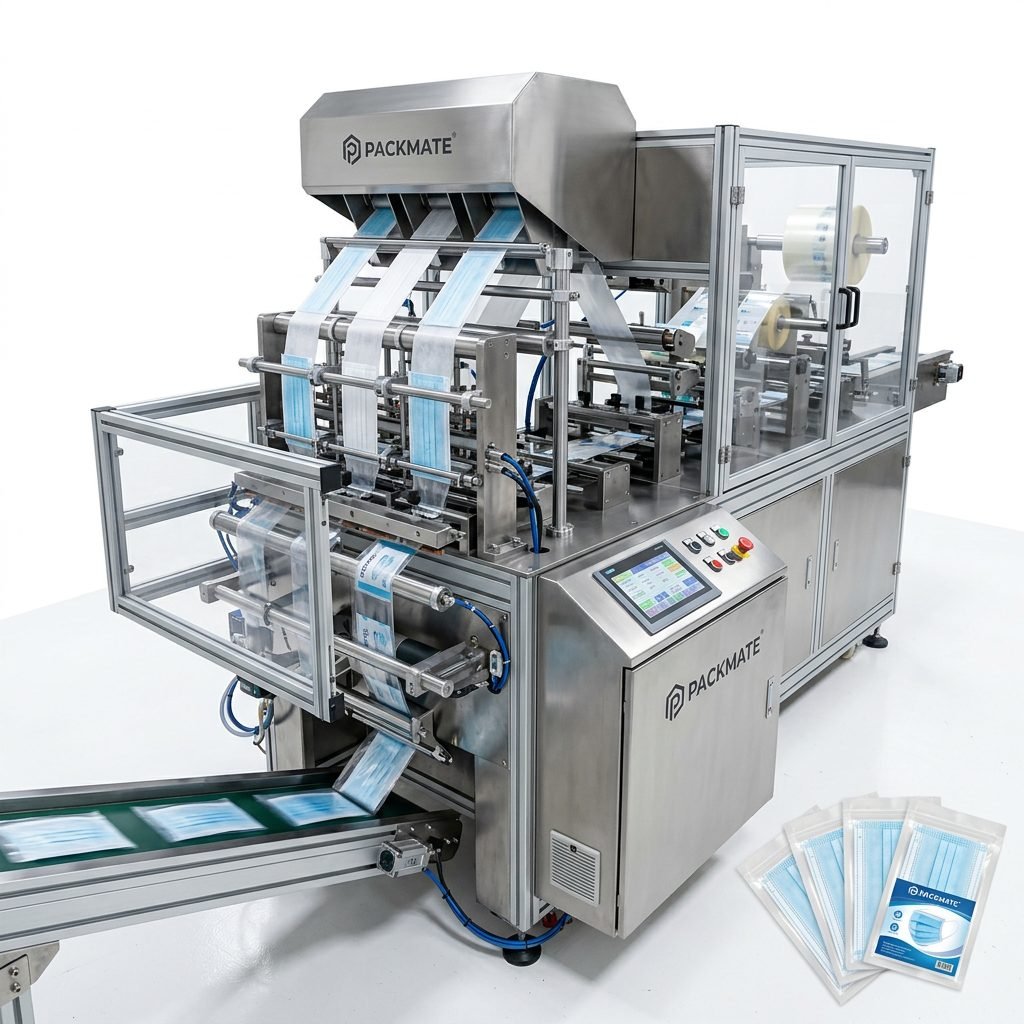
In today’s fast-paced and highly regulated manufacturing landscape, industries such as food, pharmaceuticals, and health products face immense pressure to deliver safe, consistent, and high-quality products at scale. The final and often most critical stage of this process is packaging. An intelligent management gate packaging line is no longer a luxury but a strategic necessity, serving as the crucial control point for quality, efficiency, and traceability before products reach the consumer. This article delves into the comprehensive supply solutions for these advanced packaging systems, exploring how they are tailored to meet the stringent demands of these vital sectors.
The Imperative for Intelligent Packaging in Critical Industries
The convergence of automation, data analytics, and precision engineering has given rise to the intelligent packaging line. Unlike traditional systems, these lines are integrated ecosystems where every component communicates. For food producers, this means ensuring freshness and preventing contamination. In the pharmaceutical sector, it translates to absolute accuracy in dosing, batch integrity, and compliance with Good Manufacturing Practices (GMP). Health and nutraceutical companies rely on them to guarantee product potency and correct labeling. The intelligent management gate is the brain of this operation, making real-time decisions to accept, reject, or reroute packages based on a multitude of sensor inputs.
Core Components of an Intelligent Packaging Line Supply Solution
A complete supply solution encompasses far more than just machinery. It is a turnkey partnership that includes:
- Customized Line Design & Integration: Every product has unique characteristics. Solutions begin with a deep analysis of the product format (granules, powder, liquid, tablets) and output goals to design a seamless line from filling to cartoning.
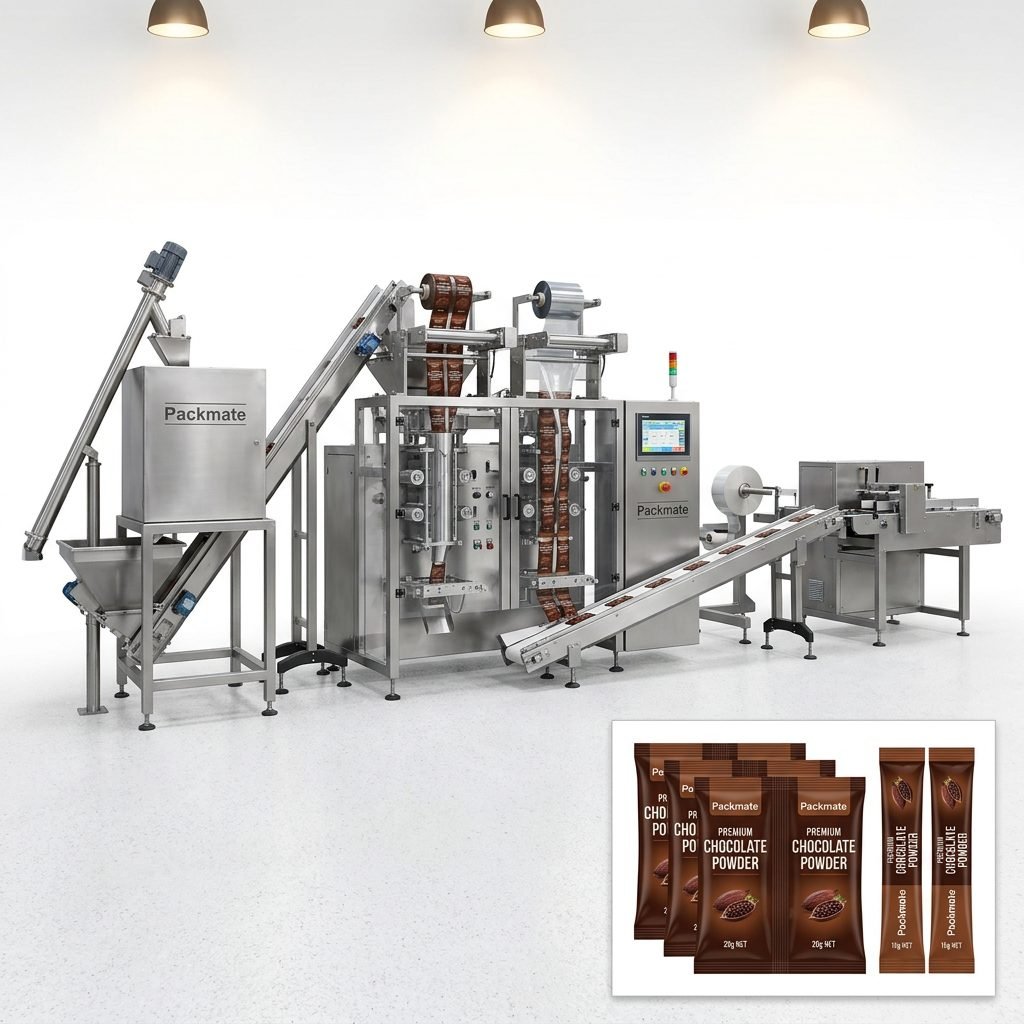
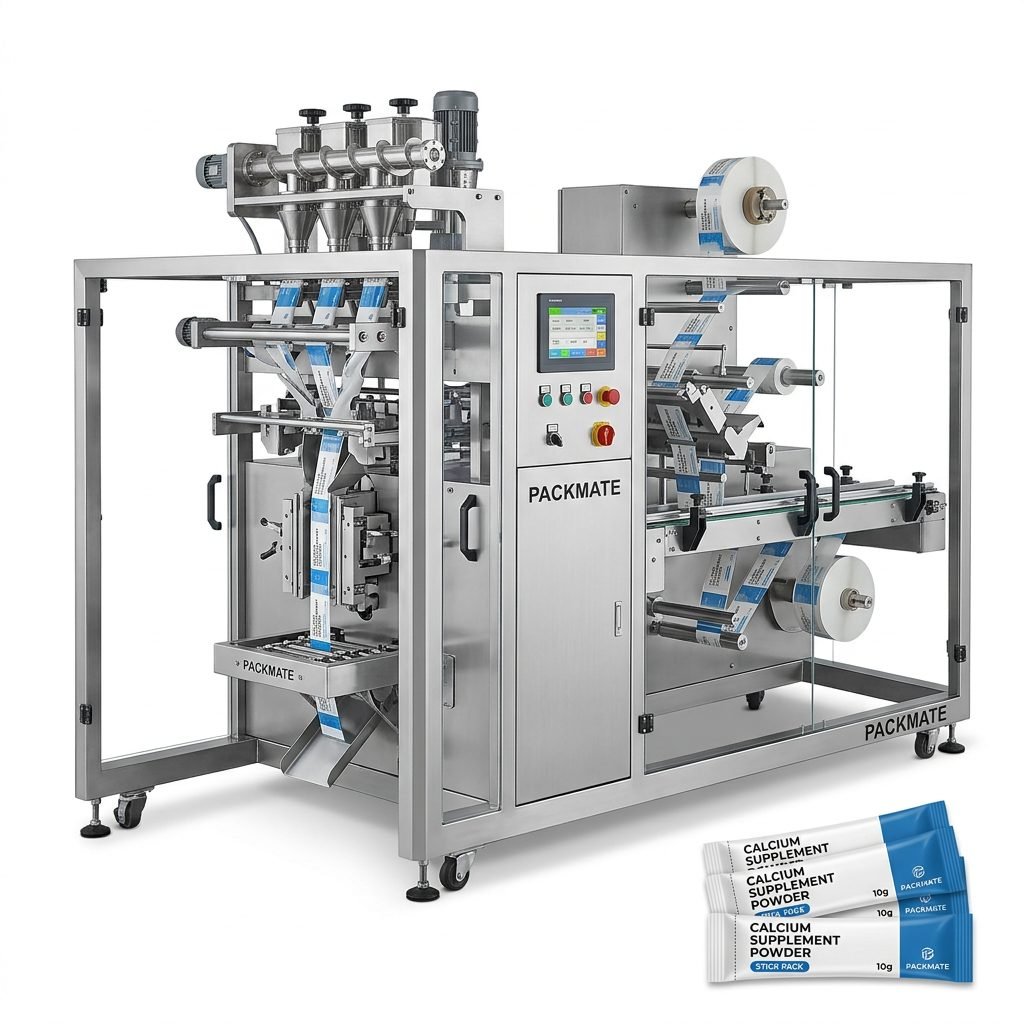
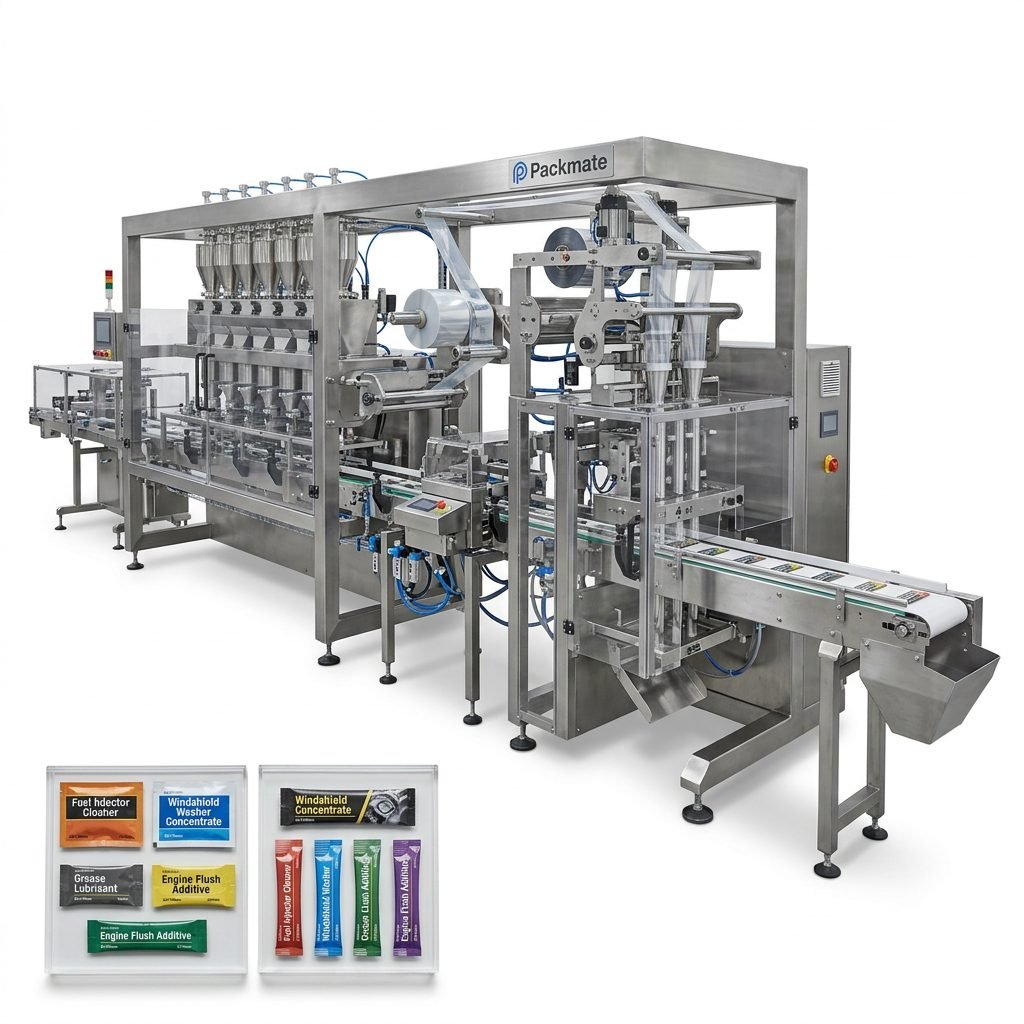
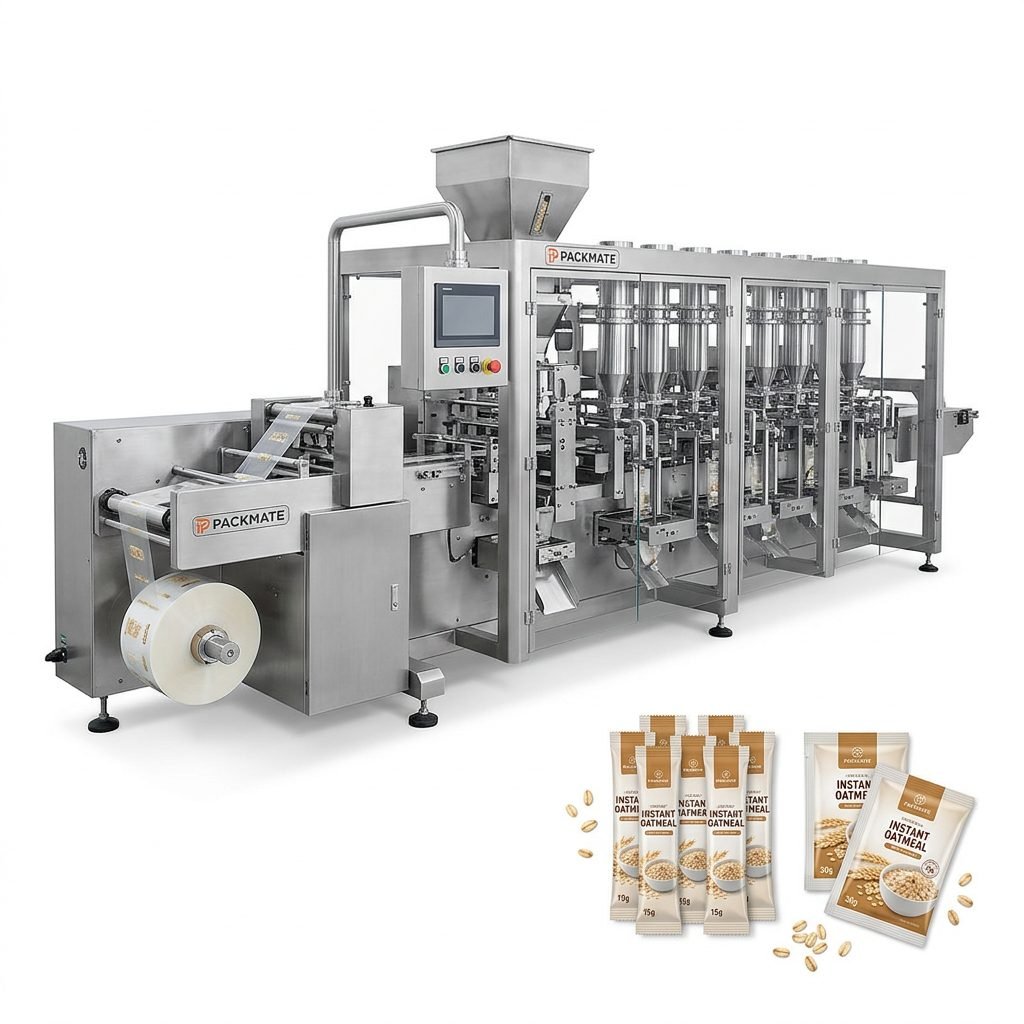
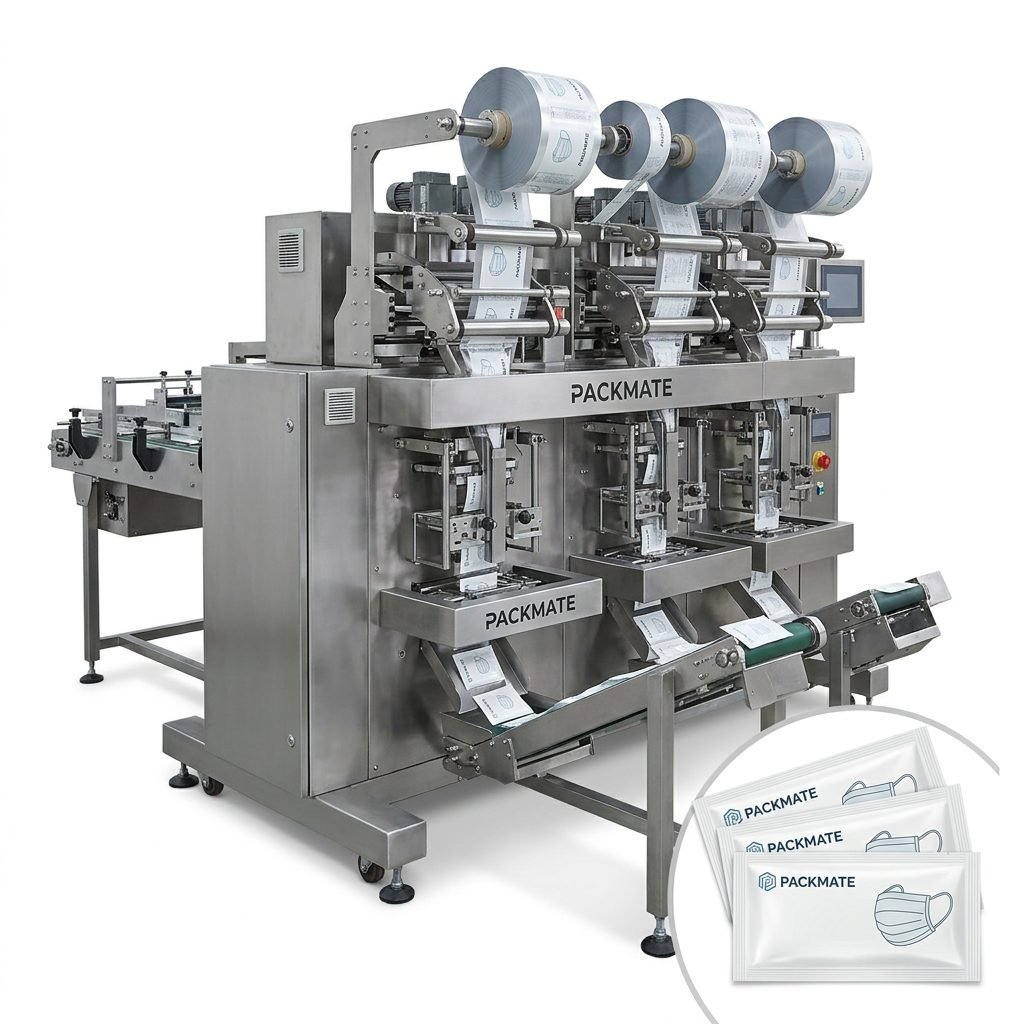
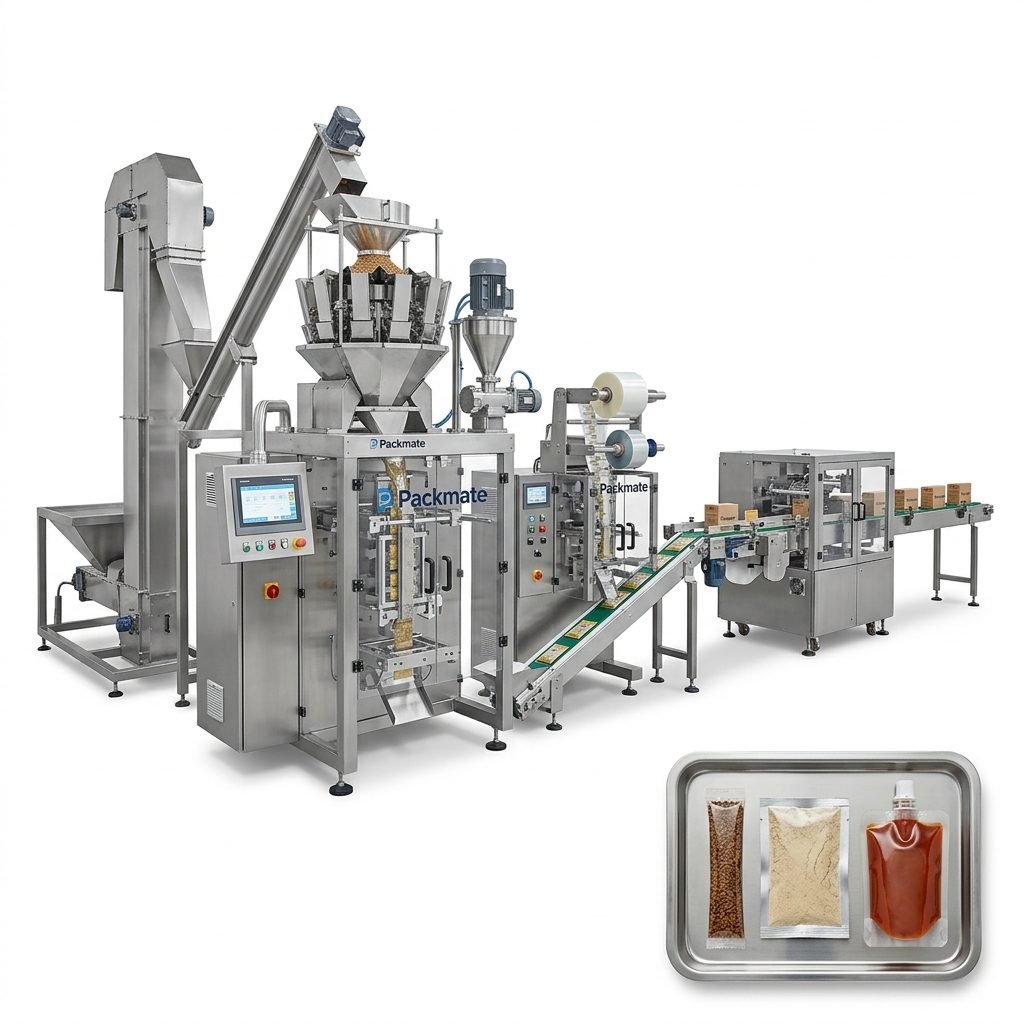
- Advanced Primary Packaging Machines: This includes multi-lane stick pack machines, high-speed sachet machines, and large-volume baggers, all equipped with servo-driven precision for consistent weight and fill.
- The Intelligent Management Gate: Typically featuring vision inspection systems, checkweighers, metal detectors, and label verifiers. This gate validates every parameter—weight, seal integrity, label presence/correctness, and foreign object contamination.
- Data Hub & Production Software: The software aggregates data from all machines and inspection points, providing OEE (Overall Equipment Effectiveness) dashboards, trend analysis, and generating compliant batch reports automatically.
- Downstream Handling & Robotics: Automated cartoning, case packing, and palletizing systems that interface directly with the management gate, ensuring only approved products move forward.
Leading providers like Packmate (GuangDong) Co., Ltd. excel in delivering such integrated solutions, leveraging over two decades of engineering expertise to build reliability into every system.
Sector-Specific Applications and Benefits
Food Industry: Ensuring Safety and Extending Shelf Life
For food products, from instant coffee granules to soup powders, the primary concerns are hygiene, accurate filling, and package integrity. An intelligent line with nitrogen flushing capabilities, coupled with a management gate that performs 100% seal inspection, drastically reduces the risk of spoilage and recall. Real-time checkweighing ensures compliance with net content regulations, protecting brand reputation and avoiding costly give-away.
Pharmaceutical Industry: Compliance and Zero Defects
The pharmaceutical environment tolerates zero error. Packaging lines must be validated and comply with stringent FDA and EMA regulations. Intelligent solutions here focus on audit trails, serialization for track-and-trace, and absolute accuracy. The management gate acts as a final guarantor, rejecting any blister pack with a missing tablet or any vial with an incorrect label. This level of control is essential for patient safety and regulatory adherence, transforming packaging from a cost center into a critical component of quality assurance.
Health & Nutraceutical Products: Building Consumer Trust
This fast-growing sector blends the needs of food and pharma. Consumers demand transparency and quality. Intelligent packaging lines provide this by ensuring precise dosing of active ingredients in supplement sticks or sachets. Vision systems verify that marketing claims and ingredient lists on labels perfectly match the product inside. This traceability, from raw material to finished box, is a powerful tool for brand building and can be a key differentiator in a crowded market. You can see real-world implementations in our detailed case studies.
Choosing the Right Supply Partner: Beyond the Machine
Selecting a supplier for an intelligent packaging line is a long-term strategic decision. Key considerations include:
- Proven Industry Experience: Look for a partner with a documented history in your specific sector, understanding its unique challenges and regulations.
- Technical Support & Training: The most advanced line is only as good as the team operating it. Ensure comprehensive training and readily available service support.
- Scalability & Future-Proofing: Can the system adapt to new product formats or higher speeds? Modular design philosophy is crucial.
- Global Compliance Standards: The partner’s manufacturing processes and final equipment should meet international safety and quality standards, evidenced by relevant certifications.
A partner like Packmate, with its 20,000㎡ modern facility and dedicated R&D team, embodies this holistic approach, ensuring clients receive not just machines, but a productivity partnership.
The Future: Connectivity and Sustainable Intelligence
The evolution of Industry 4.0 is pushing intelligent packaging lines further. The future lies in deeper connectivity—where packaging data informs upstream production and downstream logistics. Predictive maintenance, powered by AI analysis of machine sensor data, will minimize unplanned downtime. Furthermore, sustainability is becoming a core driver. Intelligent lines are being optimized to reduce material waste through precise filling, support the use of recyclable mono-materials, and incorporate energy-saving modes without compromising output.
Implementing an intelligent management gate packaging line is a significant investment that pays dividends in risk reduction, operational efficiency, and brand protection. For food, pharma, and health product manufacturers, it represents the definitive step towards a resilient, transparent, and future-ready production operation.
Frequently Asked Questions (FAQs)
1. What is the primary function of an “intelligent management gate” in a packaging line?
The intelligent management gate is a centralized quality control checkpoint. It integrates various inspection systems (like vision, checkweighing, metal detection) to make a pass/fail decision on each individual package in real-time, ensuring only products meeting all specified criteria proceed to shipping.
2. How can an intelligent packaging line improve compliance for pharmaceutical companies?
It automates and documents critical quality checks, provides unalterable audit trails, enables product serialization for track-and-trace, and ensures 100% inspection, which is often required by regulators. This significantly reduces human error and simplifies regulatory reporting.
3. Are these solutions suitable for small and medium-sized enterprises (SMEs)?
Yes. Modern solutions are scalable. Suppliers can design cost-effective, modular lines that incorporate key intelligent features appropriate for the production volume and risk profile of an SME, allowing them to benefit from automation without the scale of a large multinational.
4. What is the typical ROI period for investing in such a sophisticated packaging line?
The Return on Investment period varies but is often between 1 to 3 years. Savings are realized through reduced material waste, lower labor costs, minimized product giveaway, virtual elimination of costly recalls, and increased overall production throughput.
5. How does the supplier support the line after installation and commissioning?
Reputable suppliers offer comprehensive after-sales support, including remote diagnostics, readily available spare parts, preventive maintenance plans, and software updates. They provide operator and maintenance technician training to ensure optimal line performance throughout its lifecycle. For more details, visit our dedicated FAQs page.