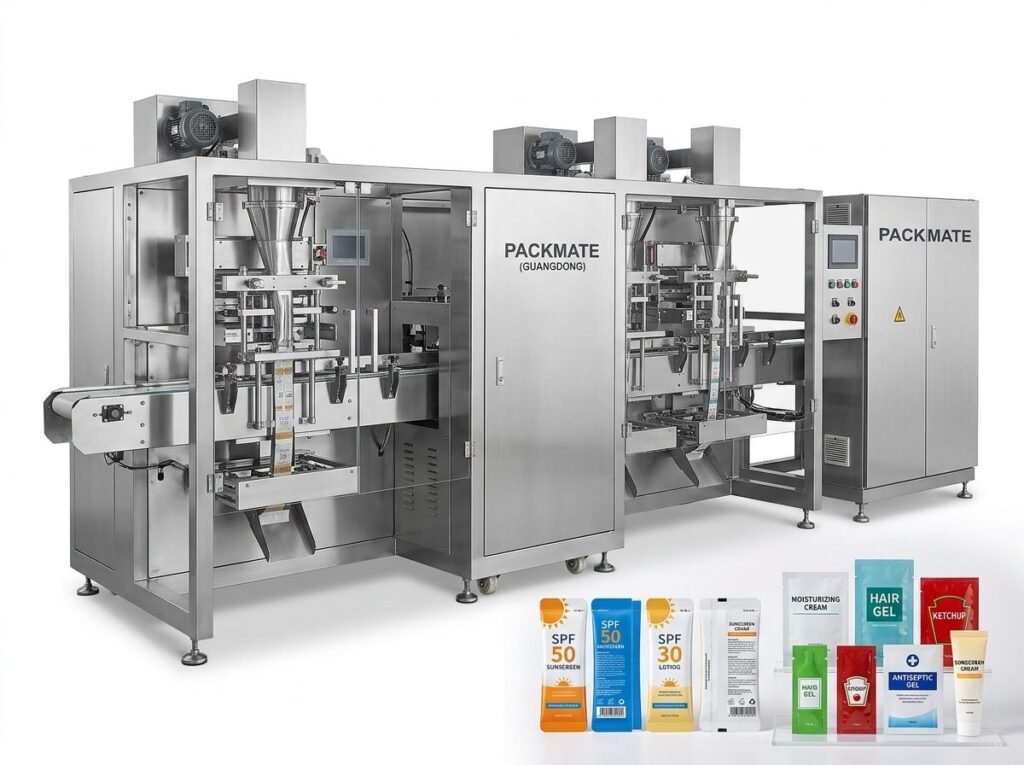
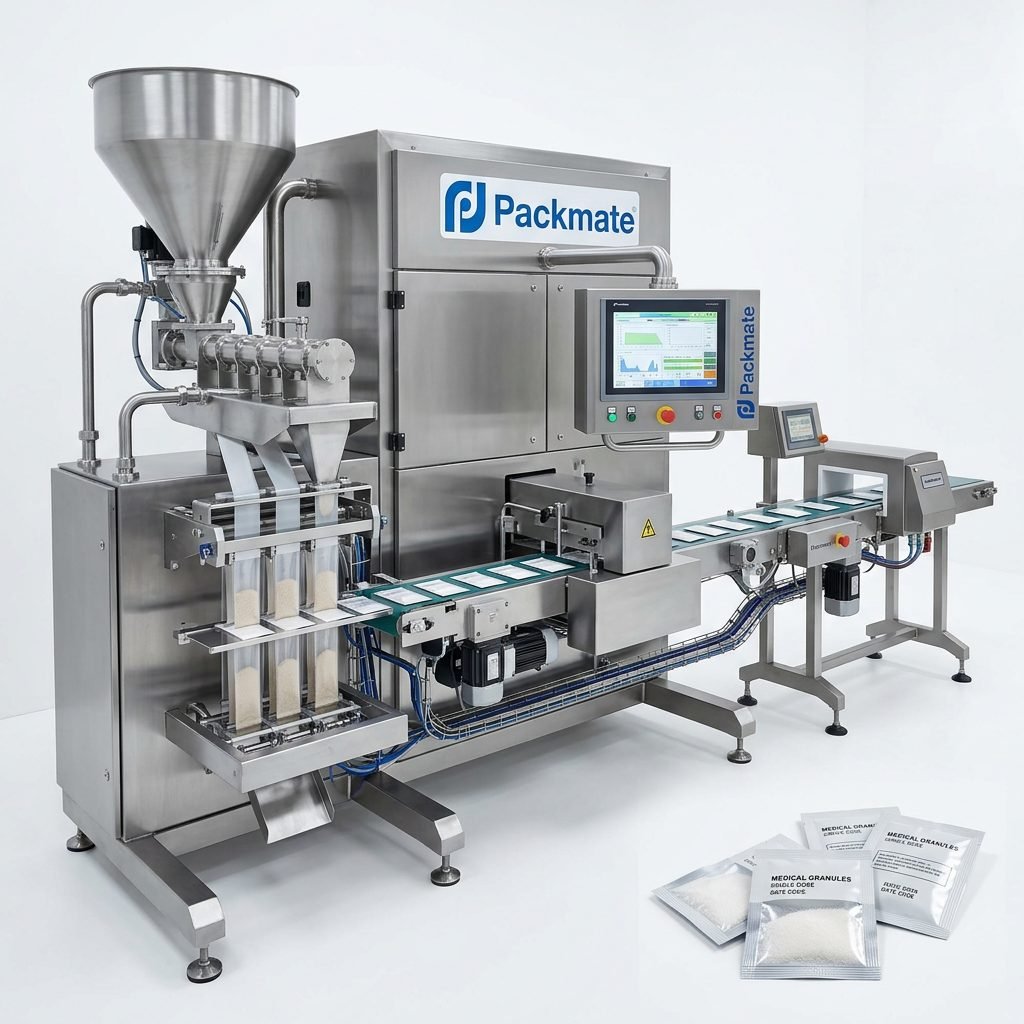
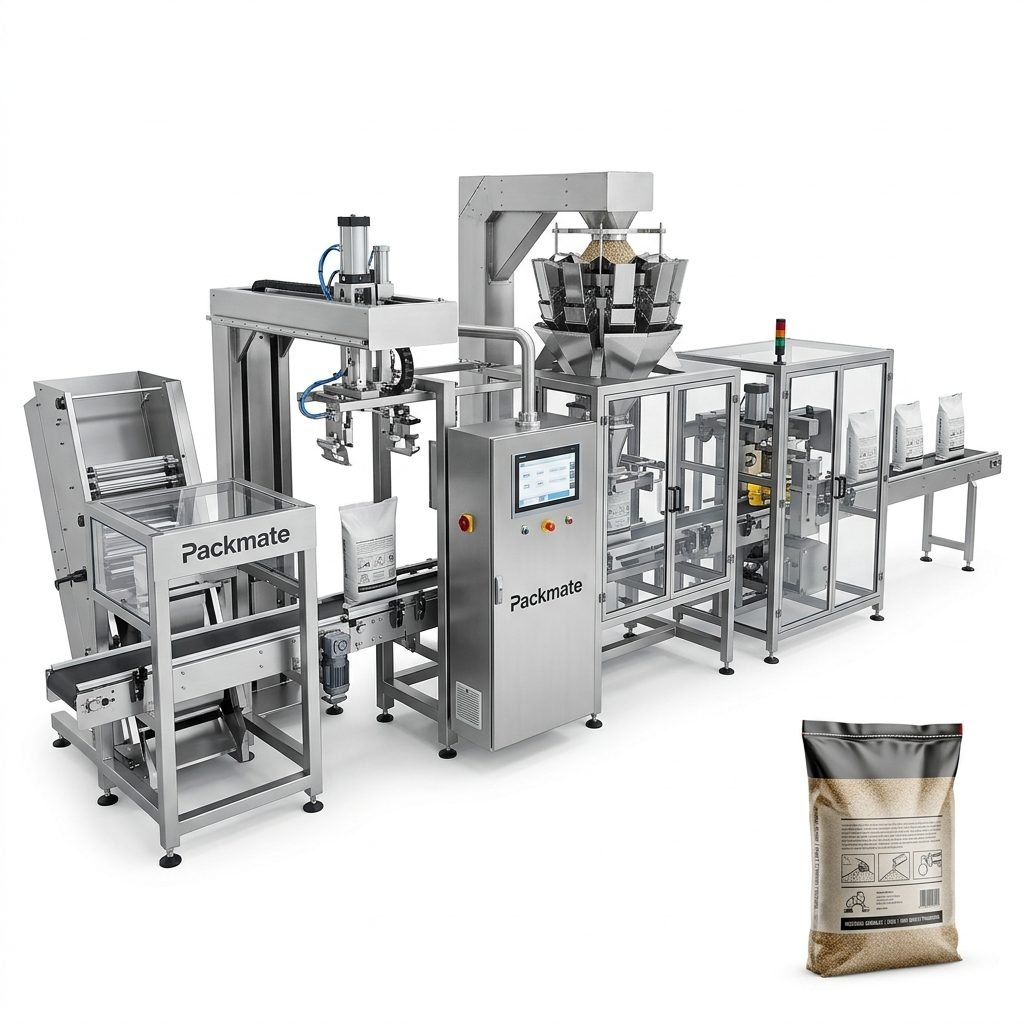
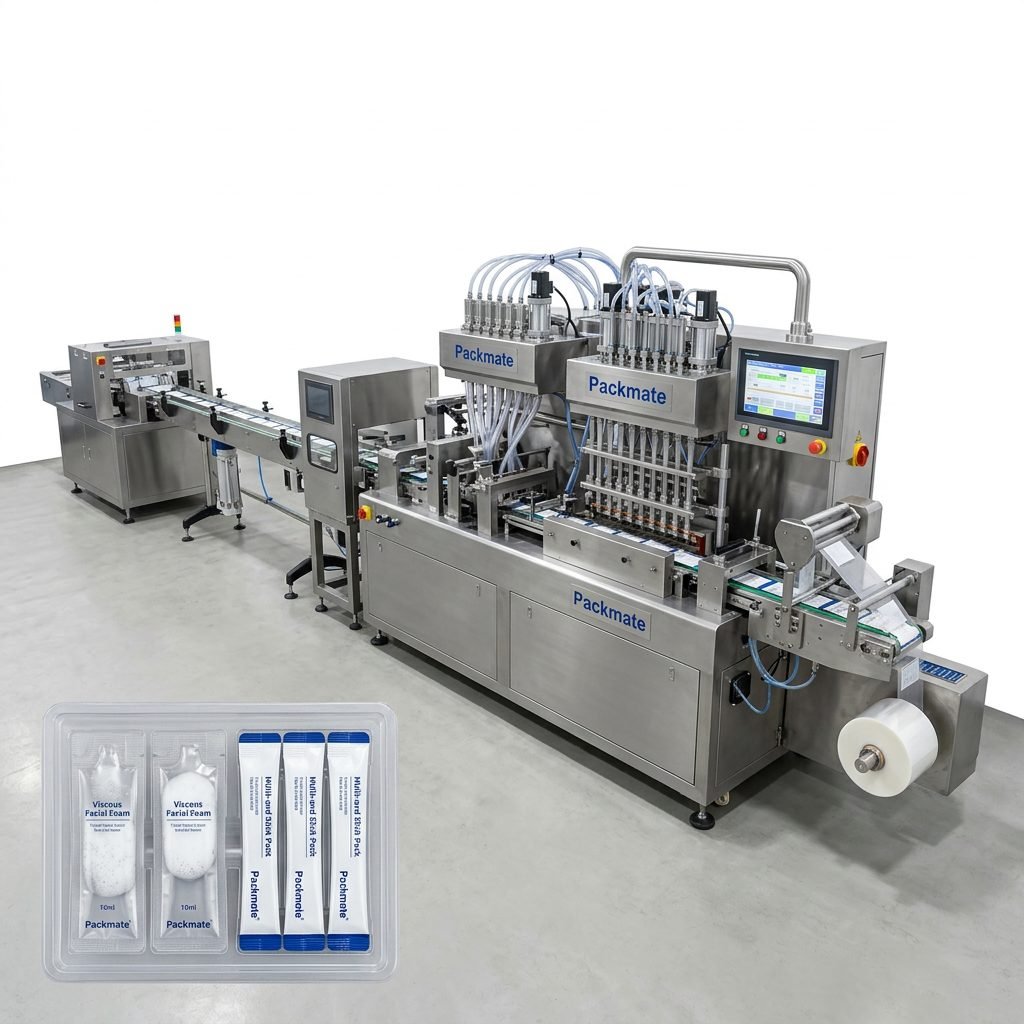
In the competitive landscape of food, pharmaceutical, and health product manufacturing, efficiency, safety, and presentation are paramount. A specialized bottle packaging line is not merely a conveyor belt; it is the central nervous system of your production, ensuring product integrity from filling to capping and labeling. For businesses seeking reliability and scalability, investing in a tailored packaging solution is a strategic decision that impacts everything from operational costs to brand perception in the market.
The Critical Role of Specialized Packaging Lines
Each industry segment—food, pharma, health—presents unique challenges that generic equipment cannot adequately address. A holistic bottle packaging line solution integrates various machines into a seamless, automated workflow, dramatically reducing human intervention and the associated risk of contamination or error.
Core Advantages of an Integrated Line:
➤ Enhanced Productivity: Automated lines achieve consistently high output, essential for meeting large-scale demand.
➤ Uncompromised Hygiene: Designed with cleanability and sanitary standards in mind, crucial for pharma and food safety.
➤ Remarkable Flexibility: Quick changeovers between bottle sizes, cap types, and labels allow for agile production scheduling.
➤ Significant Cost Reduction: Minimizes labor costs, material waste, and downtime, improving overall ROI.
Tailored Solutions for the Food Industry
Food products, from sauces and oils to beverages and dressings, require packaging that preserves freshness, prevents leakage, and appeals to consumers. A food-grade bottle packaging line must handle various viscosities and comply with stringent food safety regulations like FDA and EFSA standards.
Key components often include precision liquid fillers, nitrogen flushing systems to extend shelf life, torque-controlled cappers, and high-resolution labelers. The line’s design prioritizes easy cleaning to prevent cross-contamination between production runs, a non-negotiable aspect in food processing. For a deeper look at specific configurations, explore our dedicated packaging solutions.
Precision Engineering for Pharmaceutical Products
The pharmaceutical sector demands the highest levels of accuracy, sterility, and traceability. Packaging lines for medicines, syrups, or sterile solutions are engineered in controlled environments, often incorporating clean-in-place (CIP) and sterilize-in-place (SIP) systems. Every action, from filling exact dosages to applying tamper-evident seals, is governed by precision mechanics and validated software to meet GMP (Good Manufacturing Practice) guidelines.
Critical features include weight checkers to verify fill accuracy, vision inspection systems to detect faulty bottles or missing caps, and integrated coding for batch traceability. This meticulous attention to detail ensures patient safety and regulatory compliance, turning the packaging line into a pillar of quality assurance.
Meeting the Demands of Health & Wellness Products
The booming market for vitamins, supplements, probiotics, and nutraceuticals requires packaging that protects sensitive formulations from moisture, light, and oxygen. Health product lines often blend the speed of food packaging with the precision of pharmaceutical handling.
Essential Considerations for Health Products:
✔ Light-Resistant Bottles: Using amber or opaque PET to protect photo-sensitive ingredients.
✔ Desiccant Insertion: Automated placement of moisture-absorbing packets to ensure product stability.
✔ Child-Resistant Closures: Incorporating safety caps without compromising line speed.
✔ High-Speed Labeling: Applying compliant labels with ingredient lists and usage instructions clearly.
These specialized functions ensure the product’s efficacy is maintained from our production facility to the end consumer.
Why Partner with an Experienced Solution Provider?
Selecting a bottle packaging line is a significant capital investment. Partnering with a seasoned provider like Packmate (GuangDong) Co., Ltd. offers distinct advantages beyond machine procurement. With over 22 years of development, our expertise lies in delivering turnkey solutions—from initial concept and design to installation, training, and ongoing support service.
Our 20,000㎡ modern facility and team of 125+ professionals allow us to engineer, test, and validate complete lines tailored to your specific product and throughput requirements. We understand that a successful installation is measured by its uptime, efficiency, and seamless integration into your existing operations. You can learn more about our journey and capabilities on our Company Profile page.
Future-Proofing Your Packaging Operation
Technology in packaging is rapidly evolving. The next-generation lines incorporate Industry 4.0 principles, featuring IoT sensors for predictive maintenance, data analytics for optimizing performance, and modular designs for easy future upgrades. Investing in a smart, adaptable line today safeguards your operation against tomorrow’s challenges and market shifts.
Whether you are scaling an existing line or building a new facility, considering flexibility and connectivity from the outset is crucial. Reviewing real-world application cases can provide valuable insights into what is achievable.
Frequently Asked Questions (FAQs)
1. What is the lead time for a complete turnkey bottle packaging line?
The lead time varies significantly based on line complexity, customization, and machine availability. A standard line may take 3-6 months from order to delivery, while highly customized systems for novel applications can take longer. A detailed project timeline is provided after the initial consultation and design phase.
2. How do you ensure the line meets our specific hygiene and safety standards?
Our engineering process begins with a thorough analysis of your product and regulatory environment (e.g., FDA, GMP, HACCP). We select materials (e.g., stainless steel grades), design smooth surfaces to avoid bacterial traps, and integrate sanitization protocols. The line can be validated according to your specific quality standards.
3. Can your packaging lines handle different bottle shapes and sizes on the same line?
Yes, a key feature of our modern lines is flexibility. Through modular design and quick-change tooling (like change parts for fillers, cappers, and labelers), you can switch between compatible bottle formats with minimal downtime, often in under 30 minutes.
4. What kind of after-sales support and training do you provide?
We provide comprehensive support including on-site installation supervision, detailed operational training for your technicians, a thorough documentation package, and a warranty period. Remote support and a stock of commonly needed spare parts are also available to ensure your line maintains optimal performance.
5. How energy-efficient and sustainable are your packaging solutions?
Sustainability is a core design consideration. Our lines are engineered for energy efficiency through servo-driven motors that reduce power consumption. We also advise on material reduction strategies, such as lightweighting bottles and optimizing label size, to minimize your environmental footprint and packaging costs.