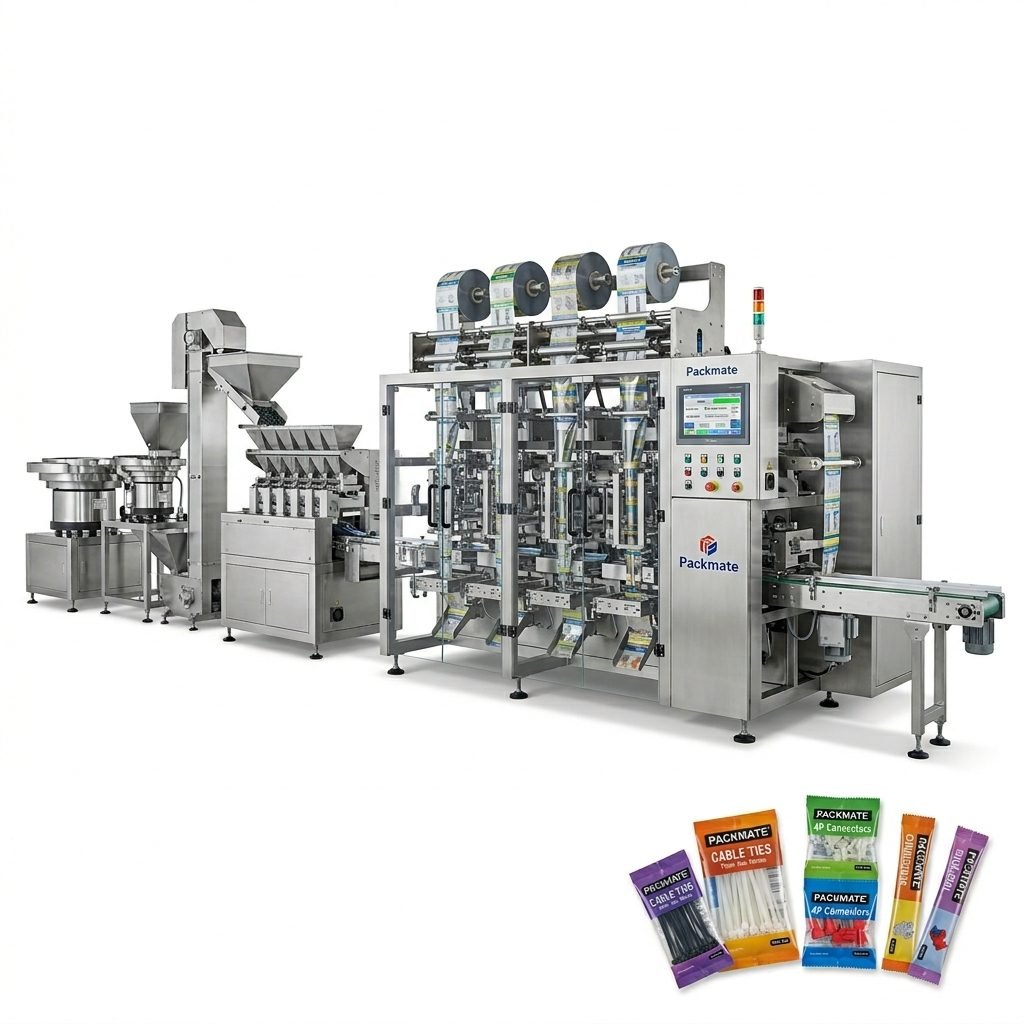
In today’s competitive global marketplace, the packaging of food, pharmaceutical, and health products is far more than a final step in production. It is a critical component of product integrity, brand reputation, and supply chain efficiency. For manufacturers in these highly regulated and sensitive sectors, selecting the right industrial packaging line is a strategic decision. A turnkey solution that seamlessly integrates speed, precision, hygiene, and compliance is not just an advantage—it’s a necessity for sustainable growth and market leadership.
The Unique Packaging Imperatives for Core Industries
Each sector within the food, pharma, and health product domains presents distinct challenges that demand specialized packaging solutions. A one-size-fits-all approach is ineffective and can lead to product waste, regulatory non-compliance, and consumer distrust.
Food Industry: Freshness, Speed & Appeal
Food packaging must act as a robust barrier against moisture, oxygen, and contaminants to ensure extended shelf life and safety. It also needs to operate at high speeds to meet large-volume demands while maintaining portion control accuracy for products like spices, instant beverages, and sauces. The visual appeal of the package—whether a sleek stick pack or a vibrant sachet—plays a vital role in point-of-sale consumer decisions.
Pharmaceutical Sector: Precision & Traceability
This is arguably the most stringent environment. Packaging lines must guarantee absolute accuracy in dosing, often down to the milligram for powders or milliliter for liquids. Compliance with Good Manufacturing Practices (GMP) and other global regulations is non-negotiable. Features like tamper-evidence, batch coding, and serialization for complete traceability throughout the supply chain are essential. Hygiene is paramount, often requiring cleanroom-compatible equipment designs.
Health & Nutraceutical Products: Integrity & Trust
Bridging food and pharma, this sector includes vitamins, protein powders, herbal supplements, and functional foods. Packaging must protect sensitive ingredients from degradation due to light or air. It requires the hygienic integrity of pharma-grade systems alongside the branding flexibility and consumer-friendly formats of the food industry. Accurate filling to prevent under-dosing (consumer fraud) or over-dosing (safety risk) is critical for maintaining brand trust.
Components of a Modern Turnkey Packaging Line
A complete industrial packaging solution is an orchestrated symphony of specialized machinery. Understanding the core components helps in specifying the right system for your products.
1. Feeding & Dosing Systems
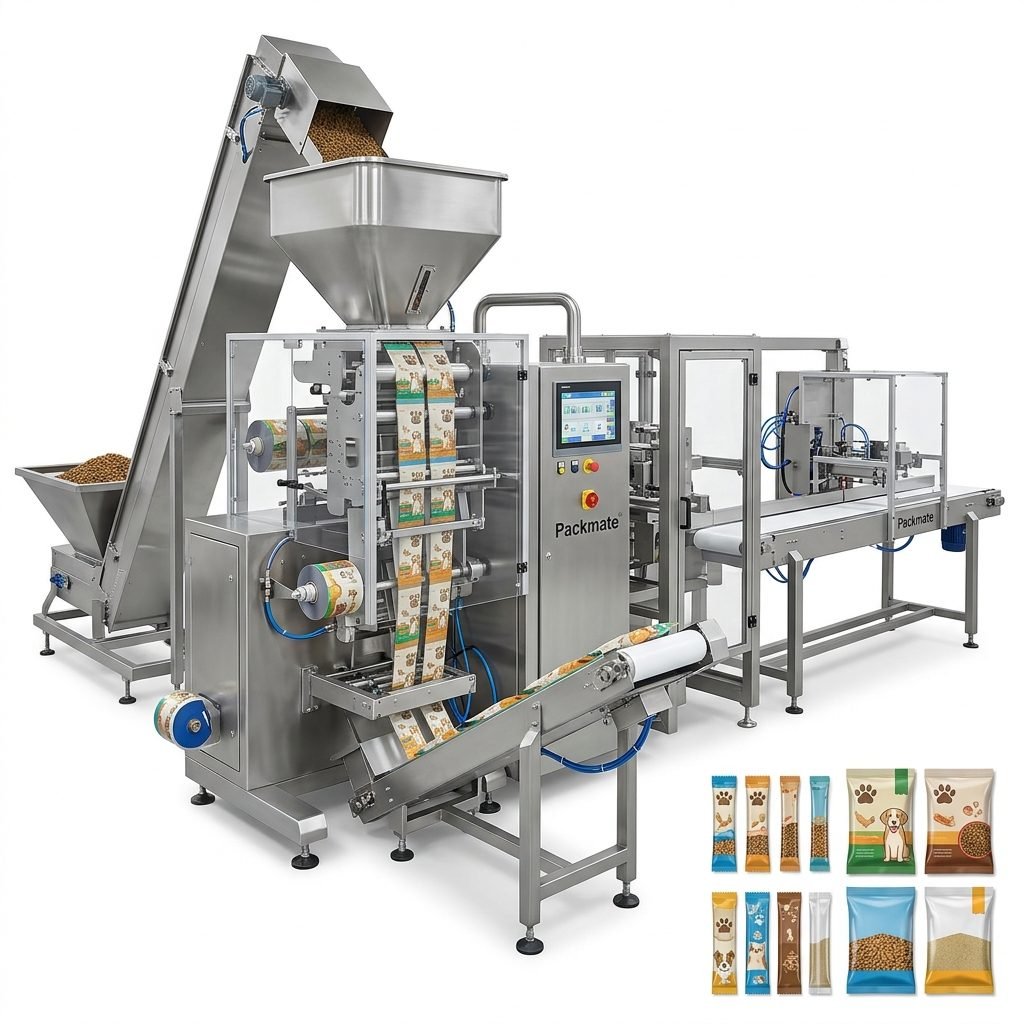
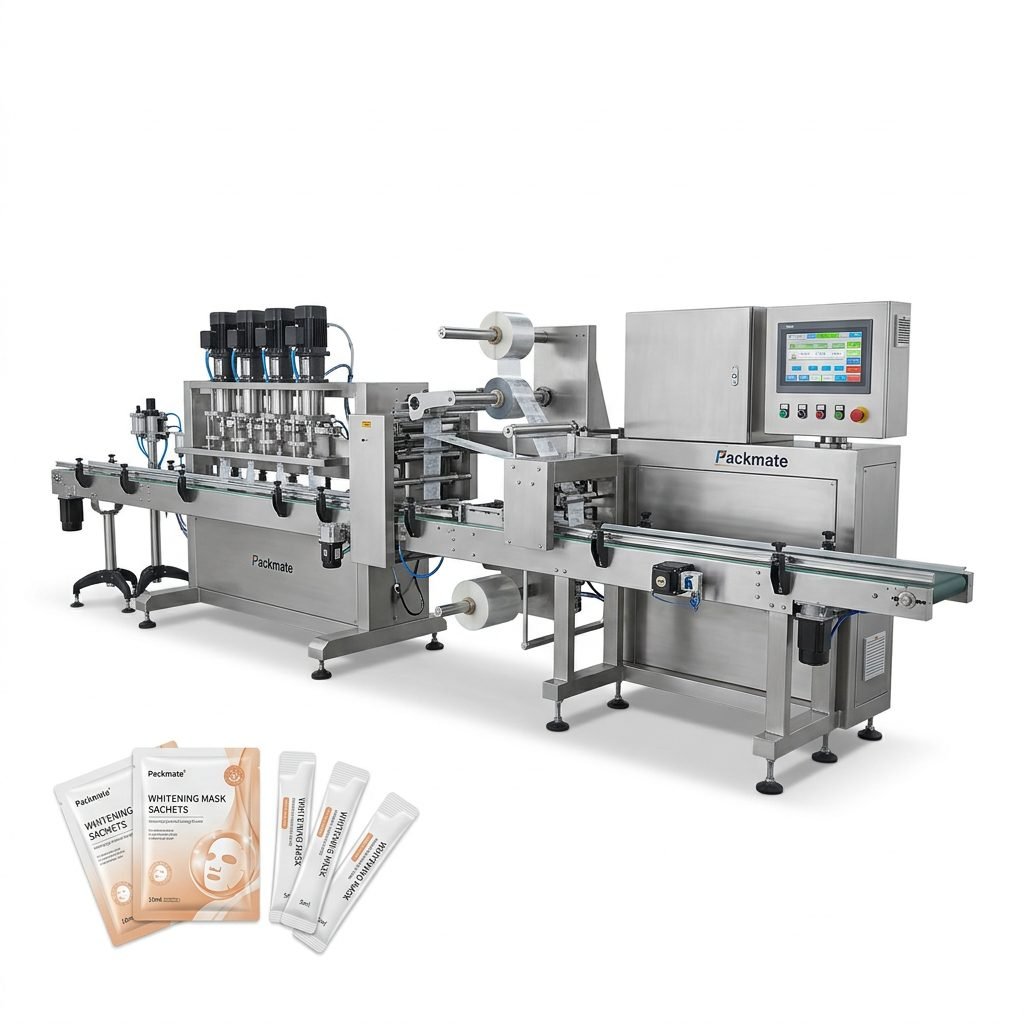
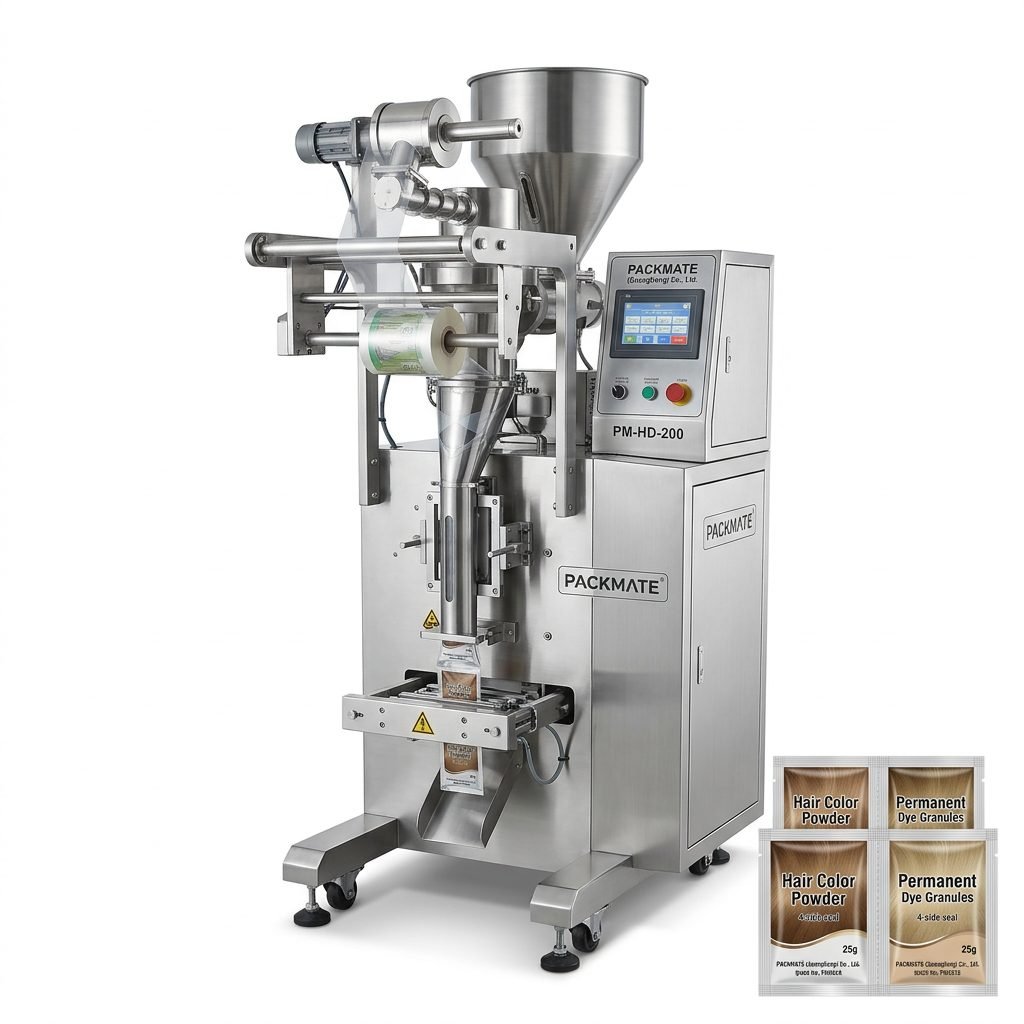
The heart of accuracy. These systems, including auger fillers, volumetric cup fillers, and liquid pumps, must handle diverse product forms—from fine powders and granules to viscous pastes and oils—with consistent precision to minimize giveaway and ensure compliance.
2. Form-Fill-Seal (FFS) Machines
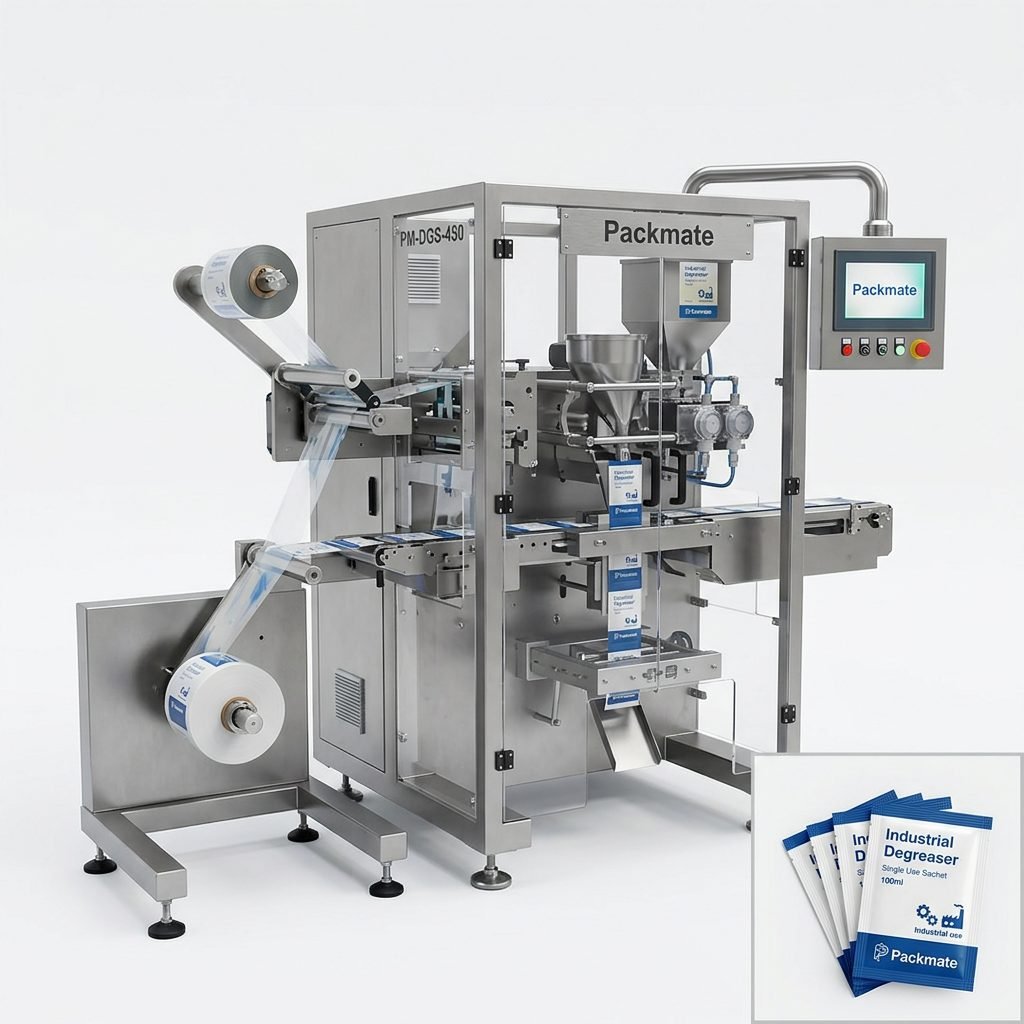
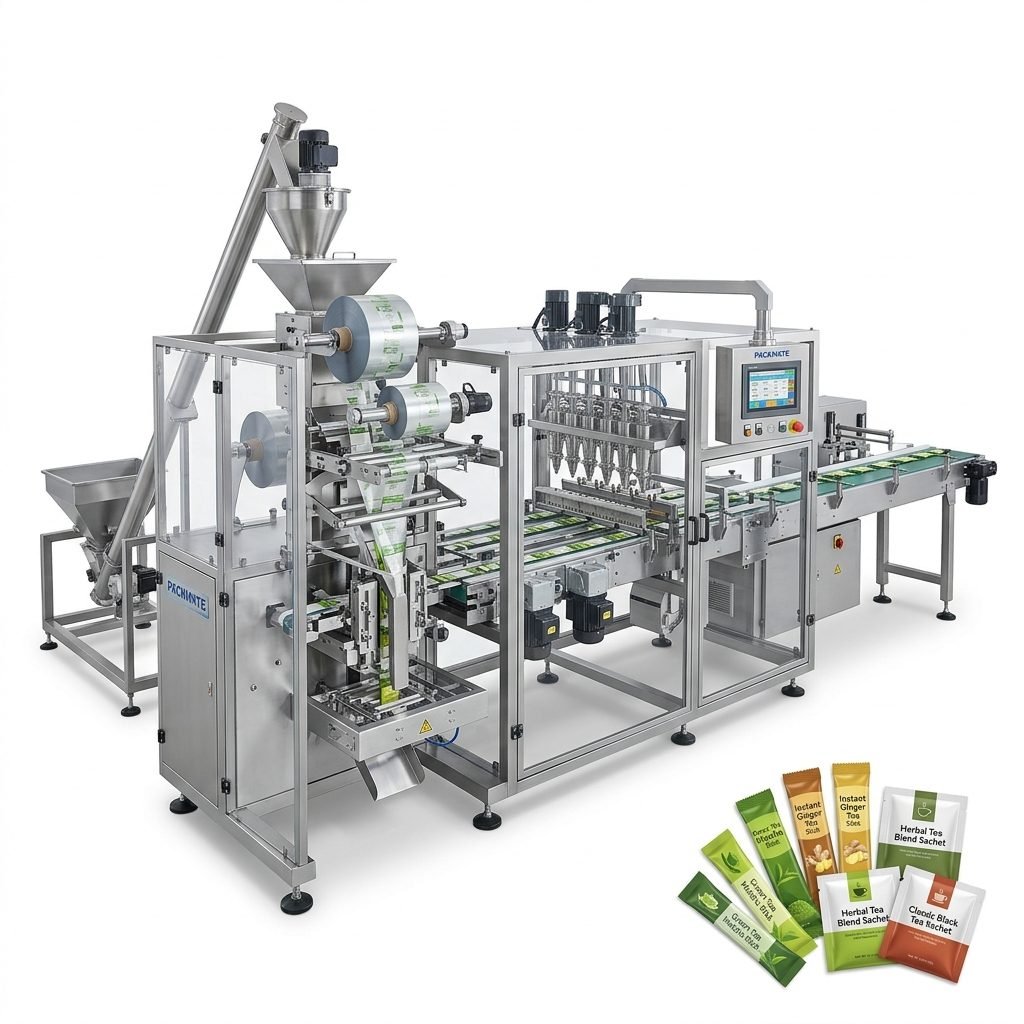
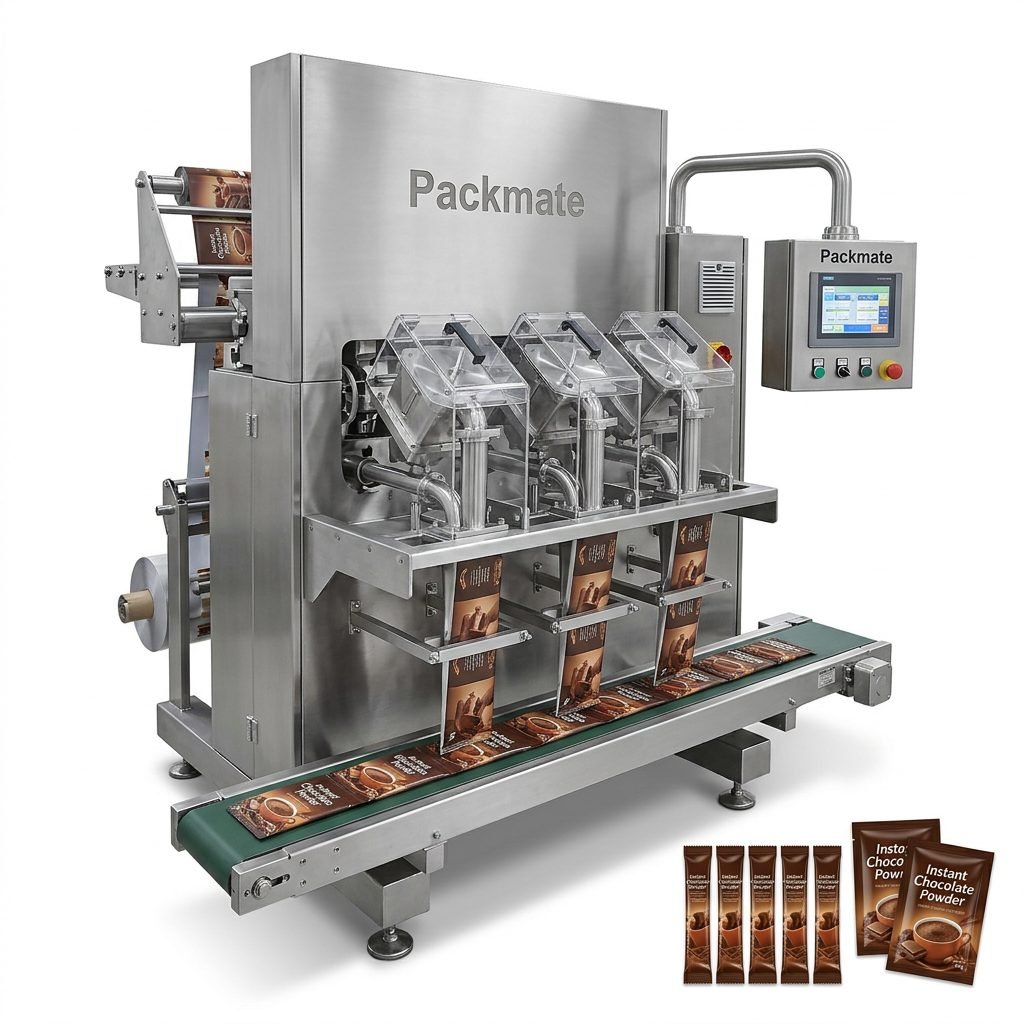
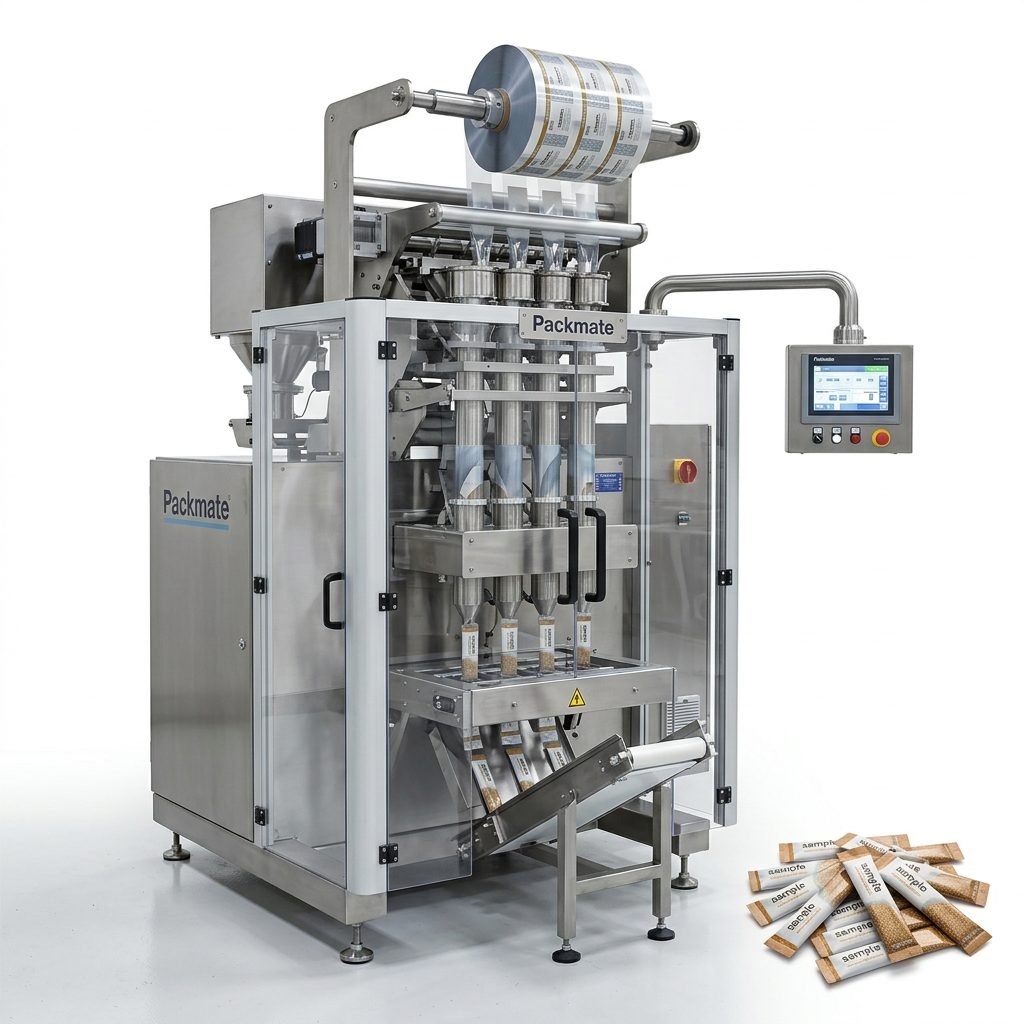
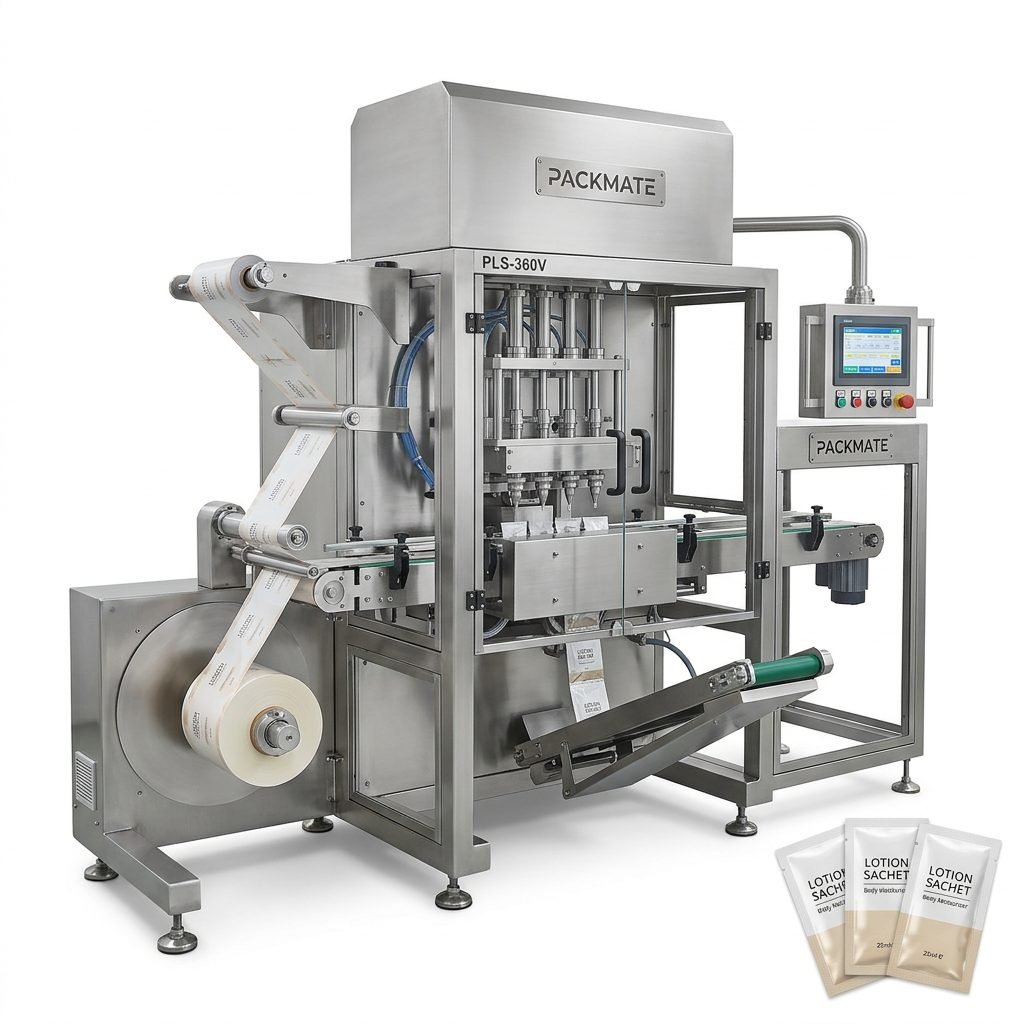
The workhorse of primary packaging. Using rolls of film, these machines form the package (like a sachet or stick pack), fill it with the exact product dose, and seal it hermetically—all in one continuous, high-speed operation. Multi-lane configurations dramatically increase output.
3. Cartoning & Secondary Packaging
After primary packaging, products are often collated into boxes or cartons. Automatic cartoners erect, load, and seal secondary packages, adding another layer of protection and preparing products for shipping and retail display.
4. Control & Monitoring Systems
The brain of the operation. Modern Programmable Logic Controllers (PLCs) and Human-Machine Interfaces (HMIs) allow for precise control of all parameters. They enable real-time monitoring of production counts, speed, and potential faults, facilitating data collection for quality assurance and operational efficiency analysis.
Why Partner with an Experienced Solution Provider?
Investing in a packaging line is a significant capital decision. Partnering with a seasoned provider like Packmate (GuangDong) Co., Ltd. offers unparalleled advantages beyond simply purchasing machinery.
✓ End-to-End Project Management: From initial concept and factory layout planning to machine design, installation, commissioning, and staff training, a turnkey provider manages the entire project, reducing downtime and integration headaches.
✓ Customization & Flexibility: Off-the-shelf machines rarely fit perfectly. An expert provider designs solutions tailored to your specific product characteristics, output goals, and factory constraints, ensuring optimal performance. Explore our range of tailored packaging solutions here.
✓ Regulatory Guidance: Navigating the complex web of FDA, EU, and other regional regulations for food and pharma packaging is challenging. An experienced partner brings valuable insight into material compliance and machine design standards.
✓ Long-Term Support & Spare Parts: The relationship doesn’t end at installation. Reliable after-sales service, technical support, and readily available genuine spare parts are crucial for maximizing the lifespan and uptime of your packaging line. Learn more about our commitment to customer care on our Service page.
Seeing is Believing: Real-World Applications
Theoretical benefits are solidified through practical application. For instance, a nutraceutical company struggling with manual filling of protein powder achieved a 300% increase in output and eliminated dosage inconsistencies by implementing an automated multi-lane stick pack line with precision auger fillers. A pharmaceutical supplier of electrolyte powders enhanced product safety and traceability with a GMP-compliant sachet line featuring integrated checkweighers and automated batch coding. You can find more inspiring success stories in our detailed project case studies.
Future-Proofing Your Packaging Investment
Technology evolves rapidly. When selecting a packaging line, consider scalability and adaptability. Can the line handle future product variations? Is the control system capable of integrating with Industrial Internet of Things (IIoT) platforms for predictive maintenance and smarter production analytics? Partnering with an innovative provider ensures your investment remains relevant and competitive for years to come.
Choosing the right industrial packaging line solution is a pivotal step toward securing operational excellence, ensuring product quality, and building a resilient brand in the food, pharma, and health product industries. It requires a partner with deep technical expertise, a proven track record, and a commitment to your long-term success. For a comprehensive overview of our capabilities and company ethos, we invite you to visit our official homepage.
Frequently Asked Questions (FAQs)
1. What is a “turnkey” packaging line solution?
A turnkey solution means the provider delivers a complete, ready-to-operate system. This includes design, manufacturing, installation, commissioning, and training. You receive the keys to a fully integrated line that can start production upon handover, eliminating the need to coordinate multiple vendors.
2. How do you ensure the packaging line meets GMP or FDA regulations?
We design machines with regulatory compliance in mind. This includes using approved materials (e.g., 304/316 stainless steel), designing for easy cleaning and sanitation, minimizing dust generation, and incorporating features for traceability. Our team stays updated on global standards to guide material and design choices.
3. Can one packaging line handle different product types or formats?
Many lines are designed with flexibility. With changeover parts and adjustable settings, a single line can often run different sizes of sachets or stick packs. However, switching between vastly different product forms (e.g., powder to liquid) typically requires significant reconfiguration or dedicated lines. We assess your product portfolio during planning to recommend the most efficient setup.
4. What kind of after-sales support and warranty do you offer?
We provide a comprehensive warranty on all our machinery. Our support includes remote technical assistance, on-site service engineers, and a readily available inventory of genuine spare parts to minimize downtime. Detailed operational manuals and training are part of every project delivery.
5. How long does it take from order to operational installation?
The timeline varies based on the complexity and customization of the line. Standard lines may be delivered in 60-90 days, while highly customized, large-scale turnkey projects can take 4-6 months or more. We provide a detailed project schedule upfront after the initial technical review. For any further specific questions, please don’t hesitate to contact our team directly.