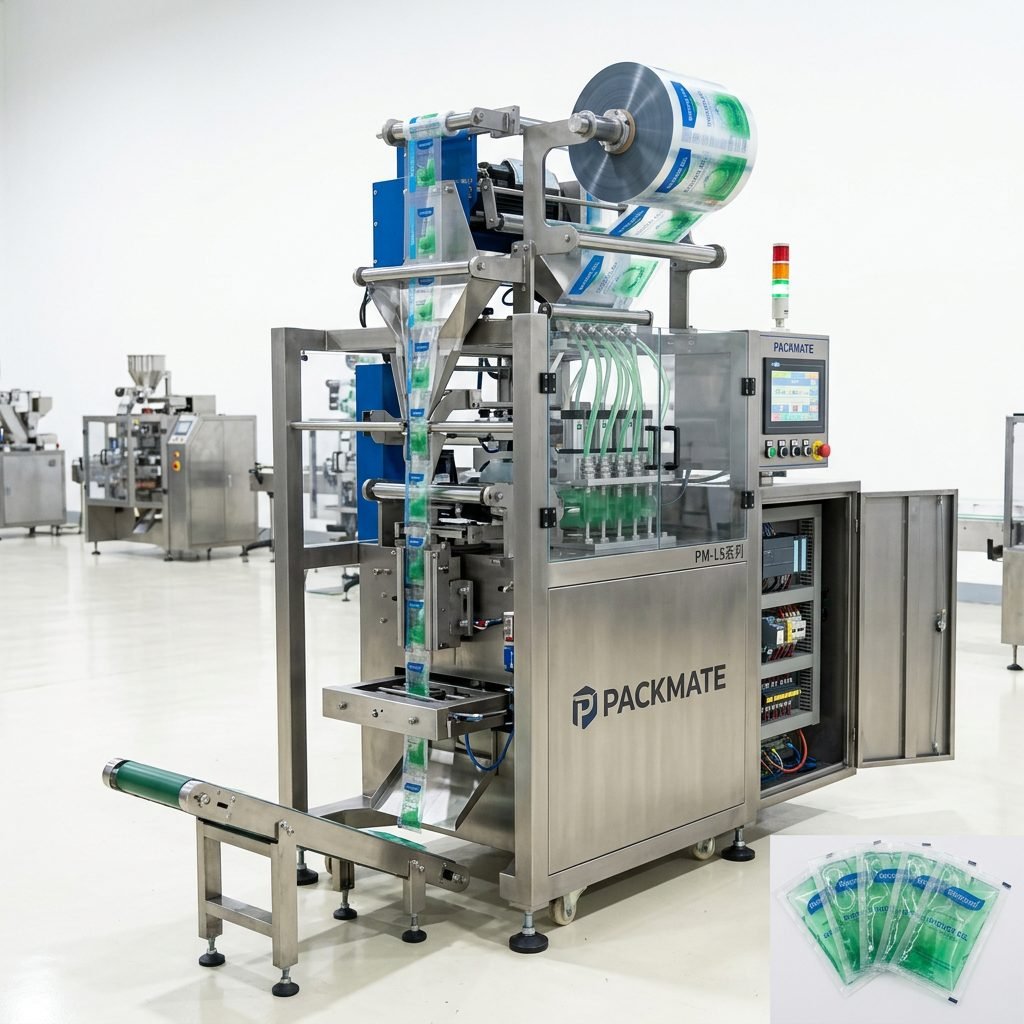
In the high-stakes worlds of food and pharmaceutical manufacturing, the margin for error is zero. Product safety, regulatory compliance, and brand reputation hinge on flawless production. Traditional manual inspection methods are no longer sufficient to meet the demands of speed, volume, and precision. This is where Vision Inspection Packaging Line Solutions emerge as the transformative force, driving faster, error-free production and setting new standards for operational excellence.
The Critical Role of Vision Inspection in Modern Packaging
Vision inspection systems are intelligent, camera-based technologies integrated into packaging lines to perform automated, non-contact quality checks at high speeds. They act as the digital “eyes” of the production floor, scrutinizing every product and package with relentless accuracy that far surpasses human capability. For industries where contamination, incorrect labeling, or seal defects can have severe consequences, these systems are not just an upgrade—they are an essential component of a robust packaging solution.
Core Inspection Capabilities:
- Fill Level Verification: Ensures every sachet, stick pack, or bottle contains the precise amount of product, preventing underfills that cheat consumers and overfills that erode profits.
- Label & Print Inspection: Checks for correct labels, legible batch codes, expiration dates, barcodes, and any printing errors or smudges.
- Package Integrity & Seal Inspection: Detects faulty seals, wrinkles, tears, or foreign material trapped in seals, which are critical for product shelf-life and safety.
- Product Presence & Placement: Confirms the correct item is in the package and is oriented properly, crucial for kits or multi-component products.
- Contaminant Detection: Identifies foreign objects like metal, glass, plastic, or organic matter within the product or package.
Driving Faster, Error-Free Production: The Tangible Benefits
Integrating a vision system is an investment that pays dividends across the entire operation, directly contributing to the title’s promise of “faster, error-free production.”
1. Unmatched Speed and Throughput
Human inspectors fatigue, leading to slower speeds and inconsistent checks. Vision systems operate 24/7 at the line’s maximum mechanical speed, processing hundreds or thousands of items per minute without a drop in vigilance. This eliminates the bottleneck of manual inspection, allowing your packaging line to achieve its true potential throughput.
2. Near-Zero Defect Escape Rate
The primary goal is “error-free.” Advanced algorithms and high-resolution cameras detect sub-millimeter defects invisible to the naked eye. By removing subjectivity and fatigue, defect escape rates plummet. This drastically reduces the risk of costly recalls, consumer complaints, and regulatory non-compliance, protecting both public health and your brand’s integrity.
3. Comprehensive Data and Traceability
Every inspection is a data point. Modern vision systems log every rejected item, including images and the reason for rejection. This creates an invaluable audit trail for quality control, provides data for process optimization (e.g., identifying a recurring seal problem on a specific machine), and supports compliance with stringent traceability regulations in the pharma and food sectors.
📈 Operational Efficiency Gains:
Beyond catching defects, vision inspection streamlines operations. It reduces waste from overfilling, minimizes material usage, and cuts labor costs associated with manual sorting and inspection. The return on investment is often realized through reduced waste, lower liability, and higher overall equipment effectiveness (OEE).
Tailored Solutions for Food & Pharma: Not a One-Size-Fits-All Approach
The application of vision technology must be tailored to the unique challenges of each industry.
For Pharmaceutical & Nutraceutical Production
Here, compliance is paramount. Vision systems ensure 100% inspection of critical parameters:
→ Blister Pack Inspection: Verifying pill count, color, shape, and broken tablets in each blister cavity.
→ Vial & Ampoule Inspection: Checking for cracks, fill level, particulate matter, and correct labeling.
→ Serialization & Aggregation: Reading and verifying unique serial codes on packages and bundles to combat counterfeiting, a key part of track-and-trace mandates. Implementing such a system requires a partner with deep regulatory understanding, like the expertise demonstrated in our industry case studies.
For Food & Beverage Packaging
Speed, variety, and consumer appeal are key. Vision systems adapt to:
→ Flexible Packaging: Inspecting printed dates and codes on fast-moving snack bags, coffee pouches, or frozen food packs.
→ Bottling Lines: Ensuring cap alignment, label placement, and fill level in beverages and sauces.
→ Ready-to-Eat Meals: Verifying component presence and placement in tray-sealing applications.
Implementing a Vision Inspection Solution: A Strategic Partnership
Successfully integrating vision inspection is more than just buying hardware. It requires a strategic partnership with a solution provider who understands your entire packaging process. A provider like Packmate (GuangDong) Co., Ltd. brings over 30 years of experience in designing turnkey packaging lines. This holistic approach ensures the vision system is not an afterthought but is seamlessly engineered into the line from the start, with proper lighting, mounting, and synchronization with other machines like fillers and sealers.
The provider’s role extends to customization, training, and ongoing support services. They configure inspection parameters for your specific products, train your staff on operation and basic troubleshooting, and offer remote diagnostics to minimize downtime. This partnership turns a complex technology into a reliable, day-to-day asset for your production team.
Conclusion: The Future of Packaging Quality Assurance
Vision Inspection Packaging Line Solutions represent the definitive move towards intelligent, data-driven manufacturing. They are the cornerstone of achieving truly faster and error-free production in the food and pharma sectors. By automating the critical task of quality assurance, they empower manufacturers to safeguard consumers, ensure compliance, protect their brands, and unlock new levels of efficiency and profitability. In an era where quality cannot be compromised, machine vision is the clear-sighted path forward.
Frequently Asked Questions (FAQs)
1. How does a vision inspection system handle different product types or packaging changes?
Modern systems are highly flexible. They use recipe-based software where inspection parameters (tolerances, regions of interest, etc.) are saved for each product SKU. When changing over, the operator simply loads the corresponding recipe from the HMI, and the system adjusts automatically, minimizing changeover time.
2. What is the typical Return on Investment (ROI) for implementing such a system?
ROI is calculated through cost savings from reduced waste, lower labor for manual inspection, avoided recall costs, and increased throughput. Many facilities see a full ROI within 12-24 months. The exact timeframe depends on production volume, the cost of defects, and line speed improvements.
3. Can vision inspection systems be retrofitted onto existing packaging lines?
Absolutely. While integration is smoothest during new line design, reputable providers specialize in retrofitting solutions. They engineer custom mounting solutions and ensure proper integration with the line’s PLC for synchronization and rejection mechanisms, breathing new life and capability into existing equipment.
4. How reliable are these systems in harsh production environments (dust, vibration, moisture)?
Industrial-grade vision systems are built for tough conditions. They feature IP-rated enclosures for cameras and lights to resist dust and moisture, ruggedized mounting hardware to withstand vibration, and specialized lighting techniques to overcome ambient light interference, ensuring consistent performance.
5. What kind of support and maintenance do vision inspection systems require?
Maintenance is generally minimal: keeping camera lenses and light covers clean. The key is having reliable support from your provider for software updates, parameter optimization for new products, and rapid technical assistance. Choosing a partner with a strong global service network is crucial for ongoing operational success.