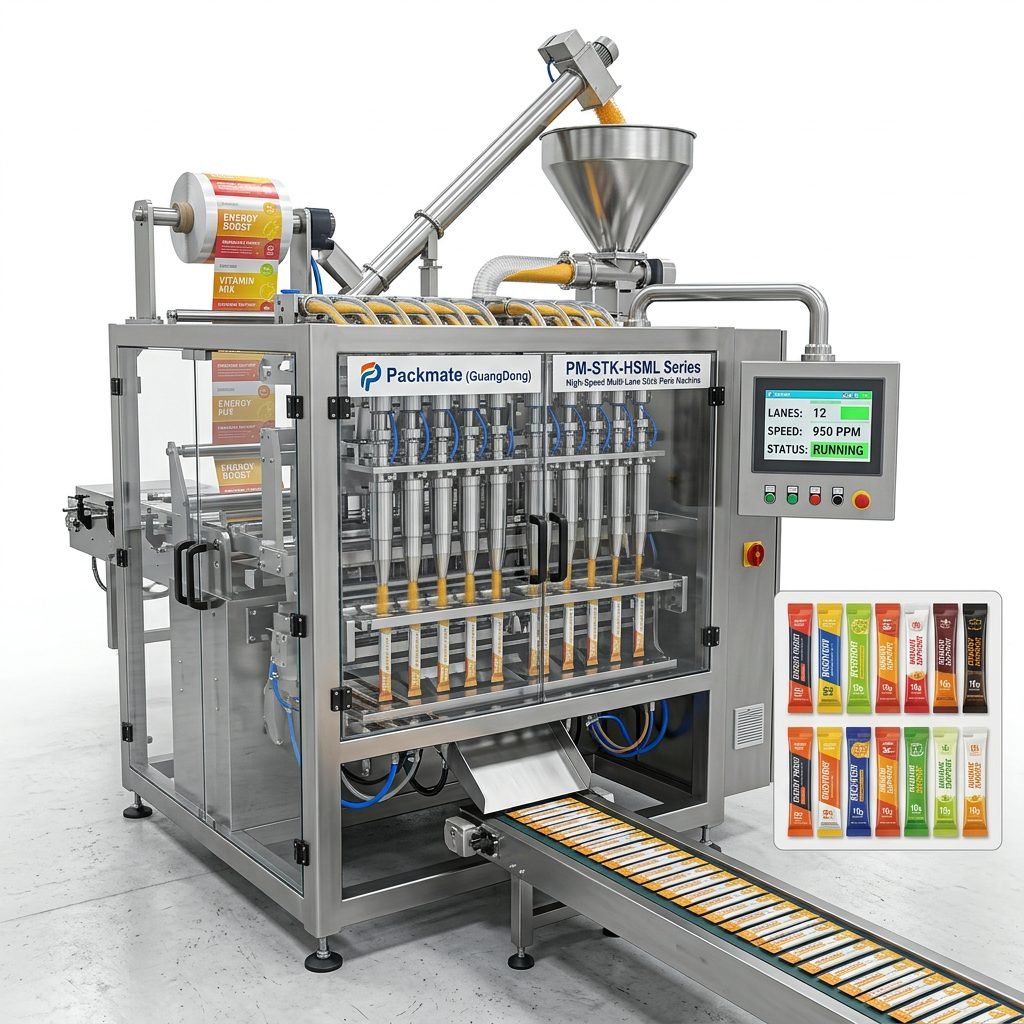
In today’s fast-paced and highly regulated industries, the efficiency, safety, and integrity of your packaging line are not just operational concerns—they are critical pillars of your brand’s success and consumer trust. For manufacturers in the food, pharmaceutical, and health product sectors, the challenge is multifaceted: achieving blistering speed and output while maintaining impeccable hygiene standards, ensuring product protection, and navigating complex compliance landscapes. This is where the concept of a turnkey intelligent packaging solution becomes a transformative investment, moving beyond individual machines to a seamlessly integrated, smart production ecosystem.
The Core of Modern Production: Beyond the Machine
A packaging line is the central nervous system of your production floor. It’s a synchronized orchestra of machines, each performing a specific task—filling, sealing, coding, cartoning—in perfect harmony. The shift from standalone equipment to a fully integrated, turnkey line represents a leap in operational philosophy. It means entrusting the entire process, from design and installation to commissioning and training, to a single, expert partner. This holistic approach eliminates compatibility issues, reduces downtime, and ensures that every component is optimized for the specific product, whether it’s a sensitive probiotic powder, a viscous nutritional syrup, or delicate herbal tea granules.
Why Intelligence is Non-Negotiable
Intelligence in packaging is no longer a luxury. It’s embedded through IoT sensors, programmable logic controllers (PLCs), and sophisticated human-machine interfaces (HMIs). An intelligent line provides:
- Real-time Monitoring & OEE Tracking: Gain instant visibility into equipment effectiveness, production rates, and potential bottlenecks.
- Predictive Maintenance Alerts: Systems analyze performance data to forecast maintenance needs, preventing unexpected breakdowns.
- Precision & Consistency: Automated weight checkers and vision inspection systems guarantee every sachet or stick pack meets exact weight and quality specifications, crucial for pharmaceutical compliance.
- Data-Driven Decision Making: Harvest production data to optimize workflows, reduce waste, and improve overall planning.
Tailored Solutions for Critical Industries
The one-size-fits-all approach is obsolete. Each sector demands unique configurations and adherence to stringent standards.
Food & Beverage Packaging
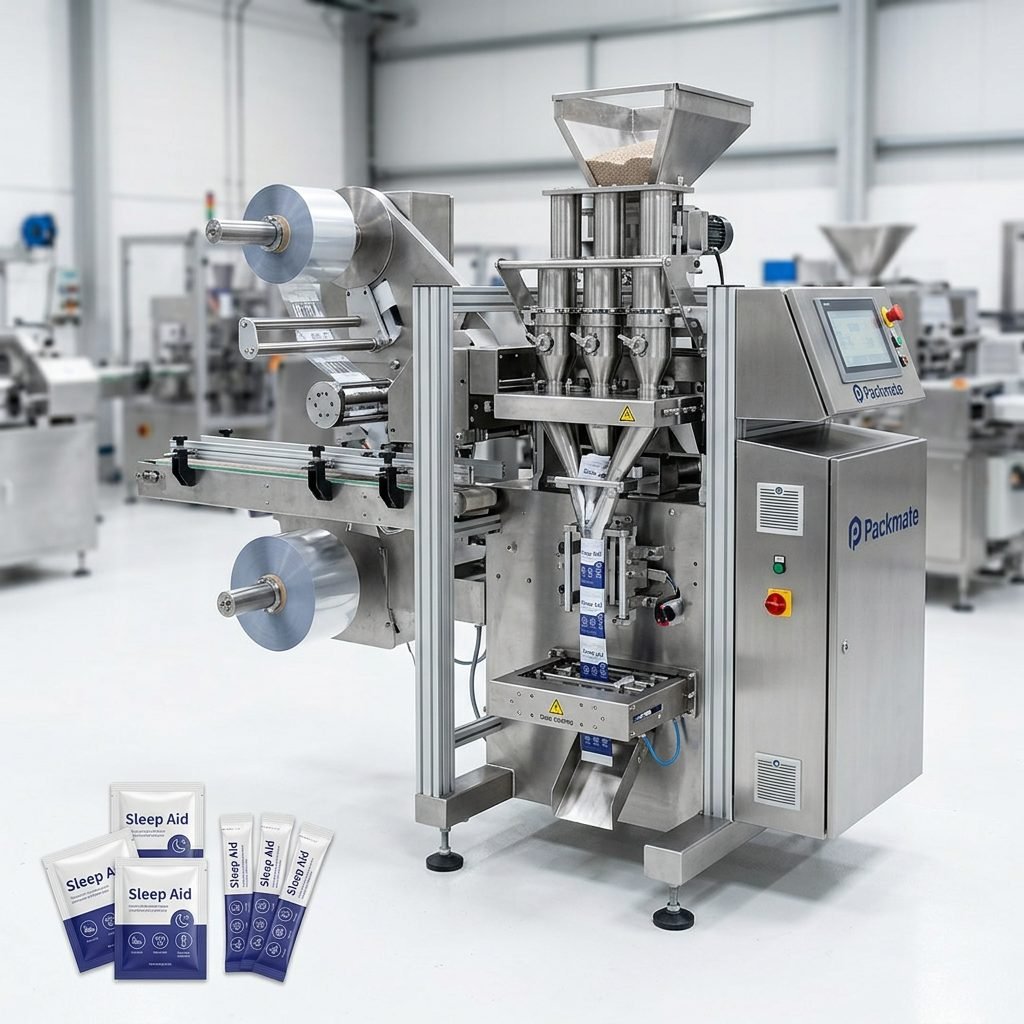
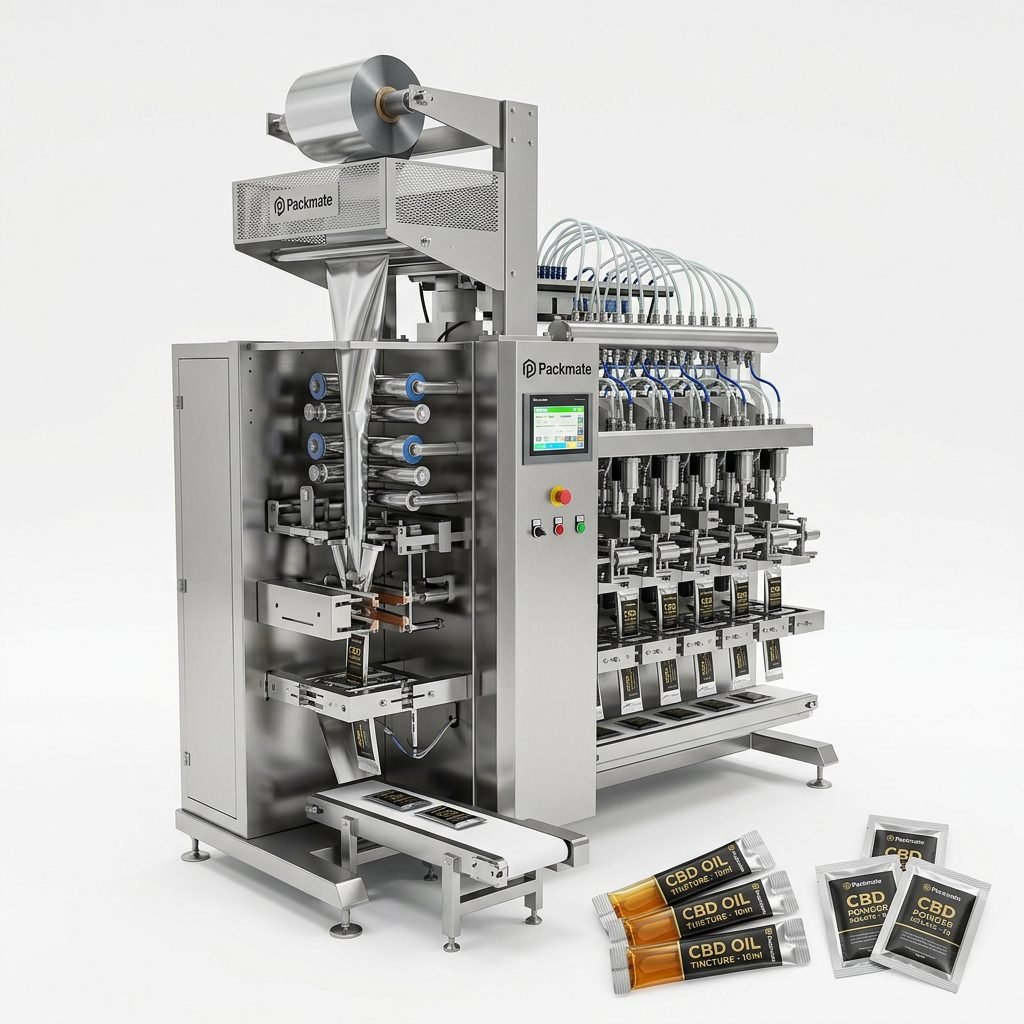
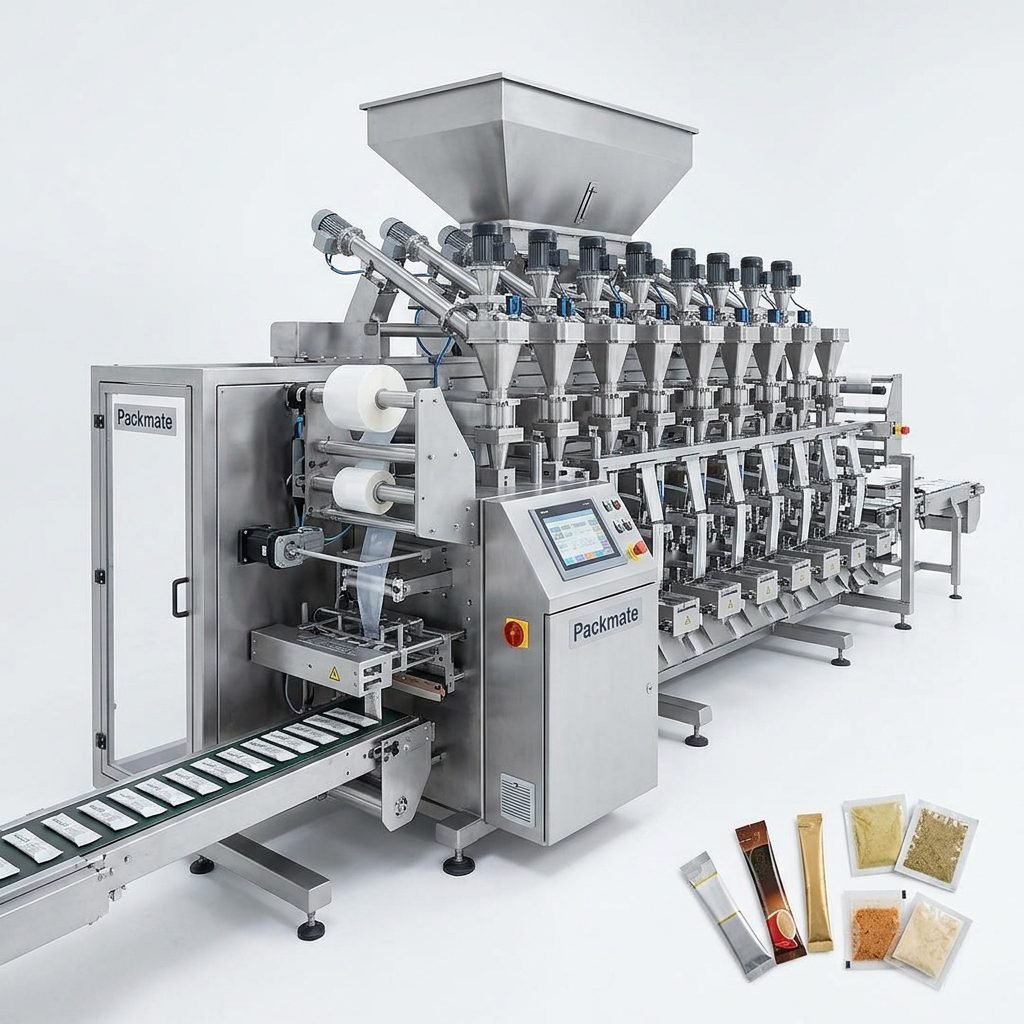
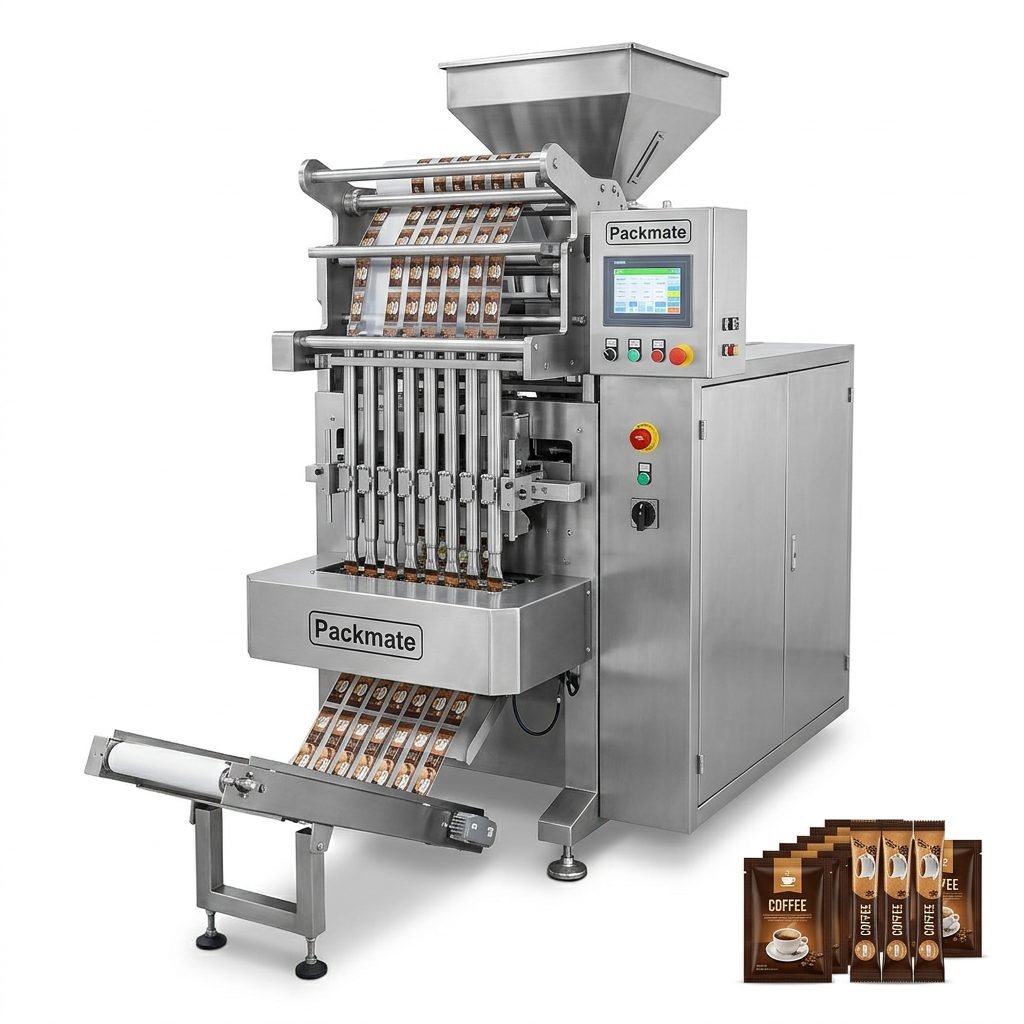
Here, speed meets freshness. Lines must handle diverse consistencies—from fine coffee powders to oily seasonings—while ensuring airtight seals to prolong shelf life. Solutions often include nitrogen flushing capabilities to prevent oxidation. High-speed multi-lane stick pack machines are ideal for single-serve portions of instant drinks, sauces, or condiments, offering consumers convenience and manufacturers high-volume efficiency.
Pharmaceutical & Nutraceutical Packaging
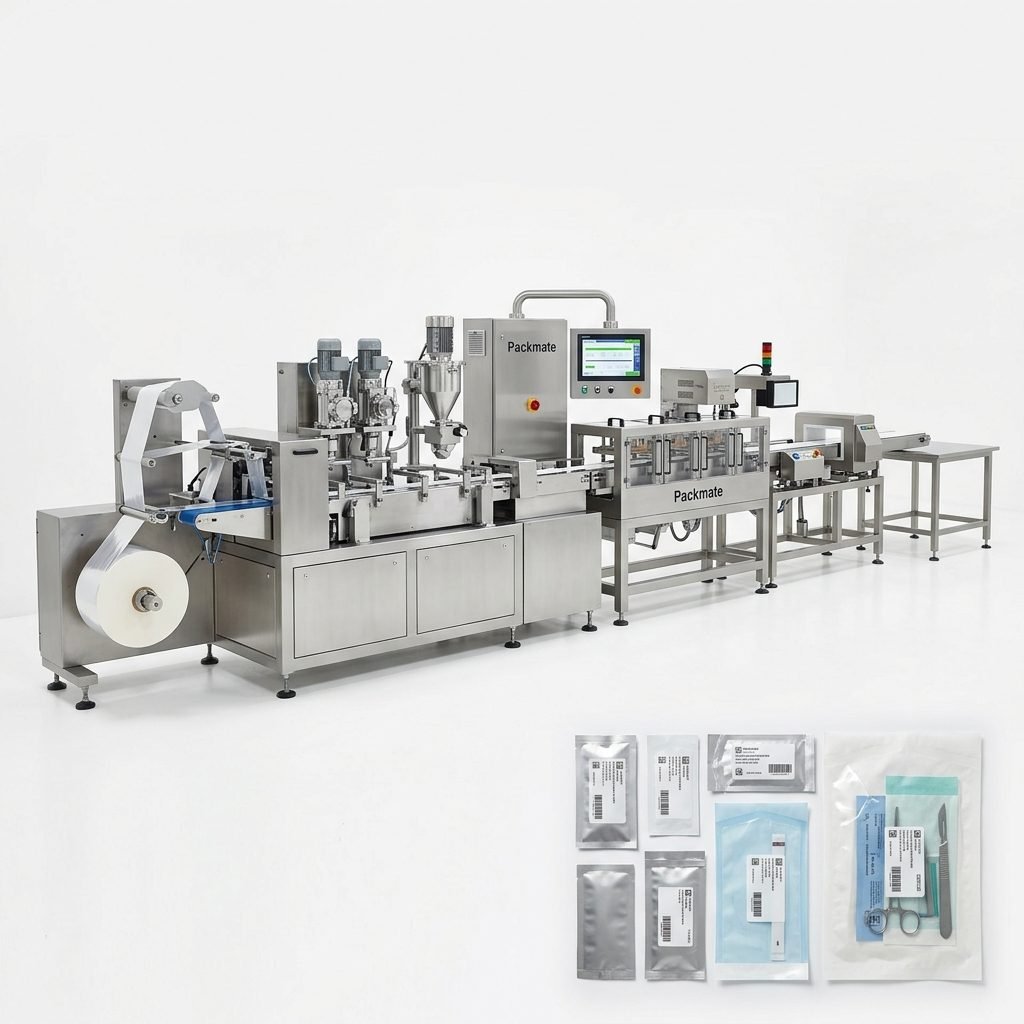
This is the domain of ultimate precision and traceability. Packaging lines must comply with cGMP and other global regulations. Features like clean-design stainless steel surfaces, dust extraction systems, and in-line metal detection are mandatory. Sequential coding and serialization for track-and-trace are integral, often managed through the line’s central intelligence. Whether packaging vitamin capsules in blister packs or powdered supplements in stick packs, the margin for error is zero.
Health & Personal Care Products
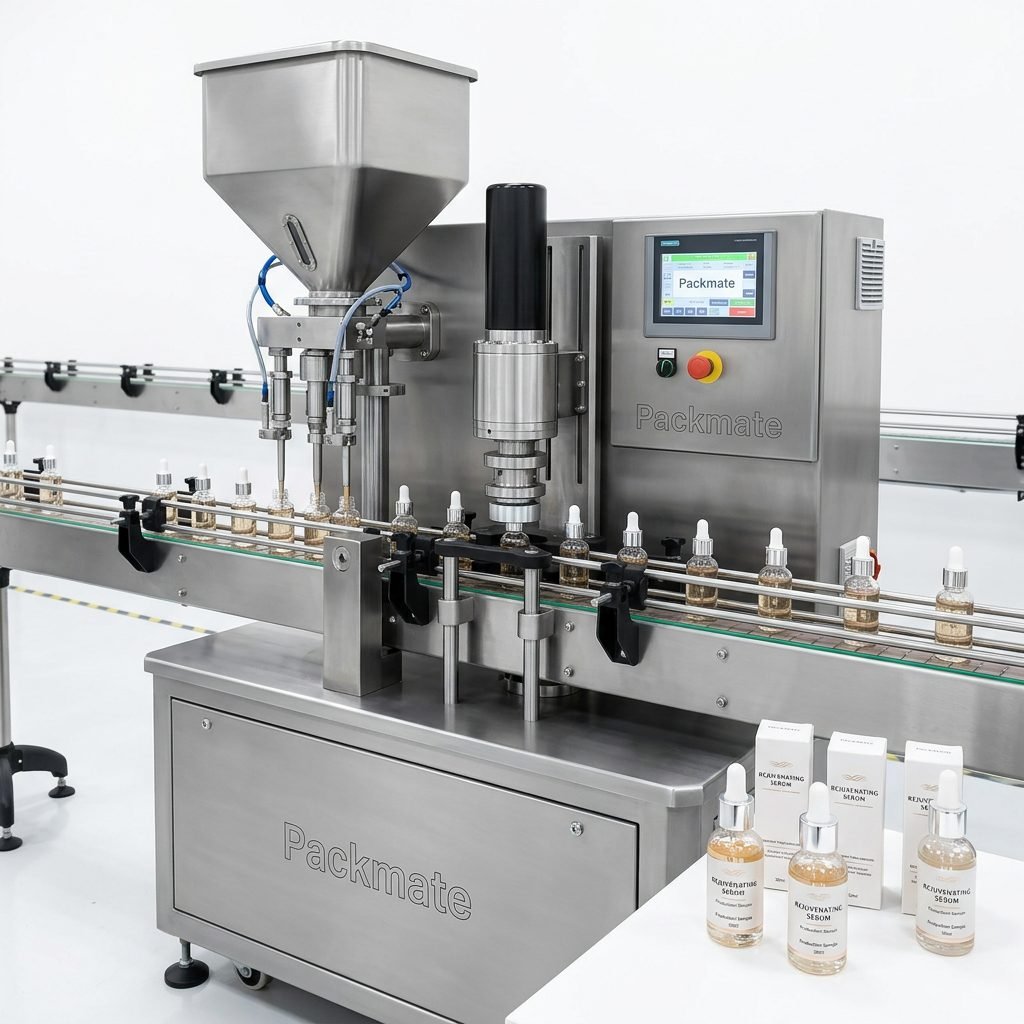
From effervescent tablets to liquid herbal extracts, this sector blends the needs of food and pharma. Aesthetic appeal, precise dosing, and product integrity are key. Versatile form-fill-seal (FFS) machines can create attractive sachets for face masks or single-dose shampoo, while ensuring the sensitive formulas inside are protected from moisture and contamination.
The Packmate Advantage: A Partnership Built on Expertise
Selecting the right partner for your turnkey solution is as crucial as the technology itself. This is where Packmate (GuangDong) Co., Ltd. distinguishes itself. With over 22 years of dedicated development since its formal establishment in 2003, the company embodies the fusion of deep engineering prowess and practical industry insight.
Operating from a sprawling 20,000㎡ modern facility in the heart of China’s manufacturing hub, Packmate’s journey began with a founder’s vision to solve real-world packaging inefficiencies. Today, that vision has scaled into a capability to deliver over 50 machine models, supported by a professional team of more than 125 engineers and technicians. Their approach is consultative: they don’t just sell machines; they analyze your product characteristics, output goals, and factory layout to design a cohesive packaging line solution that functions as a unified whole.
Key Pillars of the Packmate Packaging Line
From Granules to Liquids: A Spectrum of Capabilities
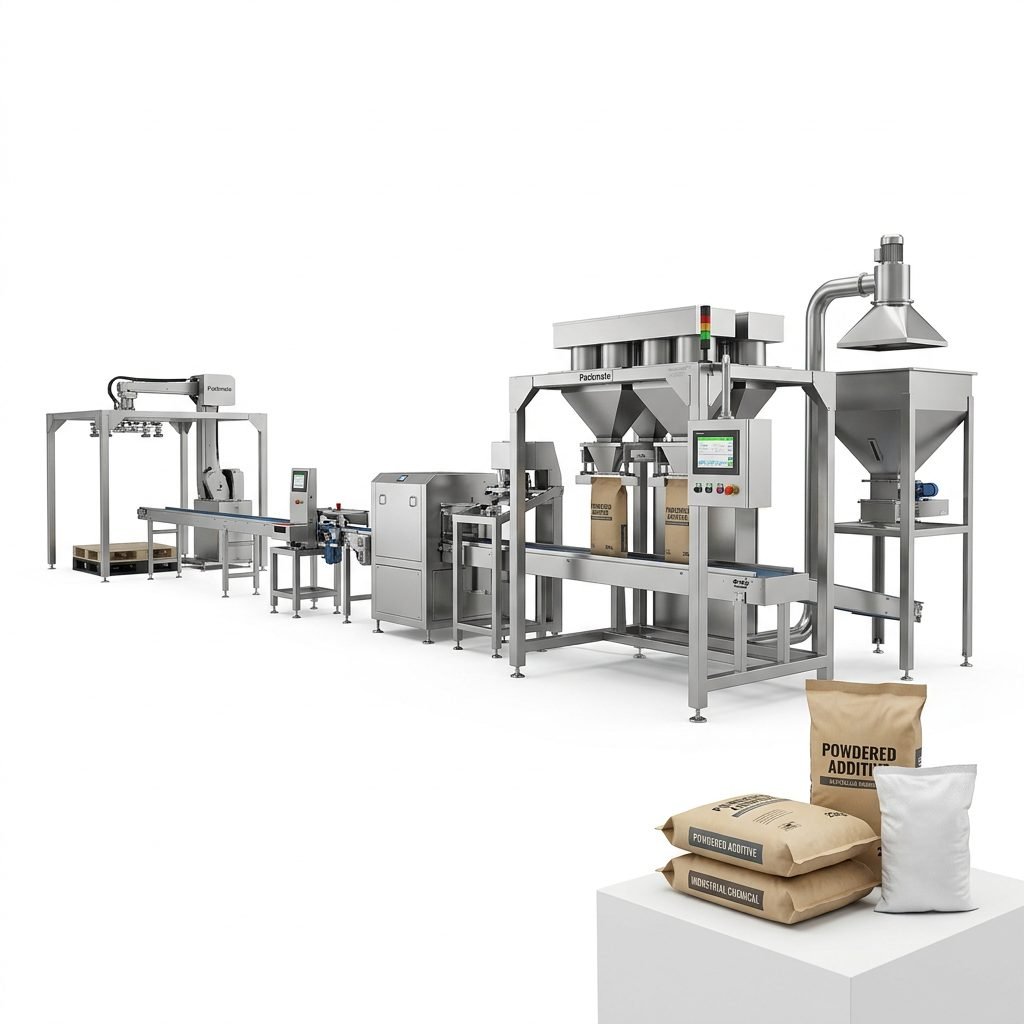
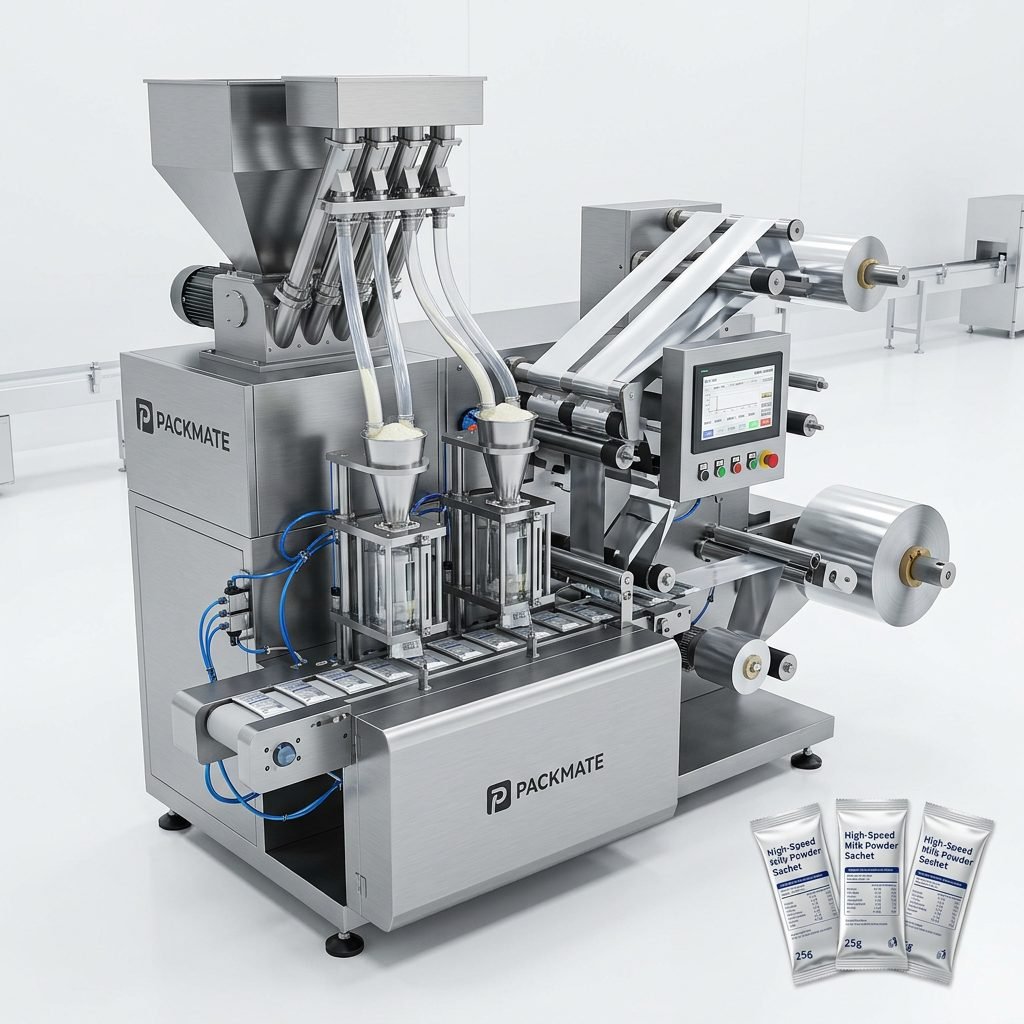
Packmate’s technical portfolio is engineered for versatility. Their multi-lane stick pack machines exemplify high-density output for powdered products, while their advanced sachet packaging lines can handle liquids, pastes, and granules with equal finesse. For larger volumes, such as bulk ingredients or retail-ready bags, their large bag packaging solutions provide robust and reliable performance. This comprehensive range ensures that whether you are a startup in the health food space or an established pharma giant, there is a configured line to meet your exact needs. You can explore their range of successful implementations in their detailed project case studies.
Implementing Your Turnkey Line: The Process
The journey to a new intelligent packaging line is a collaborative partnership.
- Consultation & Needs Analysis: Experts discuss your product, materials, desired output, and facility constraints.
- Line Design & Proposal: A custom layout and machine configuration is proposed, often using CAD simulations.
- Manufacturing & Factory Acceptance Test (FAT): The line is built and tested at Packmate’s facility, where clients can witness its performance.
- Installation & Commissioning: Packmate’s engineers supervise installation on your site, calibrate the system, and run production trials with your actual materials.
- Training & Handover: Comprehensive training for your operators and maintenance staff ensures smooth ownership.
- Ongoing Support: Access to spare parts, remote diagnostics, and technical support through their dedicated service network.
Future-Proofing Your Investment
An intelligent turnkey line is an asset designed to grow with your business. Modular designs allow for future expansion—adding lanes, integrating robotic palletizers, or upgrading software. The focus on connectivity means your line can seamlessly integrate into broader Industry 4.0 and smart factory initiatives, collecting data that drives continuous improvement for years to come.
In conclusion, the modern packaging line is a strategic cornerstone. It is the point where product, brand promise, and consumer experience converge. By investing in a turnkey intelligent solution from an experienced partner like Packmate, manufacturers in the food, pharma, and health sectors secure more than machinery; they secure reliability, compliance, scalability, and a powerful competitive edge in a demanding global marketplace.
Frequently Asked Questions (FAQs)
What does “turnkey” mean in packaging solutions?
A turnkey solution means the supplier handles everything from initial design and engineering to manufacturing, installation, commissioning, and operator training. You receive a fully functional production line ready to “turn the key” and start operations, minimizing your internal project management burden and technical risk.
How do I know if I need a multi-lane stick pack machine vs. a standard sachet machine?
The choice depends on product format, required output speed, and portion size. Multi-lane stick pack machines are typically for dry, free-flowing powders and granules (like instant coffee, protein powder) where ultra-high speed is needed. Sachet machines offer more flexibility in pouch shape and size and can handle liquids, pastes, and granules. A detailed consultation with experts, like those at Packmate, is the best way to determine the optimal technology.
Can your packaging lines meet international pharmaceutical standards (like cGMP)?
Yes. Reputable providers design lines specifically for regulated industries. This includes using 304 or 316 grade stainless steel for contact parts, incorporating easy-clean designs, providing documentation for validation (IQ/OQ/PQ), and integrating features like weight checkers and metal detectors. It’s crucial to discuss your specific compliance requirements early in the design process.
What kind of after-sales support and service can we expect?
Comprehensive support is vital. Look for a partner offering remote diagnostic support, readily available spare parts, on-site service engineers, and periodic maintenance programs. This ensures maximum uptime and long-term reliability for your investment.
How long does it typically take from order to full operation of a new turnkey line?
The timeline varies based on line complexity and customization. Generally, it can range from 3 to 9 months. This period includes detailed engineering, manufacturing, factory testing, shipping, and on-site installation/commissioning. A clear project timeline should be established during the contract phase.
For more detailed answers, visit our dedicated FAQs page.