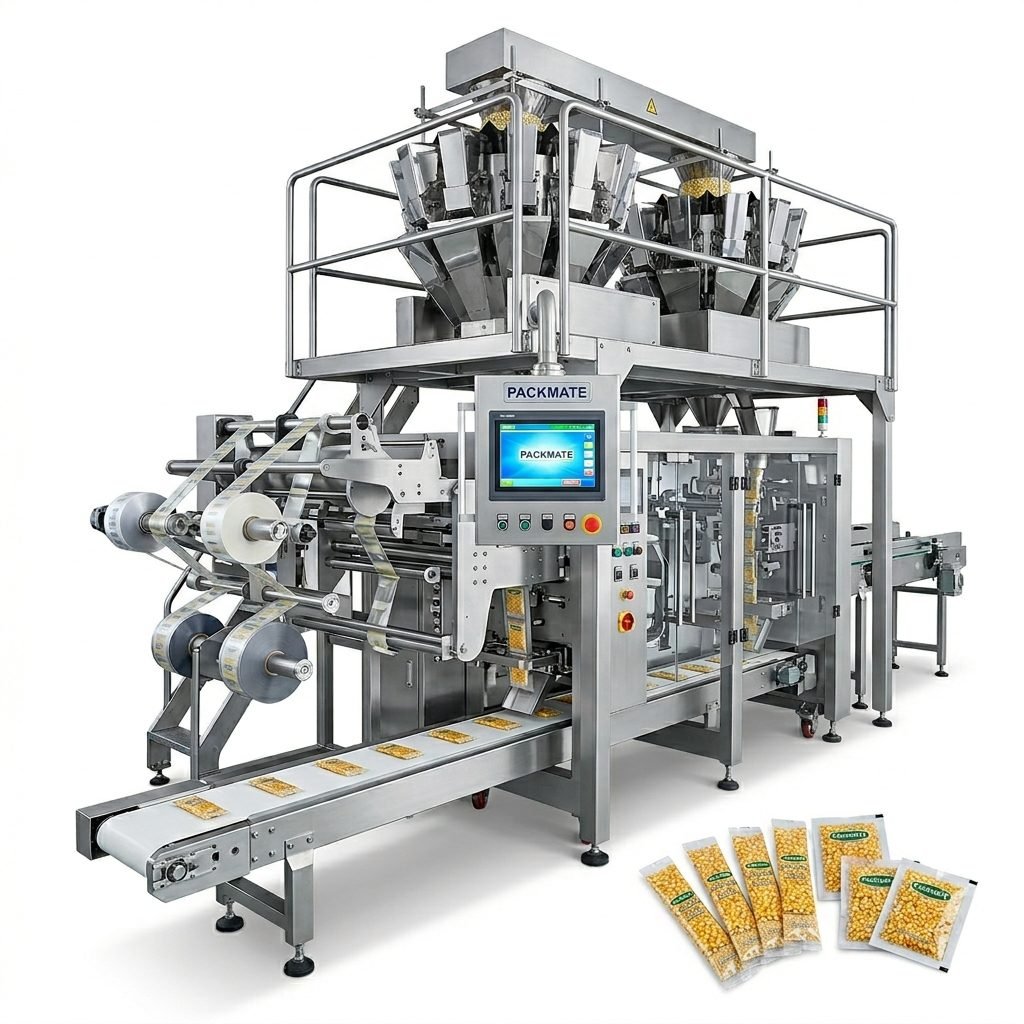
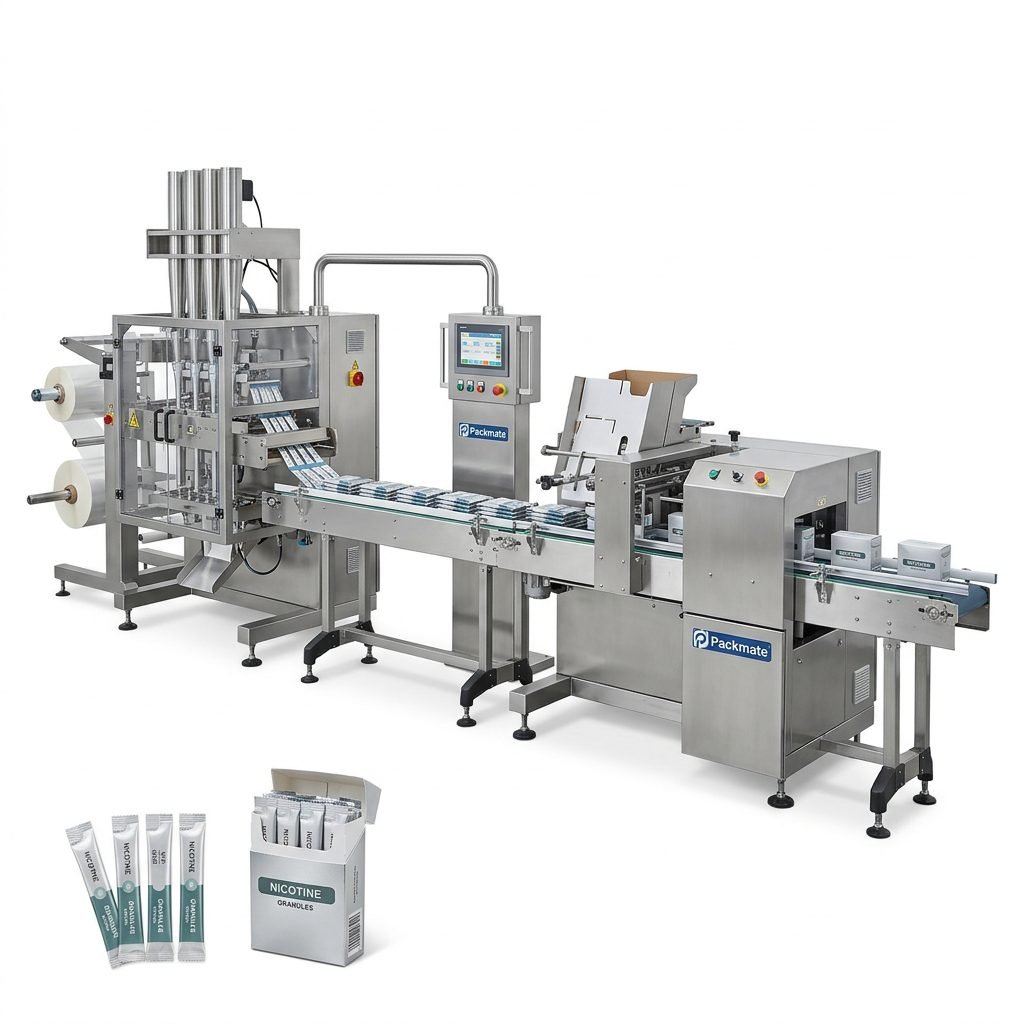
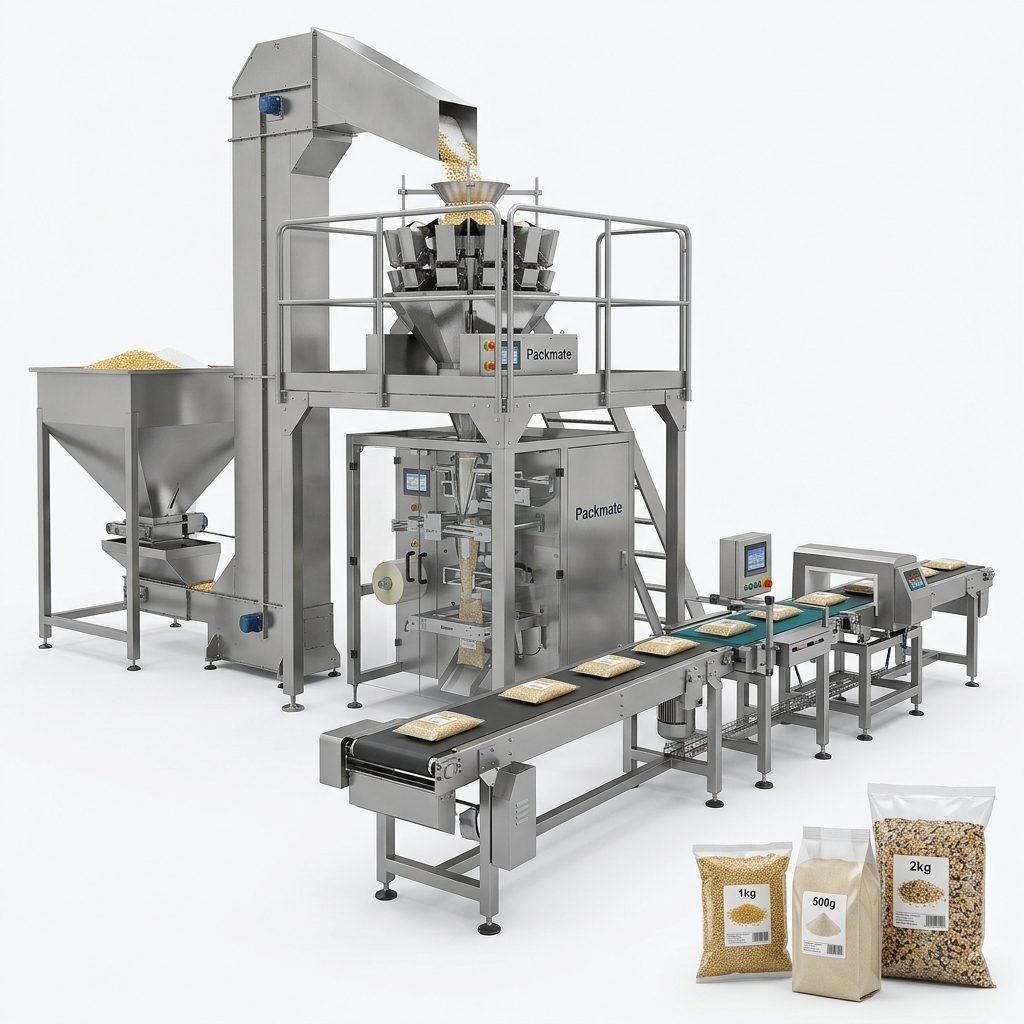
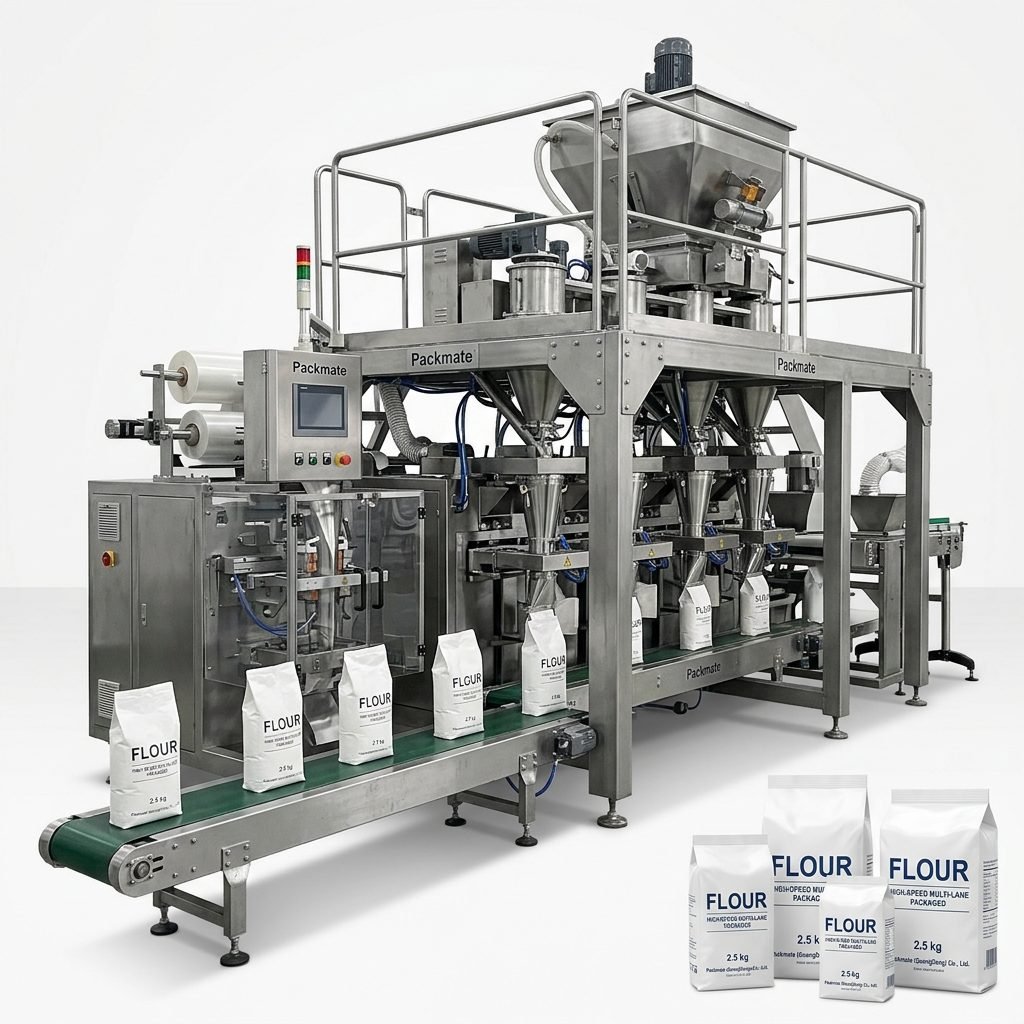
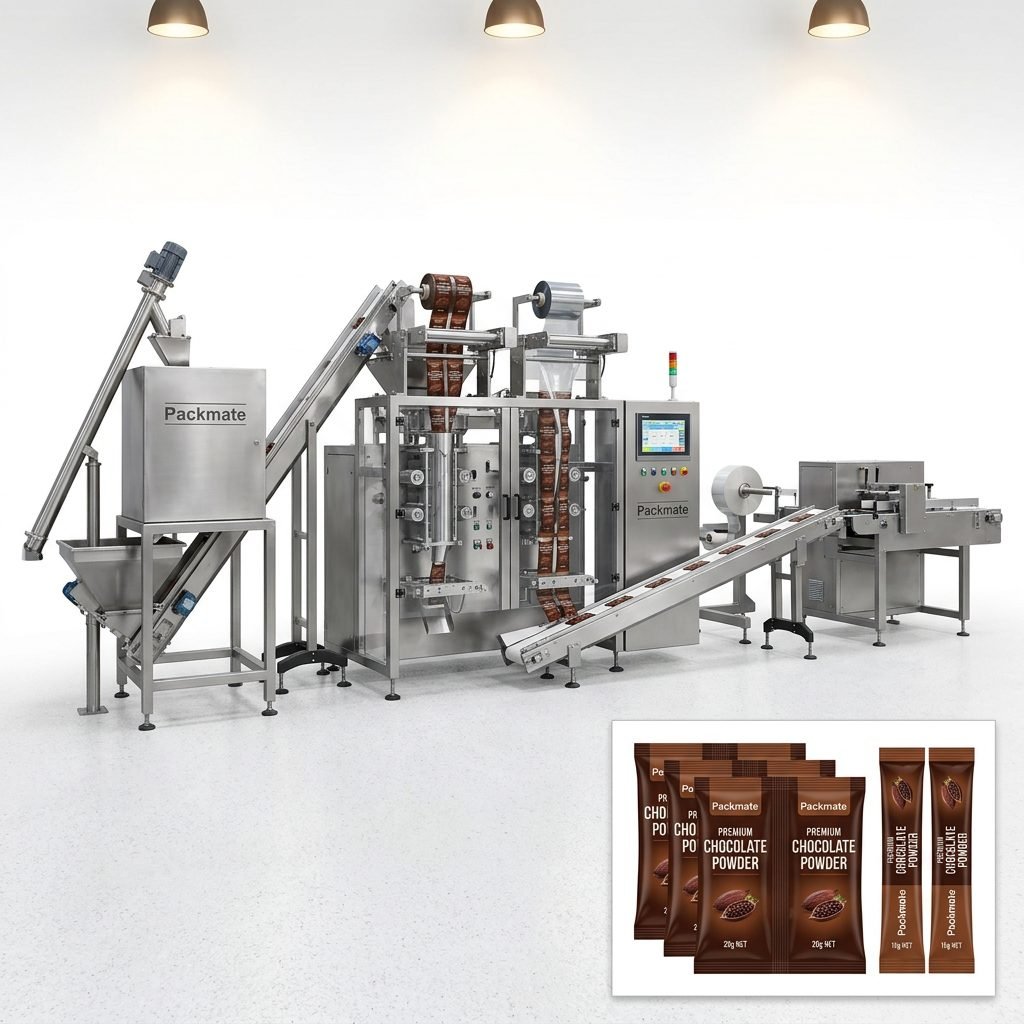
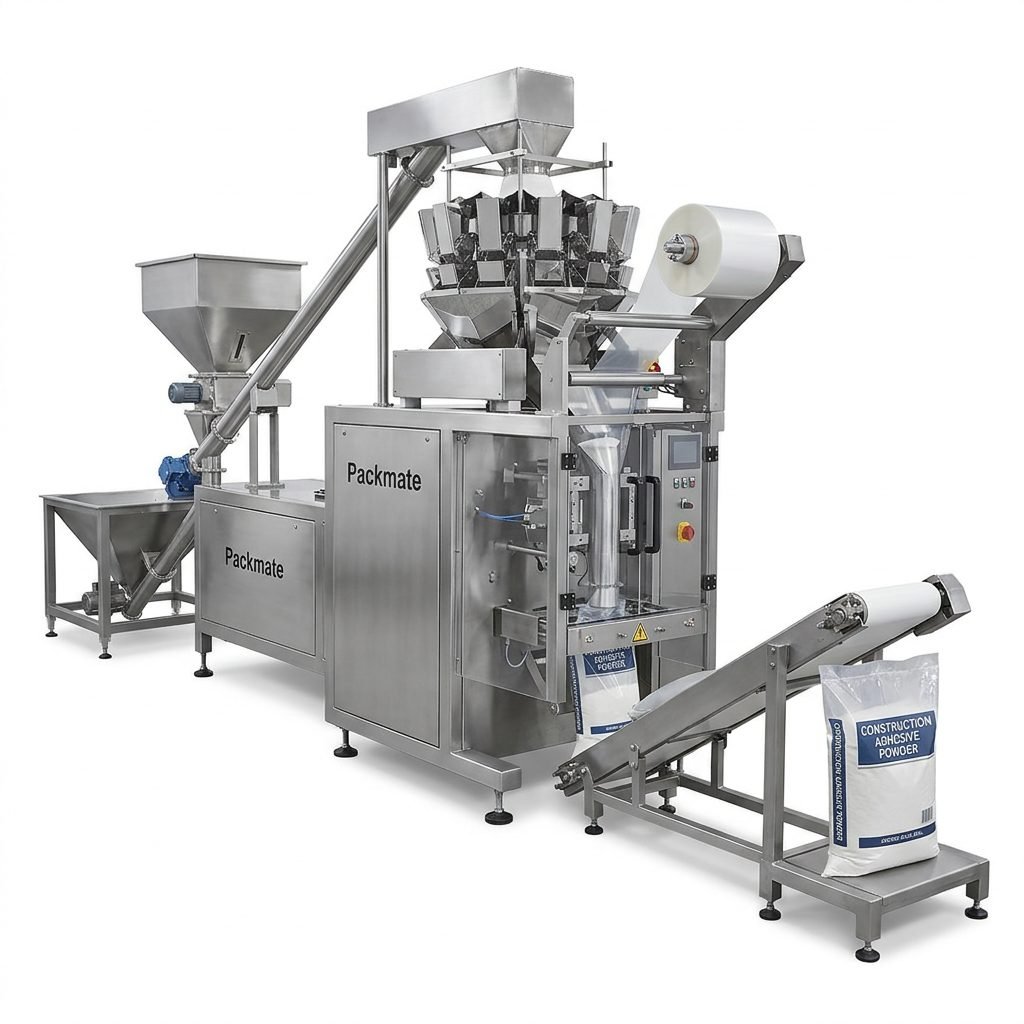
In the highly regulated and competitive landscapes of food, pharmaceutical, and health product manufacturing, the packaging line is far more than a final step—it is a critical component of product integrity, brand reputation, and operational efficiency. Selecting reliable packaging machinery is not merely a procurement decision; it is a strategic investment in the safety of your products and the sustainability of your business. This article explores the essential considerations for choosing robust packaging solutions tailored to these sensitive industries and highlights how a partner like Packmate (GuangDong) Co., Ltd. delivers the reliability demanded by modern production lines.
The Non-Negotiable Demand for Reliability
Why is reliability the paramount criterion? In sectors where consumer health is directly impacted, any failure in the packaging process can have severe consequences. A machine malfunction can lead to:
→ Product Contamination: Compromised seals or improper dosing in pharmaceuticals or supplements can render products unsafe.
→ Production Downtime: Unplanned stops disrupt the entire supply chain, causing significant financial loss.
→ Regulatory Non-Compliance: Inconsistent packaging can violate strict FDA, EMA, or other regional guidelines, risking fines and market recalls.
→ Brand Damage: One incident of packaging failure can erode years of built consumer trust.
Therefore, reliable machinery is defined by consistent performance, minimal unplanned downtime, and the ability to maintain precision under continuous operation. This reliability is engineered through robust design, high-quality components, and rigorous testing protocols.
Key Challenges Across Different Product Forms
Each product type presents unique challenges that packaging machinery must reliably overcome:
For Food Products (Granules, Powders, Liquids)
Hygiene and speed are critical. Machinery must be easy to clean (often requiring CIP/SIP systems), handle varying product viscosities and granule sizes without clogging, and provide high-speed filling to meet large-volume demands. Reliability here means maintaining hygiene standards and output targets day after day.
For Pharmaceutical Products
Precision and traceability are non-negotiable. Machines must deliver exact dosages, often in sterile environments, and integrate with data logging systems for complete batch traceability. Reliability is synonymous with unwavering accuracy and compliance.
For Health & Nutritional Products
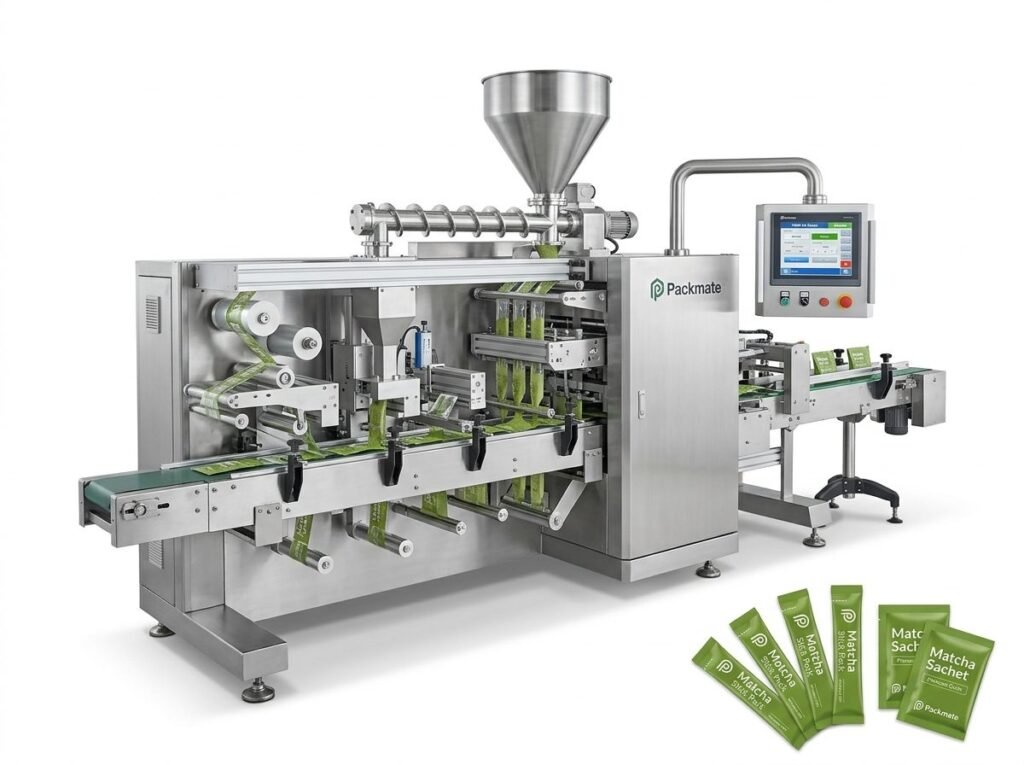
This sector often blends the needs of food and pharma. Packaging must be consumer-friendly (e.g., convenient stick packs or sachets), protect sensitive ingredients from moisture and oxygen, and allow for attractive branding. Reliability ensures product potency and shelf appeal are preserved.
Components of a Reliable Turnkey Solution
True reliability extends beyond a single machine to the entire integrated line. A turnkey solution from a trusted provider encompasses:
- Customized System Design: The line is engineered from the ground up for your specific product, packaging material, and output goals.
- Seamless Integration: All components—from feeding and filling to sealing, coding, and cartoning—work in perfect harmony, eliminating bottlenecks.
- Intelligent Control Systems: Modern PLC and HMI interfaces allow for precise control, easy changeovers, and predictive maintenance alerts.
- Comprehensive Validation & Support: This includes Factory Acceptance Testing (FAT), installation qualification (IQ), operational qualification (OQ), and ongoing technical service.
Exploring a provider’s project portfolio is the best way to assess their capability to deliver such integrated, reliable systems.
The Packmate Advantage: Engineering Reliability for Over Two Decades
With a foundation built over 22+ years, Packmate’s evolution from a specialized workshop to a modern manufacturer with a 20,000㎡ facility is a testament to its focus on reliable engineering. The company’s journey, detailed in its Company Profile, reflects a deep understanding of the market’s evolving needs.
Core Pillars of Packmate’s Reliability:
In-House Manufacturing
Rigorous Testing
Modular Design
Global Support Network
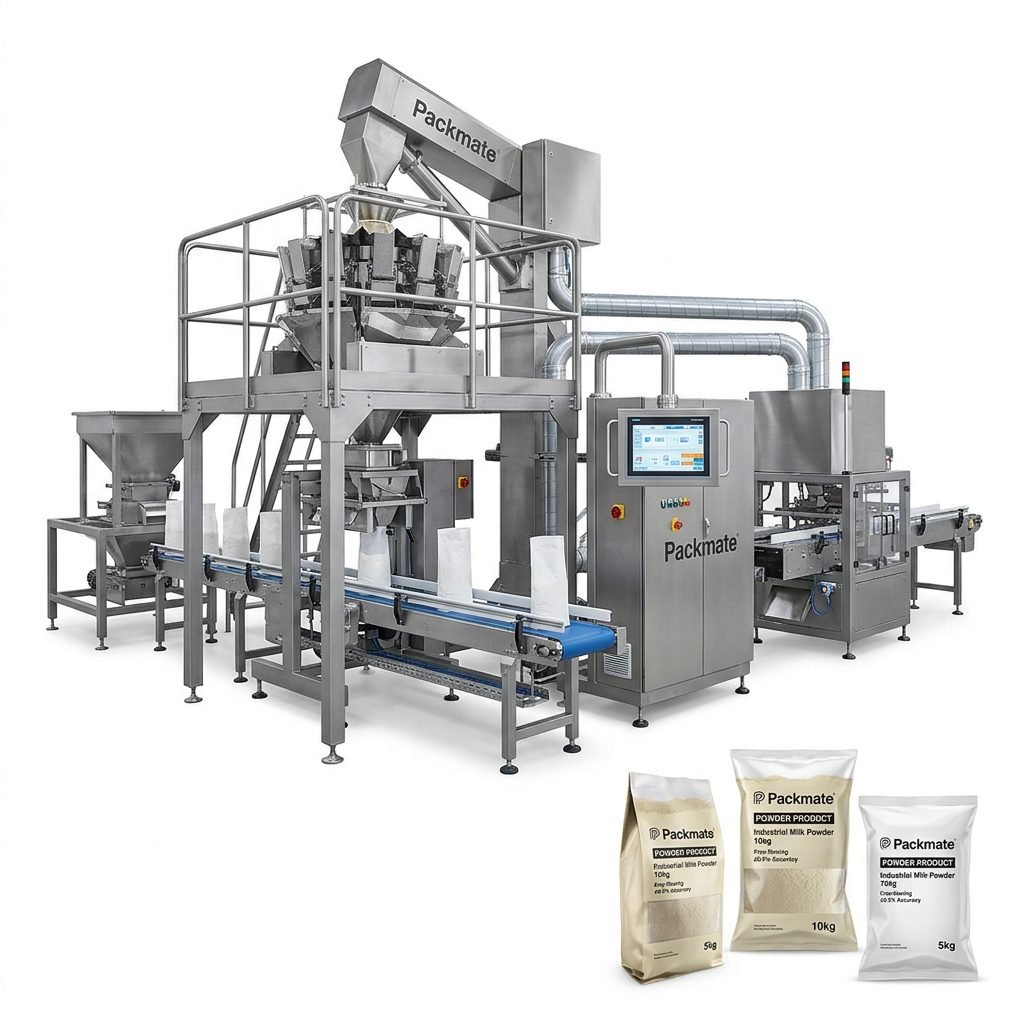
This controlled production process ensures every machine meets stringent quality standards before it reaches the client’s floor. Their expertise spans multi-lane stick pack machines, sachet packaging lines, and large-bag filling systems—all designed for the rigorous demands of food, pharma, and health products.
Future-Proofing Your Investment
Reliability also means adaptability. The best packaging solutions are scalable and can adapt to new products, packaging formats, and increased speeds. When evaluating machinery, consider:
- Modularity: Can the line be easily upgraded or reconfigured?
- Technology Roadmap: Does the supplier invest in R&D for trends like smart factory integration and sustainable packaging?
- Global Compliance: Are machines built to meet international safety and quality standards? Packmate’s various certifications underscore this capability.
Partnering with a forward-thinking provider ensures your investment remains viable and productive for years to come.
In conclusion, reliable packaging machinery is the cornerstone of a successful, compliant, and efficient production line in the food, pharmaceutical, and health product industries. It is an investment that safeguards product quality, protects your brand, and ensures operational continuity. By choosing an experienced partner like Packmate, which offers engineered, turnkey solutions backed by decades of expertise, manufacturers can achieve not just reliability, but a genuine competitive advantage. For a deeper look into specific packaging solutions, visit their dedicated resource pages.
Frequently Asked Questions (FAQs)
Q1: What is the most important factor when choosing packaging machinery for pharmaceutical products?
A: Beyond reliability, the absolute priority is compliance and validation. The machinery must be designed and documented to meet stringent regulatory standards (like FDA 21 CFR Part 11 for data integrity) and must support a full validation protocol (IQ, OQ, PQ) to ensure consistent, traceable performance.
Q2: Can one packaging line handle different product types, such as powders and liquids?
A: While some machines are versatile, highly specialized lines often deliver superior reliability and efficiency. For handling fundamentally different product forms (e.g., dry powder vs. viscous liquid), significant changeover involving different filling systems and cleaning protocols is required. A trusted supplier can design modular lines or recommend the optimal configuration for multi-product facilities.
Q3: How does a turnkey solution differ from buying individual machines?
A: A turnkey solution provides a fully integrated, ready-to-operate system from a single supplier. This eliminates compatibility issues, ensures unified control and service, and provides a single point of accountability. Buying individual machines from different vendors requires you to manage integration, which can lead to downtime and finger-pointing if issues arise.
Q4: What kind of after-sales support should I expect for critical production machinery?
A: Expect comprehensive support including detailed documentation (manuals, schematics), readily available spare parts, remote diagnostic assistance, and on-site technician support. Providers like Packmate often offer training programs for your operators and maintenance staff to ensure long-term, self-sufficient reliability.
Q5: How can I assess the true reliability of a packaging machine supplier?
A: Request and contact references from clients with similar applications. Ask about mean time between failures (MTBF), service response times, and overall satisfaction. Inspect their manufacturing facility if possible, review their quality control processes, and examine their history of innovation and industry participation, such as their presence at international exhibitions.