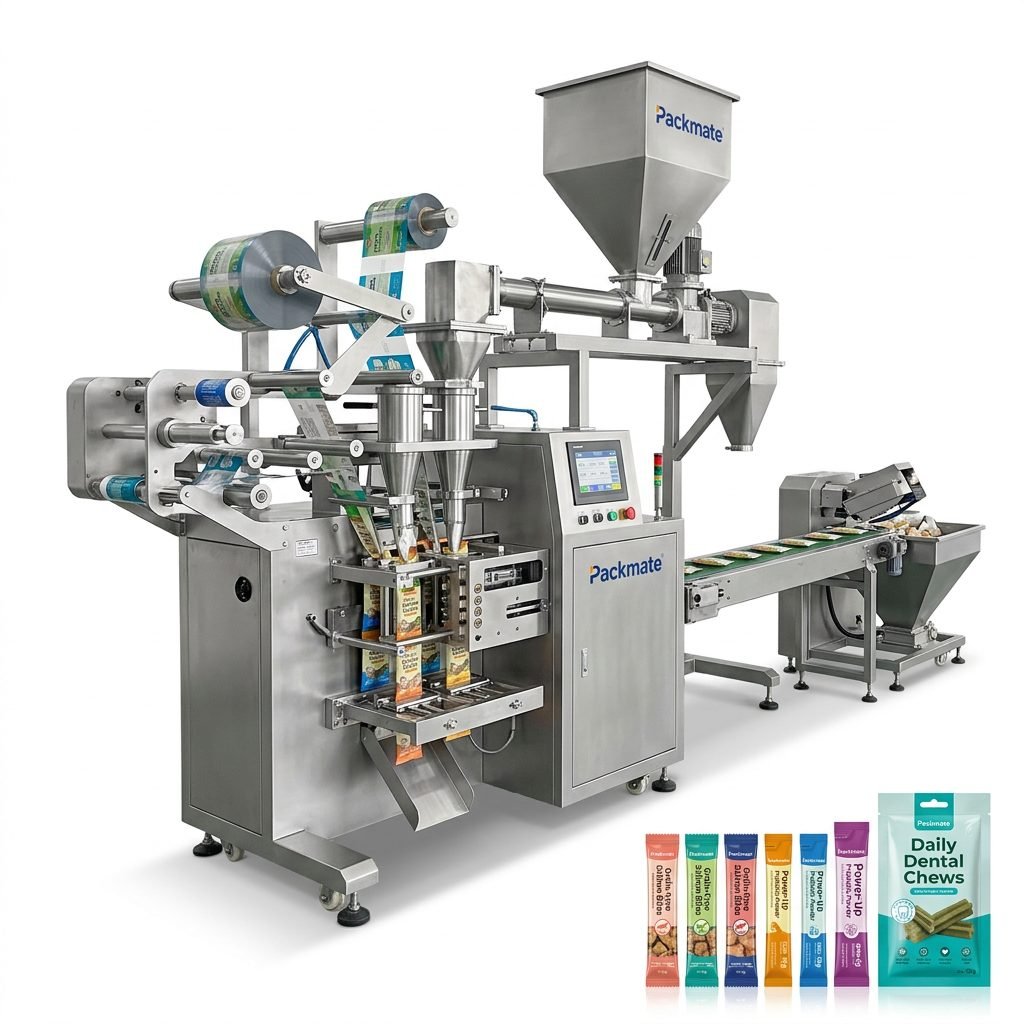
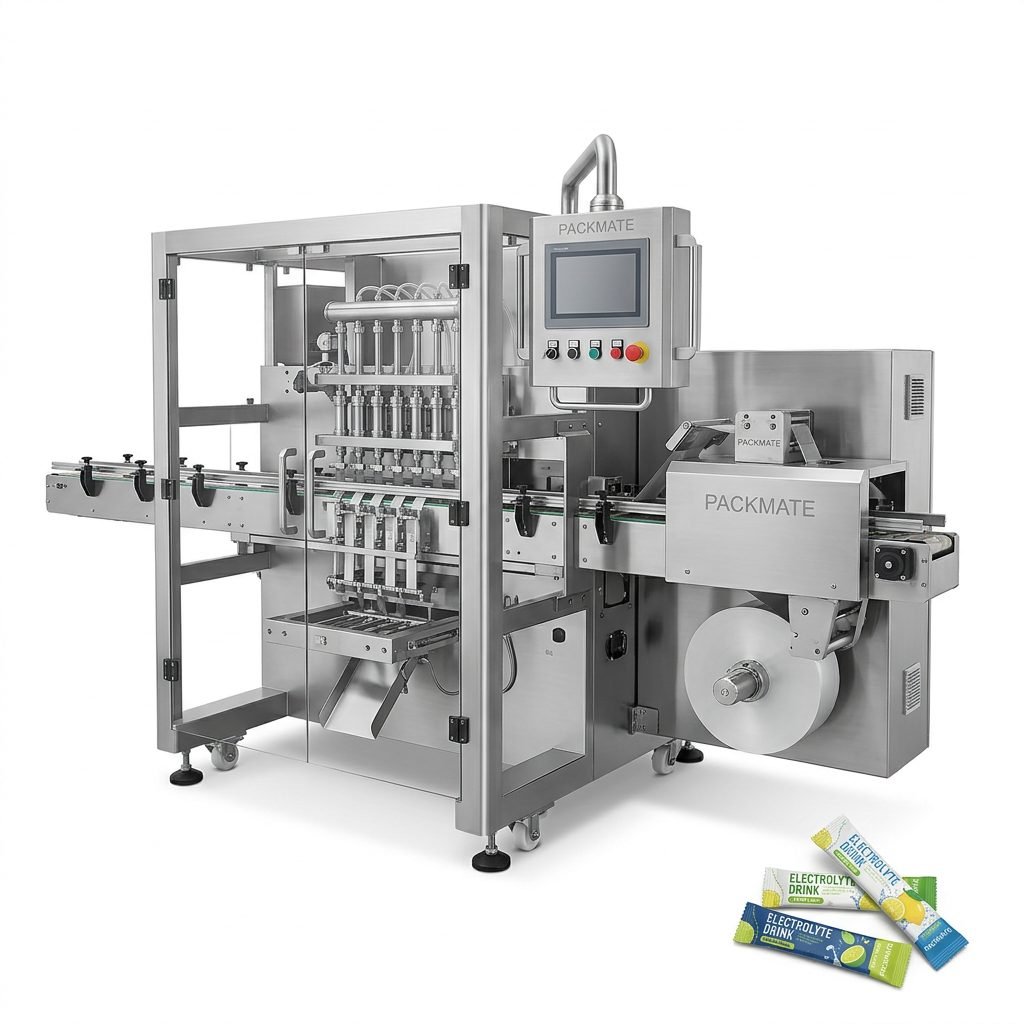
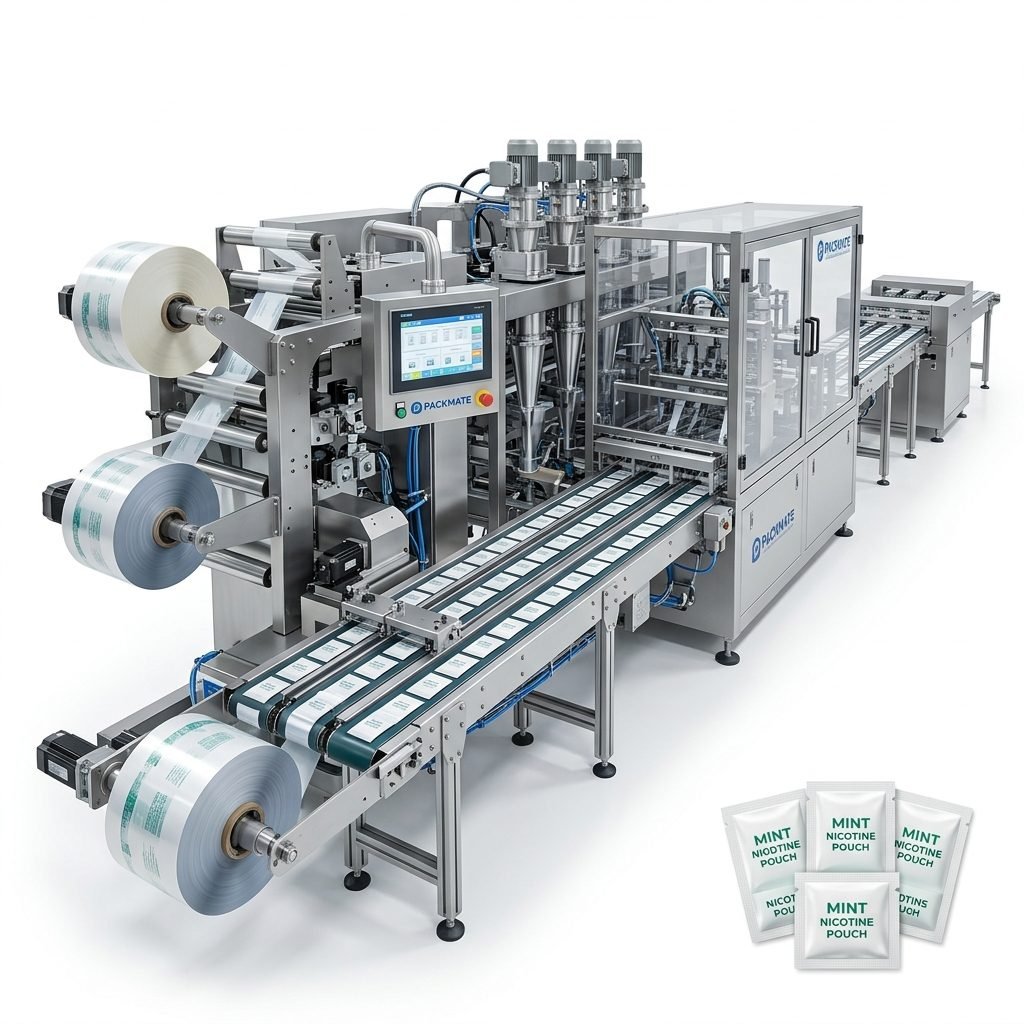
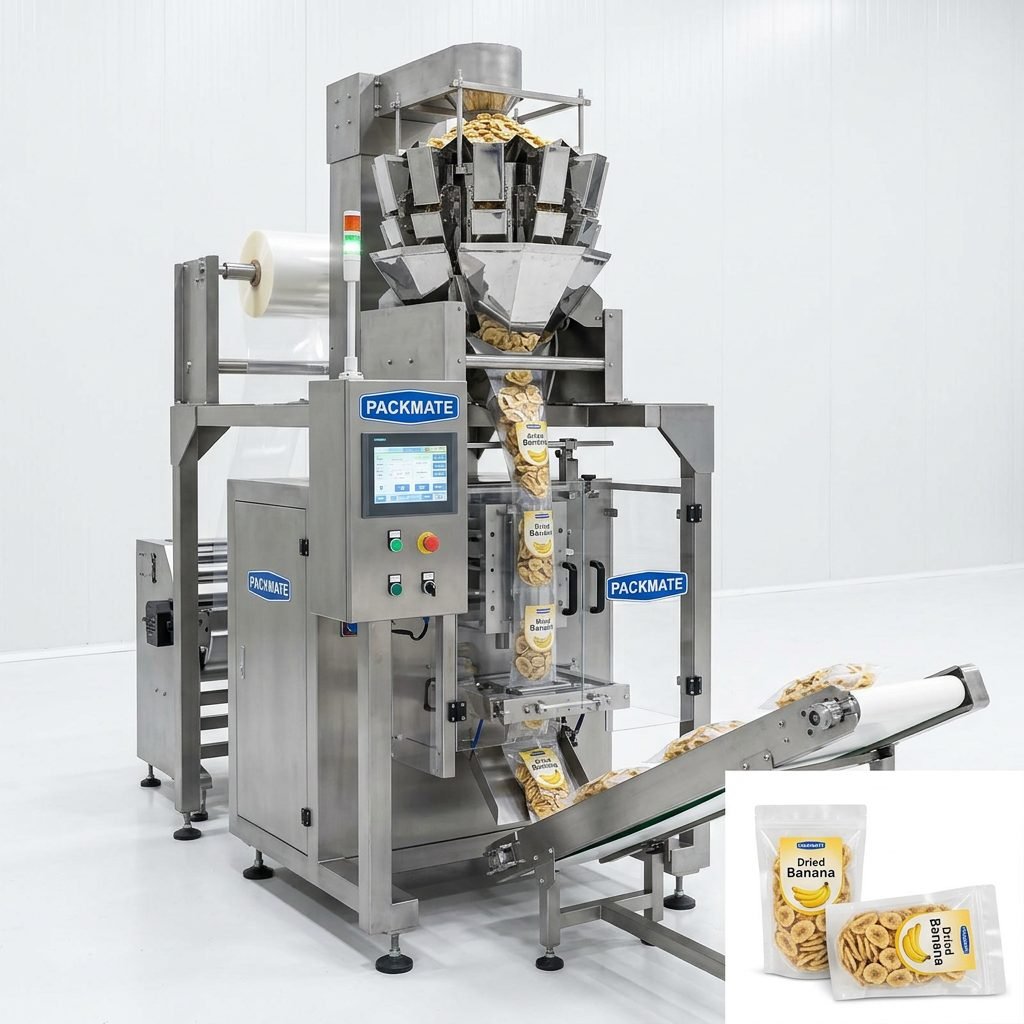
In today’s fast-paced and highly regulated manufacturing landscape, selecting the right packaging line equipment is not just an operational decision—it’s a strategic imperative. For industries where product integrity, safety, and presentation are paramount, such as food, pharmaceuticals, and health products, the packaging line is the final and most critical guardian of quality before a product reaches the consumer. A well-designed, intelligent packaging solution ensures compliance, maximizes efficiency, minimizes waste, and protects brand reputation.
The Critical Role of Specialized Packaging Solutions
The demands placed on packaging machinery vary dramatically across different sectors. What works for a breakfast cereal may be wholly unsuitable for a sterile medical device or a sensitive probiotic supplement. This divergence necessitates specialized equipment solutions tailored to the unique challenges of each industry.
Food Industry: Speed, Hygiene, and Versatility
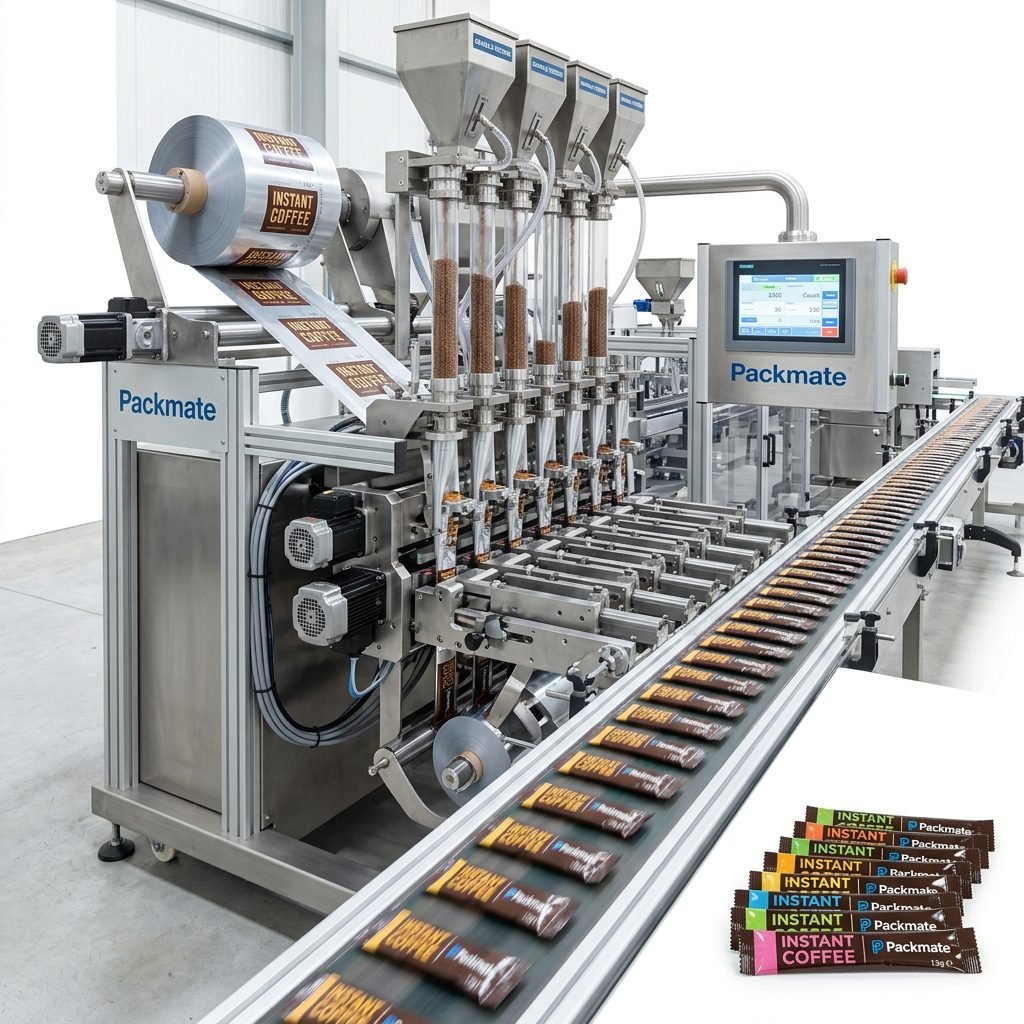
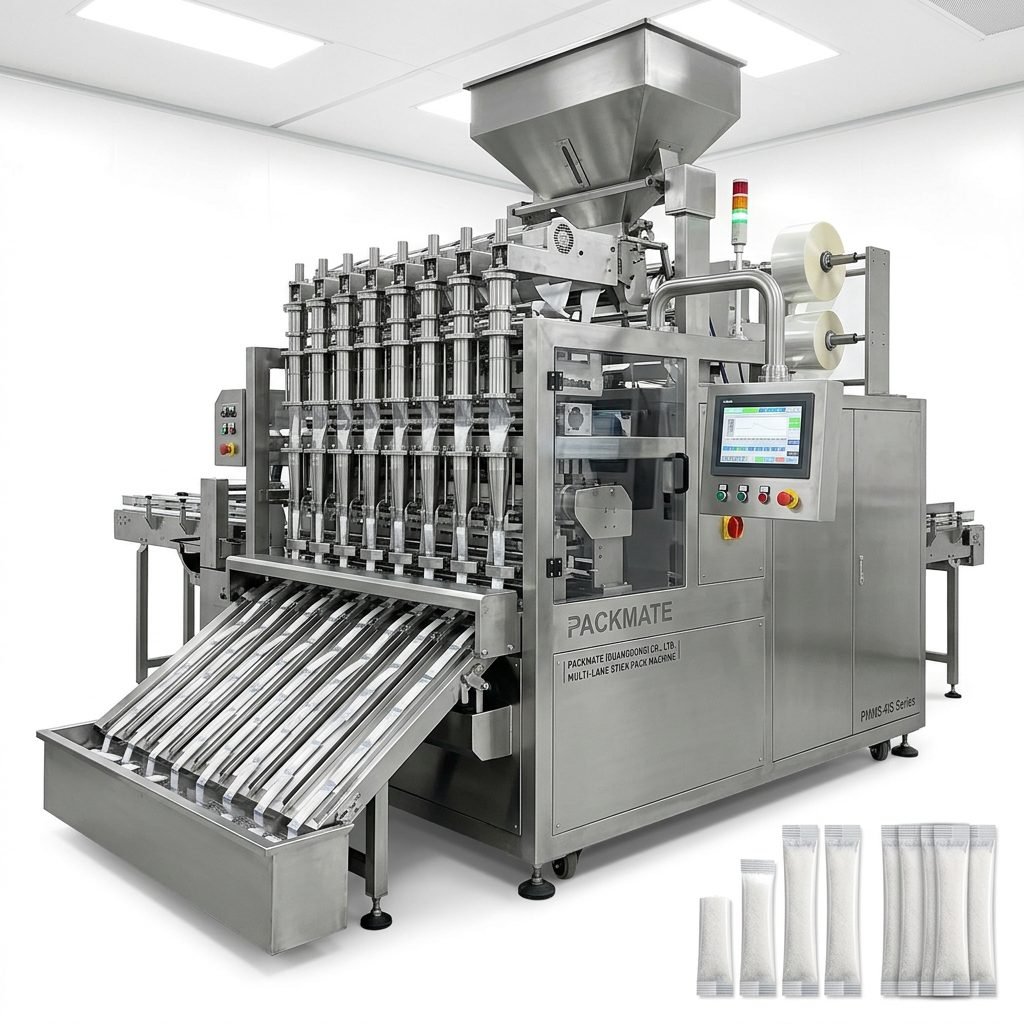
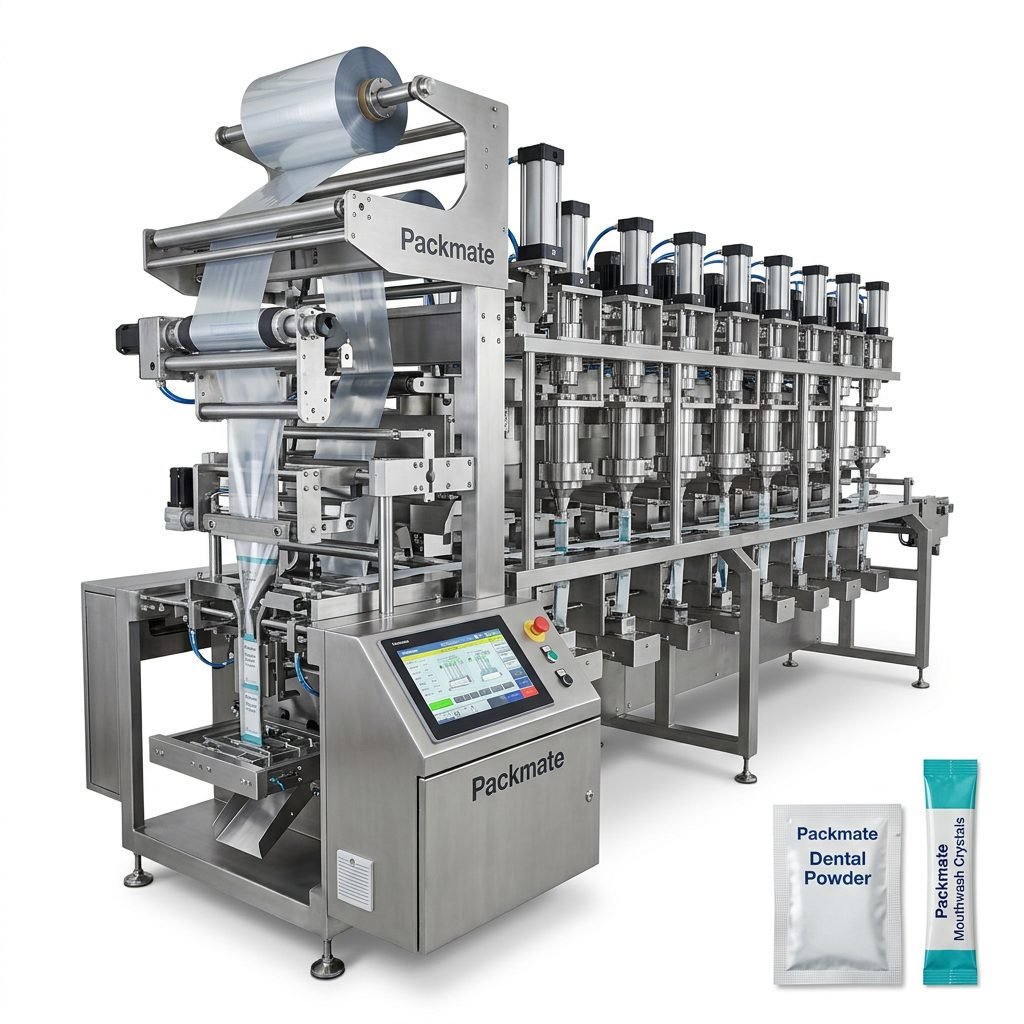
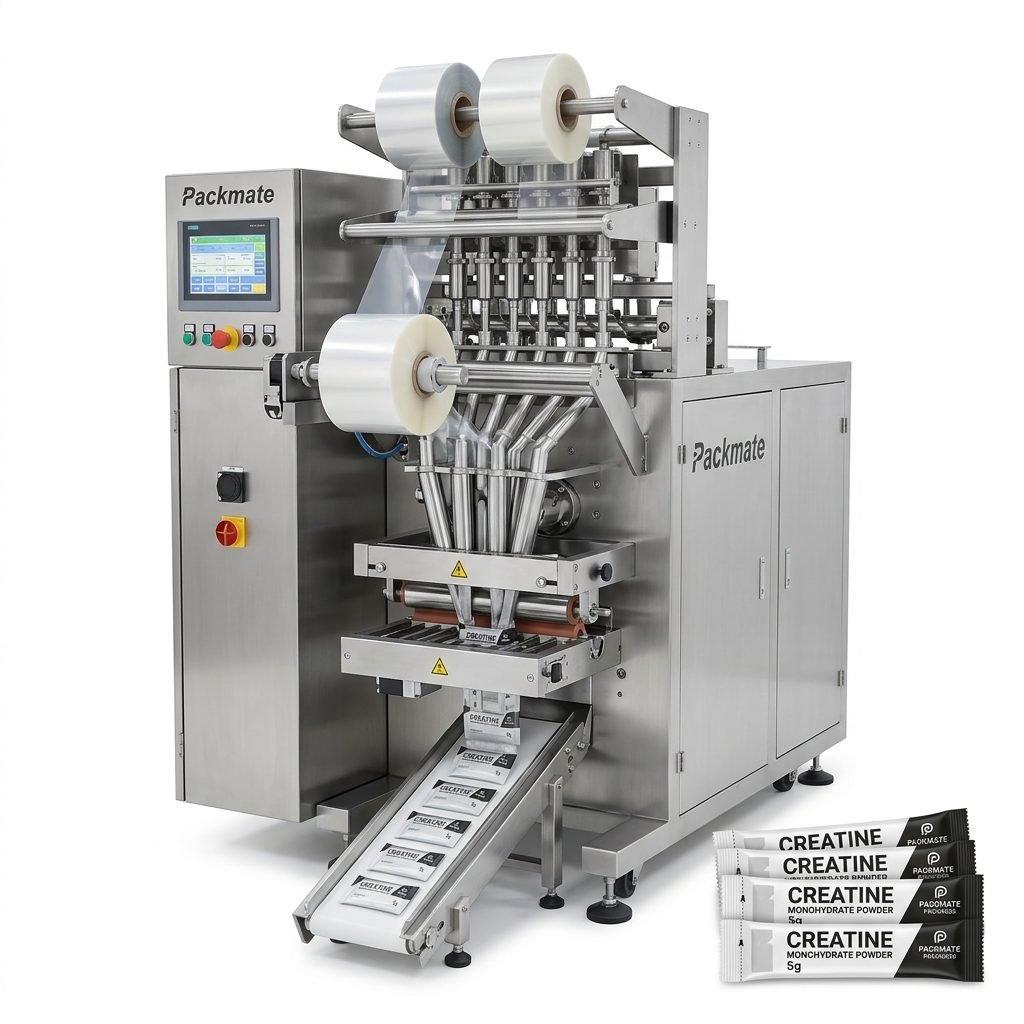
Food packaging lines must handle a diverse range of consistencies—from granules and powders to liquids and pastes—while operating at high speeds to meet volume demands. Hygiene is non-negotiable, requiring equipment with easy-clean designs, sanitary surfaces, and often compliance with standards like HACCP. Solutions like multi-lane stick pack machines or high-speed sachet fillers are essential for portion control, freshness preservation, and appealing retail presentation. The ability to quickly changeover between different product types and packaging formats is also a key efficiency driver for food producers.
Pharmaceutical Industry: Precision, Traceability, and Compliance
This is arguably the most stringent environment for packaging. Equipment must deliver exact, repeatable dosing with zero tolerance for error. Compliance with Good Manufacturing Practices (GMP) and regulatory standards (e.g., FDA, EMA) governs every aspect, from material selection to data integrity. Features like in-line weight checkers, vision inspection systems, and serialization capabilities for track-and-trace are not optional but mandatory. The packaging process itself must often be conducted in controlled environments to prevent contamination.
Health & Nutraceutical Products: Blending Consumer Appeal with Integrity
Health products, including vitamins, supplements, and nutraceuticals, sit at the intersection of pharmaceutical rigor and consumer goods marketing. The packaging must ensure product stability and potency (often requiring barrier materials against moisture and oxygen) while also being attractive on shelf. Accuracy in filling is critical to deliver promised dosages. Many health products also utilize specific formats like stick packs for powder supplements or blister packs for tablets, requiring equally specific and reliable machinery.
Core Components of a Modern Packaging Line
A complete, turnkey packaging line is a symphony of integrated machines, each performing a specific function. Understanding these components is key to specifying the right solution for your needs.
1. Feeding & Dosing Systems
The heart of accuracy. These systems meter the exact amount of product into each package. Technologies range from volumetric cups and auger fillers for powders to precision pumps for liquids and advanced weigh-fill systems for granules. The choice depends entirely on product characteristics and required accuracy.
2. Packaging Machine (Form-Fill-Seal)
This is the core unit where packaging material (film, foil, laminate) is formed into a bag, filled with product, and sealed. Vertical Form-Fill-Seal (VFFS) machines are ubiquitous for bags and pouches, while horizontal machines (HFFS) are often used for blister packs or sachets. Multi-lane configurations dramatically increase output.
3. Ancillary Equipment
This category includes all supporting units that add functionality: checkweighers to reject under/overweight packs, metal detectors or X-ray inspectors for contamination control, date/batch coders, labeling systems, and cartoners for secondary packaging.
4. Control & Integration System
The brain of the operation. Modern lines are governed by Programmable Logic Controllers (PLCs) and Human-Machine Interfaces (HMIs) that allow for centralized control, recipe management, production data logging, and seamless communication between all line components. This is essential for efficiency and traceability.
Why Partner with a Specialist Provider like Packmate?
Building a reliable packaging line involves more than purchasing individual machines. It requires deep application knowledge, engineering expertise, and a commitment to after-sales support. This is where a partner with a proven track record becomes invaluable.
With over 30 years of industry experience, Packmate (GuangDong) Co., Ltd. embodies this specialist approach. Operating from a modern 20,000㎡ facility, our journey from a focused workshop to a leading provider of turnkey lines gives us unique insight into the practical challenges manufacturers face. We don’t just sell machines; we deliver complete packaging line solutions.
Our portfolio of over 50 machine models is designed to address the specific needs of food, pharma, and health products. From high-speed multi-lane stick pack machines for instant beverage powders to precise sachet lines for pharmaceutical samples, our engineering is driven by the core principles of reliability, innovation, and hygienic design. We understand that our clients’ success depends on lines that run smoothly, minimize downtime, and adapt to future needs. You can learn more about our foundational principles on our Mission & Vision page.
Furthermore, our global service network ensures that support is always available, maximizing your line’s uptime and productivity over its entire lifecycle. For a comprehensive overview of our technical capabilities, our equipment catalog provides detailed specifications.
Frequently Asked Questions (FAQs)
1. What is the most important factor when choosing packaging equipment for pharmaceutical products?
Compliance and precision are paramount. The equipment must be designed to meet GMP standards, allow for full validation (IQ/OQ/PQ), and provide auditable data traceability. Dosing accuracy and the ability to integrate with inspection and serialization systems are critical non-negotiable features.
2. Can one packaging line handle different types of products (e.g., powder and granules)?
Yes, but with considerations. Many modern lines are designed for quick changeover. This may involve interchangeable dosing systems (e.g., swapping an auger filler for a volumetric cup) and easy-to-adjust forming tools. Discussing your product range with your supplier during the planning phase is crucial to ensure the line’s flexibility meets your needs.
3. How do I ensure the packaging line will be reliable and minimize downtime?
Choose a supplier with a strong reputation for quality engineering and robust after-sales service. Look for machines built with high-grade components, accessible maintenance points, and comprehensive training for your operators. A reliable partner will also offer readily available spare parts and remote support capabilities.
4. What is a “turnkey” packaging line solution?
A turnkey solution means the supplier takes single-point responsibility for the entire project—from design and engineering to manufacturing, installation, commissioning, and training. They deliver a fully integrated, production-ready line where you essentially “turn the key” to begin operation. This approach reduces risk, saves time, and ensures all components work together seamlessly.
5. How can I see examples of your equipment in action or discuss a specific project?
We encourage you to explore our case studies to see real-world applications. For direct discussion and customized proposals, please visit our Contact Us page to get in touch with our engineering and sales team. We are ready to understand your challenges and develop the optimal solution for your production goals.