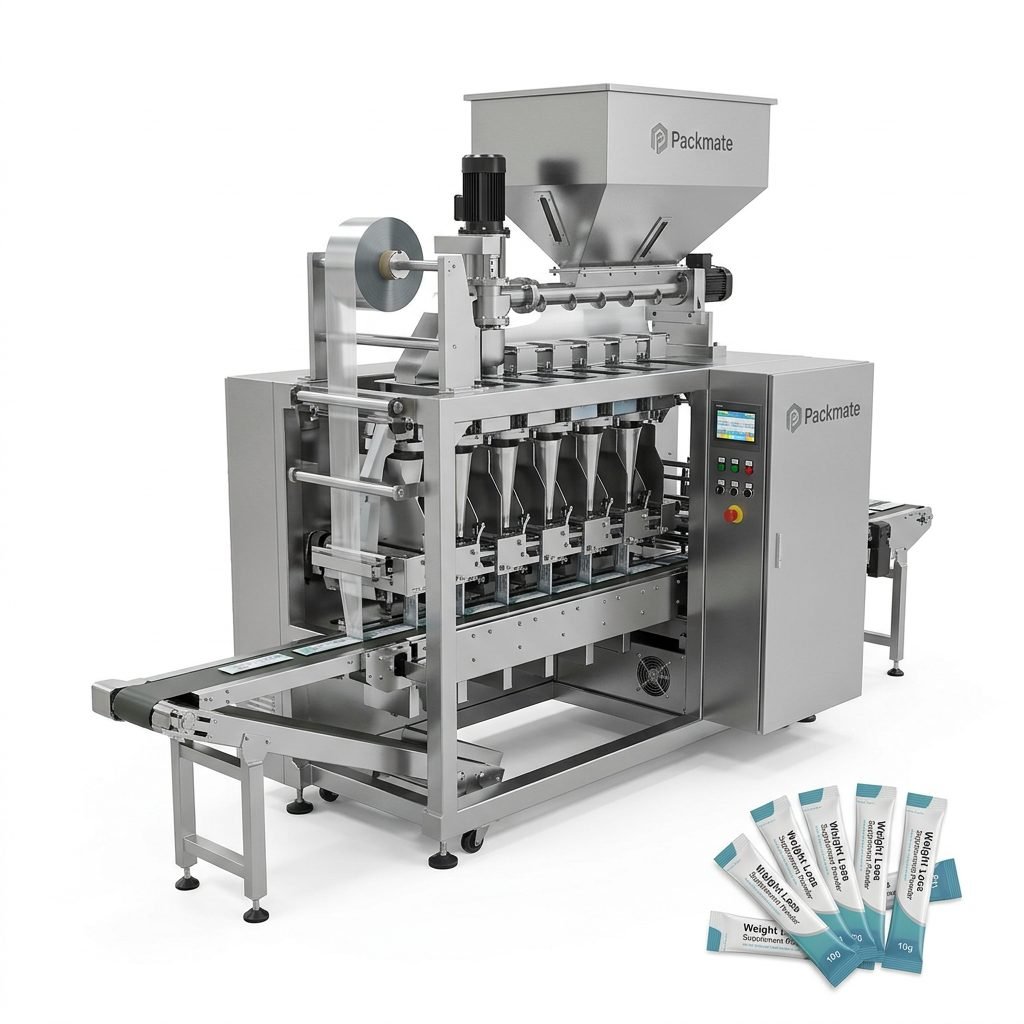
The pharmaceutical and medical device industries operate under a unique and uncompromising set of rules. Precision, sterility, traceability, and patient safety are not just goals—they are absolute mandates. In this high-stakes environment, the final step of production—packaging—transcends mere containment. It becomes a critical component of the product’s integrity, safety, and efficacy. This is where specialized Healthcare Packaging Line Solutions move from being an operational advantage to a fundamental necessity.
The Critical Role of Packaging in Pharma & Medical Products
Packaging in healthcare serves a multi-layered purpose far beyond that of consumer goods. Its primary functions include:
- Product Protection: Shielding sensitive pharmaceuticals from moisture, light, oxygen, and contamination throughout the supply chain.
- Sterility Assurance: Maintaining a sterile barrier for medical devices, implants, and surgical tools until the point of use.
- Dosage Integrity & Compliance: Ensuring accurate dosing (e.g., in unit-dose blister packs) and providing clear, tamper-evident features to prevent misuse.
- Regulatory Compliance: Enabling full traceability with serialization and aggregation codes as required by global regulations like the U.S. FDA’s DSCSA and the EU’s Falsified Medicines Directive.
- Patient Safety & Usability: Incorporating features like child-resistant closures, senior-friendly opening mechanisms, and clear instructional labeling.
A failure in any of these areas can have dire consequences, making the reliability and precision of the packaging process paramount.
Why Turnkey Automated Systems Are the Answer
Piecemeal approaches to packaging—sourcing individual machines from different vendors—introduce significant risk in a regulated industry. Inconsistent interfaces, data silos, and finger-pointing during downtime are liabilities. A turnkey automated system, provided by a single, experienced supplier like Packmate (GuangDong) Co., Ltd., offers a cohesive, validated solution. This approach ensures seamless integration from the infeed of primary containers to the final palletized load, all controlled by a unified system that guarantees data integrity and process consistency.
Core Components of a Modern Healthcare Packaging Line
A comprehensive, turnkey line integrates several advanced modules, each performing a critical function with pharmaceutical-grade precision.
1. Automated Feeding & Orientation Systems
Gentle, precise handling of vials, syringes, bottles, or blister cards is the first step. Vision systems and sophisticated conveyors ensure each item is correctly positioned for downstream processes, minimizing jams and product damage.
2. Primary Packaging: Filling, Sealing, and Capping
This is the heart of the line, where the product meets its immediate container. Technologies include:
- Aseptic Fill-Finish Lines: For injectables and biologics, operating in ISO 5 environments.
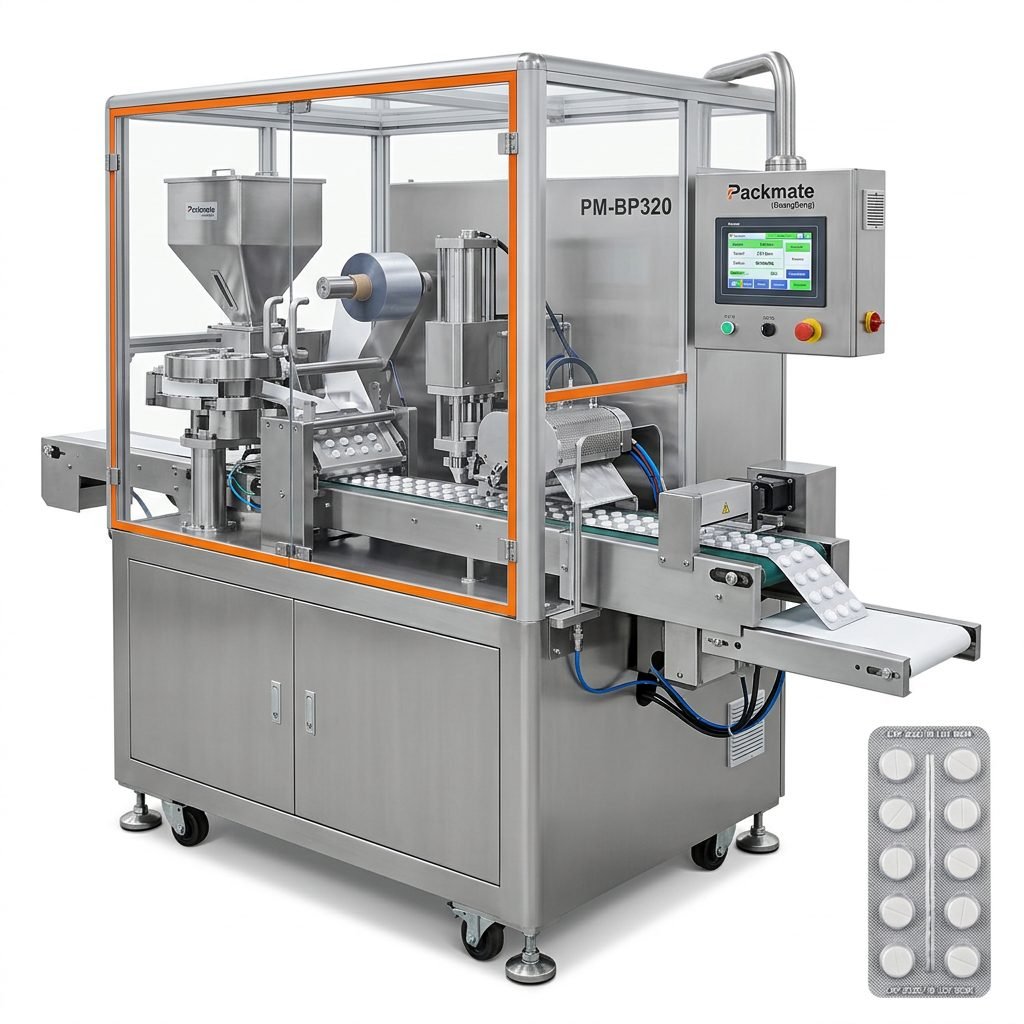
- High-Speed Blister Packaging: For tablets and capsules, with integrated vision inspection for missing or damaged product.
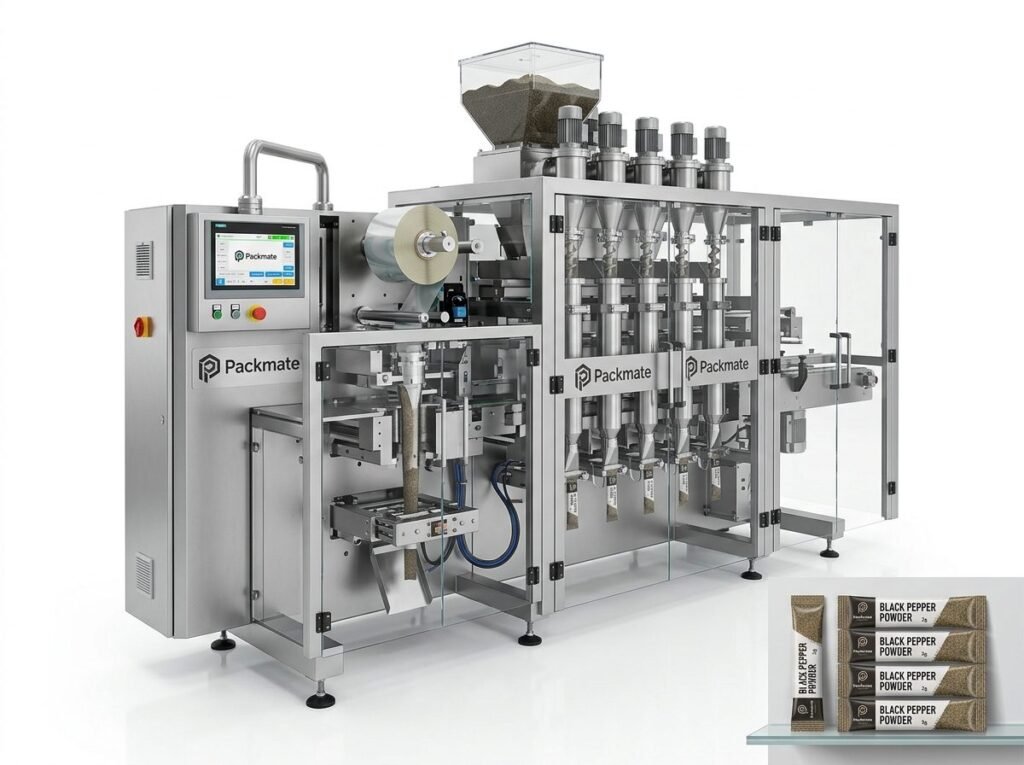
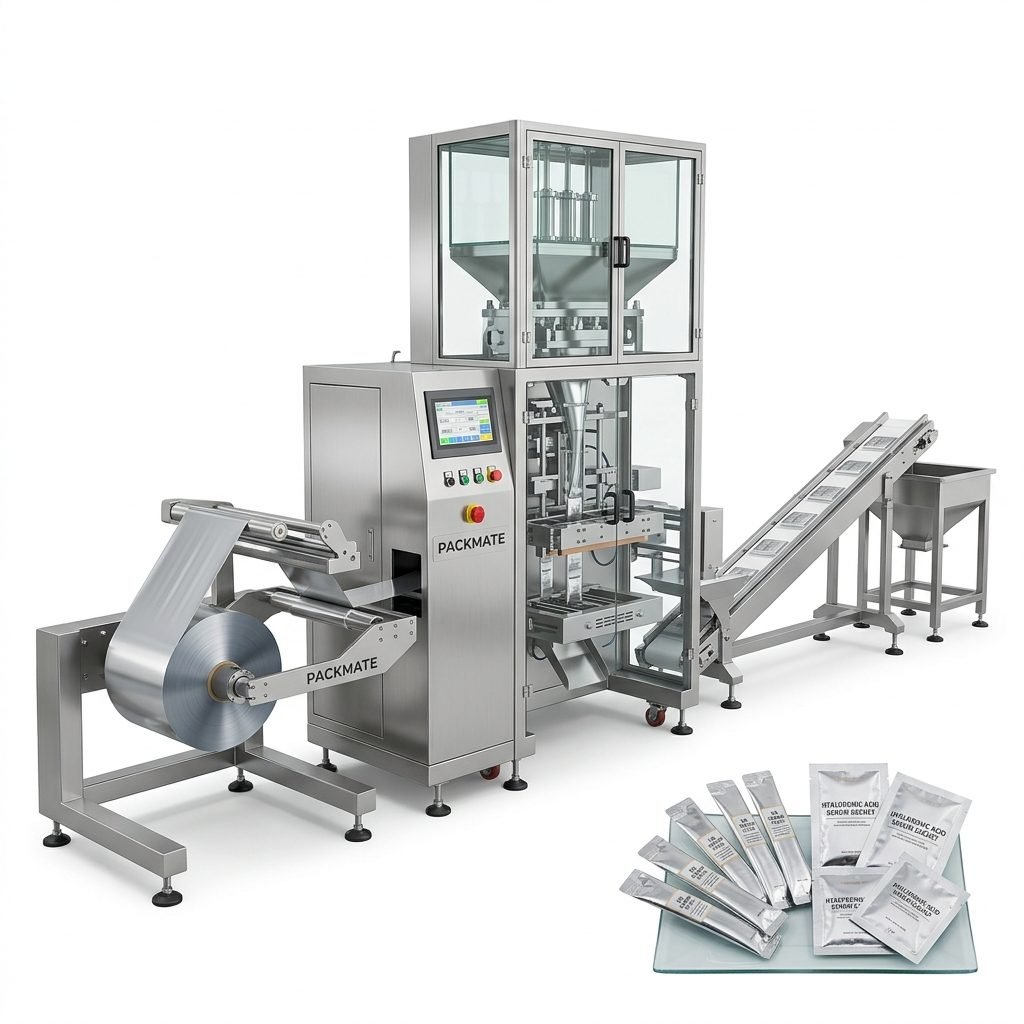
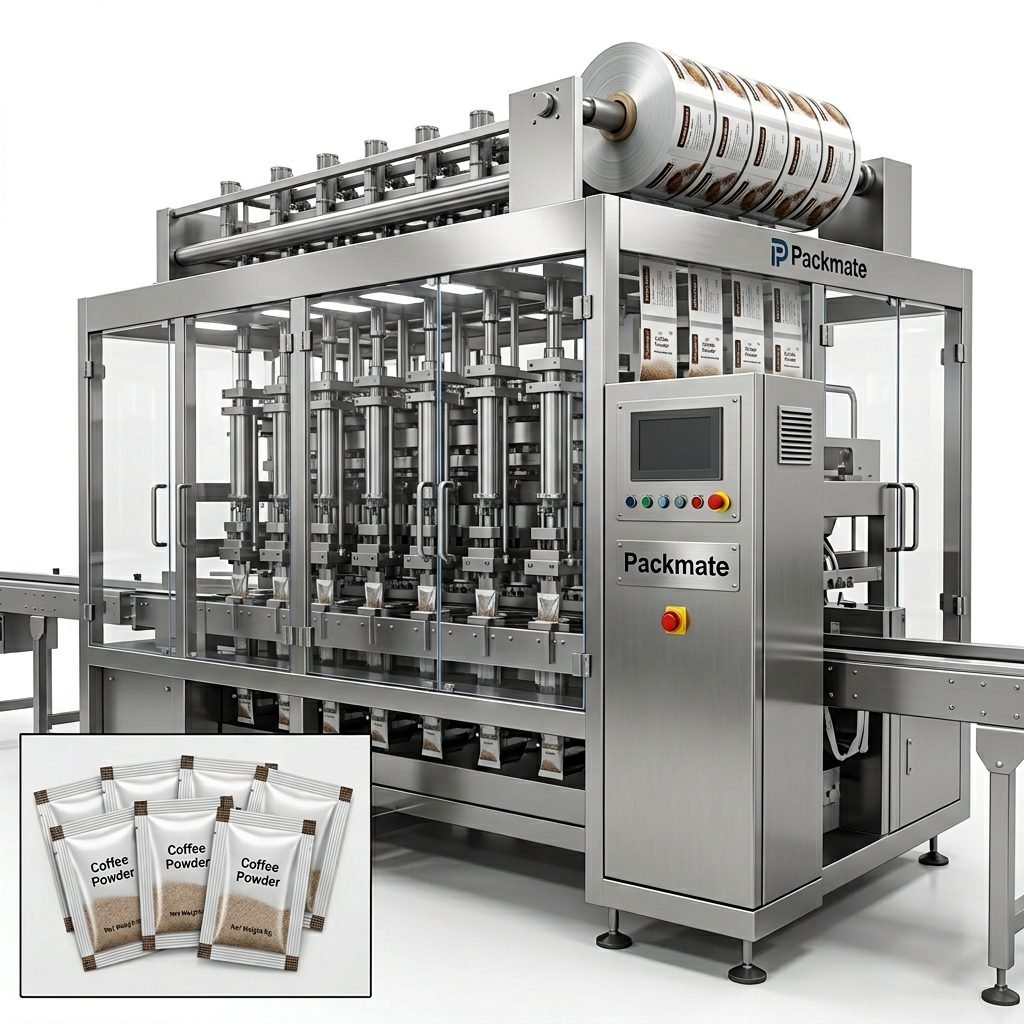
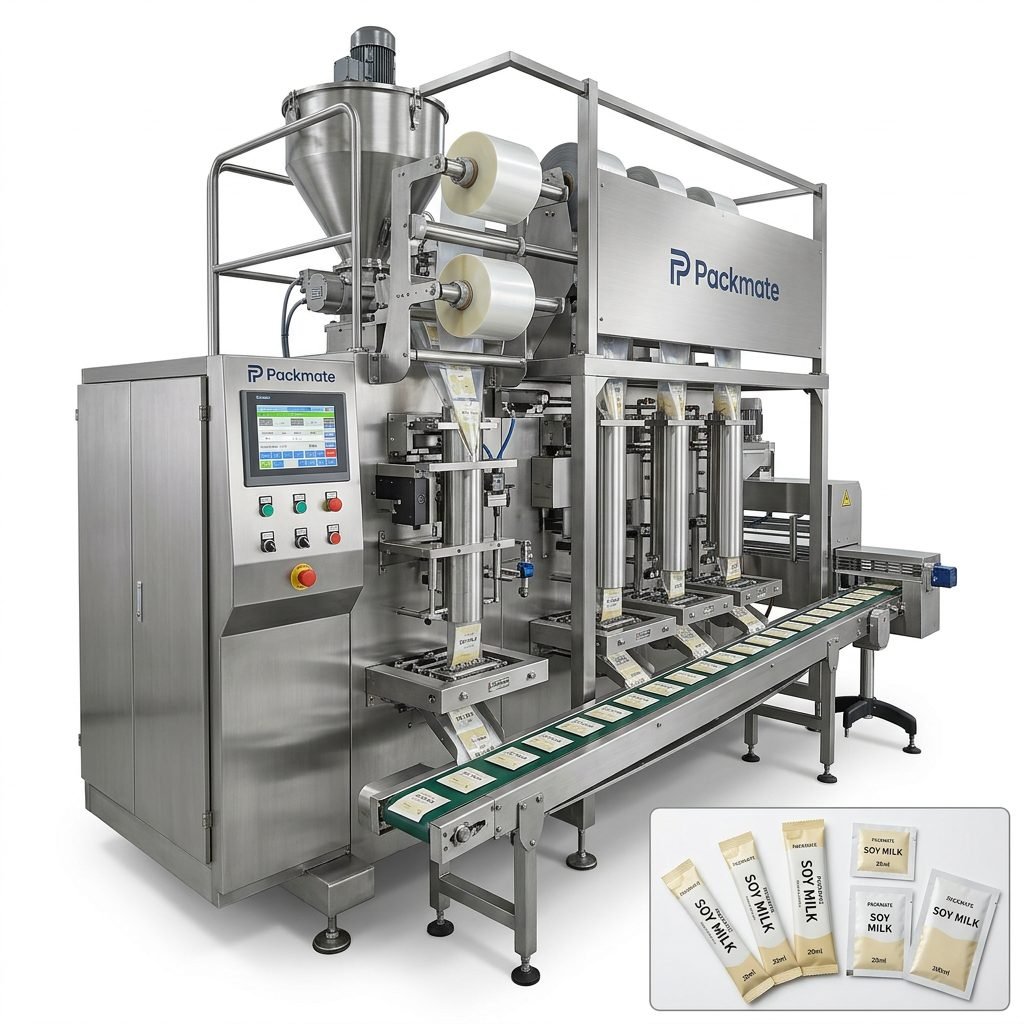
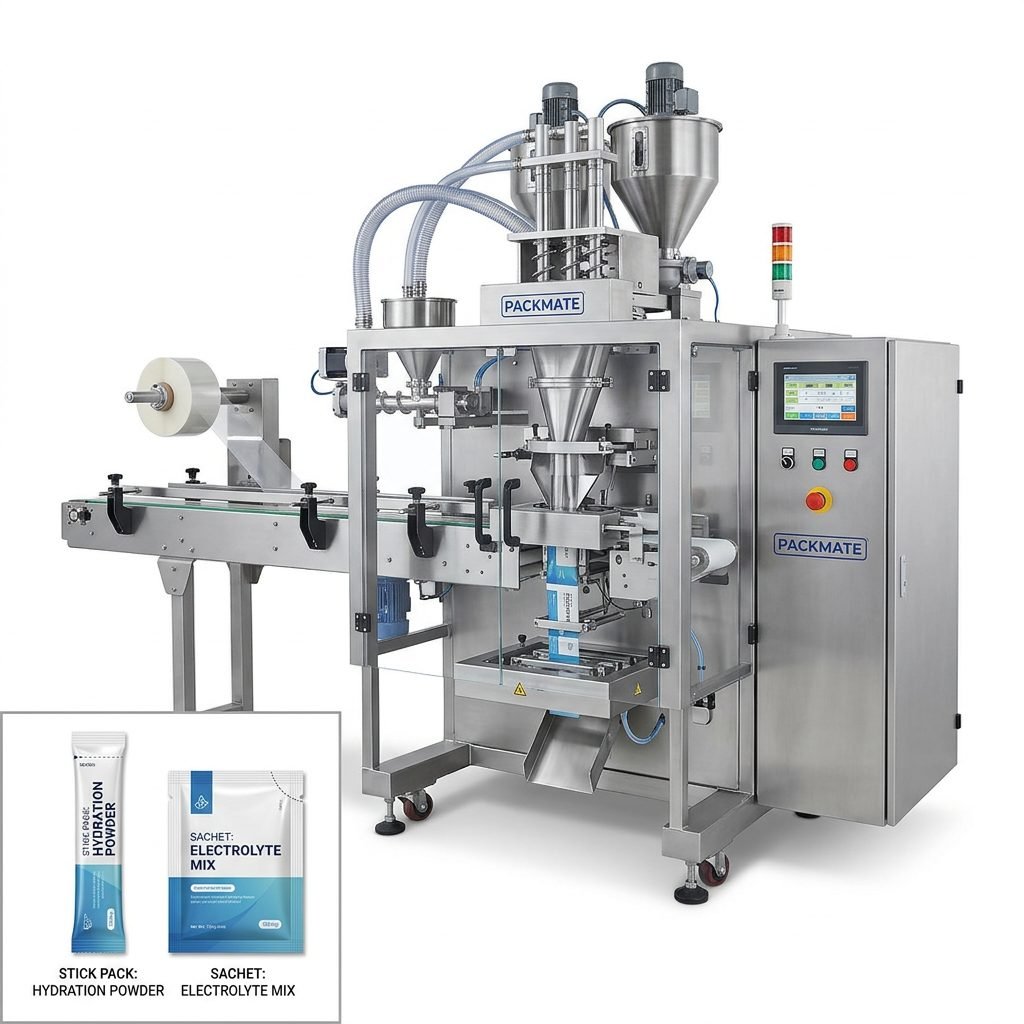
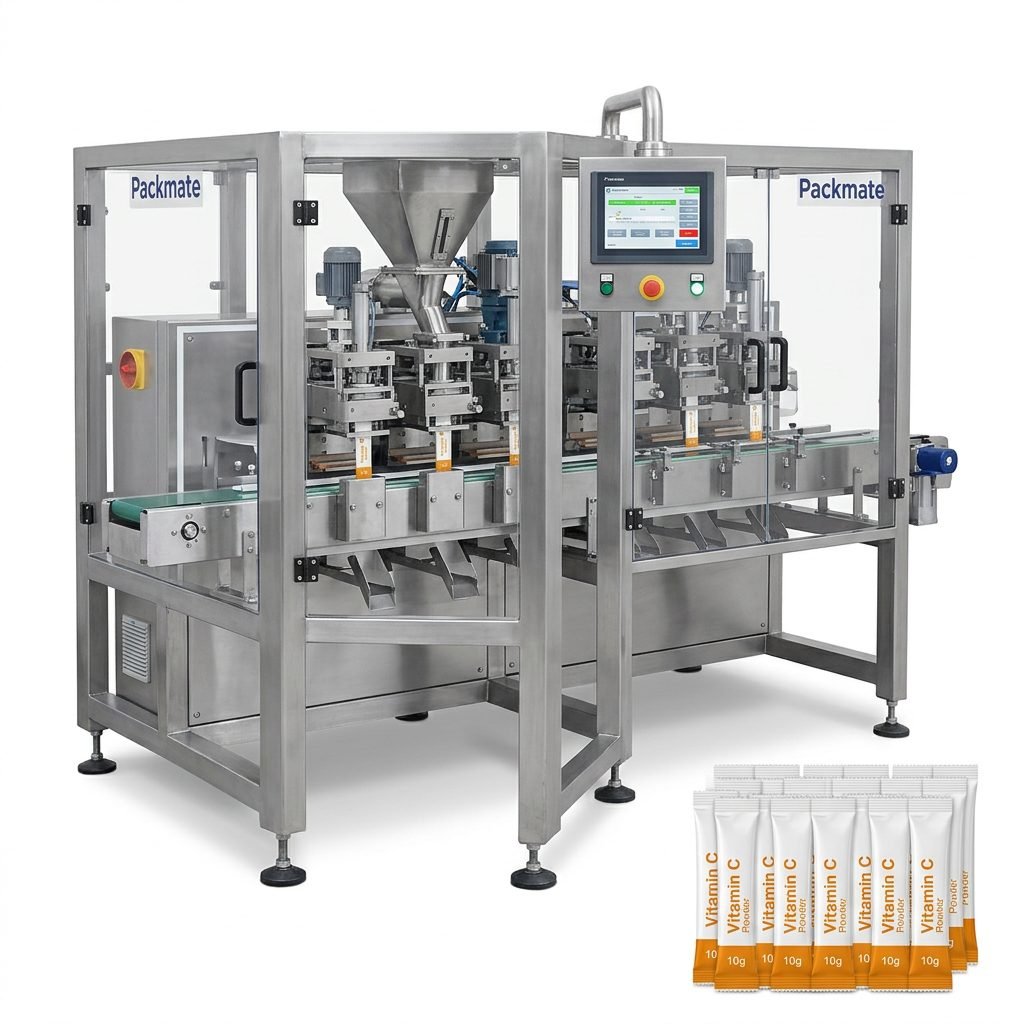
- Liquid & Powder Dosing Systems: Ultra-precise pumps and augers for sachets, stick packs, or bottles, crucial for accurate dosage.
3. Labeling, Serialization & Aggregation
This module applies product labels with critical information and, more importantly, prints and verifies unique serial numbers (like 2D Data Matrix codes) on each saleable unit. It then aggregates these units into cases and pallets, creating a digital “parent-child” relationship for complete supply chain visibility. Compliance with global track-and-trace mandates is impossible without this integrated step.
4. Secondary & Tertiary Packaging
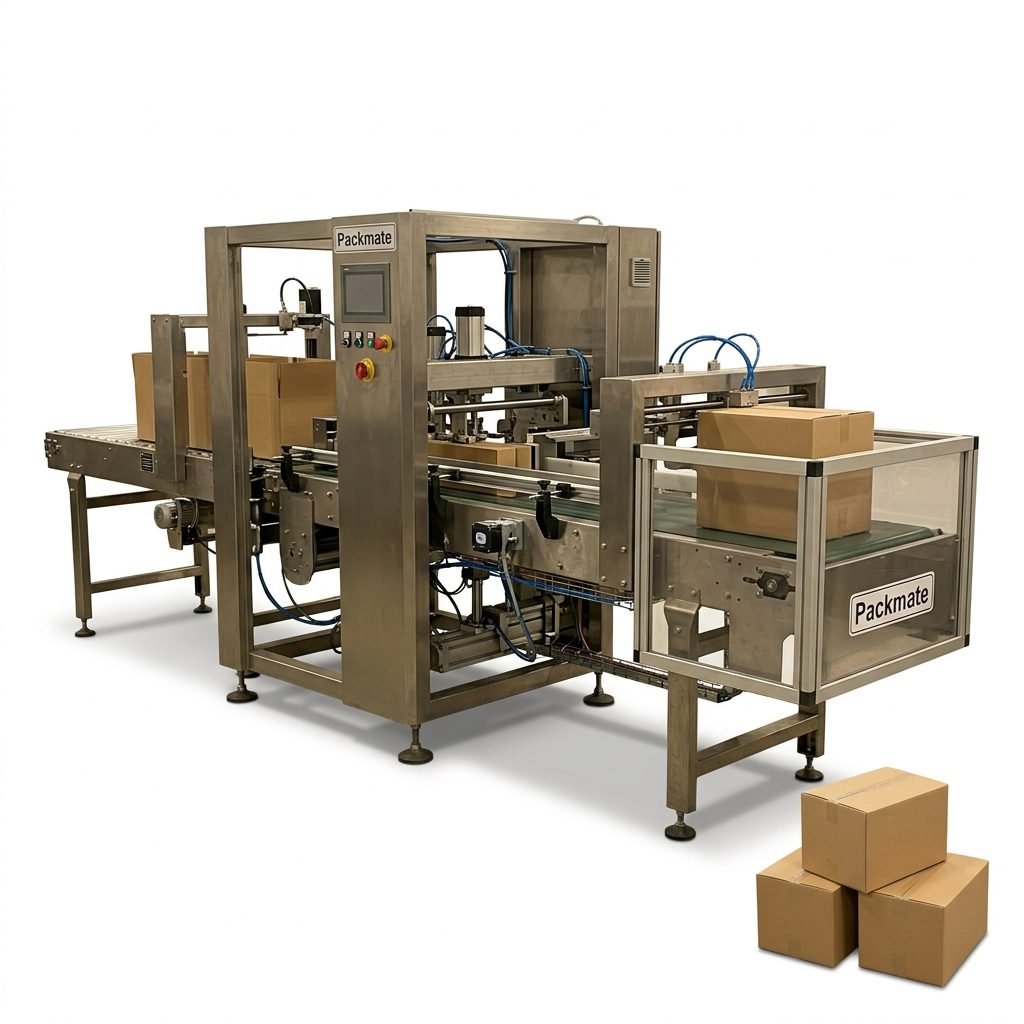
Automated cartoners erect, load, and seal secondary packaging. Robotic palletizers then arrange cases onto pallets according to optimized patterns, ready for warehousing and shipment. This stage ensures physical protection and logistical efficiency.
5. The Central Nervous System: Integrated Control & Data Acquisition
An overarching SCADA (Supervisory Control and Data Acquisition) system or MES (Manufacturing Execution System) layer monitors and controls the entire line. It collects real-time data on OEE (Overall Equipment Effectiveness), production counts, downtime reasons, and quality metrics, providing actionable insights for continuous improvement and simplified regulatory reporting.
Key Benefits of Partnering with a Turnkey Solution Provider
Choosing a partner like Packmate for your healthcare packaging line delivers strategic advantages:
✔ Single Point of Accountability: One partner is responsible for the performance of the entire system, from design and installation to validation and ongoing service.
✔ Reduced Validation Complexity: An integrated system from one vendor simplifies the demanding IQ/OQ/PQ (Installation/Operational/Performance Qualification) validation process.
✔ Optimized Line Efficiency: Machines designed to work together from the outset minimize bottlenecks and maximize throughput (UPH) and Overall Equipment Effectiveness (OEE).
✔ Future-Proof Scalability: A forward-looking design allows for easier integration of new technologies or capacity expansion as your product portfolio grows.
✔ Lifecycle Support & Expertise: Access to dedicated technical support, spare parts, and process expertise for the lifecycle of your equipment. Explore our commitment to this in our Service section.
Selecting the Right Partner for Your Healthcare Packaging Line
Not all automation providers are equipped for the rigors of healthcare. When evaluating a partner, consider these essential criteria:
- Regulatory Experience & GMP Mindset: Do they have a proven track record with FDA, EMA, or other relevant regulatory frameworks? Is their design philosophy rooted in Good Manufacturing Practices (GMP)?
- Technical Expertise & Innovation: Can they demonstrate deep knowledge in handling your specific product form (powder, liquid, sterile device)? Do they invest in R&D for next-generation solutions?
- Project Management & Validation Support: Do they offer comprehensive project management, including FAT (Factory Acceptance Testing), SAT (Site Acceptance Testing), and validation documentation support?
- Global Service Network: For multinational companies, can they provide timely service and support in your key manufacturing regions?
With over 22 years of company development and a 20,000㎡ modern manufacturing facility, Packmate embodies these qualities, bringing a wealth of experience to every project.
Conclusion: Packaging as a Strategic Pillar
In the world of pharmaceuticals and medical products, packaging is a strategic pillar of product success and patient safety. Investing in a turnkey, automated packaging line is an investment in quality, compliance, and operational excellence. It mitigates risk, enhances efficiency, and provides the robust data integrity required in today’s regulated landscape. By partnering with an experienced, single-source provider, companies can transform their packaging operations from a necessary cost center into a reliable, compliant, and competitive asset.
Frequently Asked Questions (FAQs)
1. What is the main advantage of a turnkey system over buying individual machines?
The primary advantage is single-source accountability and seamless integration. A turnkey provider designs all components to work harmoniously, ensuring optimal communication, data flow, and mechanical interfacing. This drastically reduces validation time, eliminates integration headaches between different machine vendors, and provides one point of contact for service and support, simplifying the entire lifecycle of the packaging line.
2. How do healthcare packaging lines ensure compliance with track-and-trace regulations?
Modern lines integrate dedicated serialization and aggregation stations. These units apply a unique identifier (like a 2D data matrix code) to each saleable unit, verify its quality, and then associate (“aggregate”) those units to their case and pallet codes. This creates a digital hierarchy that allows for precise tracking throughout the supply chain, which is mandatory under regulations like the U.S. DSCSA and the EU FMD.
3. Can an automated packaging line handle different product formats or sizes?
Yes, with proper design. Many lines are built with changeover flexibility in mind. This can include quick-change parts, adjustable conveyors, and programmable settings stored in the line’s HMI (Human-Machine Interface). The level of flexibility should be defined during the project’s initial design phase based on your current and future product portfolio needs.
4. What is typically included in the validation package for a pharmaceutical packaging line?
A comprehensive validation package follows the IQ/OQ/PQ protocol. The supplier typically assists with Installation Qualification (documenting correct installation), Operational Qualification (proving each machine function works to spec), and provides the framework for Performance Qualification (proving the entire line produces consistent, acceptable product under normal operating conditions). This documentation is critical for regulatory submissions.
5. How important is after-sales service and support for these complex systems?
It is critical. Given the high cost of downtime in pharmaceutical production, reliable and rapid technical support is essential. A good partner will offer comprehensive service agreements, readily available spare parts, remote diagnostics, and on-site technician support. This ensures maximum line uptime and protects your long-term investment. For more details, visit our dedicated FAQs page.