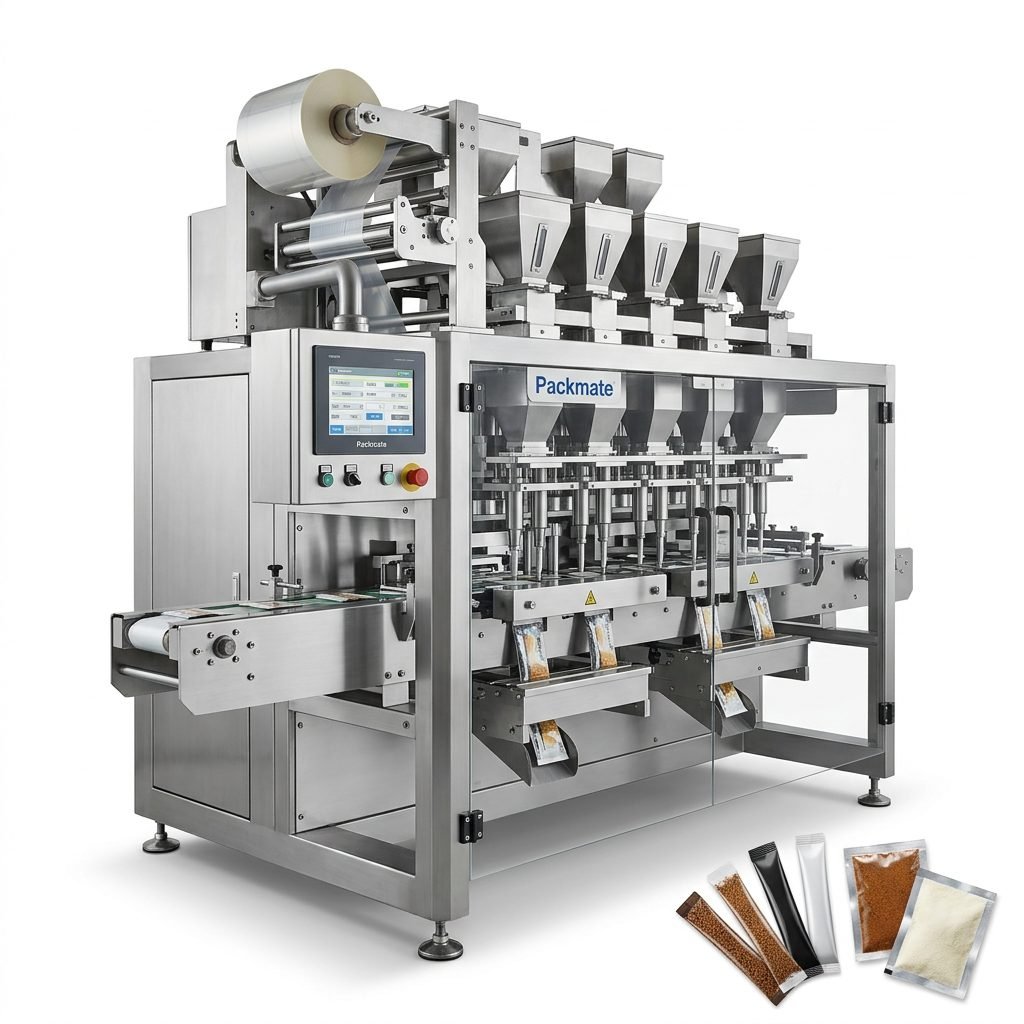
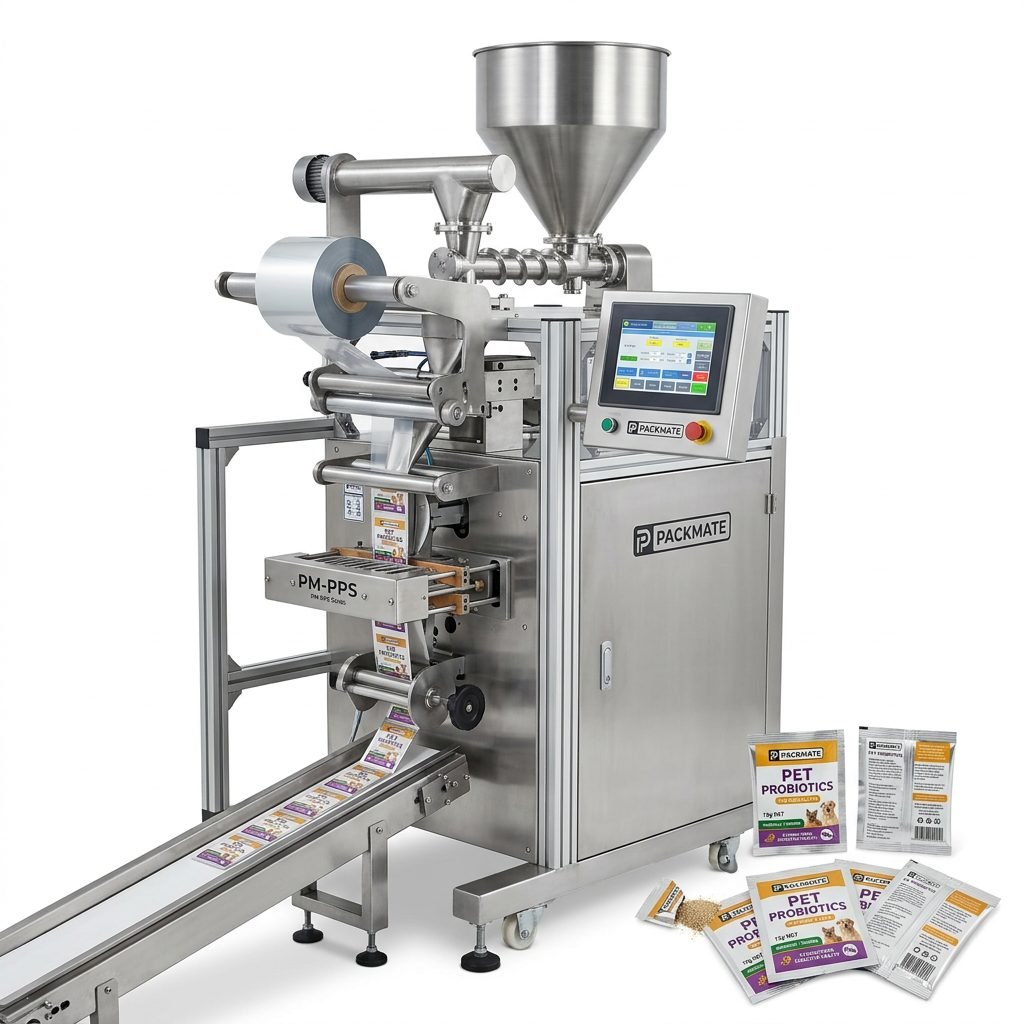
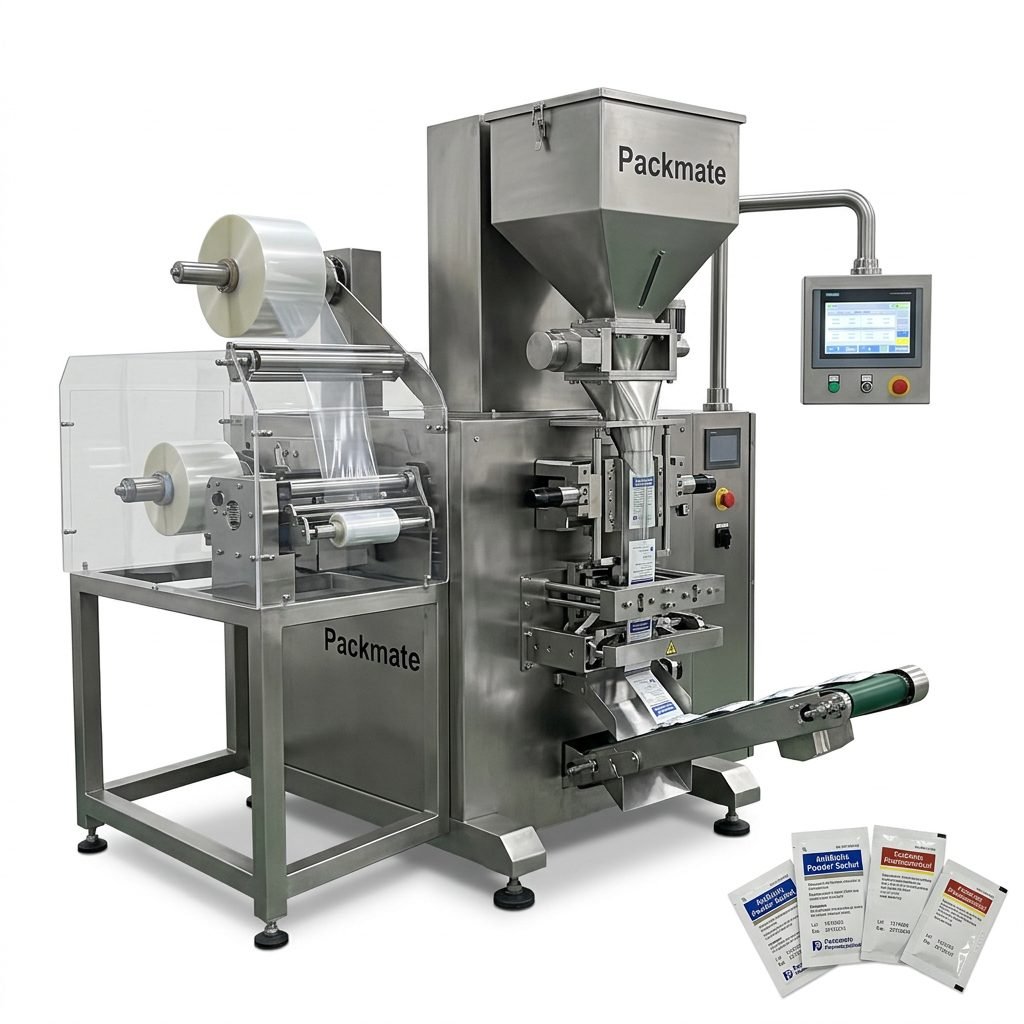
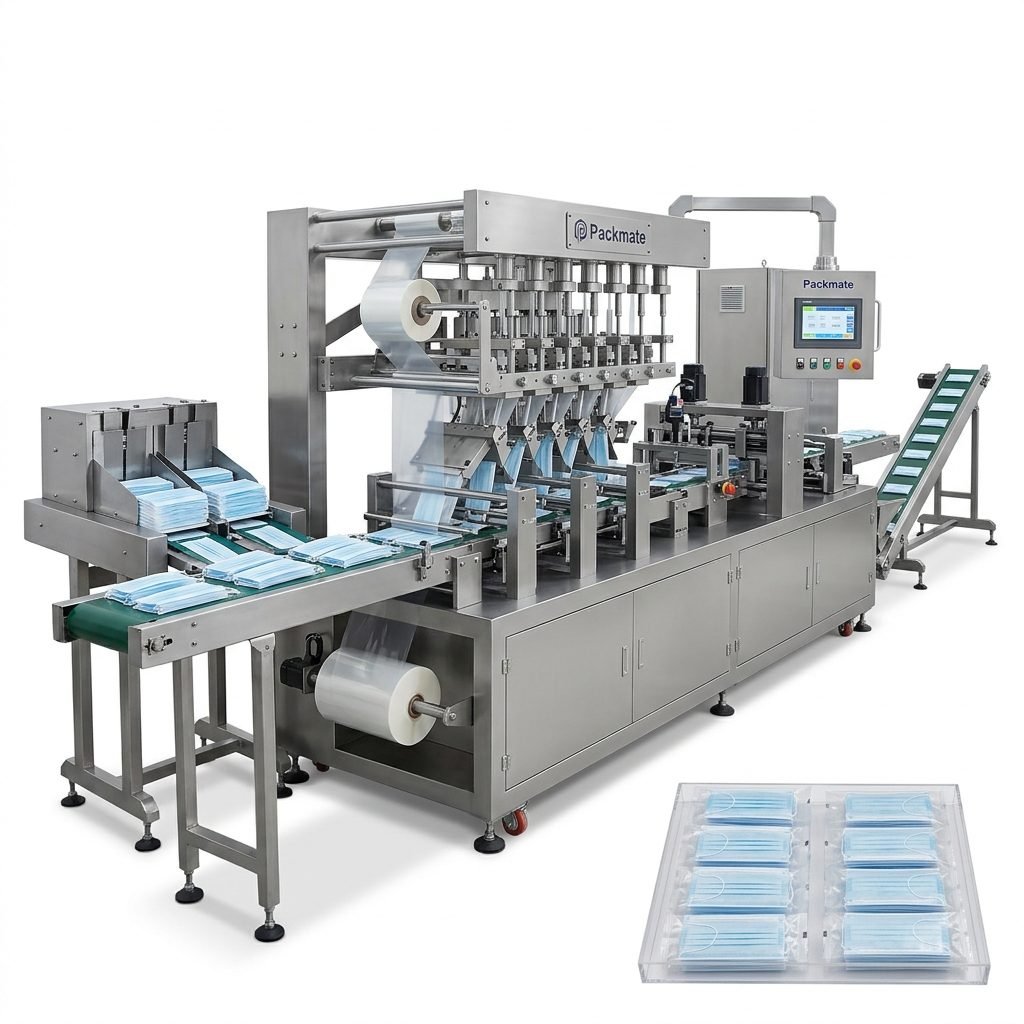
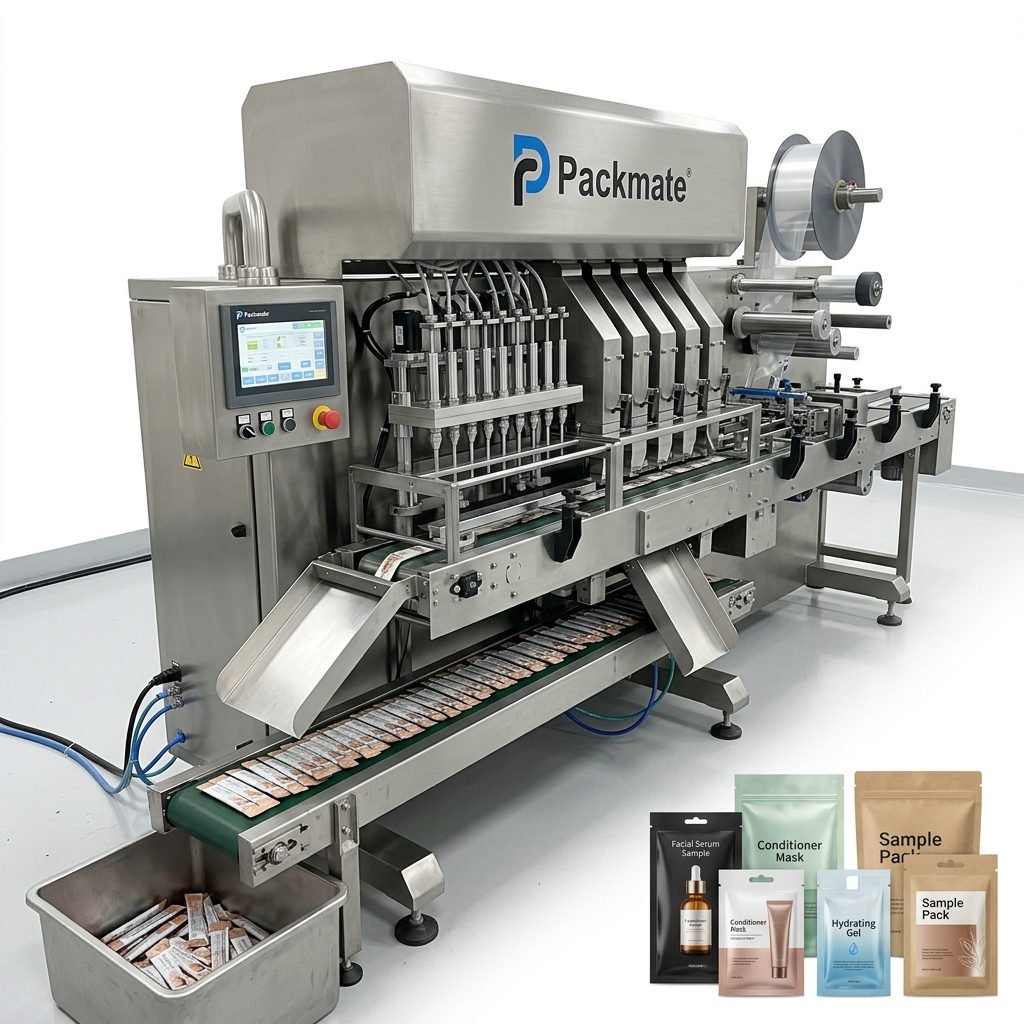
In the dynamic and highly regulated sectors of food, pharmaceuticals, and health products, packaging is far more than just a final step in production. It is a critical component that ensures product integrity, safety, shelf life, and consumer trust. A Liquid Packaging Line Factory Solution represents the pinnacle of this process, integrating advanced machinery, intelligent controls, and hygienic design into a seamless, turnkey operation. For manufacturers seeking efficiency, compliance, and scalability, investing in a comprehensive factory solution is not an option—it’s a necessity for competitive advantage and market leadership.
The Core of Modern Production: Integrated Liquid Packaging Lines
An effective liquid packaging line is a symphony of coordinated systems. It begins with precise liquid handling and dosing, moves through filling and sealing with impeccable accuracy, and concludes with labeling, coding, and secondary packaging. The factory solution approach means every component—from the unscrambler and filler to the capper and labeler—is designed to work in perfect harmony. This integration minimizes transition points where contamination could occur or efficiency could drop, creating a robust and reliable production flow. For businesses looking to streamline their operations, exploring our comprehensive packaging solutions provides a clear pathway to achieving these operational goals.
Meeting Stringent Industry-Specific Demands
The requirements for packaging vary dramatically across different industries, making a one-size-fits-all approach ineffective. A world-class factory solution is meticulously tailored to address these unique challenges.
Food & Beverage Industry
Here, speed, hygiene, and preserving freshness are paramount. Solutions must handle a wide range of viscosities—from thin juices to viscous sauces—and often incorporate features like nitrogen flushing to extend shelf life. Lines must be easy to clean (CIP/SIP systems) and quick to change over for different products or package sizes, supporting high-volume production runs common in this sector.
Pharmaceutical & Nutraceutical Industry
Precision and sterility are non-negotiable. Packaging lines for syrups, suspensions, or injectables must operate in controlled environments, often meeting cGMP standards. Accuracy in fill volume is critical for dosage, and traceability through serialization is increasingly mandatory. Equipment must be constructed with pharmaceutical-grade materials that prevent leaching and withstand rigorous sterilization processes. The complexity of these requirements is why partnering with an expert provider, as detailed in our company profile, is essential for compliance and success.
Health & Personal Care Products
This segment, encompassing items like shampoos, lotions, and sanitizers, demands a blend of aesthetic appeal and functional integrity. Packaging lines need to be versatile to handle various bottle shapes and materials (plastic, glass), while ensuring perfect fills with no leakage. High-quality labeling and tamper-evident features are also crucial for brand image and consumer safety.
Key Components of a Turnkey Factory Solution
A successful implementation hinges on more than just hardware. It encompasses a full lifecycle partnership:
- Consultation & Custom Design: Experts analyze your product, output goals, and facility to design an optimal line layout.
- High-Precision Machinery: Including fillers (piston, volumetric), cappers, labelers, vision inspection systems, and conveyors.
- Integration & Automation: PLC controls and HMI interfaces allow for centralized monitoring, data collection, and minimal manual intervention.
- Hygienic & Compliant Engineering: Use of 316L stainless steel, sanitary fittings, and designs that prevent bacterial harborage.
- Training & Ongoing Support: Comprehensive training for operators and maintenance teams, backed by reliable spare parts and service. Our commitment to this level of support is part of our core service philosophy.
The Packmate Advantage: Three Decades of Innovation
With over 30 years of specialized experience, Packmate (GuangDong) Co., Ltd. stands as a leader in delivering intelligent packaging solutions. Our journey from a dedicated workshop to a modern 20,000㎡ manufacturing facility is built on a foundation of deep technical expertise and client collaboration. We understand that a factory solution is a significant investment, and we partner with clients to ensure it delivers maximum return through unparalleled reliability, efficiency, and adaptability. Our diverse portfolio of successful projects can be seen in our detailed case studies.
Our solutions are designed for the future. They offer the flexibility to adapt to new products, incorporate emerging technologies like IoT for predictive maintenance, and scale output to meet growing demand. This forward-thinking approach ensures your packaging line remains a valuable asset for years to come, protecting your brand and empowering your growth.
Driving Value: The Tangible Benefits of a Holistic Solution
Investing in an integrated factory solution from a trusted partner like Packmate delivers measurable outcomes:
✔ Enhanced Efficiency & Output: Streamlined processes and high-speed automation drastically increase production capacity and Overall Equipment Effectiveness (OEE).
✔ Superior Product Quality & Consistency: Precision engineering eliminates fill volume variations and packaging defects, reducing waste and customer complaints.
✔ Reduced Operational Costs: Lower labor dependency, minimized product giveaway, and decreased downtime translate directly to a healthier bottom line.
✔ Guaranteed Regulatory Compliance: Built-in compliance with FDA, cGMP, EHEDG, and other international standards mitigates risk and simplifies audits.
✔ Future-Proof Scalability: A modular design allows for easy expansion or reconfiguration, protecting your investment as your business evolves.
Conclusion
Choosing the right liquid packaging line factory solution is a strategic decision that impacts every facet of your production, from cost and compliance to brand reputation. In the exacting worlds of food, pharma, and health, partnering with an experienced provider who offers true turnkey integration is the key to unlocking sustained productivity and market success. By focusing on precision, hygiene, automation, and partnership, manufacturers can build a packaging operation that is not just efficient, but truly exemplary.
Frequently Asked Questions (FAQs)
1. What is the typical lead time for a complete turnkey liquid packaging line?
Lead times vary based on the line’s complexity and customization level. A standard configuration may take 3-6 months from order to delivery, while a highly customized solution for pharmaceutical applications can take 6-12 months. Detailed project planning during the consultation phase establishes a clear timeline.
2. How do you ensure the packaging line meets international sanitary standards (e.g., FDA, cGMP)?
We design and build with compliance as a core principle. This includes using certified materials (e.g., 316L stainless steel), implementing sanitary design principles (no dead legs, easy-clean surfaces), and providing full documentation packs. Our equipment often comes with standard certifications, and we can guide clients through regional validation processes.
3. Can your solutions handle different container types and sizes on the same line?
Yes, versatility is a key feature. Many of our lines are designed with quick-changeover systems for formats like bottles, vials, or pouches. Change parts for different container sizes can be swapped efficiently, minimizing downtime during product switches. The degree of flexibility is defined during the project’s design phase.
4. What kind of after-sales support and training do you provide?
We provide comprehensive support including on-site installation supervision, detailed operational and maintenance training for your team, a warranty period, and access to a global network for spare parts and technical service. Our goal is to ensure your line operates at peak performance throughout its lifecycle. For more details, visit our dedicated FAQ page.
5. How do you approach the integration of a new line into an existing factory facility?
Our process begins with a thorough facility audit. We analyze spatial layout, utility connections (power, air, water), and material flow to design a line that integrates seamlessly. Our engineering team creates detailed layout plans and works closely with your team to manage the installation process with minimal disruption to ongoing operations.