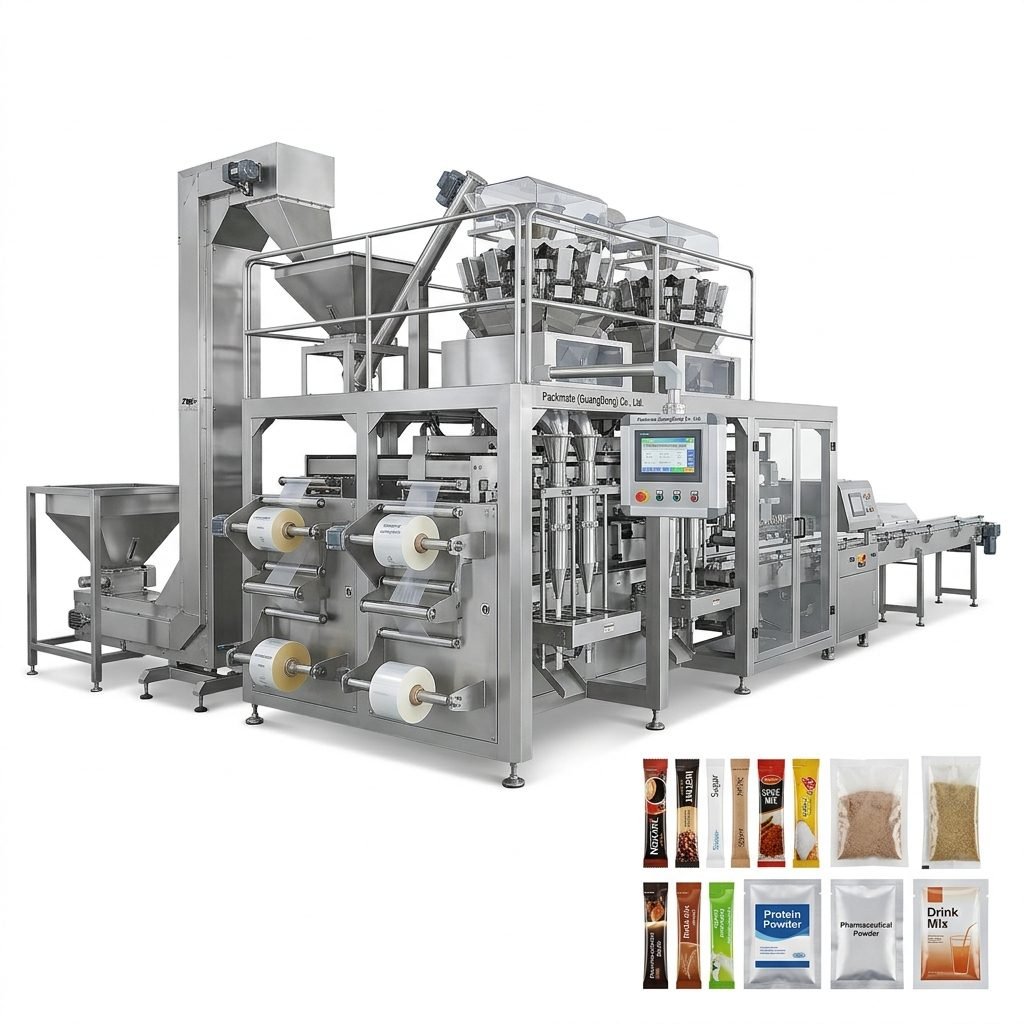
Heavy-Duty Bucket Elevator for Granules and Powders, High-Capacity Vertical Conveying System

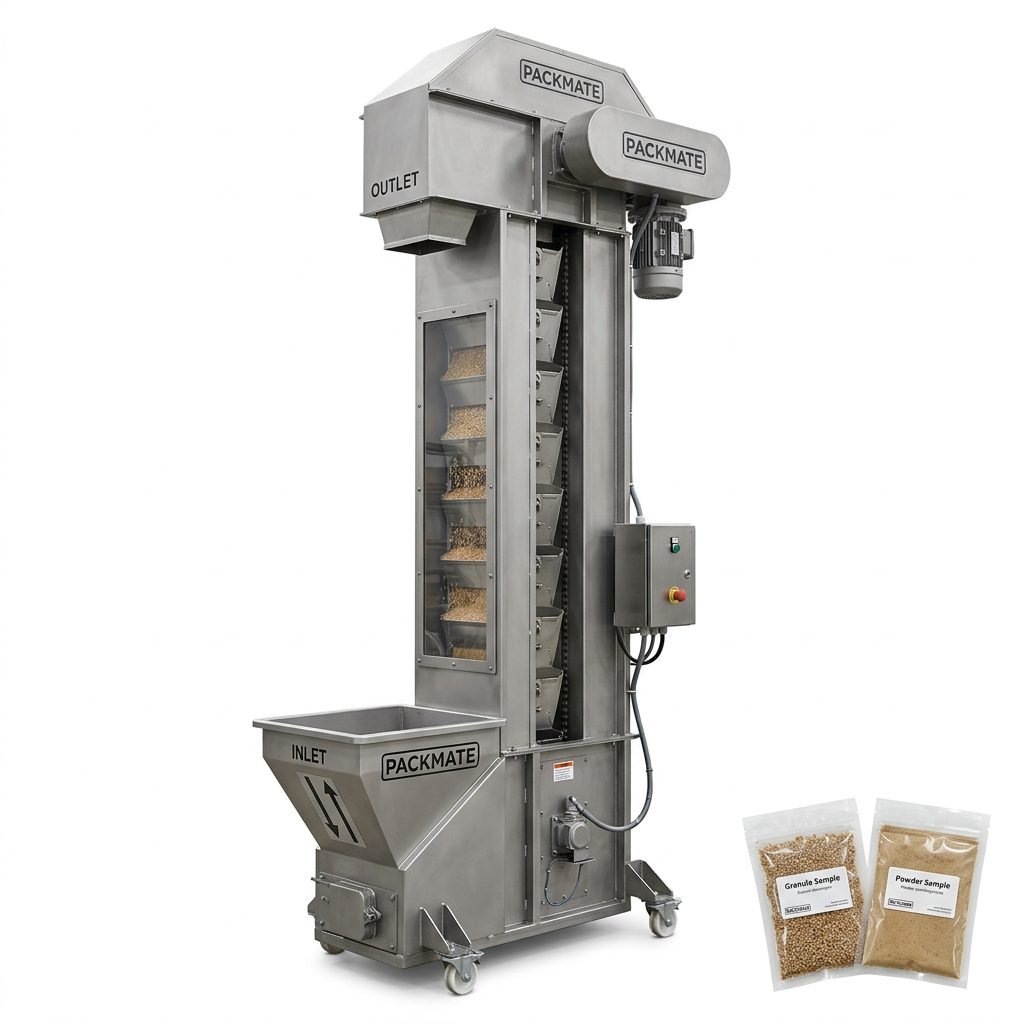
Heavy-duty bucket elevator ensures efficient vertical conveying of granules and powders with high capacity. Durable construction reduces downtime and maintenance costs. Ideal for industrial applications, boosting productivity and material handling reliability.

Product Details

Heavy-Duty Bucket Elevator for Granules and Powders

Packmate’s Heavy-Duty Bucket Elevator is engineered for the high-capacity vertical conveying of granular and powdered materials in demanding industrial environments. As a core component in automated production lines, this robust system seamlessly integrates with feeding, processing, and packaging machinery to ensure a continuous and efficient material flow. Built with durability and reliability at its core, it is designed to handle a wide range of bulk densities and material characteristics, from fine, aerated powders to coarse, abrasive granules. This elevator is the ideal solution for operations looking to optimize floor space, minimize manual handling, and enhance overall production throughput with a dependable, low-maintenance conveying system.

Product Features

Our vertical conveying system incorporates advanced engineering to deliver superior performance and longevity.

  • Heavy-Duty Construction: Fabricated from high-grade stainless steel or carbon steel, the frame, buckets, and chain/belt assembly are built to withstand continuous operation and resist wear, corrosion, and impact.
  • High-Capacity Performance: Engineered for large-volume transfer, featuring optimized bucket design and drive power to move significant quantities of material per hour with consistent speed and minimal spillage.
  • Gentle Material Handling: The precision-engineered bucket design and smooth operation ensure minimal degradation, dust generation, or separation of blended materials, preserving product integrity.
  • Sealed & Dust-Free Operation: Equipped with effective sealing gaskets and dust containment features to maintain a clean production environment, crucial for food, pharmaceutical, and chemical applications.
  • Easy Maintenance & Cleaning: Designed with accessibility in mind, featuring inspection panels, easy-release mechanisms, and a smooth, crevice-free interior for quick cleaning and routine maintenance, reducing downtime.
  • Adaptable & Modular Design: Customizable in height, bucket size, material, and discharge options to perfectly match specific material properties and plant layout requirements. Can be integrated as a standalone unit or as part of a complete Packmate turnkey line.
  • Intelligent Control Integration: Compatible with modern PLC control systems, allowing for automated start/stop, speed regulation, and interlocking with upstream/downstream equipment for synchronized line operation.

Technical Specifications

The following table outlines standard specifications. All parameters can be customized to suit your application.

Parameter Specification Range / Details
Material Types Granules, Powders, Pellets, Flakes, Seeds
Standard Capacity Up to 50 m3/h (Customizable)
Lifting Height 2m – 20m (Customizable)
Bucket Material Stainless Steel (304/316), Carbon Steel, Polyethylene
Conveying Element High-Strength Steel Chain or Abrasion-Resistant Belt
Frame Material Powder-Coated Carbon Steel or Stainless Steel
Drive Power 1.5 kW – 7.5 kW (Depending on capacity & height)
Inlet/Outlet Options Flanged, Custom hopper, Flexible connections
Control System Local Control Panel, PLC Integration Ready
Safety Features Emergency Stop, Inspection Doors, Overload Protection

Application Areas

Packmate’s Heavy-Duty Bucket Elevator is versatile and finds essential use across multiple industries requiring reliable vertical transport.

  • Food & Beverage: Conveying sugar, salt, flour, grains, coffee beans, spices, milk powder, and snack items within processing and packaging lines.
  • Pharmaceutical & Nutraceuticals: Handling powdered active ingredients, excipients, granules for tableting, and encapsulated products in controlled environments.
  • Chemical & Plastics: Transporting resin pellets, compound powders, fertilizers, pigments, and other industrial chemicals.
  • Agriculture & Feed: Moving animal feed pellets, seeds, grains, and processed agricultural products.
  • Building Materials: Elevating cement, sand, gypsum, and other granular construction materials.

As part of Packmate’s comprehensive portfolio, this bucket elevator can be seamlessly supplied as a standalone unit or integrated into a complete, intelligent packaging production line, backed by our over 30 years of expertise in automation for granules and powders.

Need A High-Quality Packaging Production Line?

Our experts are ready to help you choose the right machine.

Related Articles

Request Your Free Quote Anytime

Our experts are available 24/7 to support you. Whatever packaging solution you need, we can design and manufacture it to meet your exact requirements.

Contact Us Now

Our specialists will get back to you within 10 minutes.