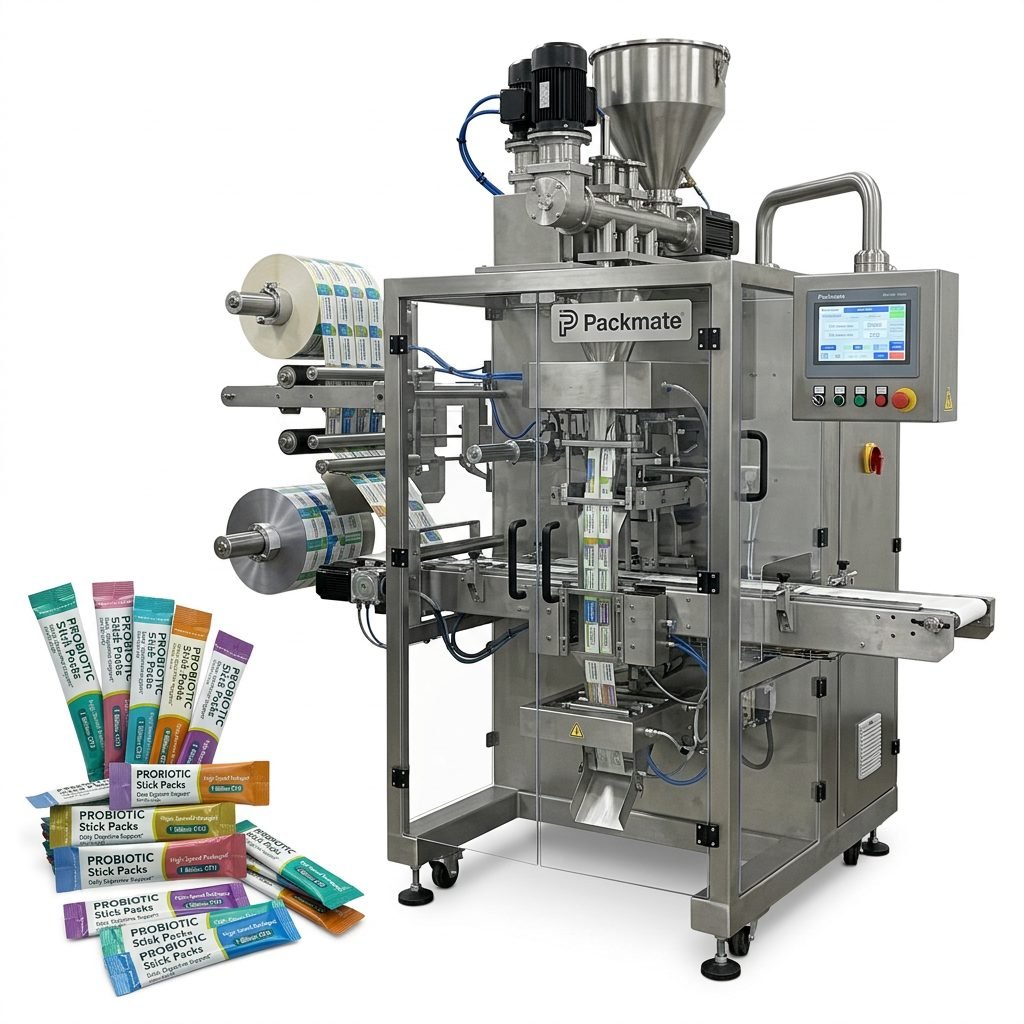
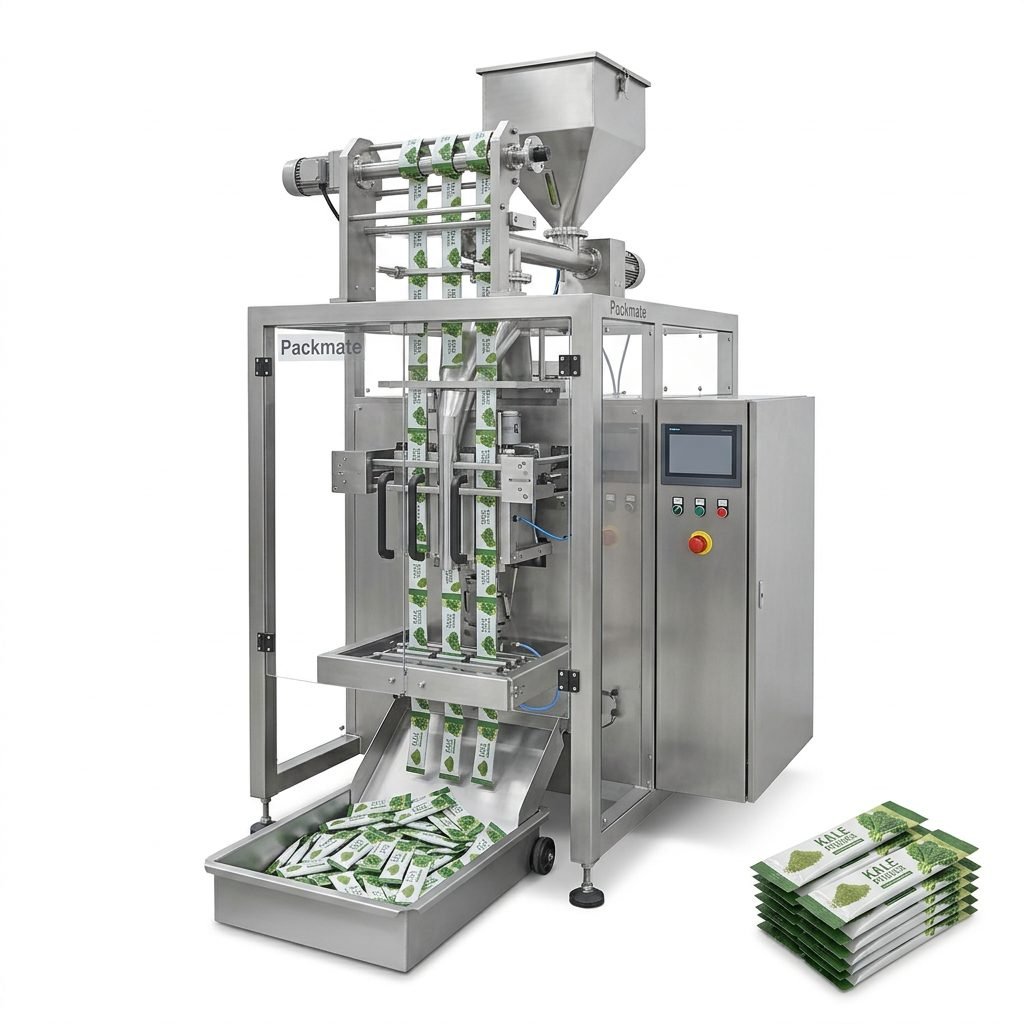
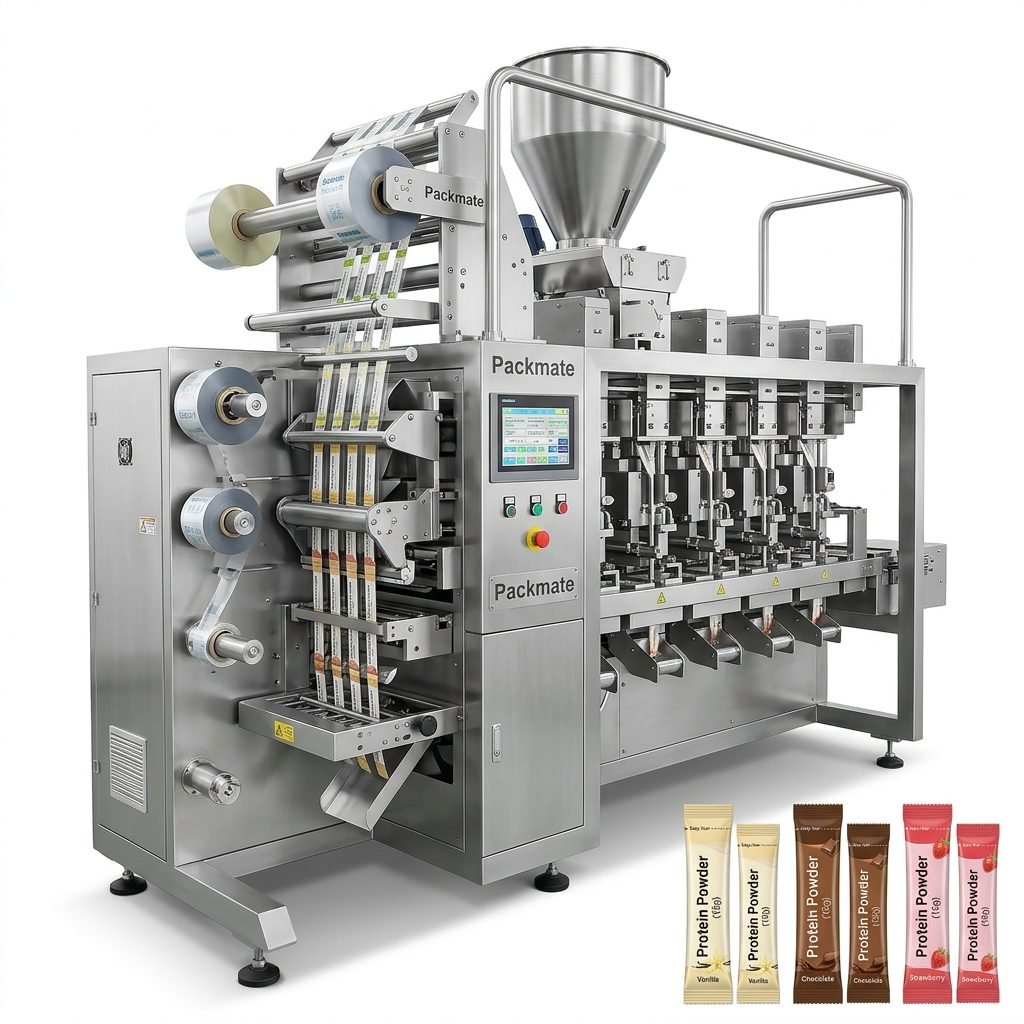
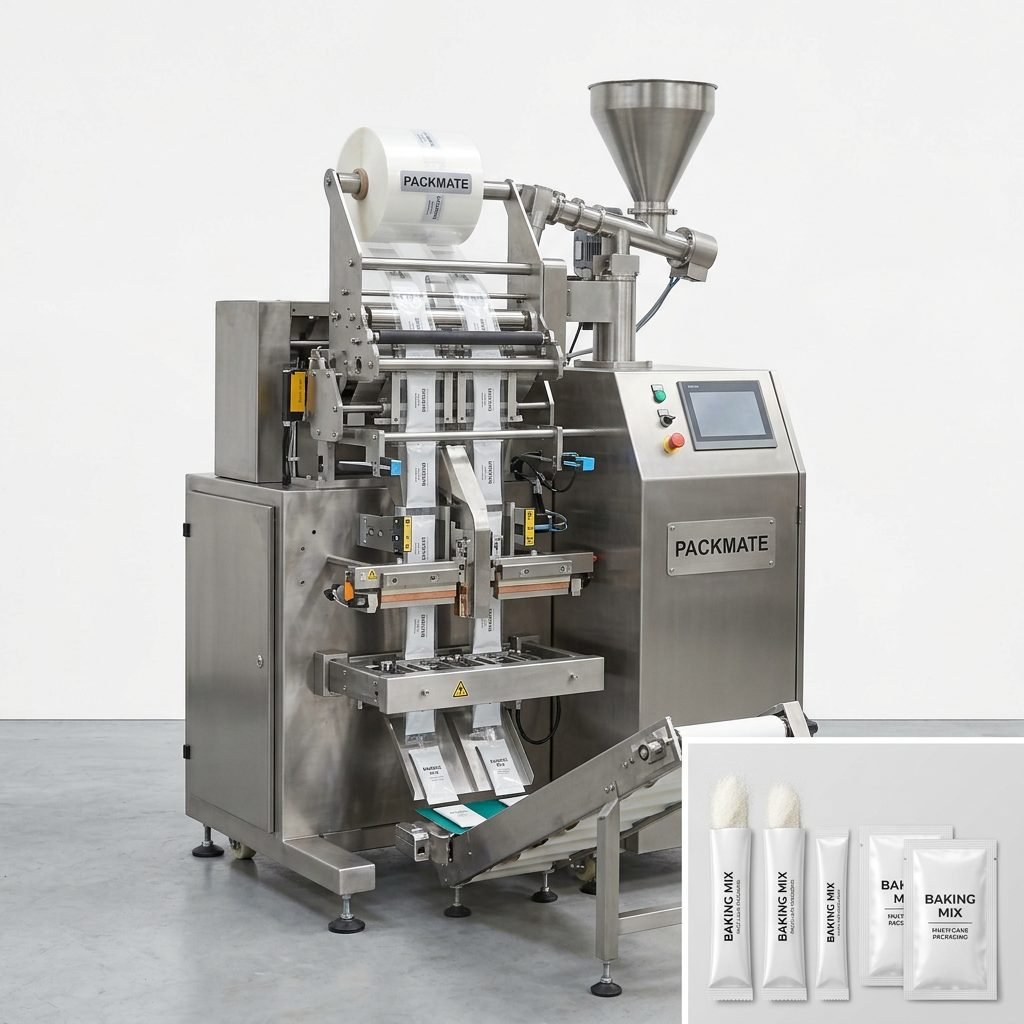
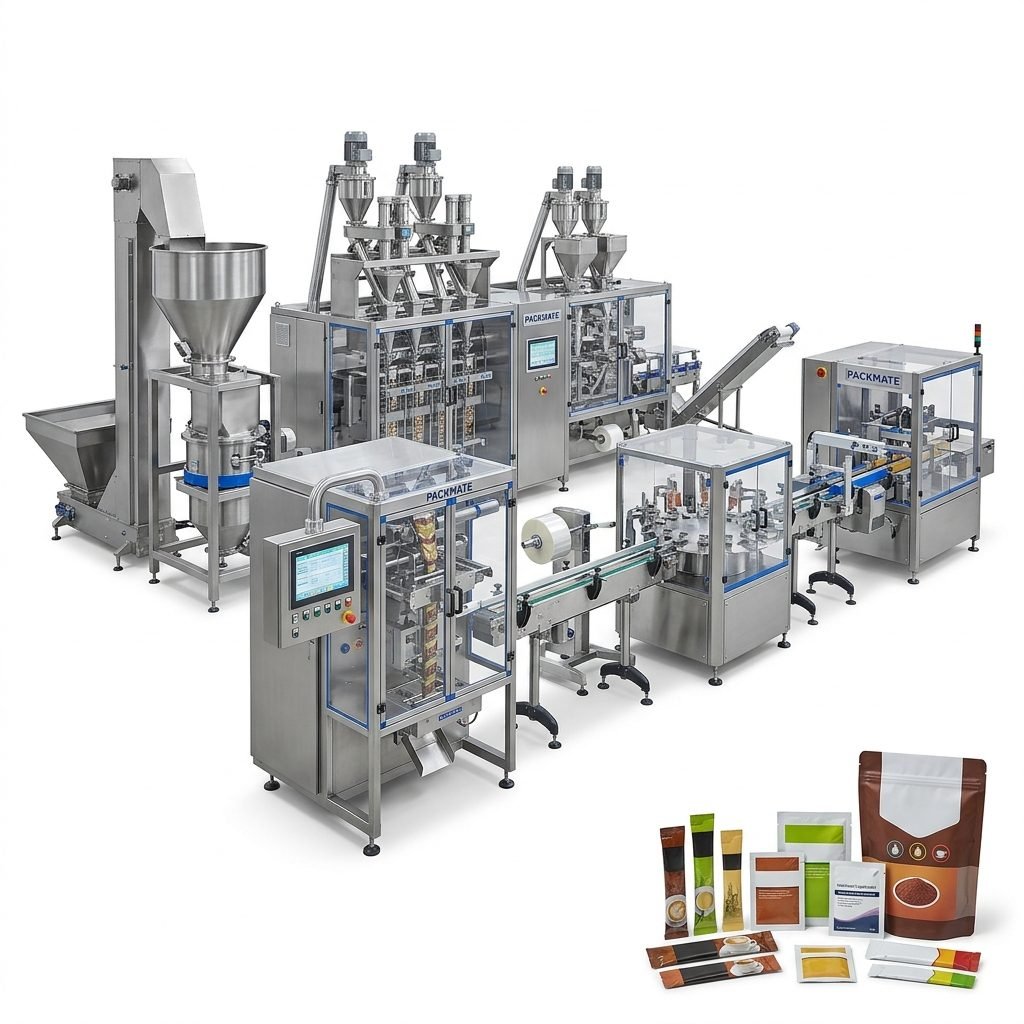
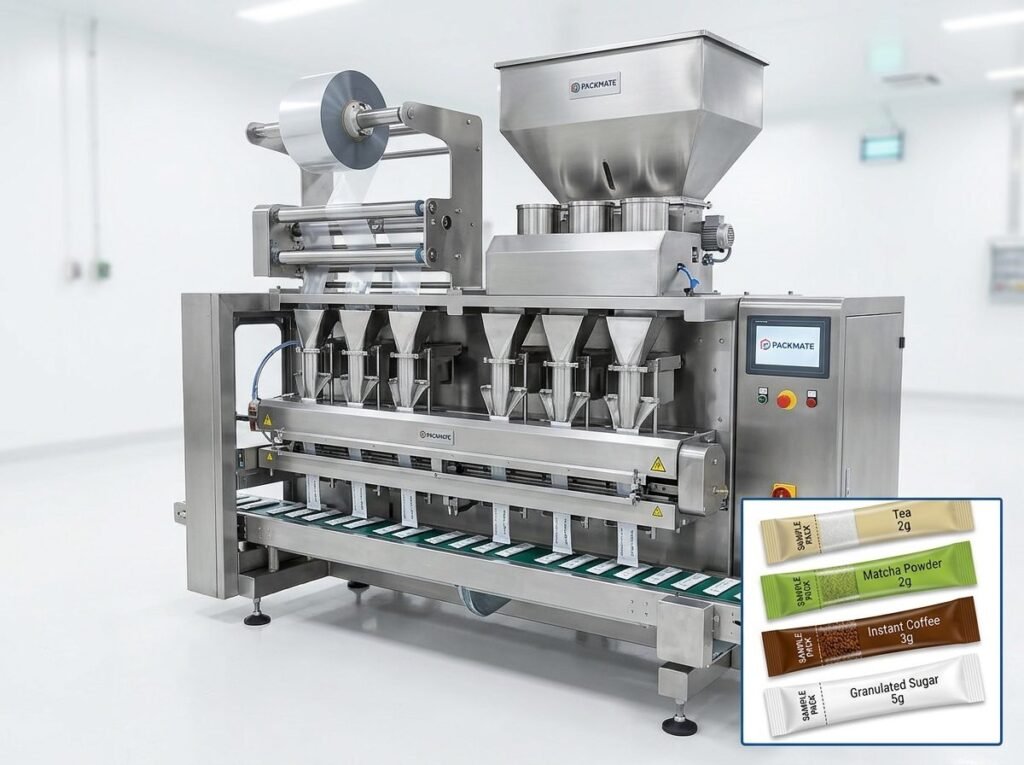
In today’s competitive global market, the efficiency and reliability of your packaging line are not just operational concerns—they are critical business advantages. For industries where product integrity, hygiene, and speed to market are paramount, such as food, pharmaceuticals, and health products, investing in a robust wholesale road gate packaging line is a strategic decision. These comprehensive solutions encompass the entire journey from raw material filling to final palletizing, ensuring a seamless, automated, and high-throughput production process. This article explores the essential components, benefits, and considerations for implementing such a line, with insights from industry leaders like Packmate (GuangDong) Co., Ltd..
The Anatomy of a Modern Road Gate Packaging Line
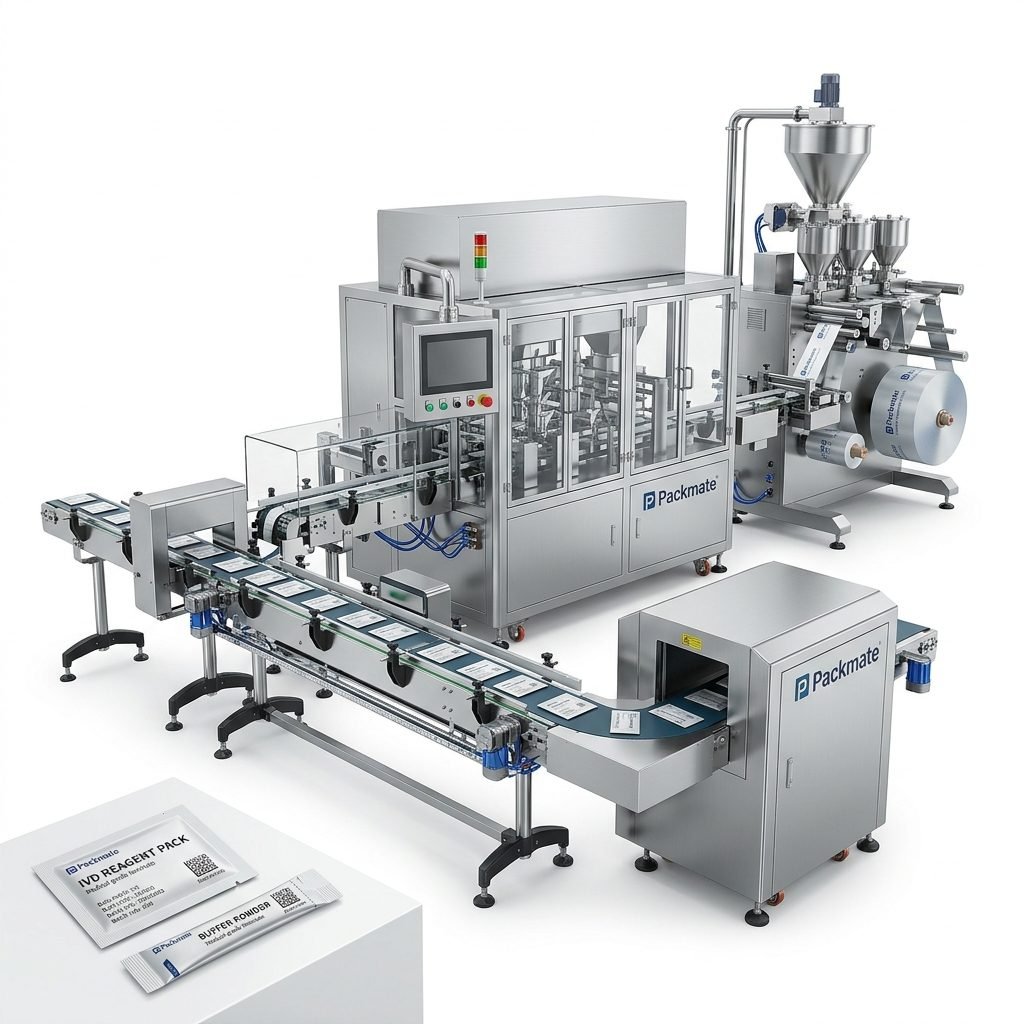
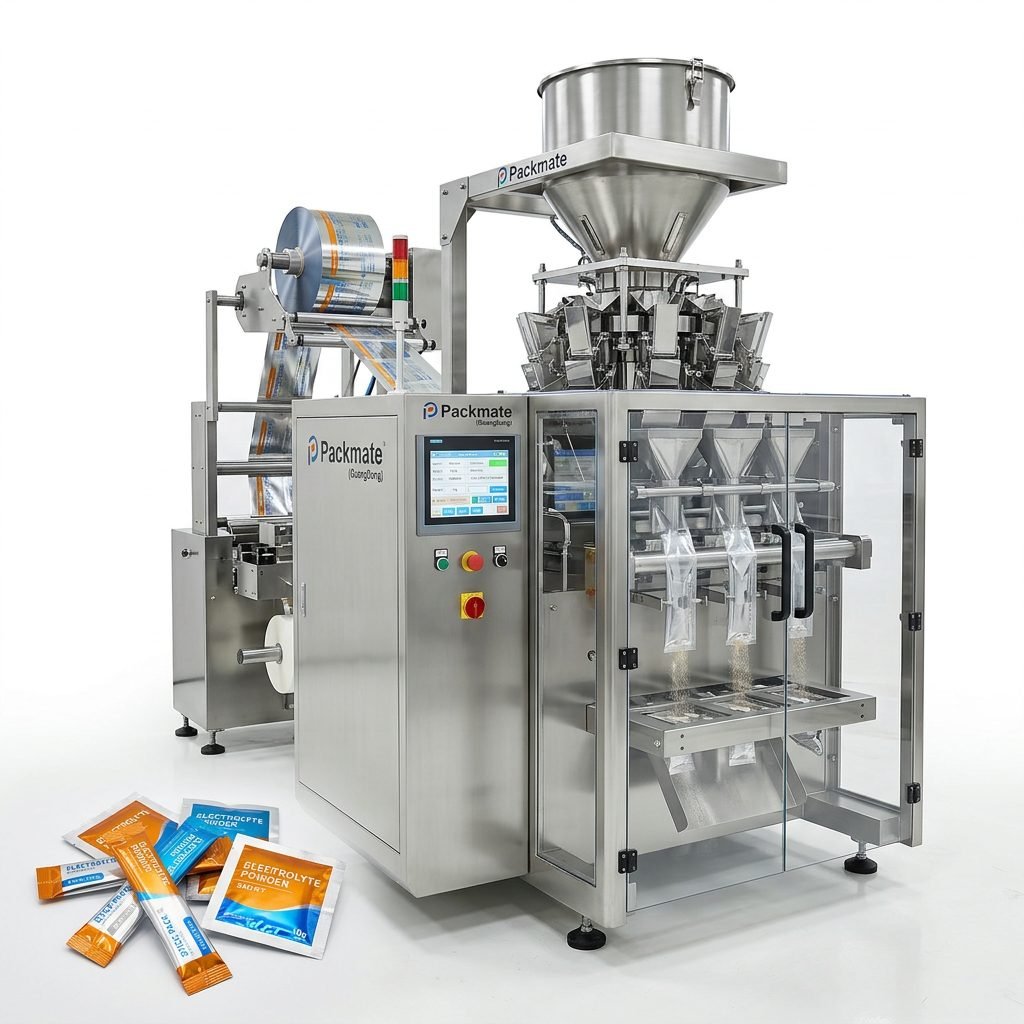
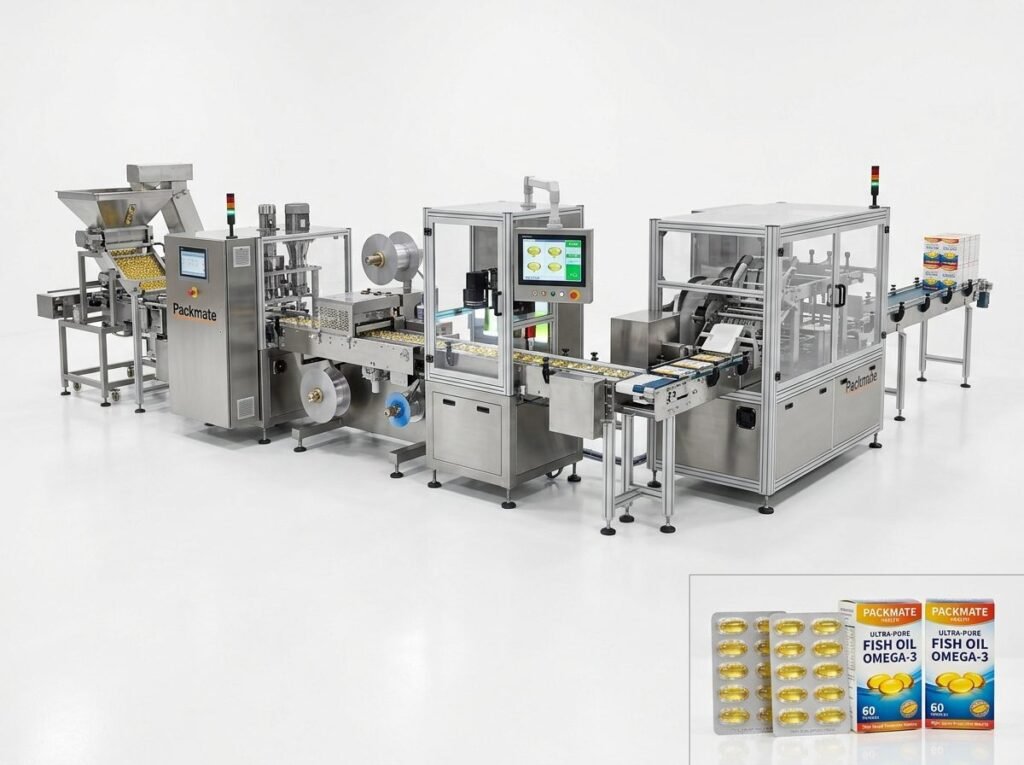
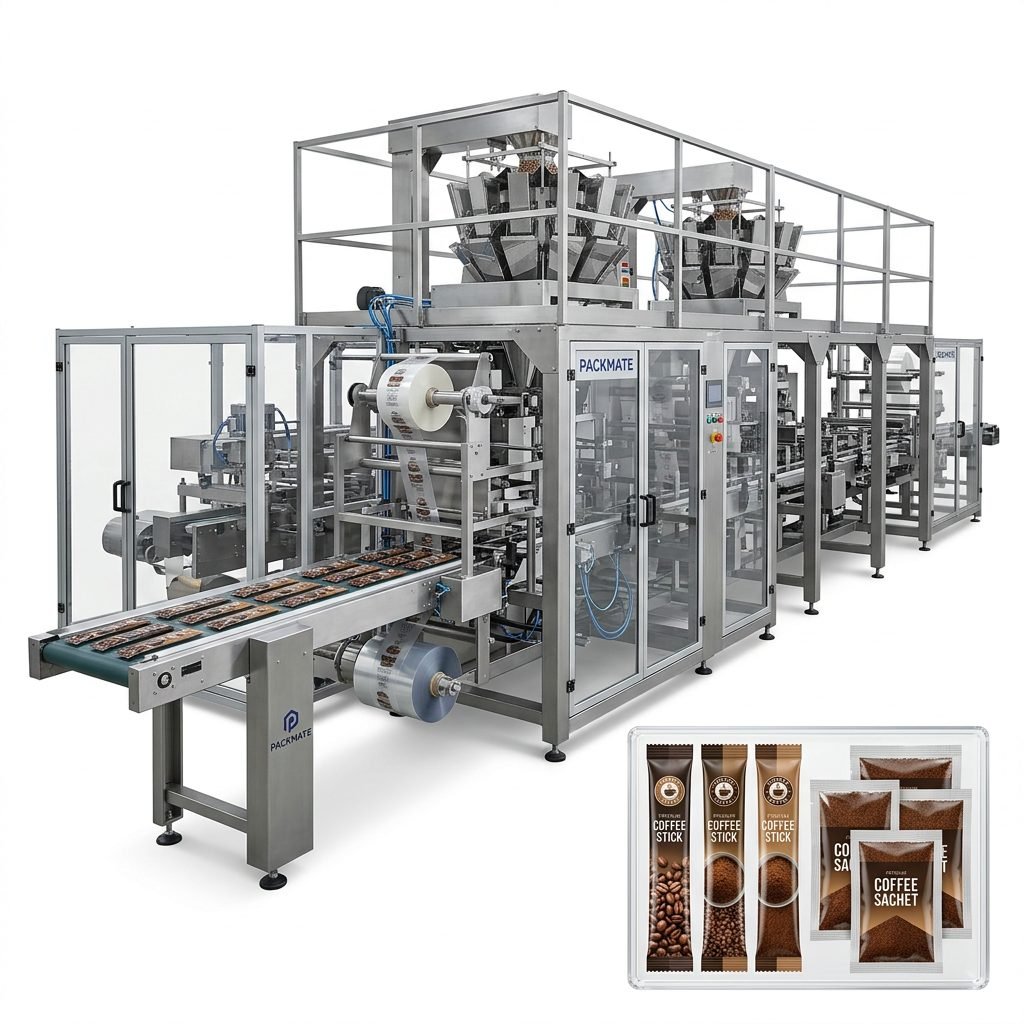
A complete road gate packaging line is a symphony of synchronized machinery. It typically begins with product feeding and dosing systems, ensuring precise measurement—a non-negotiable requirement in pharma and premium food sectors. This is followed by the core packaging machines, which could be high-speed sachet machines, multi-lane stick pack machines for portion control, or large bag fillers for bulk products. The sealed packages then travel through checkweighers and metal detectors for quality assurance before being collated, cartoned, and finally palletized for shipment. The “road gate” concept signifies a turnkey solution: a single, integrated pathway your product travels from start to finish, managed and supplied by one trusted partner.
Key Advantages for Target Industries
➤ For the Food Industry: Speed and hygiene are king. A fully automated line minimizes human contact, reducing contamination risk. It ensures consistent package weight and seal integrity, which is crucial for perishables and snacks. High-speed capabilities, such as those offered by multi-lane systems, meet the demands of large-scale production runs for items like coffee sticks, sugar sachets, or seasoning powders.
➤ For the Pharmaceutical Industry: Compliance and precision are absolute. Packaging lines must adhere to strict GMP (Good Manufacturing Practice) standards. Solutions include dust-free environments, precision dosing for powders and granules, and impeccable traceability systems. The reliability of the machinery, backed by thorough validation support, is critical to avoid costly downtime and ensure patient safety.
➤ For Health & Nutraceutical Products: This sector often blends the needs of food and pharma. Products like protein powders, vitamin supplements, and herbal teas require attractive, tamper-evident packaging that also preserves product potency. Versatile lines that can handle different product forms (powders, granules, liquids) and package types (stick packs, sachets, bottles) provide the agility needed for a dynamic market.
Why Choose a Wholesale Turnkey Solution?
Procuring individual machines from different vendors creates a complex web of integration challenges, potential compatibility issues, and multiple points of responsibility. A wholesale turnkey solution from a single provider like Packmate simplifies everything. It means one point of contact for design, manufacturing, installation, training, and after-sales service. This holistic approach guarantees that all components are engineered to work in perfect harmony, optimizing line efficiency (OEE) and minimizing bottlenecks. Furthermore, it often results in significant cost savings in terms of project management, spare parts inventory, and long-term maintenance.
Customization: The Heart of an Effective Line
No two production facilities are identical. The true value of a specialist provider lies in their ability to customize. This includes tailoring machine speeds, choosing specific sealing technologies (such as ultrasonic sealing for sensitive products), integrating specific coding and serialization equipment, and designing layouts to fit existing factory floorspace. Reviewing real-world case studies can provide tangible proof of a supplier’s capability to deliver tailored solutions.
Evaluating Your Packaging Line Partner
Selecting the right partner is as important as selecting the right machinery. Key evaluation criteria should include:
- Proven Industry Experience: Look for a track record in your specific sector (food, pharma, health).
- Technical & Engineering Depth: Assess their R&D capability and willingness to engineer custom solutions.
- Manufacturing Quality: A modern facility with advanced equipment, like Packmate’s 20,000㎡ plant, is a strong indicator of quality control.
- Global Support Network: Ensure they can provide timely technical support, spare parts, and service wherever your operations are located. Explore their commitment to comprehensive service offerings.
- Financial Stability: A partner with a long history, such as Packmate’s 22+ years of development, offers security for long-term partnerships.
The Future: Smart Packaging Lines
The next frontier is the integration of Industry 4.0 principles. Smart packaging lines feature IoT sensors for predictive maintenance, real-time production data dashboards for remote monitoring, and AI-driven quality control systems that learn and adapt. These technologies minimize unplanned downtime, optimize production schedules, and provide unparalleled transparency across the supply chain. Investing in a solution from a forward-thinking provider ensures your operation remains competitive and future-proof.
Implementing a wholesale road gate packaging line is a significant capital investment, but one that pays dividends in efficiency, compliance, brand protection, and scalability. By partnering with an experienced and innovative provider who understands the unique demands of the food, pharma, and health product industries, you secure more than just machinery—you secure a foundation for sustainable growth and market leadership. For a deeper understanding of what drives such companies, consider reviewing their core mission and vision.
Frequently Asked Questions (FAQs)
1. What is the lead time for a complete turnkey packaging line?
Lead times vary significantly based on line complexity, customization level, and current production schedules. A standard line might take 3-6 months from order to delivery, while highly customized systems for pharmaceuticals may require 6-12 months. Detailed project planning with your supplier will establish a clear timeline.
2. Can your packaging line handle a switch between different product types?
Yes, many modern lines are designed for changeover flexibility. Quick-change parts, programmable logic controller (PLC) recipes, and modular design allow for efficient switching between similar product forms (e.g., different powder flavors). However, switching between vastly different formats (e.g., from liquids to granules) may require more extensive reconfiguration.
3. How do you ensure the line meets pharmaceutical GMP standards?
Reputable suppliers design machines with GMP in mind: using stainless steel AISI 304/316, sanitary finishes, easy-clean designs, and validated cleaning procedures. They provide documentation packages (DQ, IQ, OQ, PQ) to support your validation process and often have experience working within regulated environments.
4. What kind of after-sales support and training is provided?
A comprehensive support package should include on-site installation supervision, detailed operational and maintenance training for your engineers, a clear warranty period, access to spare parts, and remote/on-call technical support. Ensure this is clearly defined in your agreement.
5. Are your machines CE certified or compliant with other international standards?
Leading manufacturers ensure their machines comply with relevant international safety and quality standards, such as CE for Europe, UL for North America, or GB standards for China. Always request to see relevant certifications for the specific models you are purchasing.